Bitzer Condensing Unit Factory Guide

All Categories

bitzer condensing unit factory

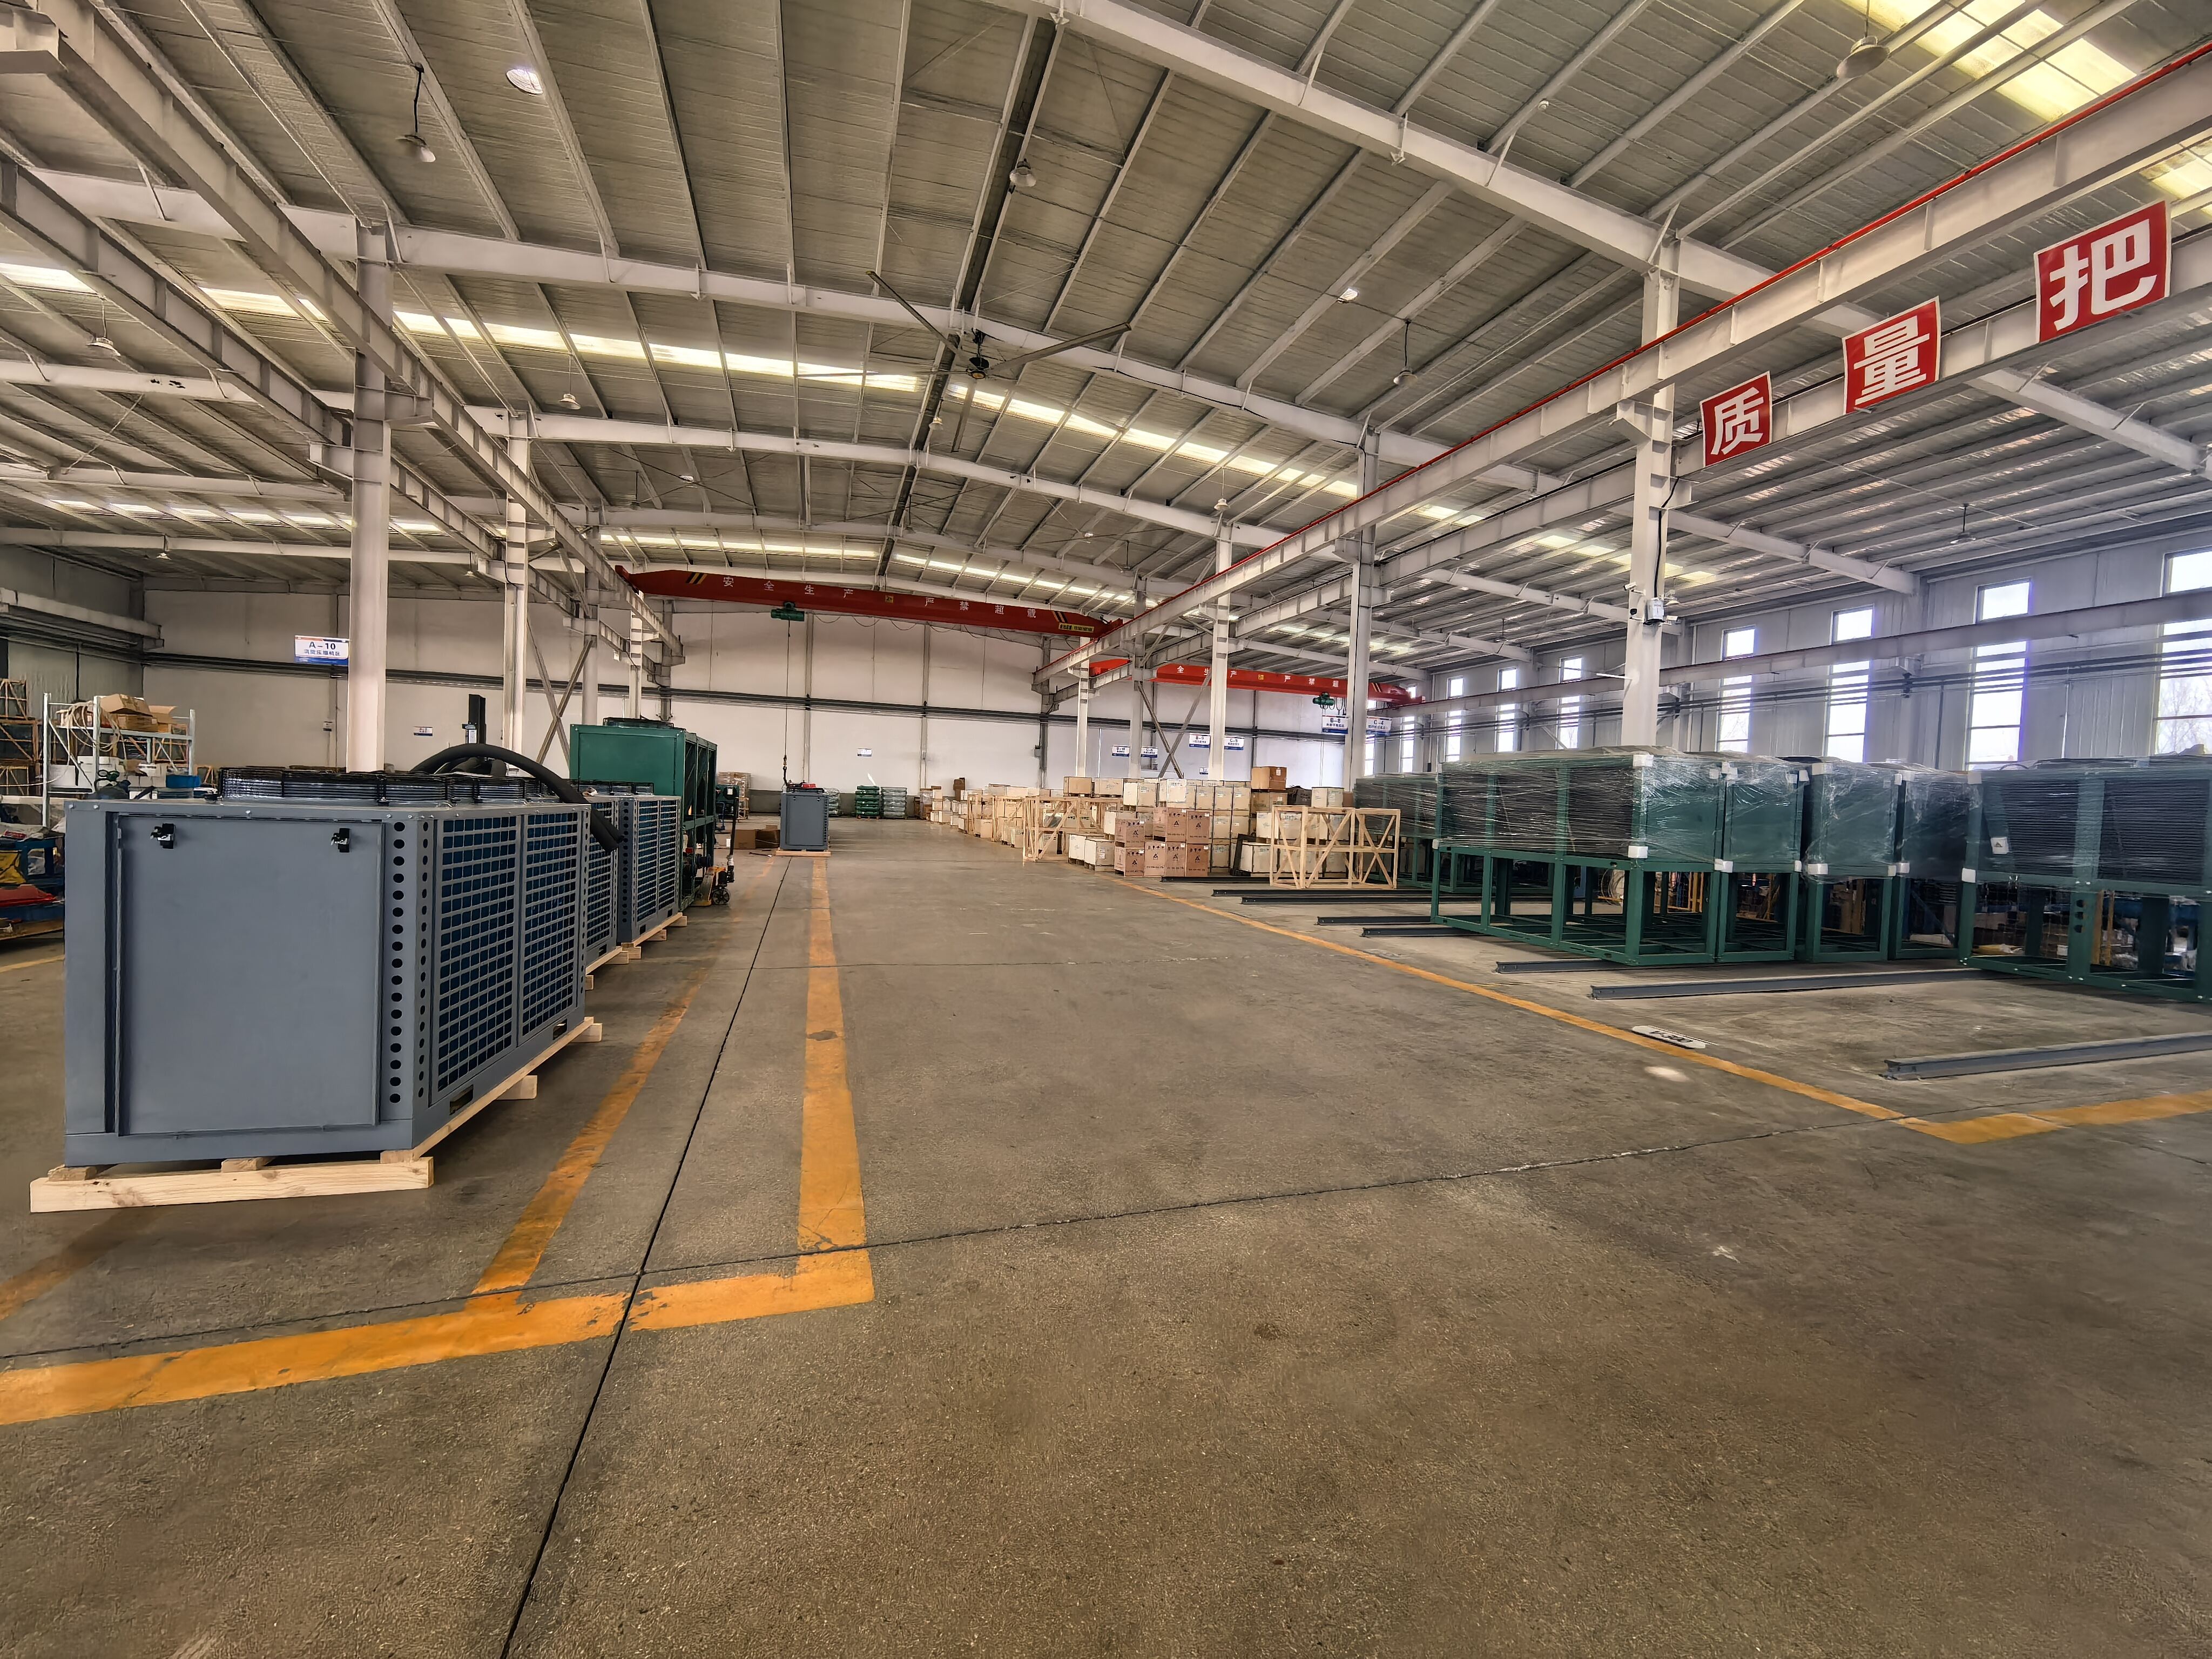
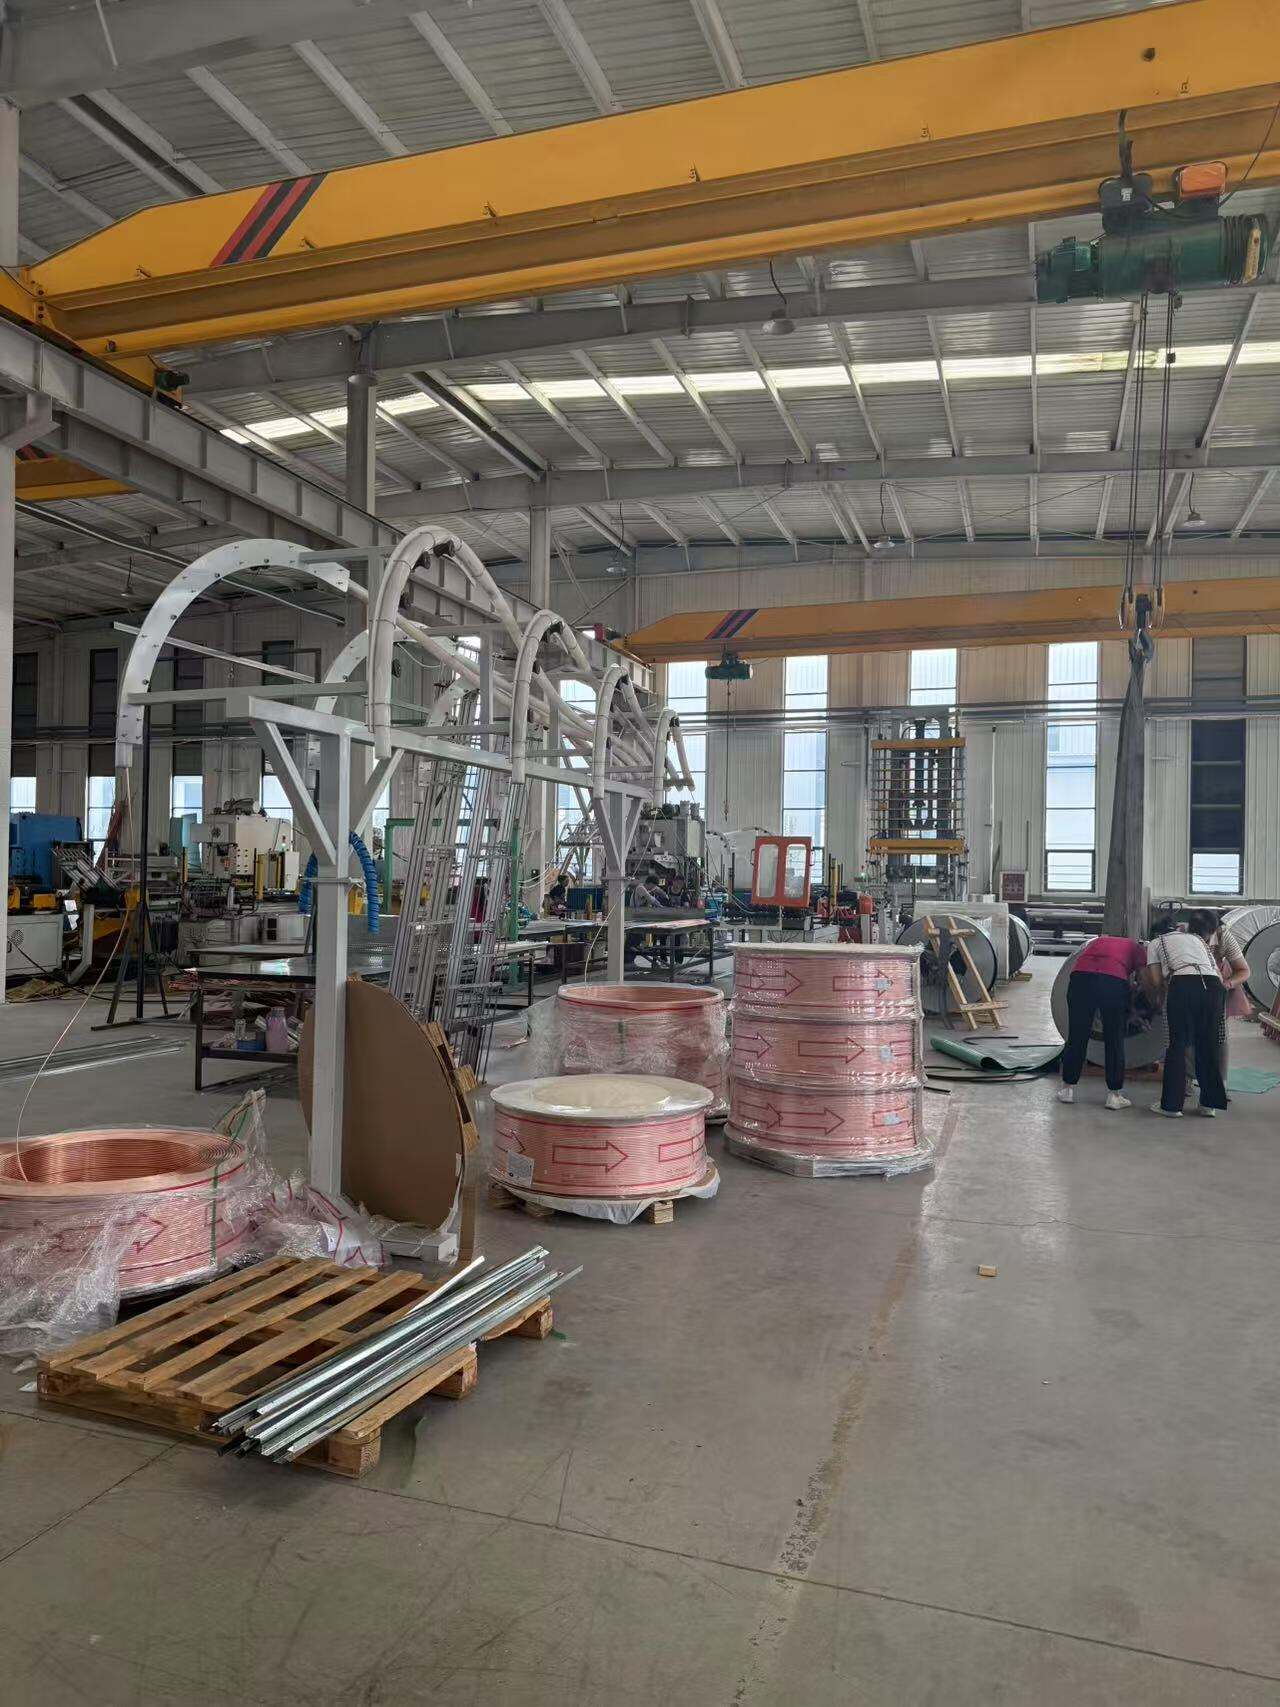
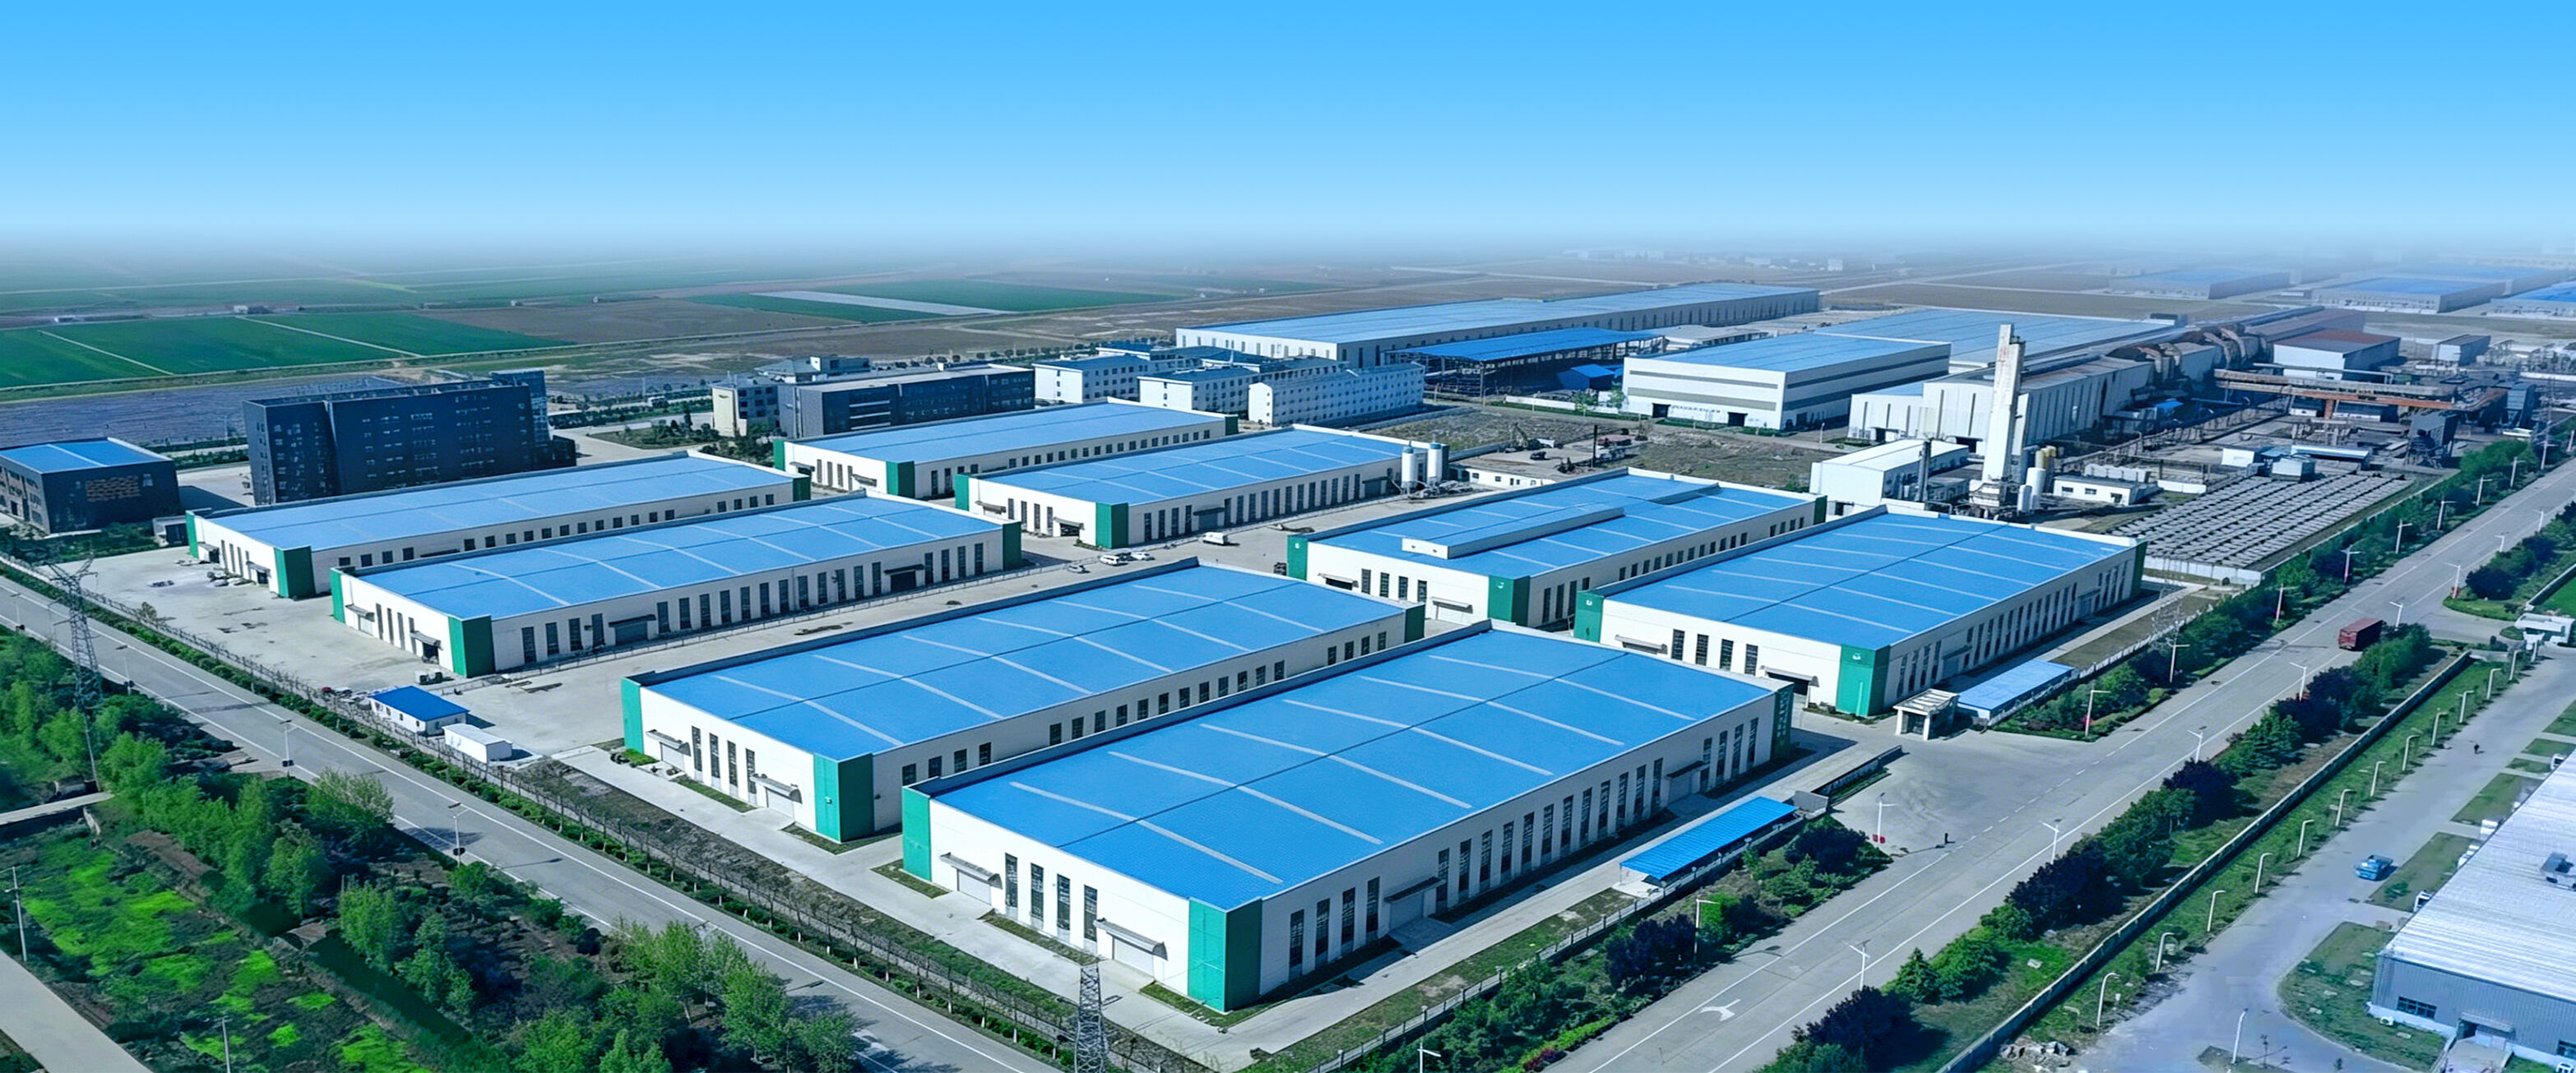
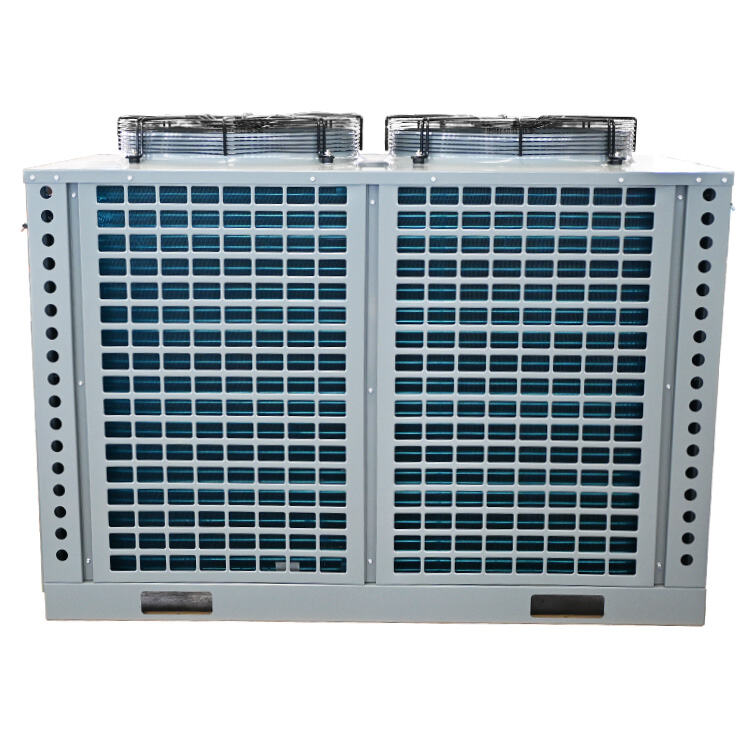
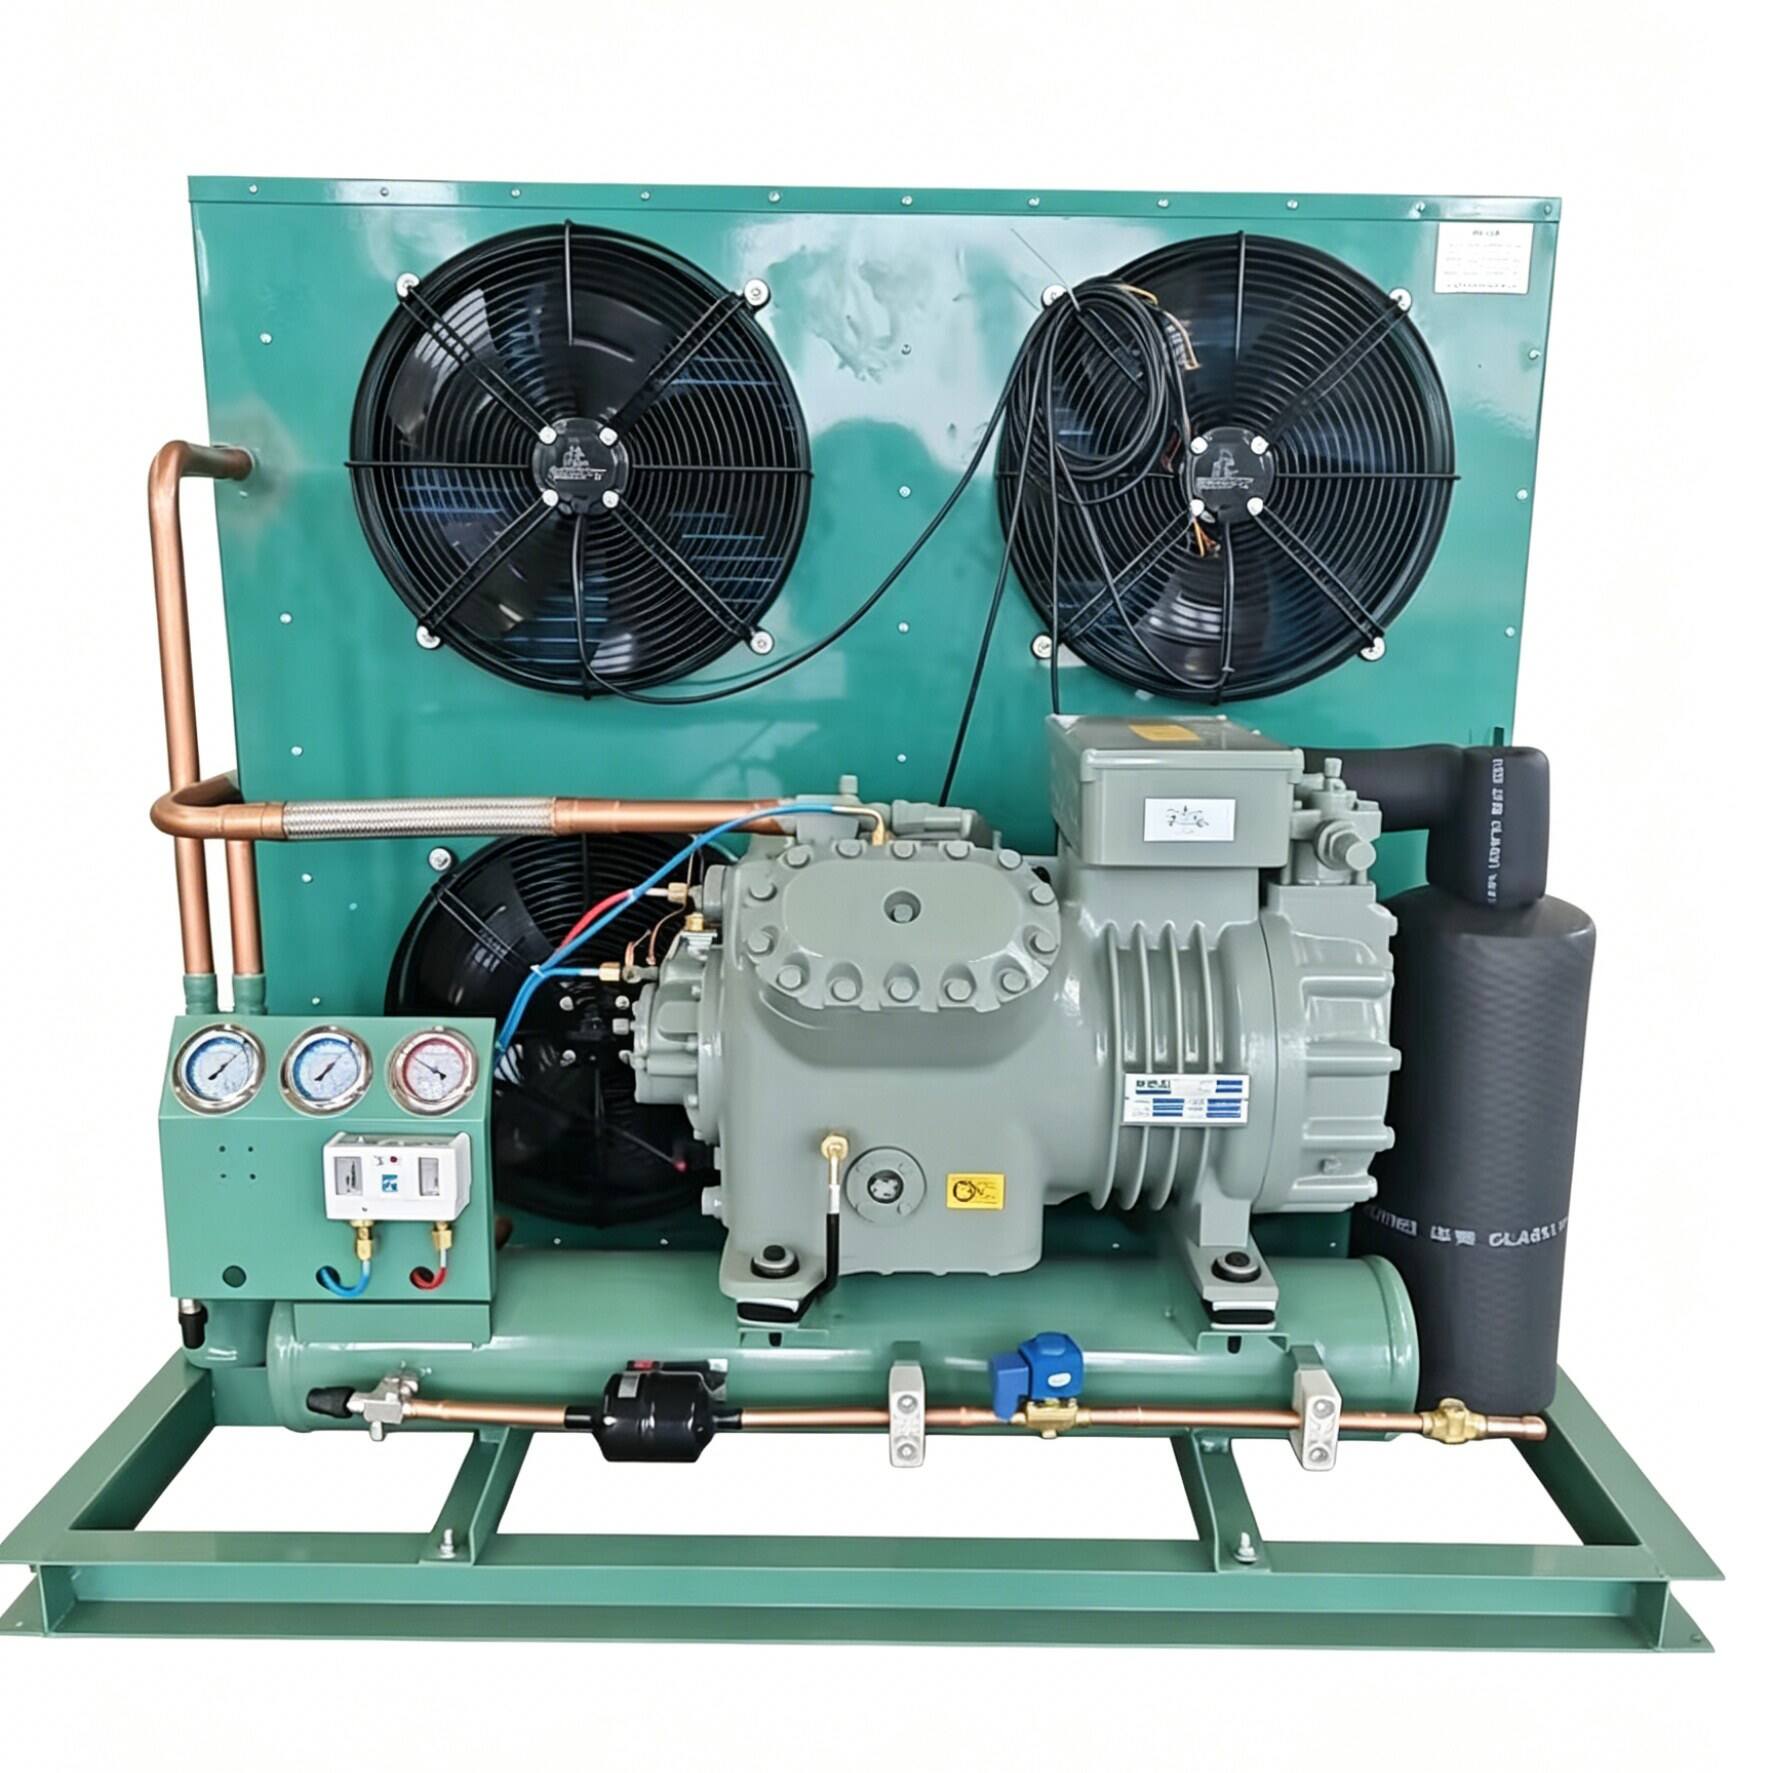
A Bitzer condensing unit factory specializes in manufacturing high-performance refrigeration systems that serve as the heart of commercial and industrial cooling applications. These facilities produce complete condensing units that integrate compressors, condensers, receivers, and control systems into ready-to-install packages. The Bitzer condensing unit factory employs advanced production techniques to ensure each unit meets stringent quality standards for reliability and efficiency. The main function of these units is to remove heat from refrigeration systems by compressing refrigerant gas and condensing it into liquid form through heat exchange processes. Technological features include precision-engineered Bitzer semi-hermetic and scroll compressors, optimized condenser coil designs for maximum heat transfer, and integrated control systems that monitor performance parameters. Modern facilities incorporate automated testing procedures to verify operational efficiency, leak detection, and system integrity before shipment. Applications span across supermarket refrigeration, cold storage warehouses, food processing plants, pharmaceutical facilities, and industrial cooling systems. The Bitzer condensing unit factory produces various configurations including air-cooled and water-cooled models, with cooling capacities ranging from small commercial applications to large industrial installations. These factories maintain strict environmental controls during manufacturing to ensure consistent product quality and implement sustainable practices in production processes. Each unit undergoes comprehensive performance testing under simulated operating conditions to guarantee reliable operation in diverse climates and demanding applications.
New Products

Choosing products from a Bitzer condensing unit factory delivers significant operational advantages that directly impact your bottom line. First, these units offer exceptional energy efficiency that reduces electricity consumption by up to thirty percent compared to conventional systems, translating into substantial cost savings over the equipment lifespan. The manufacturing precision ensures consistent cooling performance with minimal temperature fluctuation, protecting your valuable inventory from spoilage and quality degradation. Reliability stands as a cornerstone benefit, with robust construction and premium components minimizing unexpected breakdowns and costly downtime. The Bitzer condensing unit factory implements rigorous quality control measures throughout production, meaning you receive equipment that operates dependably for years with routine maintenance. Installation simplicity represents another practical advantage, as these pre-assembled units arrive ready for quick integration into your refrigeration system, reducing installation time and labor costs. Maintenance accessibility is thoughtfully designed into every unit, with serviceable components positioned for easy access, allowing technicians to perform routine checks and repairs efficiently. Application versatility makes these units suitable for diverse environments, from retail food displays to large-scale cold storage operations, providing flexibility as your business grows. The factory backing ensures comprehensive technical support, readily available replacement parts, and extensive documentation that simplifies troubleshooting. Noise reduction technology incorporated during manufacturing creates quieter operation, important for customer-facing retail environments. Environmental responsibility is built into the design, with units compatible with modern low-GWP refrigerants that meet evolving regulatory requirements. Long-term value emerges through durable construction that withstands harsh operating conditions, protecting your capital investment while delivering consistent performance throughout extended service life.

Tips And Tricks

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

28

Feb

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

View More
Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

28

Feb

Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

View More
Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

28

Feb

Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

bitzer condensing unit factory

Advanced Manufacturing Excellence and Quality Assurance

Advanced Manufacturing Excellence and Quality Assurance

The Bitzer condensing unit factory distinguishes itself through state-of-the-art manufacturing processes that guarantee superior product quality. Every production stage incorporates automated precision equipment that maintains exact tolerances critical for optimal refrigeration performance. The factory implements multi-point quality inspection protocols, examining each component before assembly and conducting full-system performance validation before units leave the facility. This meticulous approach eliminates defects and ensures every Bitzer condensing unit factory product meets exact specifications. Advanced metallurgy and coating processes protect components against corrosion and environmental degradation, extending equipment lifespan significantly. The manufacturing environment maintains controlled temperature and humidity conditions that prevent contamination during assembly. Sophisticated testing chambers simulate extreme operating conditions, verifying unit performance across temperature ranges from arctic cold to tropical heat. This comprehensive quality assurance means customers receive condensing units that perform reliably from initial startup through decades of continuous operation, reducing total cost of ownership and maximizing return on investment.
Engineered Performance Optimization and Energy Efficiency

Engineered Performance Optimization and Energy Efficiency

Products from the Bitzer condensing unit factory incorporate cutting-edge engineering that maximizes cooling efficiency while minimizing energy consumption. Computational fluid dynamics modeling optimizes airflow patterns across condenser coils, enhancing heat rejection efficiency by maximizing surface area utilization. Variable speed technology adapts compressor operation to actual cooling demand, eliminating energy waste during partial load conditions that represent typical operating scenarios. The factory engineers condensing units with intelligent control systems that continuously monitor system parameters and adjust operation for peak efficiency. High-efficiency motors exceed premium efficiency standards, converting electrical input into cooling output with minimal losses. Precisely matched component sizing ensures compressors, condensers, and expansion devices work in harmony without inefficient oversizing. The Bitzer condensing unit factory tests each configuration under load conditions that replicate real-world applications, confirming published performance specifications. Advanced refrigerant circuit design minimizes pressure drops and optimizes superheat control for maximum coefficient of performance. This engineering excellence translates directly into lower operating costs, reduced environmental impact, and improved profitability for businesses operating these reliable refrigeration systems.
Comprehensive Application Flexibility and Technical Support

Comprehensive Application Flexibility and Technical Support

The Bitzer condensing unit factory produces an extensive range of configurations that address virtually any commercial or industrial refrigeration requirement. Product lines include compact units for small retail applications, medium-capacity systems for restaurants and convenience stores, and large industrial models for cold storage warehouses and food processing facilities. Temperature range versatility accommodates both medium-temperature applications like produce storage and low-temperature requirements for frozen goods. The factory offers both air-cooled and water-cooled configurations, allowing customers to select optimal solutions based on available utilities and climate conditions. Modular design philosophy enables easy capacity expansion by adding units in parallel as business needs grow. The Bitzer condensing unit factory provides comprehensive technical documentation including detailed wiring diagrams, refrigerant charging procedures, and troubleshooting guides that empower maintenance personnel. Factory-trained technical support specialists offer application assistance, helping customers select appropriate models and optimize system design. Worldwide parts distribution networks ensure replacement components arrive quickly when needed, minimizing downtime. This combination of product versatility and support infrastructure makes the Bitzer condensing unit factory the preferred choice for demanding refrigeration applications.
Bitzer Condensing Unit Factory Guide

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
Bitzer Condensing Unit Factory Guide

Copyright © 2026 Ningbo Lucky Star Import & Export Co., Ltd. All rights reserved.  -  Privacy policy