Heavy Duty Hermetic Condensing Unit Solutions

All Categories

heavy duty hermetic condensing unit

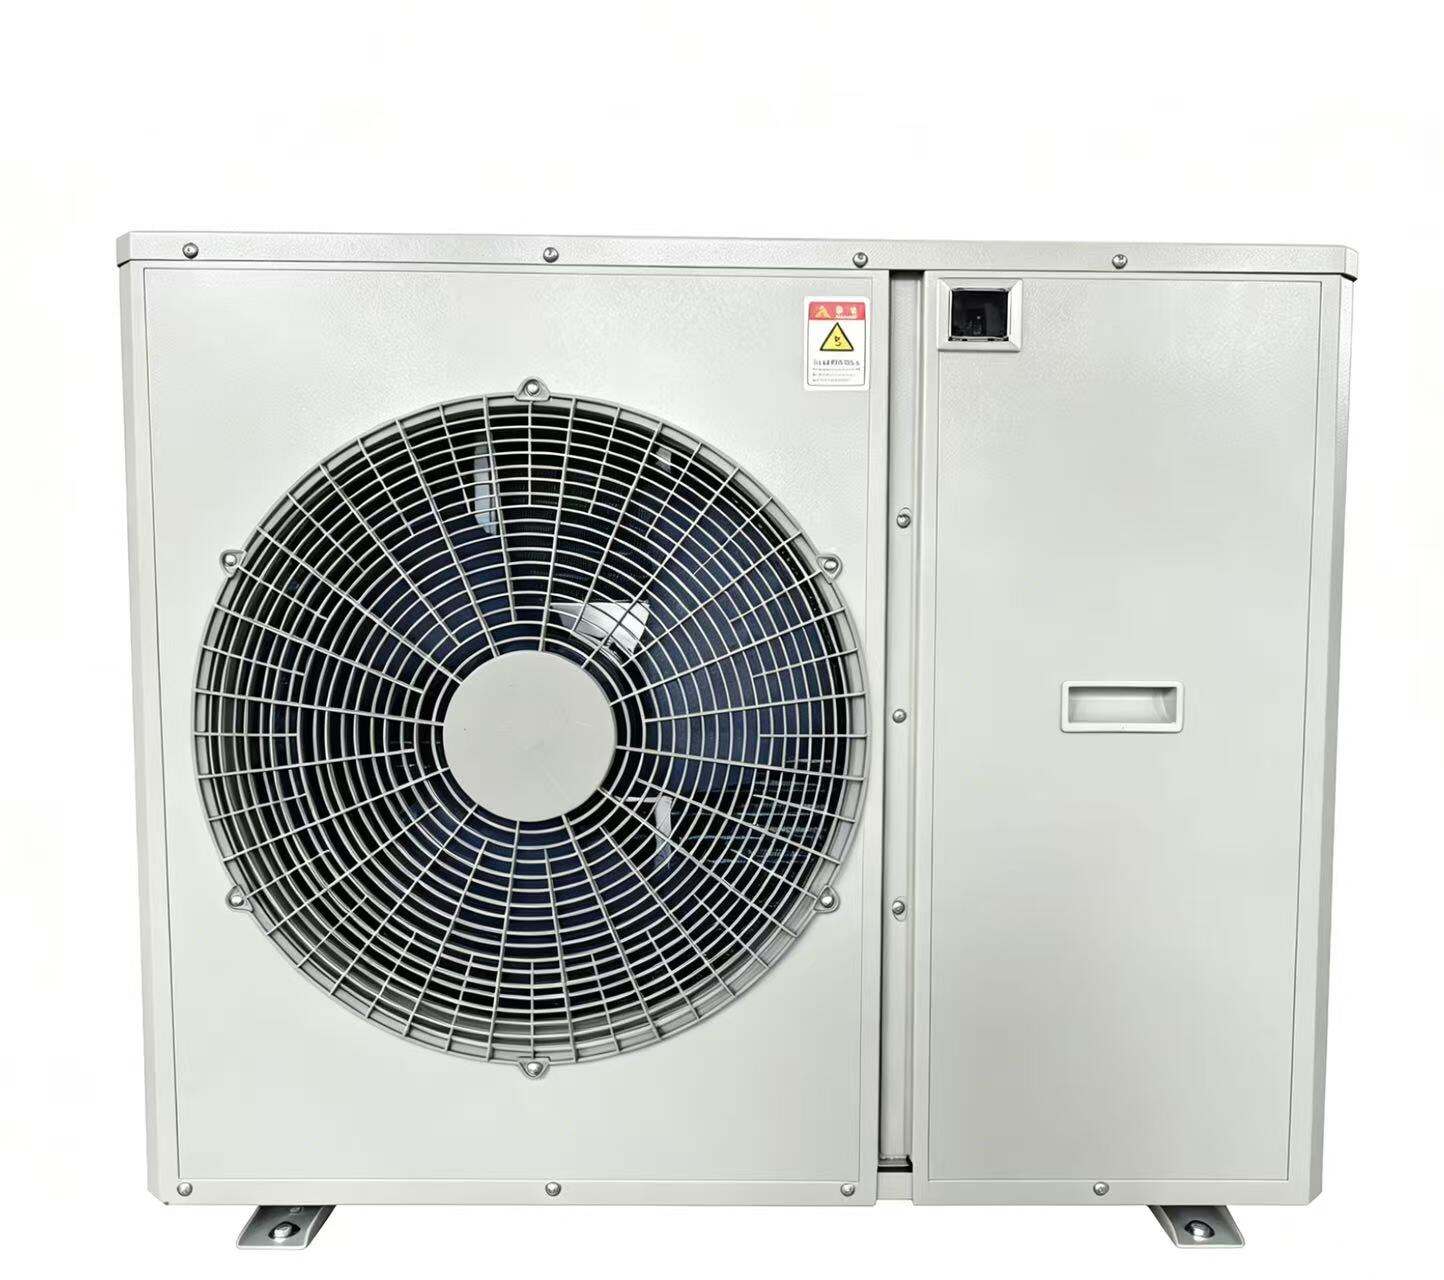
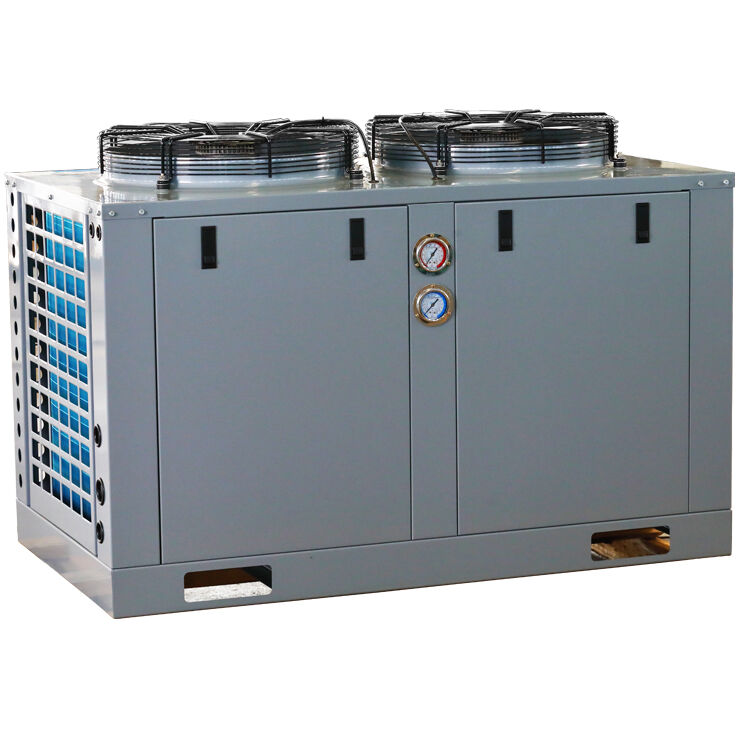
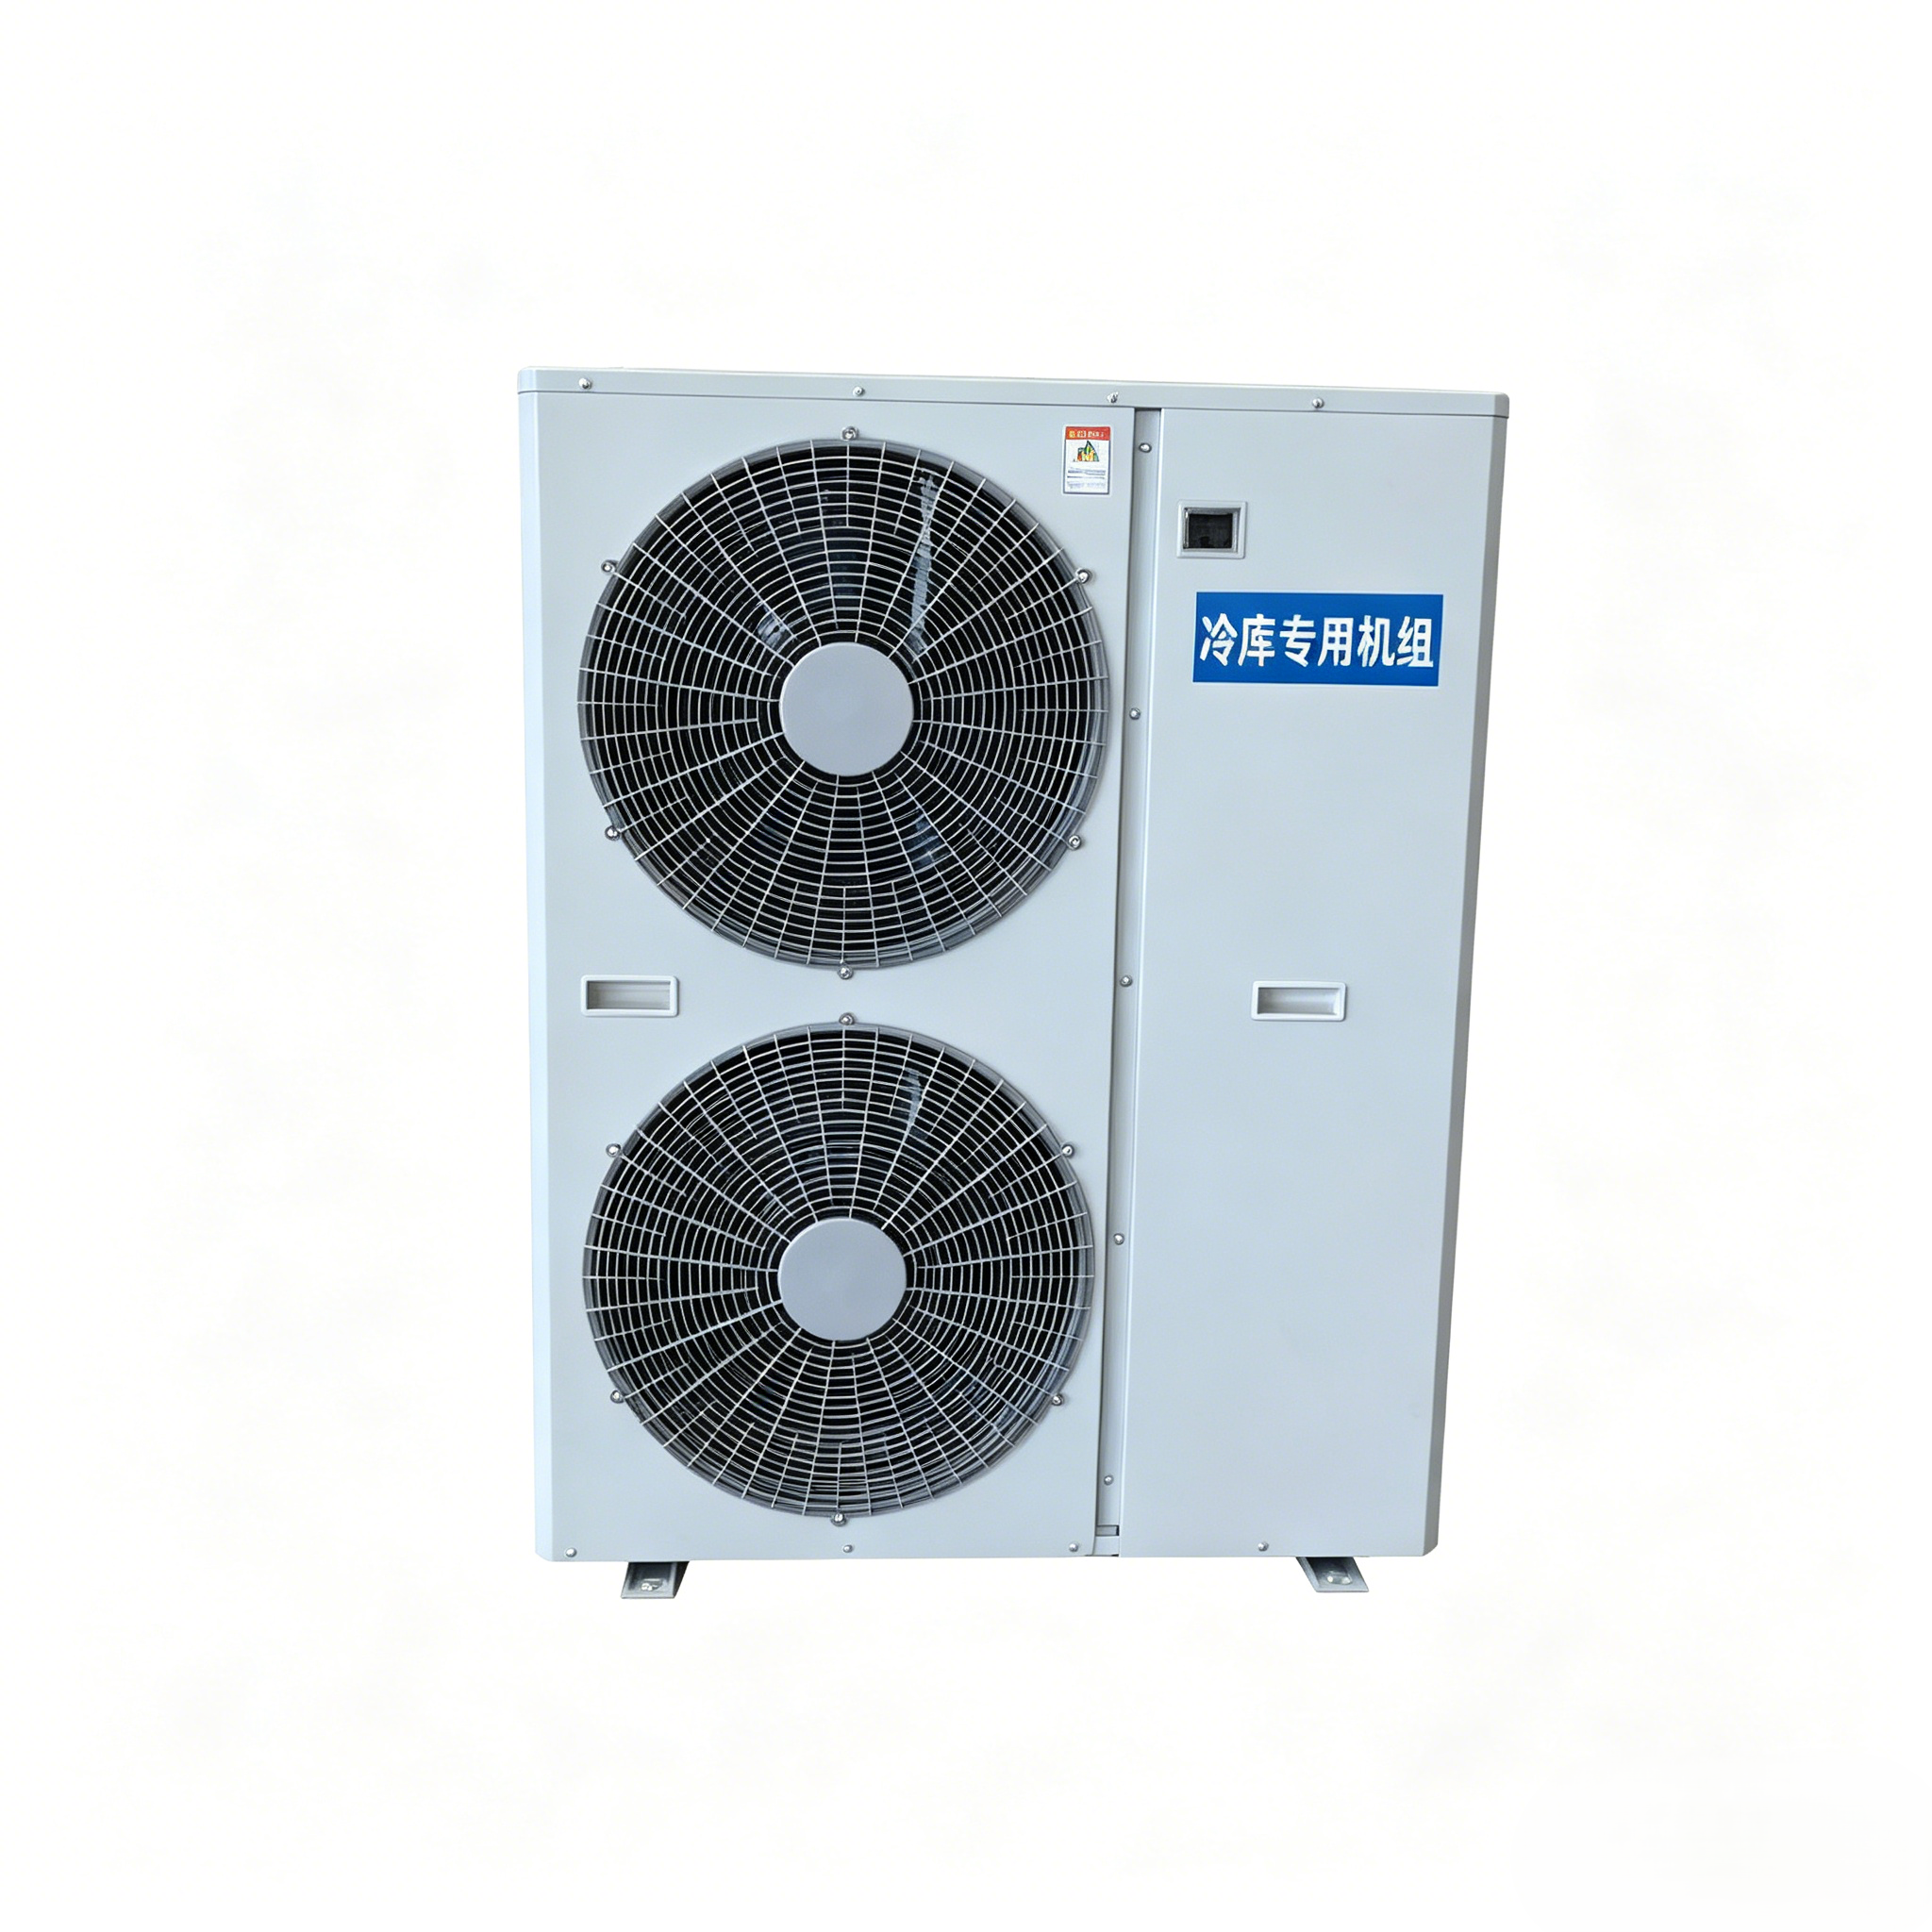
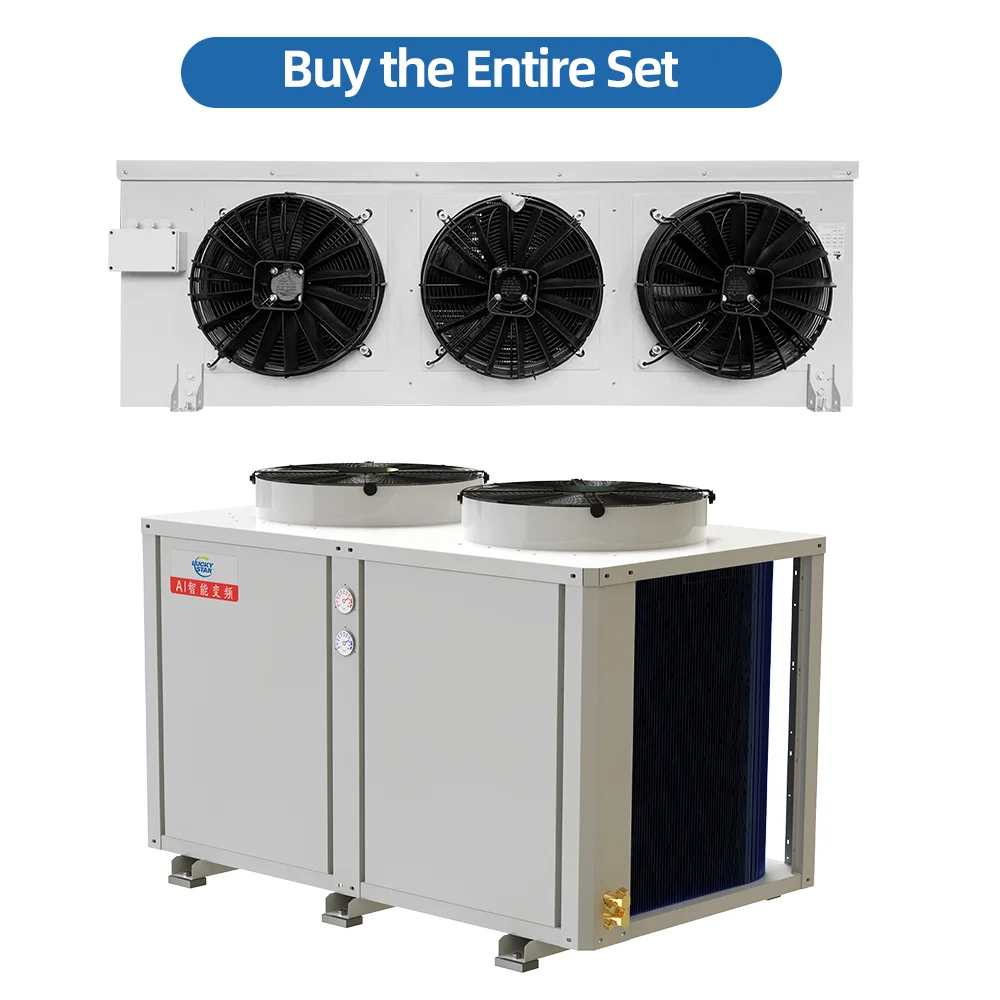
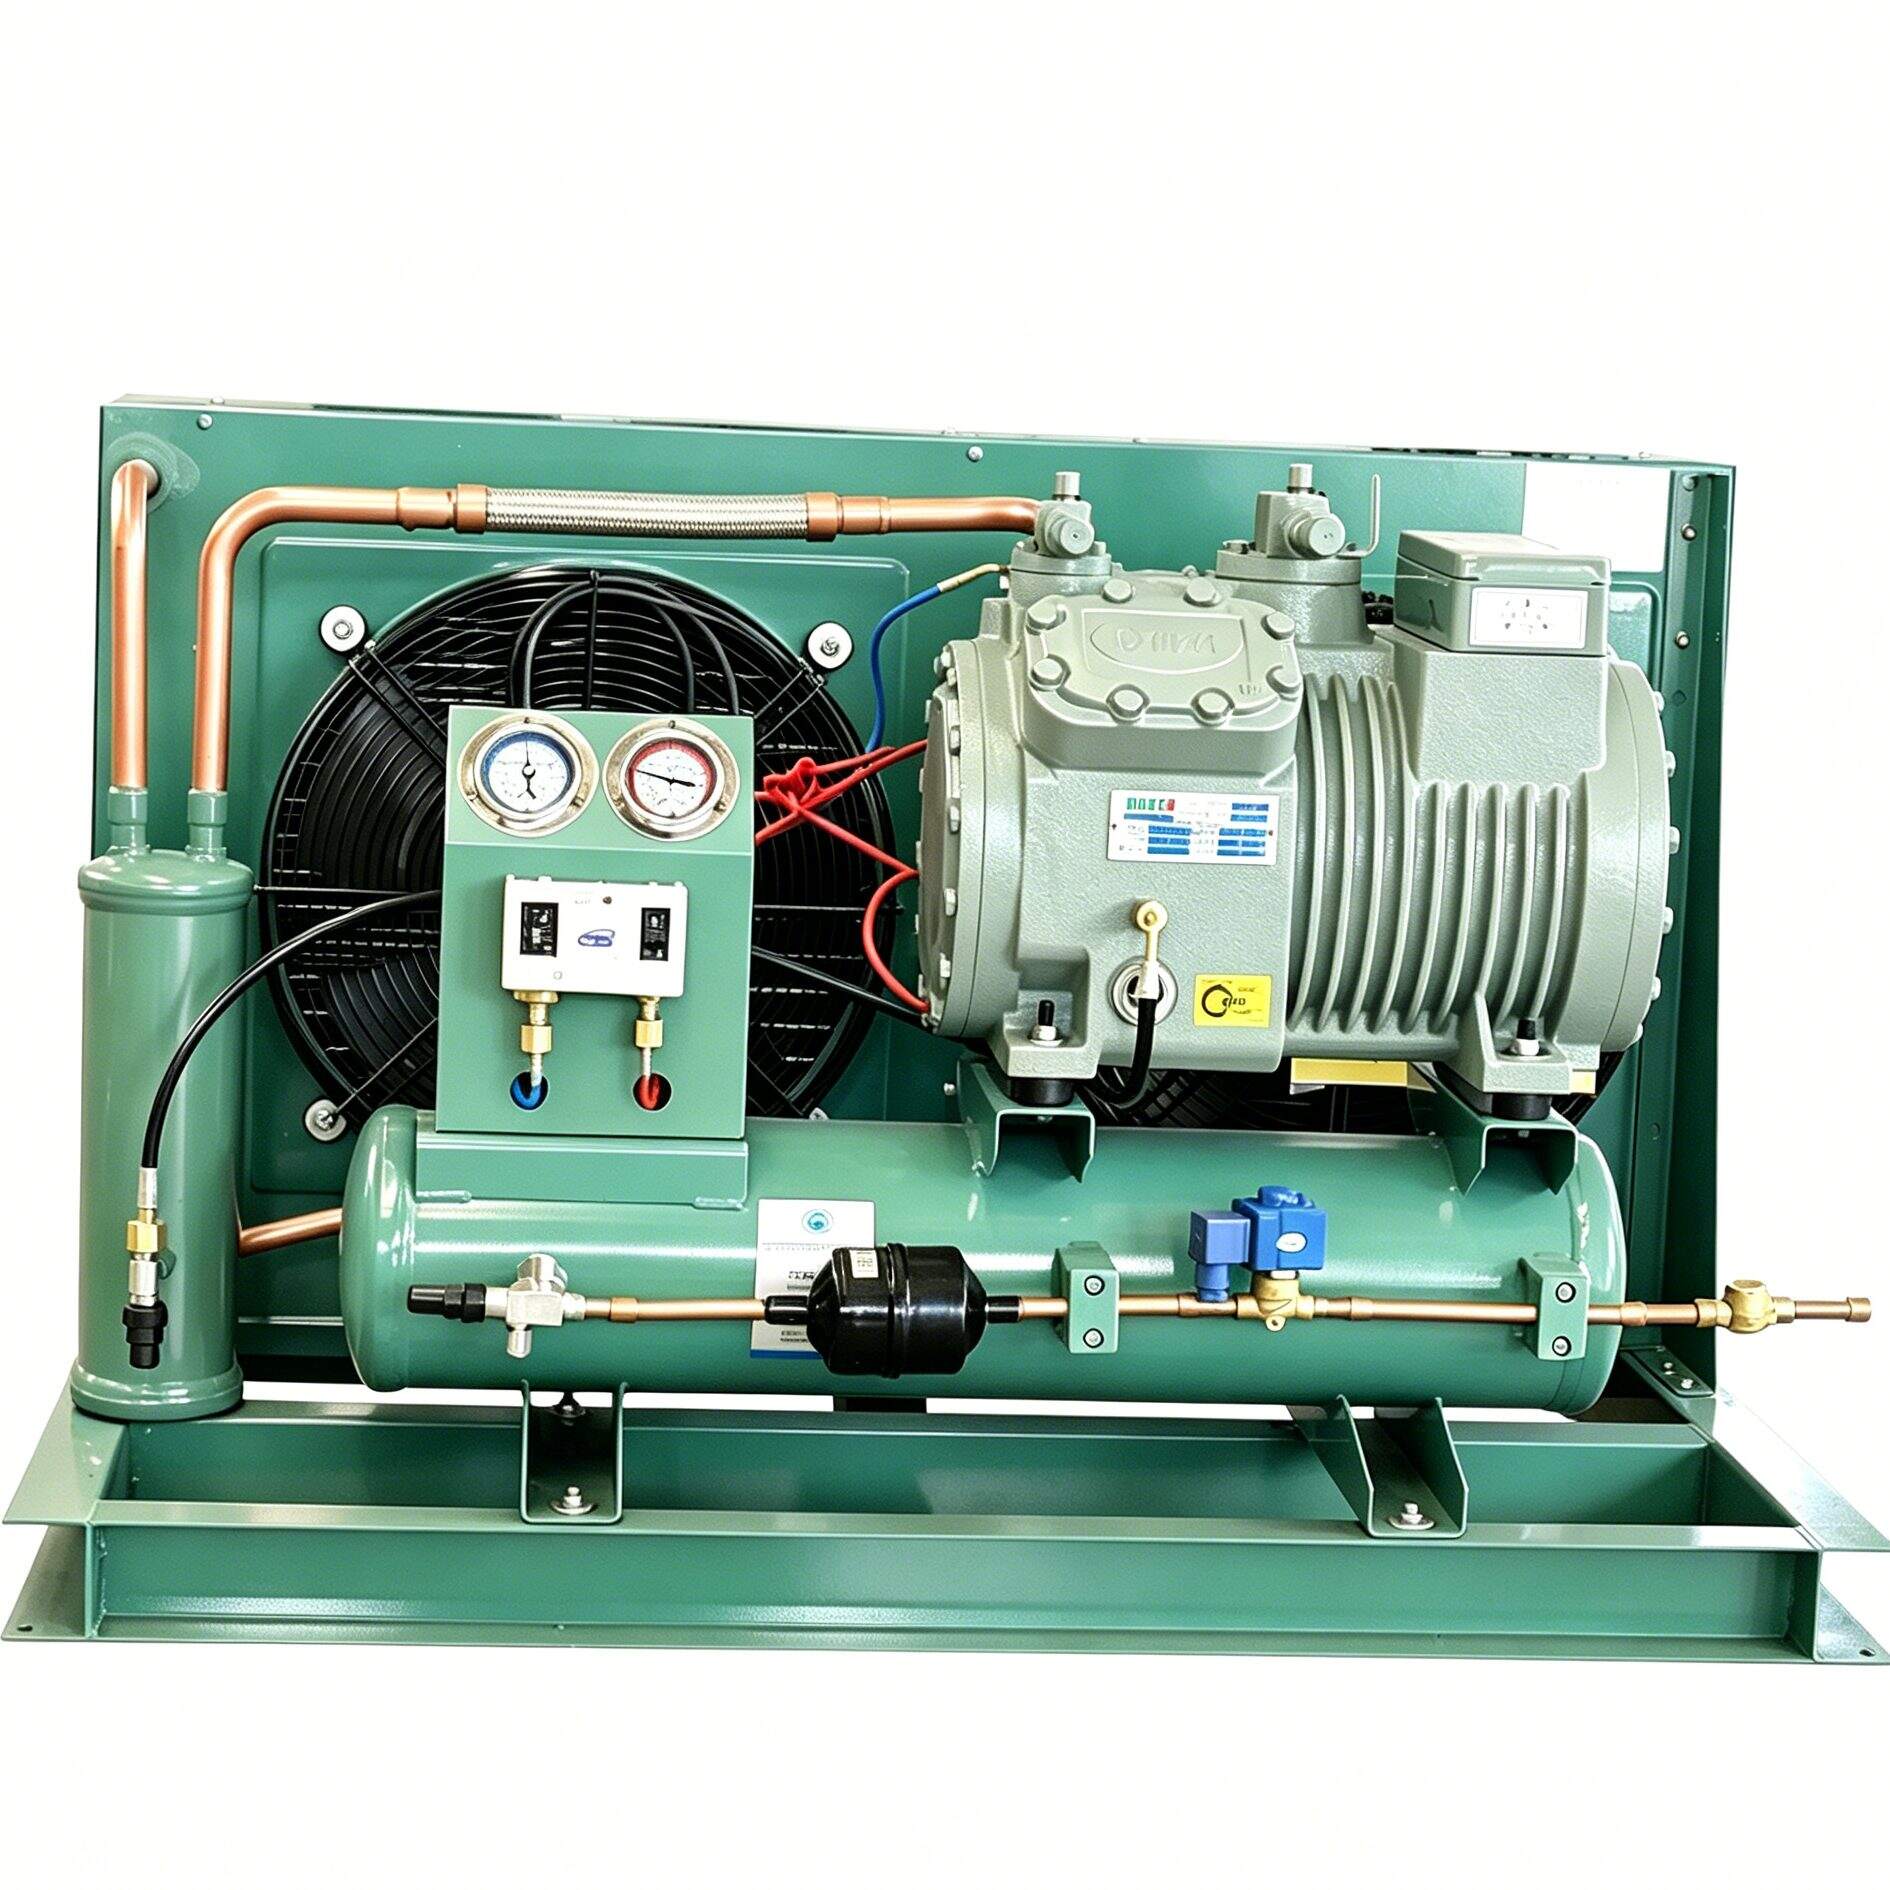
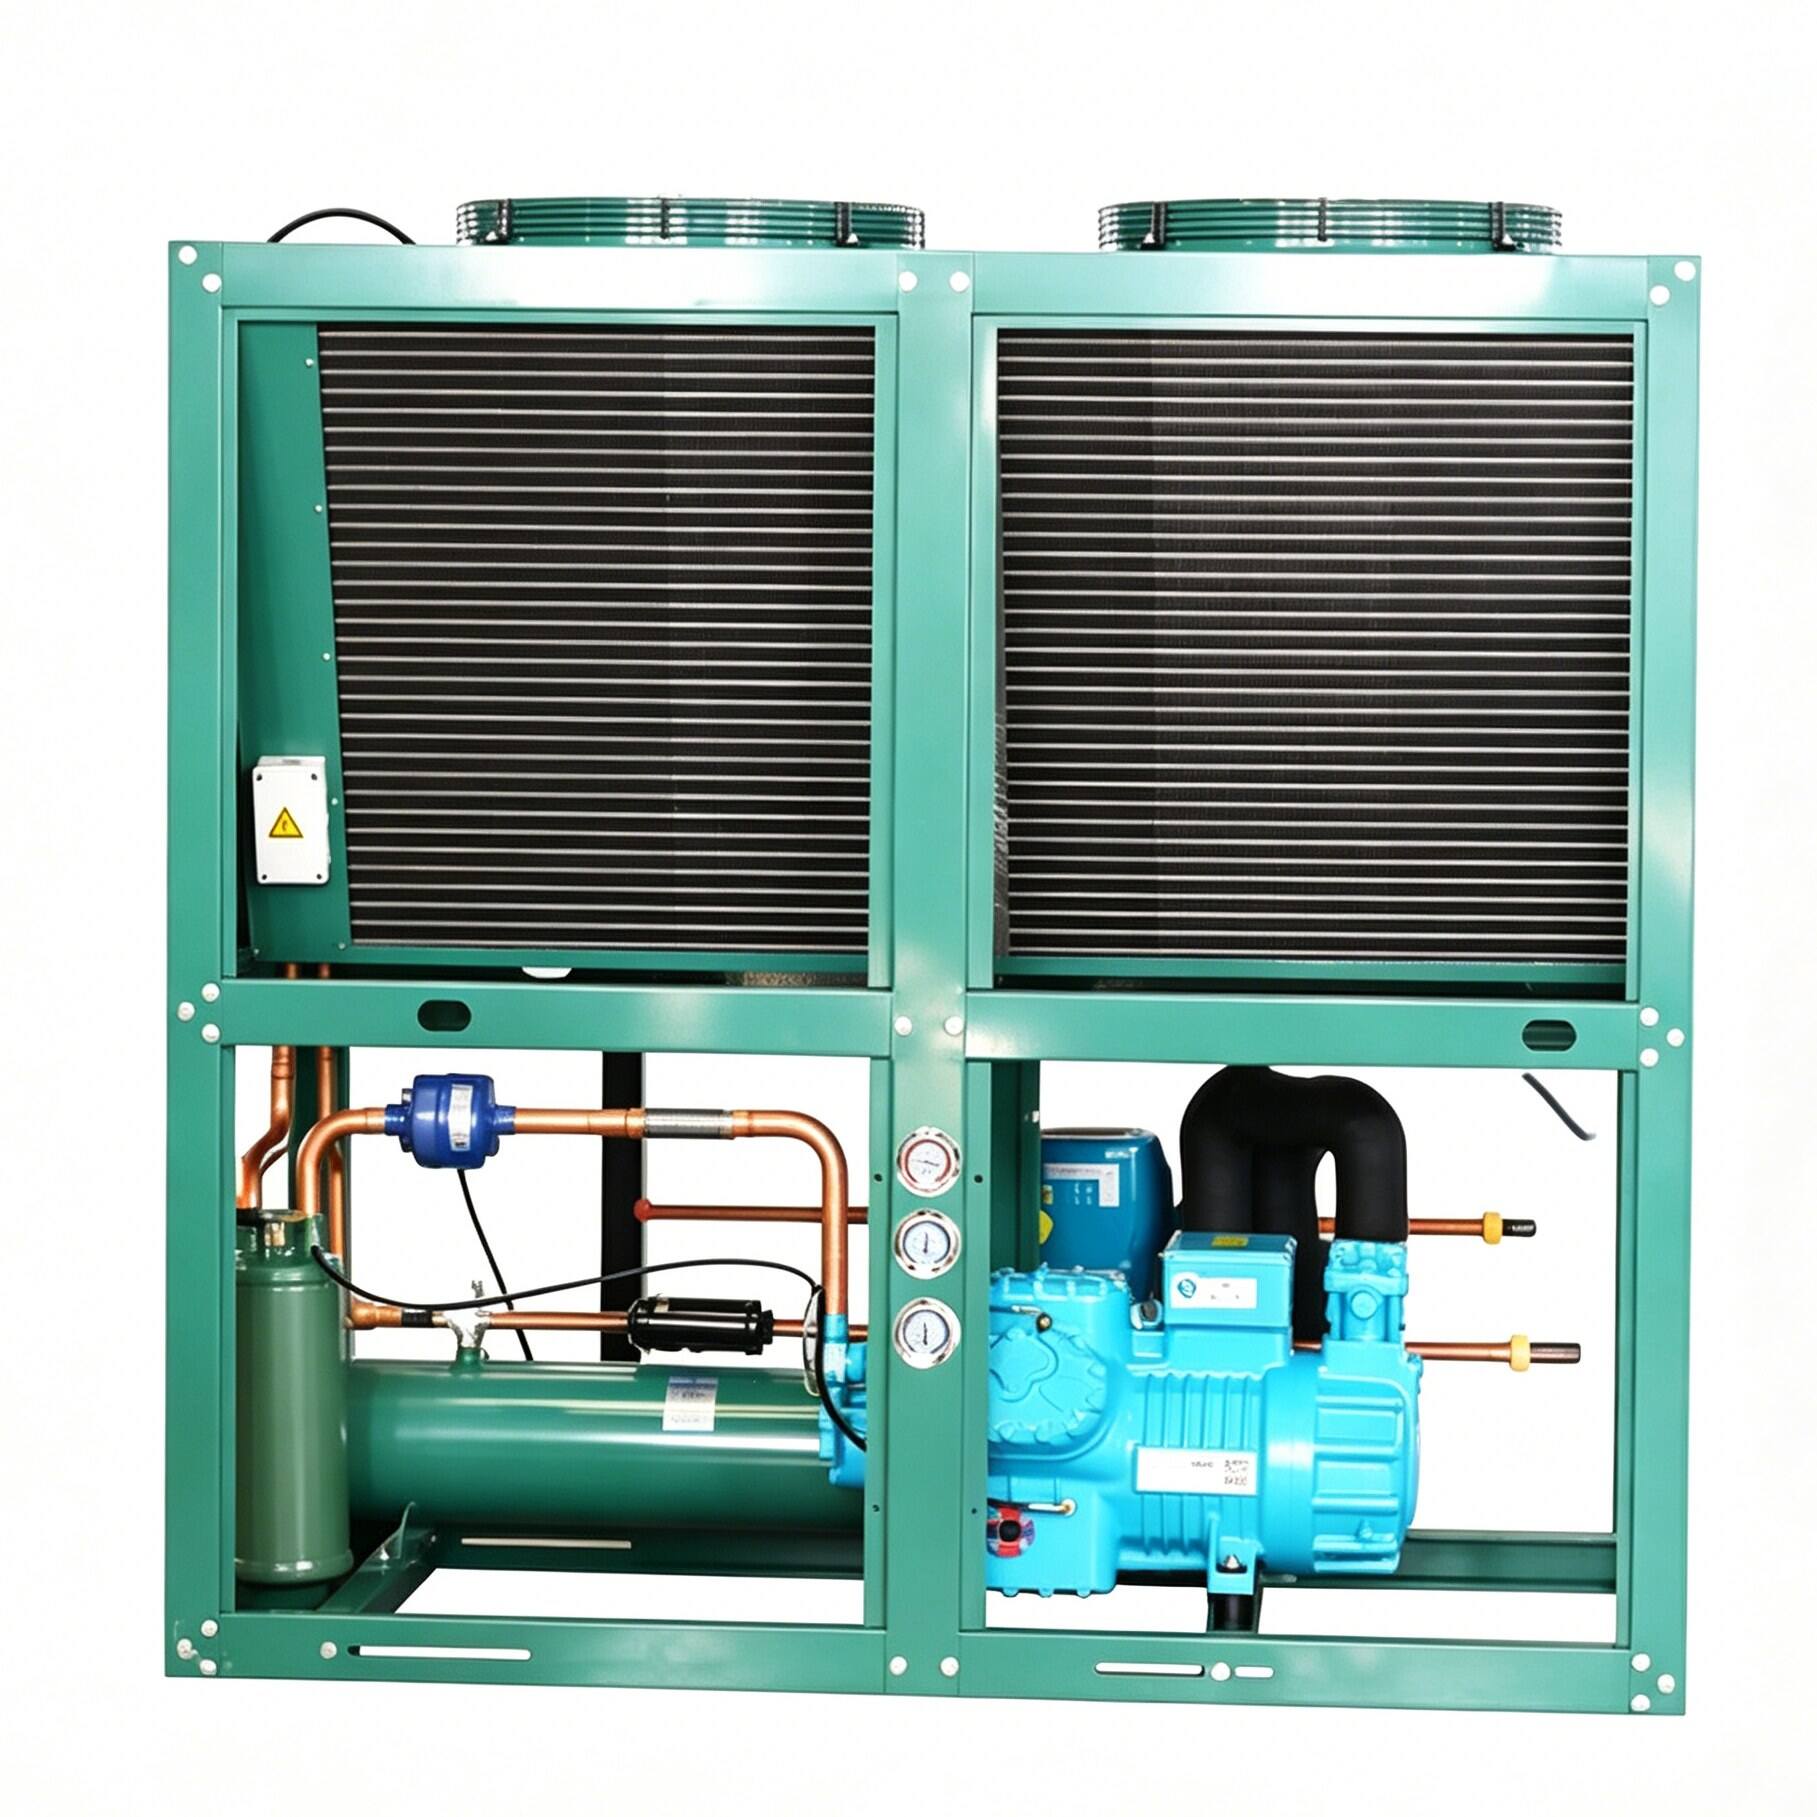
A heavy duty hermetic condensing unit represents a critical component in industrial and commercial refrigeration systems, designed to deliver reliable cooling performance under demanding operational conditions. This self-contained system integrates a hermetically sealed compressor, condenser coil, and necessary controls into a single compact assembly. The hermetic design ensures that the refrigerant and lubricating oil remain sealed within the system, preventing leaks and contamination while maintaining consistent performance. These units are engineered specifically for applications requiring continuous operation and high cooling capacities. The heavy duty hermetic condensing unit functions by compressing refrigerant gas to high pressure and temperature, then condensing it back to liquid form through the condenser coil. Advanced technological features include robust compressor construction, efficient heat exchange surfaces, precision control systems, and protective devices that monitor temperature, pressure, and electrical parameters. Modern heavy duty hermetic condensing units incorporate variable speed technology, enhanced coil designs, and intelligent defrost systems to optimize energy consumption. These units find extensive applications across cold storage facilities, food processing plants, pharmaceutical manufacturing, supermarket refrigeration, industrial cooling processes, and large-scale air conditioning installations. The robust construction and sealed design make the heavy duty hermetic condensing unit particularly suitable for environments where reliability, longevity, and minimal maintenance are paramount considerations for facility managers and refrigeration professionals.
New Products

Investing in a heavy duty hermetic condensing unit provides significant operational and financial benefits that directly impact your bottom line. The sealed compressor design eliminates refrigerant leakage concerns, reducing maintenance costs and environmental compliance issues while ensuring consistent cooling performance throughout the system's lifespan. You benefit from lower operating expenses because these units operate more efficiently than open-type systems, consuming less electricity while delivering the same cooling capacity. The integrated design simplifies installation, requiring less floor space and fewer connection points, which translates to reduced installation time and labor costs. Your facility gains operational reliability through continuous duty ratings that allow 24/7 operation without performance degradation, critical for businesses that cannot afford downtime. The heavy duty hermetic condensing unit features protective mechanisms that automatically respond to adverse conditions, preventing costly equipment damage and extending service life. You experience fewer service calls because the hermetic seal protects internal components from dust, moisture, and contaminants that typically cause premature failure in non-sealed systems. These units adapt to diverse temperature requirements and cooling loads, making them suitable whether you operate a small cold storage room or a large industrial freezer complex. The robust construction withstands harsh environmental conditions including extreme temperatures, humidity, and corrosive atmospheres. Your purchasing decision becomes easier knowing these units comply with international refrigeration standards and environmental regulations. The long-term value proposition includes extended warranty coverage, readily available replacement parts, and compatibility with modern refrigerants, protecting your investment as regulations evolve and ensuring your heavy duty hermetic condensing unit remains serviceable for years to come.

Latest News

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

28

Feb

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

View More
Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

28

Feb

Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

View More
Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

28

Feb

Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

heavy duty hermetic condensing unit

Superior Hermetic Sealing Technology

Superior Hermetic Sealing Technology

The heavy duty hermetic condensing unit employs advanced sealing technology that completely encloses the compressor motor and mechanical components within a welded steel shell. This hermetic construction provides exceptional protection against external contaminants, moisture infiltration, and refrigerant loss that plague open compressor systems. The sealed environment maintains optimal lubrication conditions, preventing oil degradation and extending component life significantly beyond conventional designs. You gain peace of mind knowing that refrigerant containment meets stringent environmental standards while eliminating the need for shaft seals that require periodic replacement. The hermetic design reduces noise transmission, creating a quieter working environment in your facility. This sealing approach also minimizes the risk of compressor contamination from airborne particles, chemical vapors, or humid conditions that would otherwise compromise performance. The welded construction withstands high internal pressures and thermal cycling without developing leaks, ensuring long-term reliability. For facility managers, this translates to predictable maintenance schedules, reduced emergency service calls, and lower total cost of ownership throughout the equipment's operational life.
Heavy Duty Construction for Demanding Applications

Heavy Duty Construction for Demanding Applications

Engineered specifically for rigorous industrial environments, the heavy duty hermetic condensing unit features reinforced components that deliver exceptional durability under continuous operation. The compressor utilizes hardened internal parts, precision-balanced rotating assemblies, and enhanced bearing systems designed to withstand millions of operating cycles without failure. Heavy gauge steel cabinets protect internal components from physical damage while providing excellent corrosion resistance in challenging environments. The condenser coils employ thicker tube walls and reinforced fin configurations that resist damage from debris, cleaning procedures, and environmental exposure. Electrical components meet industrial ratings for voltage fluctuations, temperature extremes, and moisture resistance. This robust construction proves essential in applications such as food processing facilities, chemical plants, and outdoor installations where equipment faces demanding conditions daily. You benefit from extended service intervals because wear-resistant materials and oversized components operate well below their stress limits. The heavy duty hermetic condensing unit maintains consistent performance even when ambient temperatures fluctuate significantly, ensuring your refrigeration needs are met regardless of seasonal variations or facility conditions that would compromise lesser equipment.
Optimized Energy Efficiency and Control

Optimized Energy Efficiency and Control

Modern heavy duty hermetic condensing units incorporate intelligent control systems and efficient designs that substantially reduce energy consumption compared to older refrigeration equipment. Variable speed compressor technology automatically adjusts cooling output to match actual load requirements, eliminating the energy waste associated with constant-speed operation and frequent on-off cycling. High-efficiency condenser coils maximize heat transfer while minimizing fan power requirements, reducing electrical demand during peak cooling periods. Advanced refrigerant circuitry ensures optimal superheat and subcooling conditions that improve coefficient of performance across the entire operating range. Digital controls monitor system parameters continuously, making real-time adjustments that maintain setpoint temperatures precisely while minimizing energy use. You benefit from lower utility bills month after month, with energy savings often recovering the initial equipment investment within several years. The heavy duty hermetic condensing unit supports integration with building management systems, enabling remote monitoring, automated scheduling, and performance analytics that identify optimization opportunities. Efficient operation also reduces heat rejection into your facility, potentially lowering air conditioning costs in climate-controlled spaces. Environmental benefits include reduced carbon footprint and compliance with energy efficiency regulations that increasingly affect commercial and industrial operations.
Heavy Duty Hermetic Condensing Unit Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
Heavy Duty Hermetic Condensing Unit Solutions

Copyright © 2026 Ningbo Lucky Star Import & Export Co., Ltd. All rights reserved.  -  Privacy policy