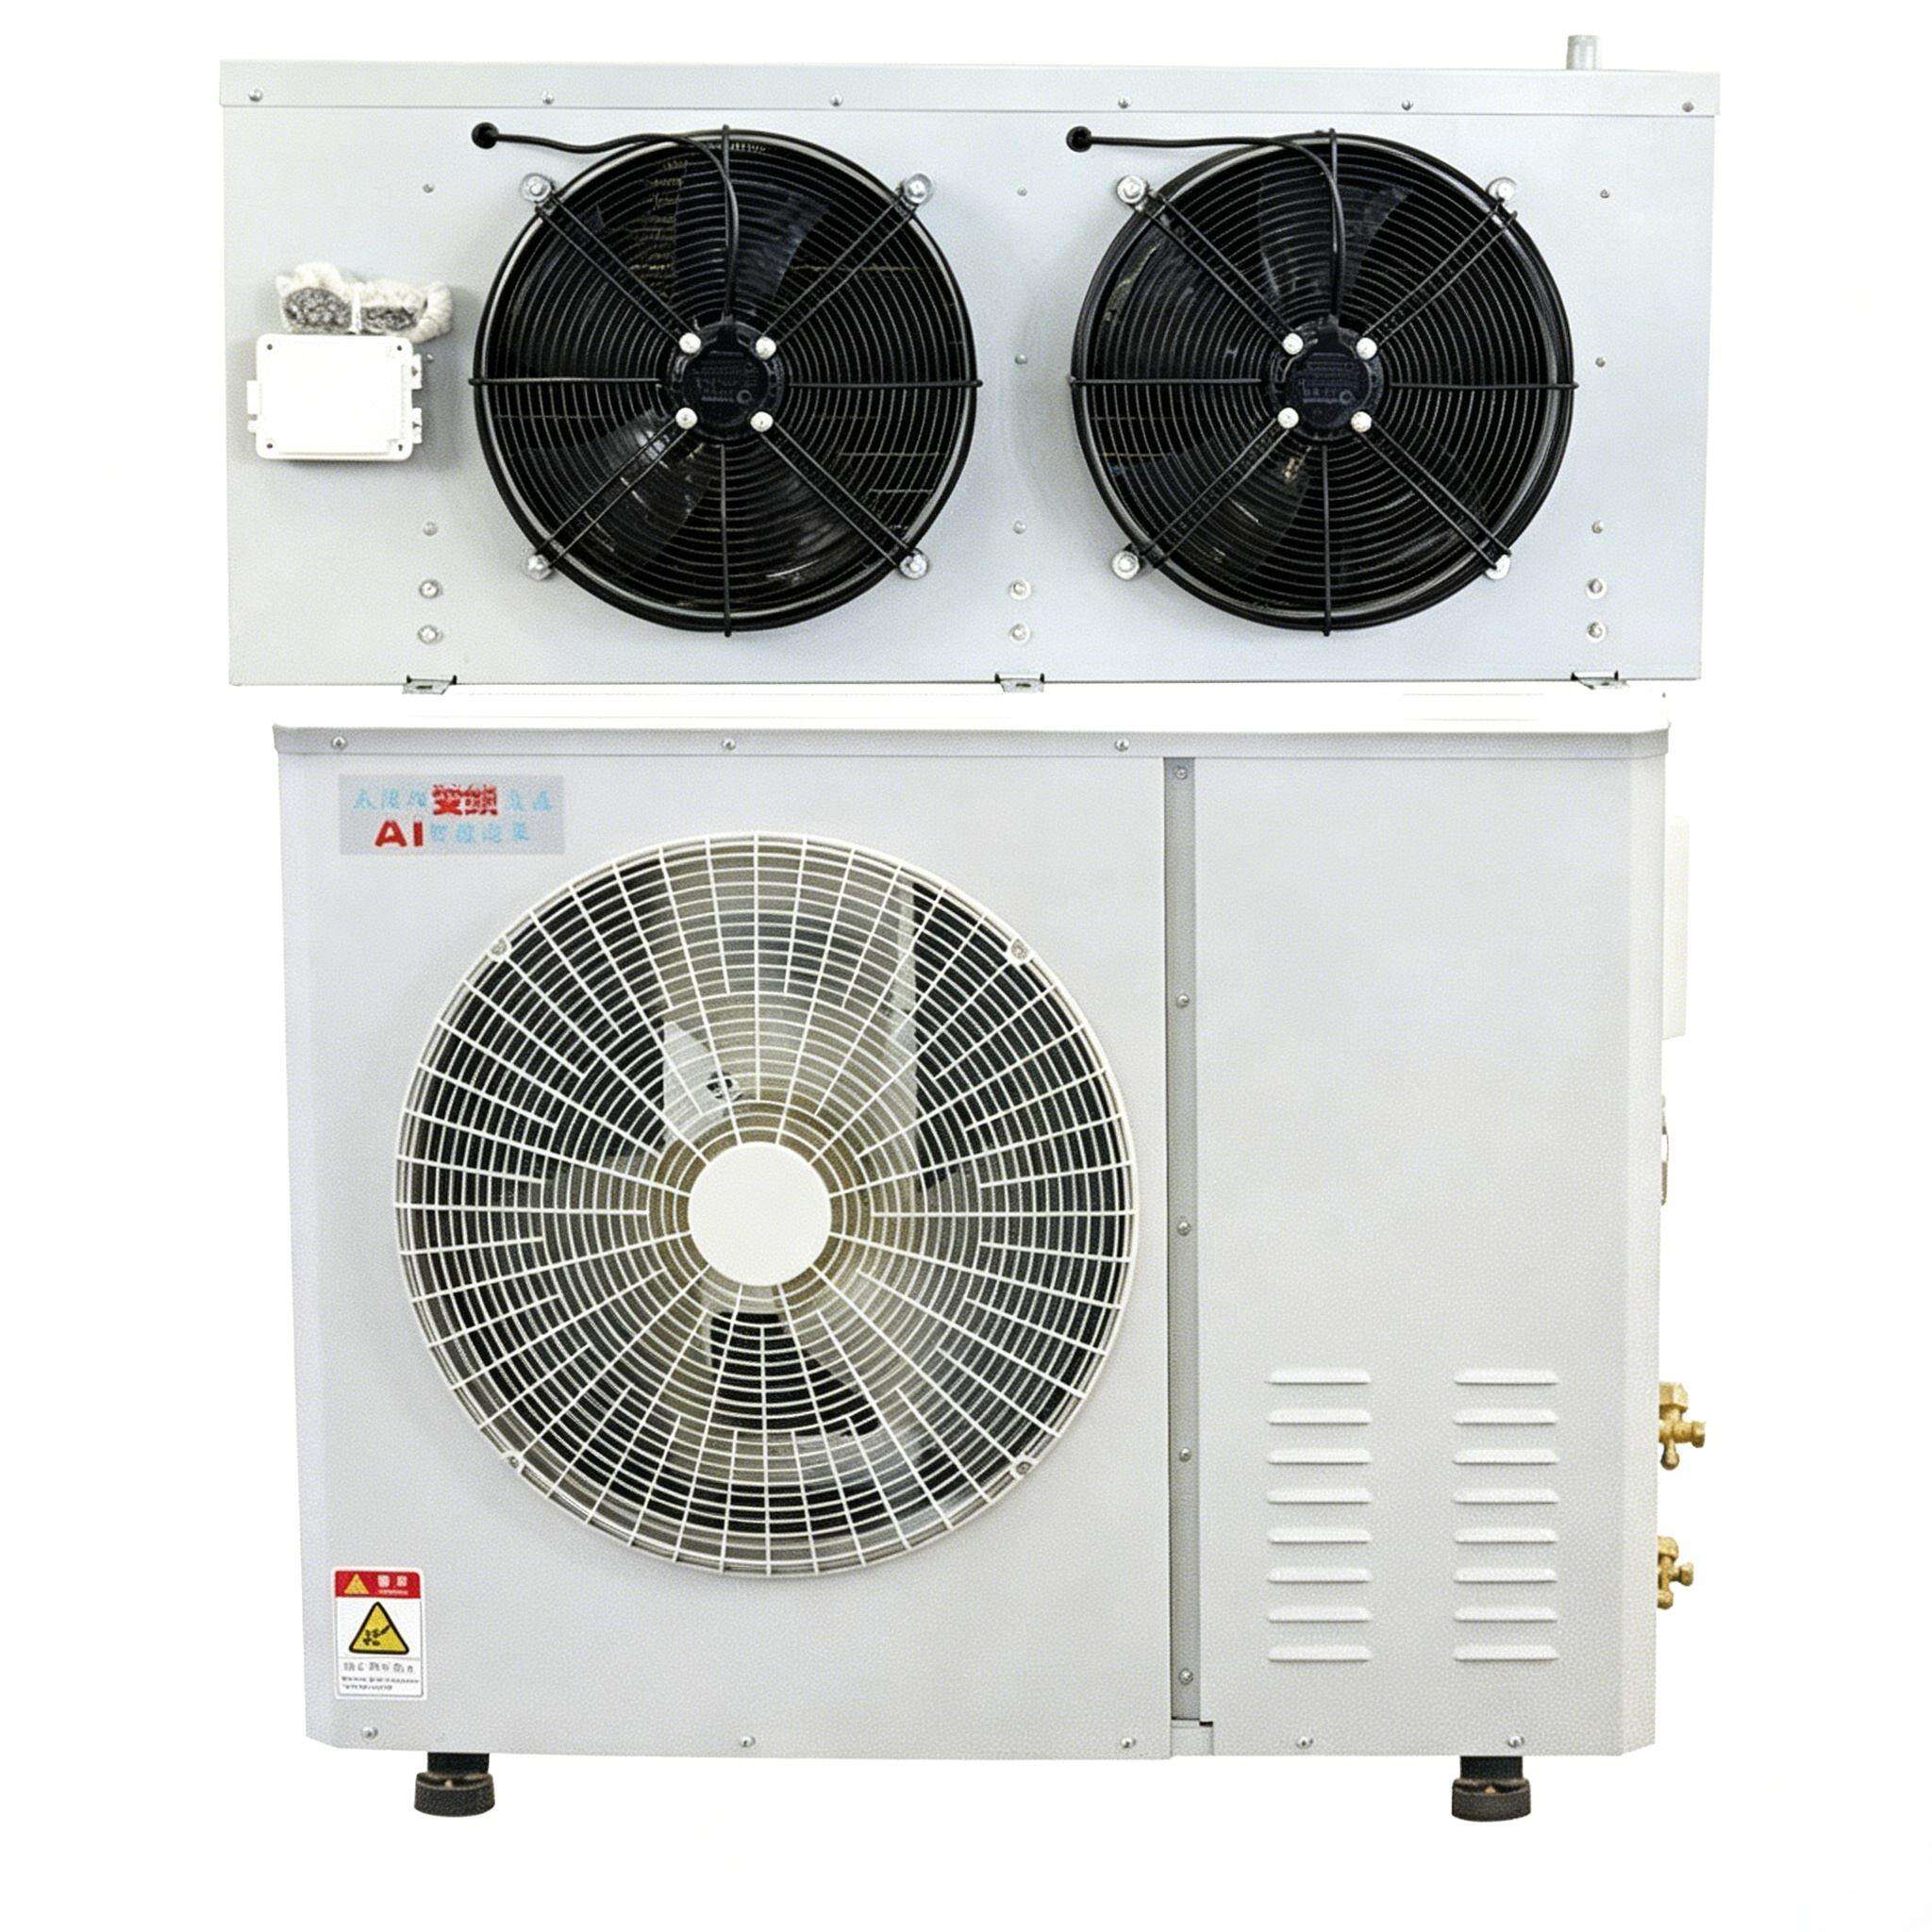
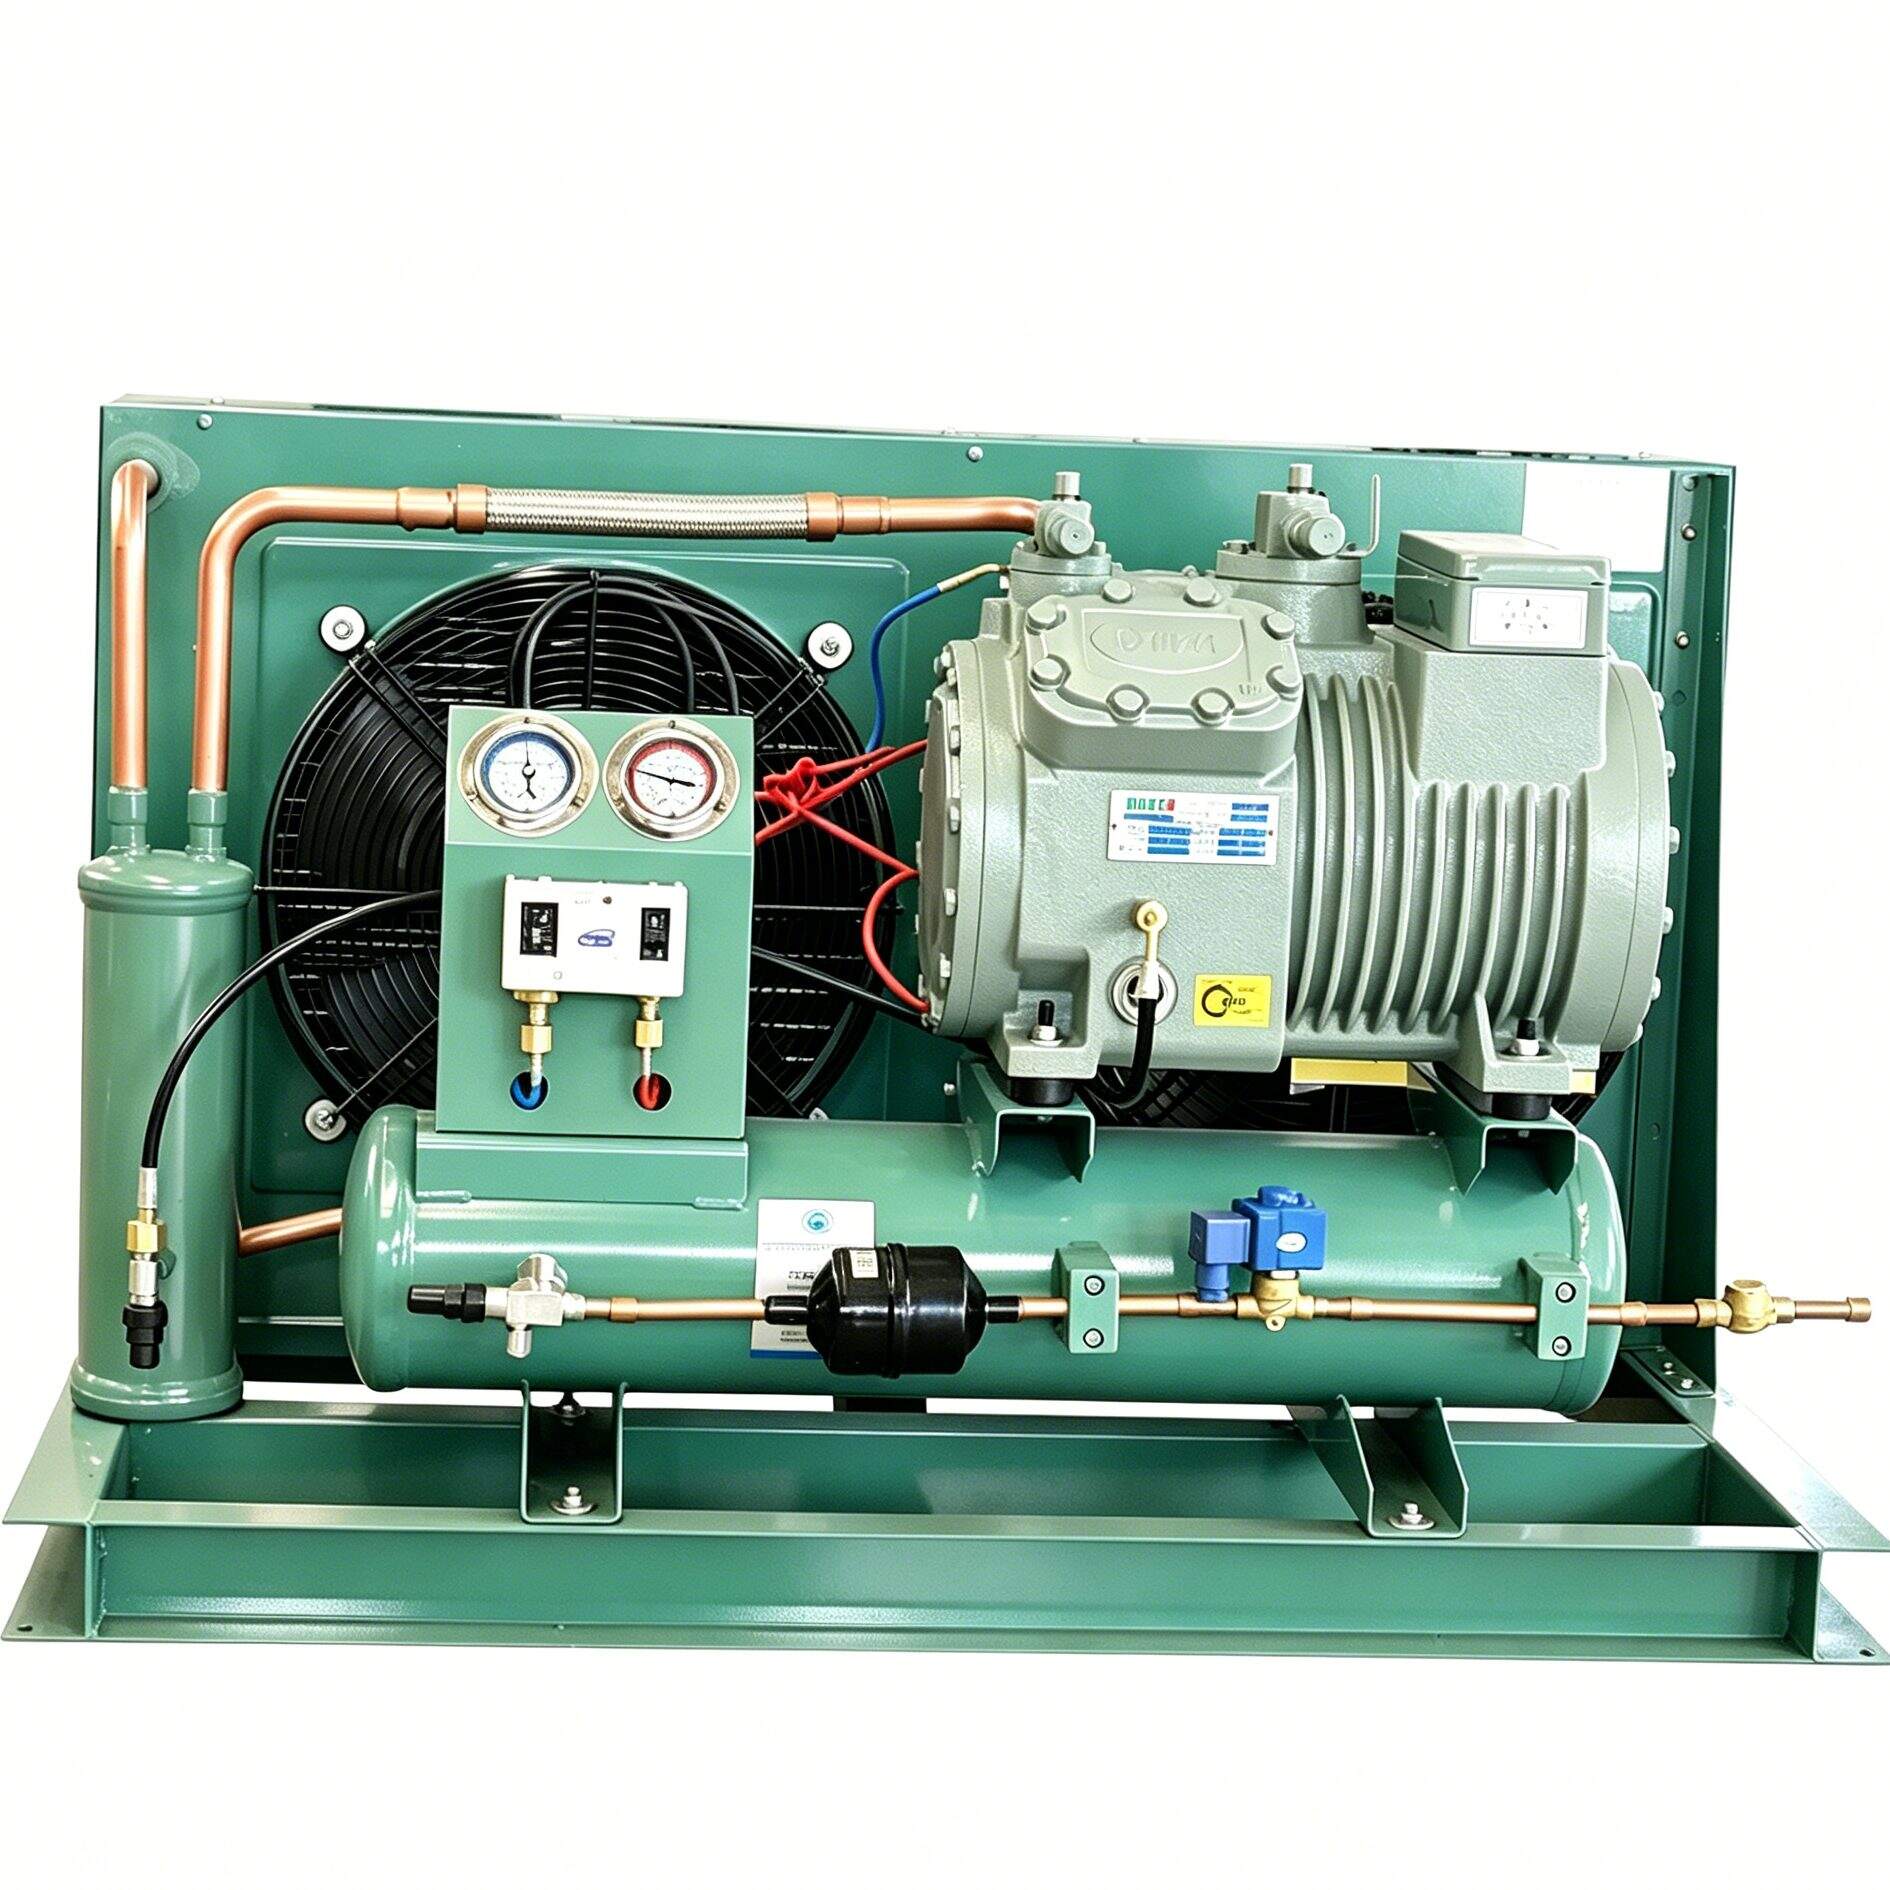
quality h type condensing unit
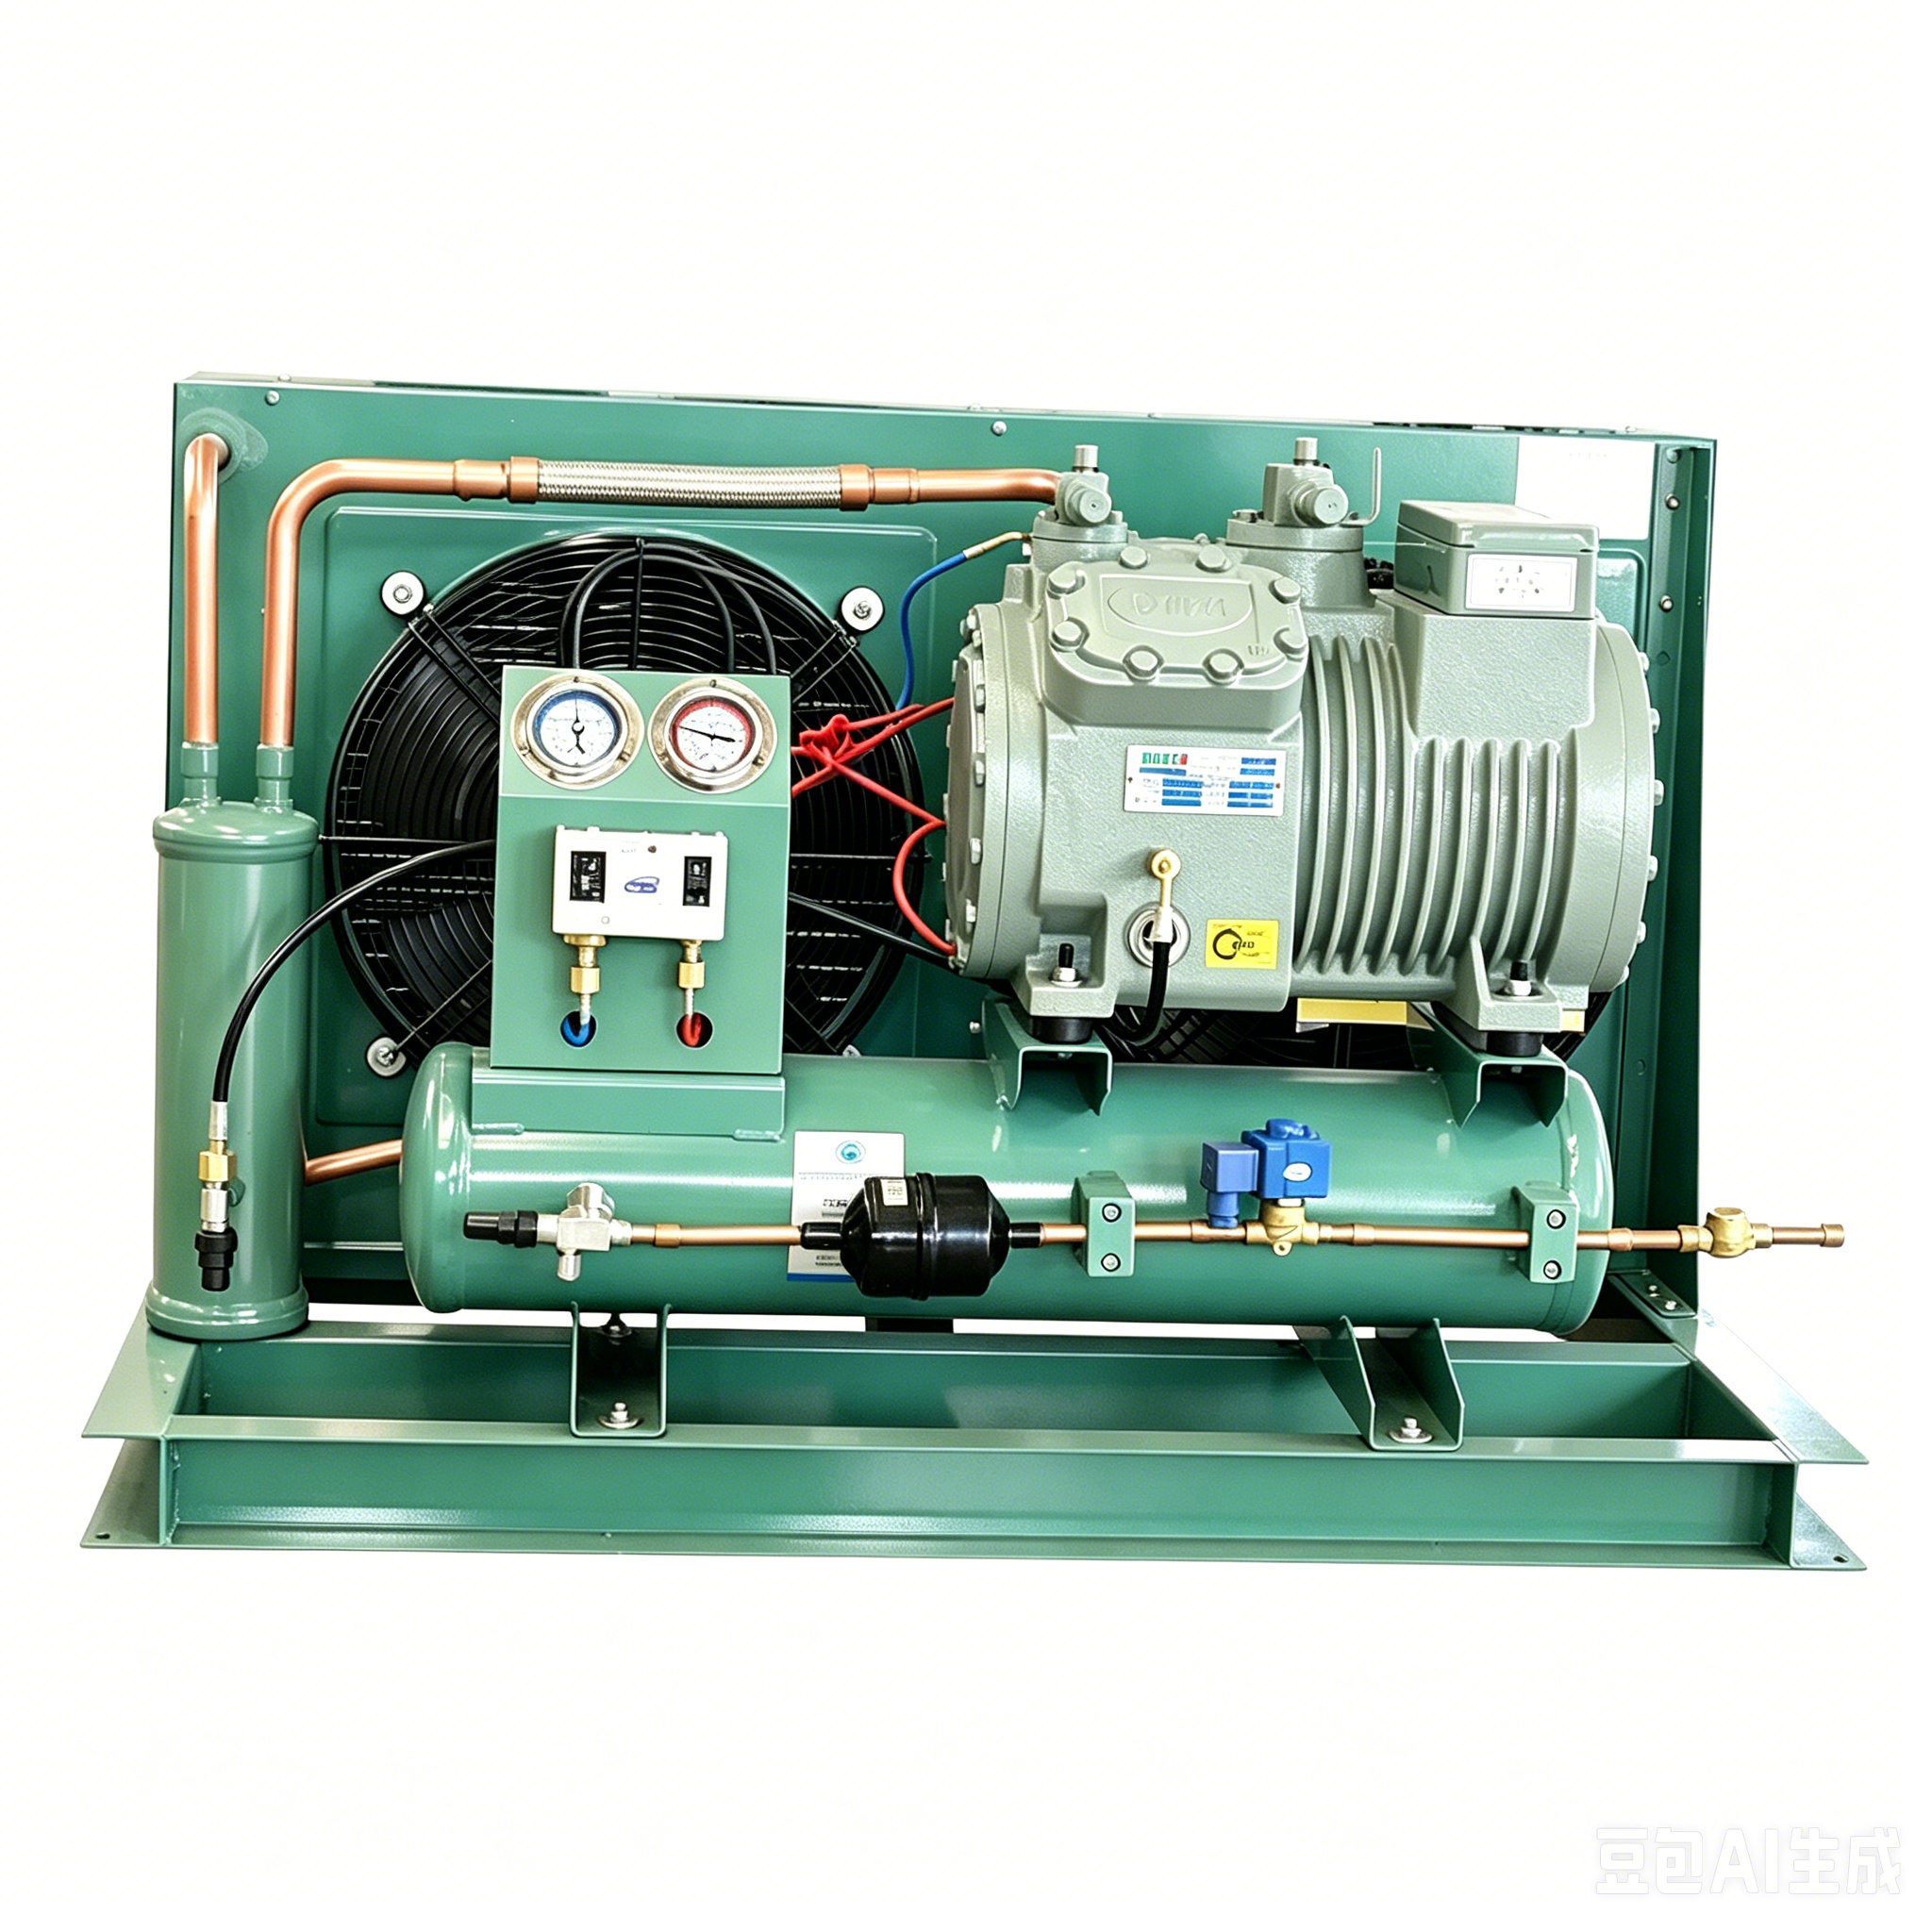
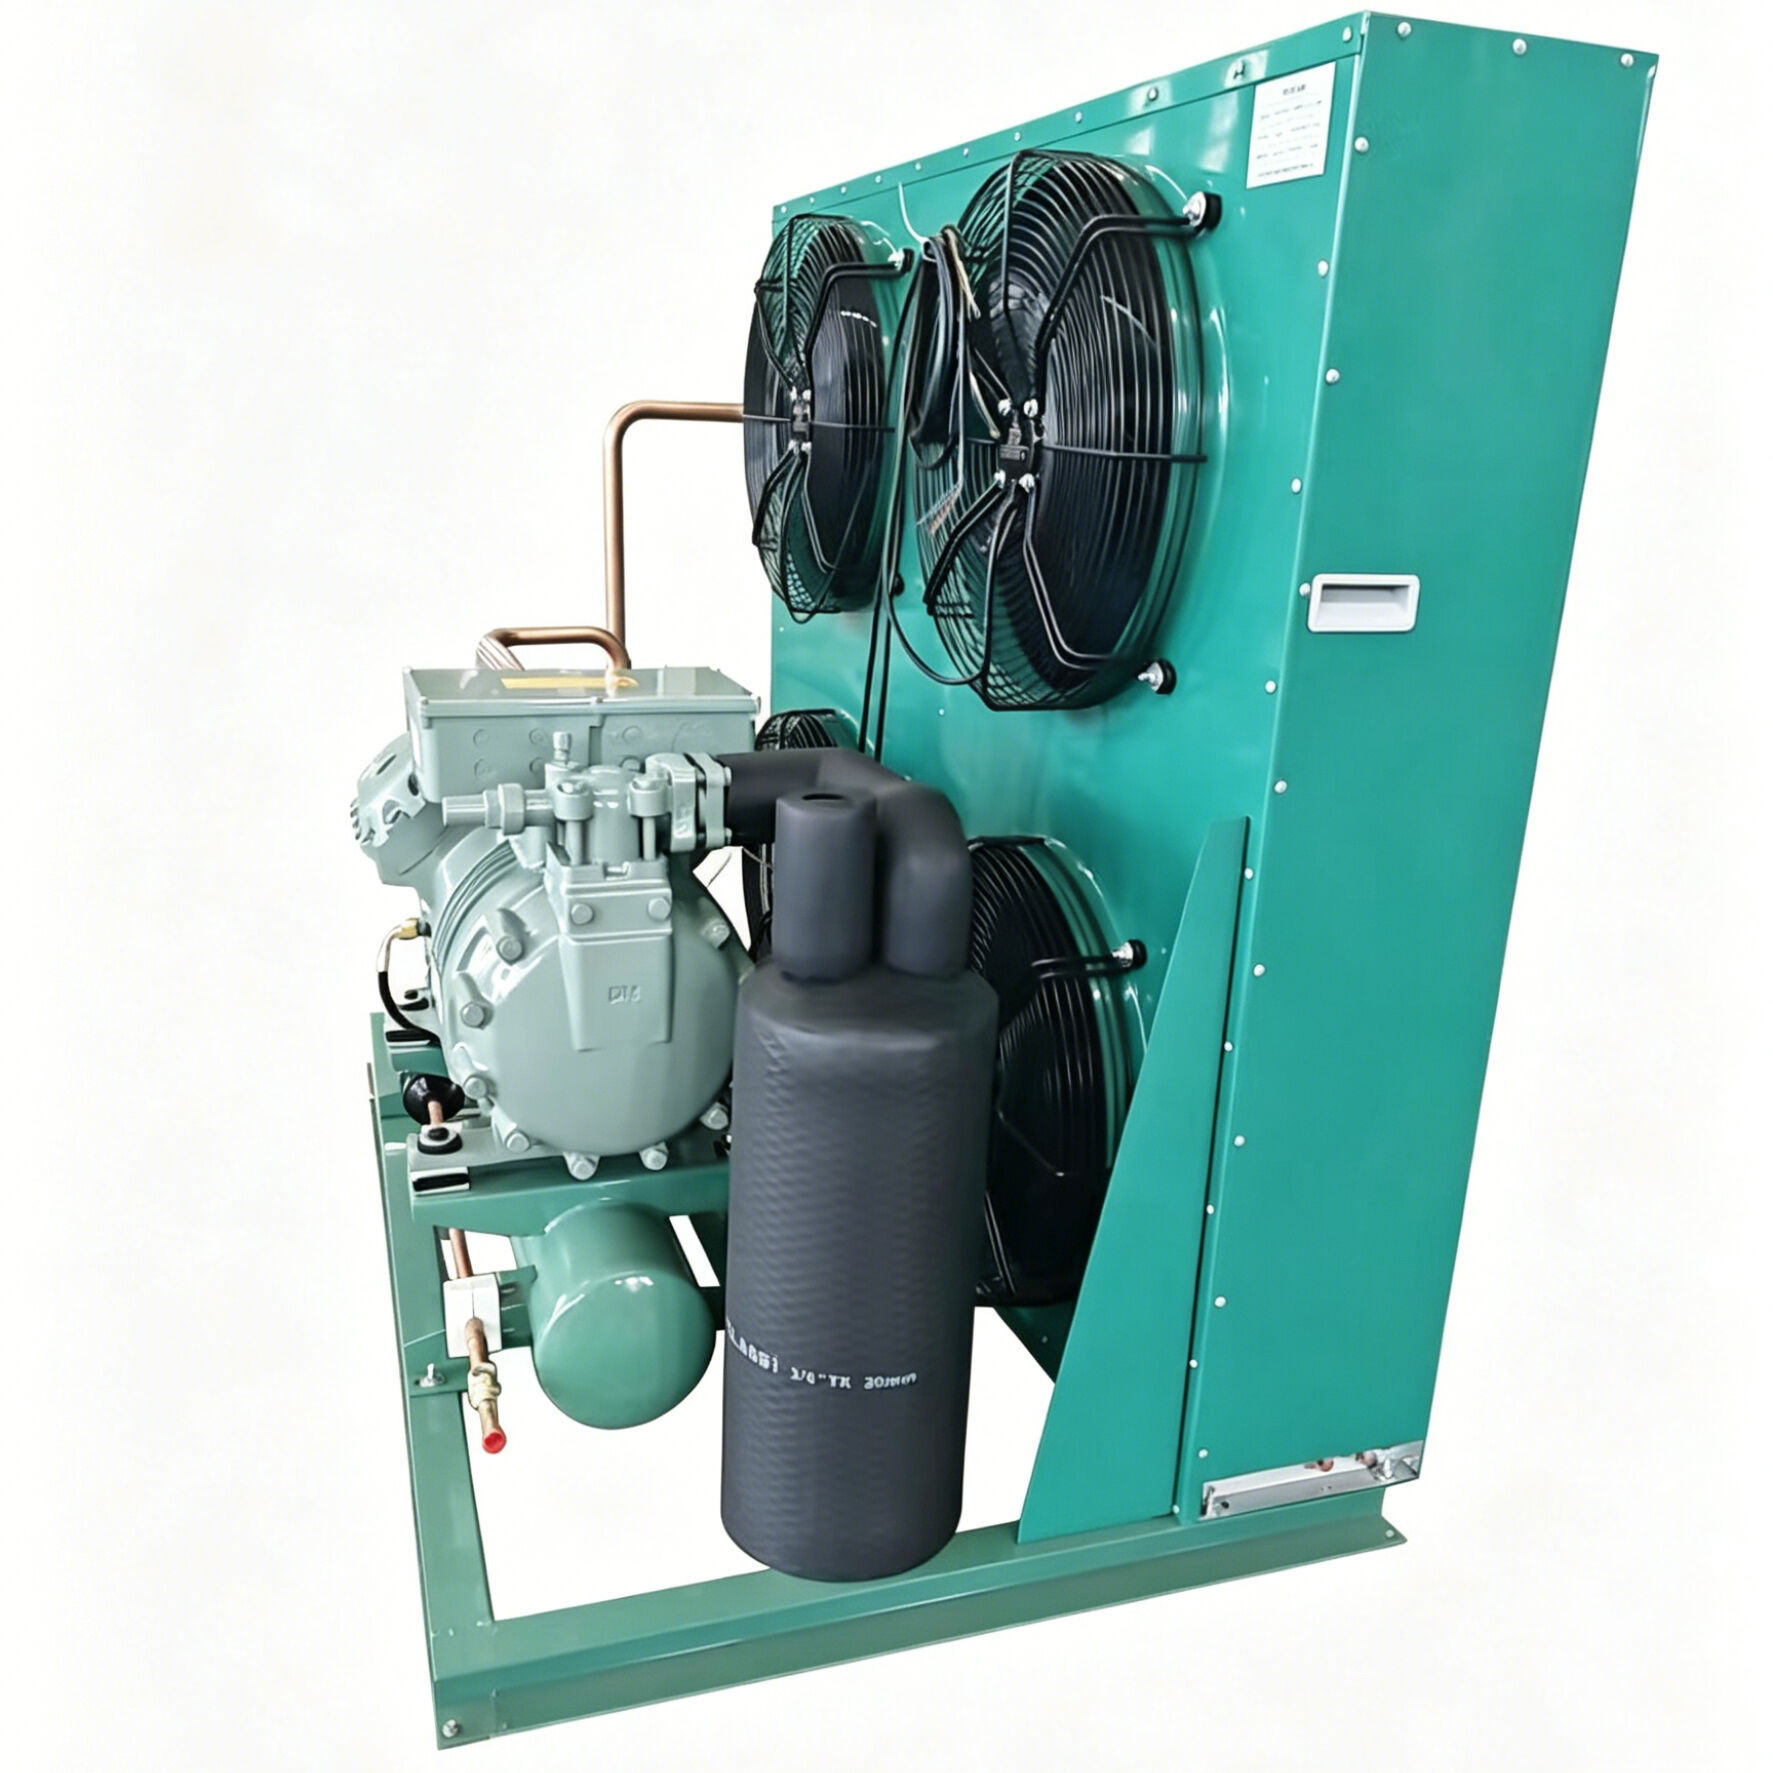
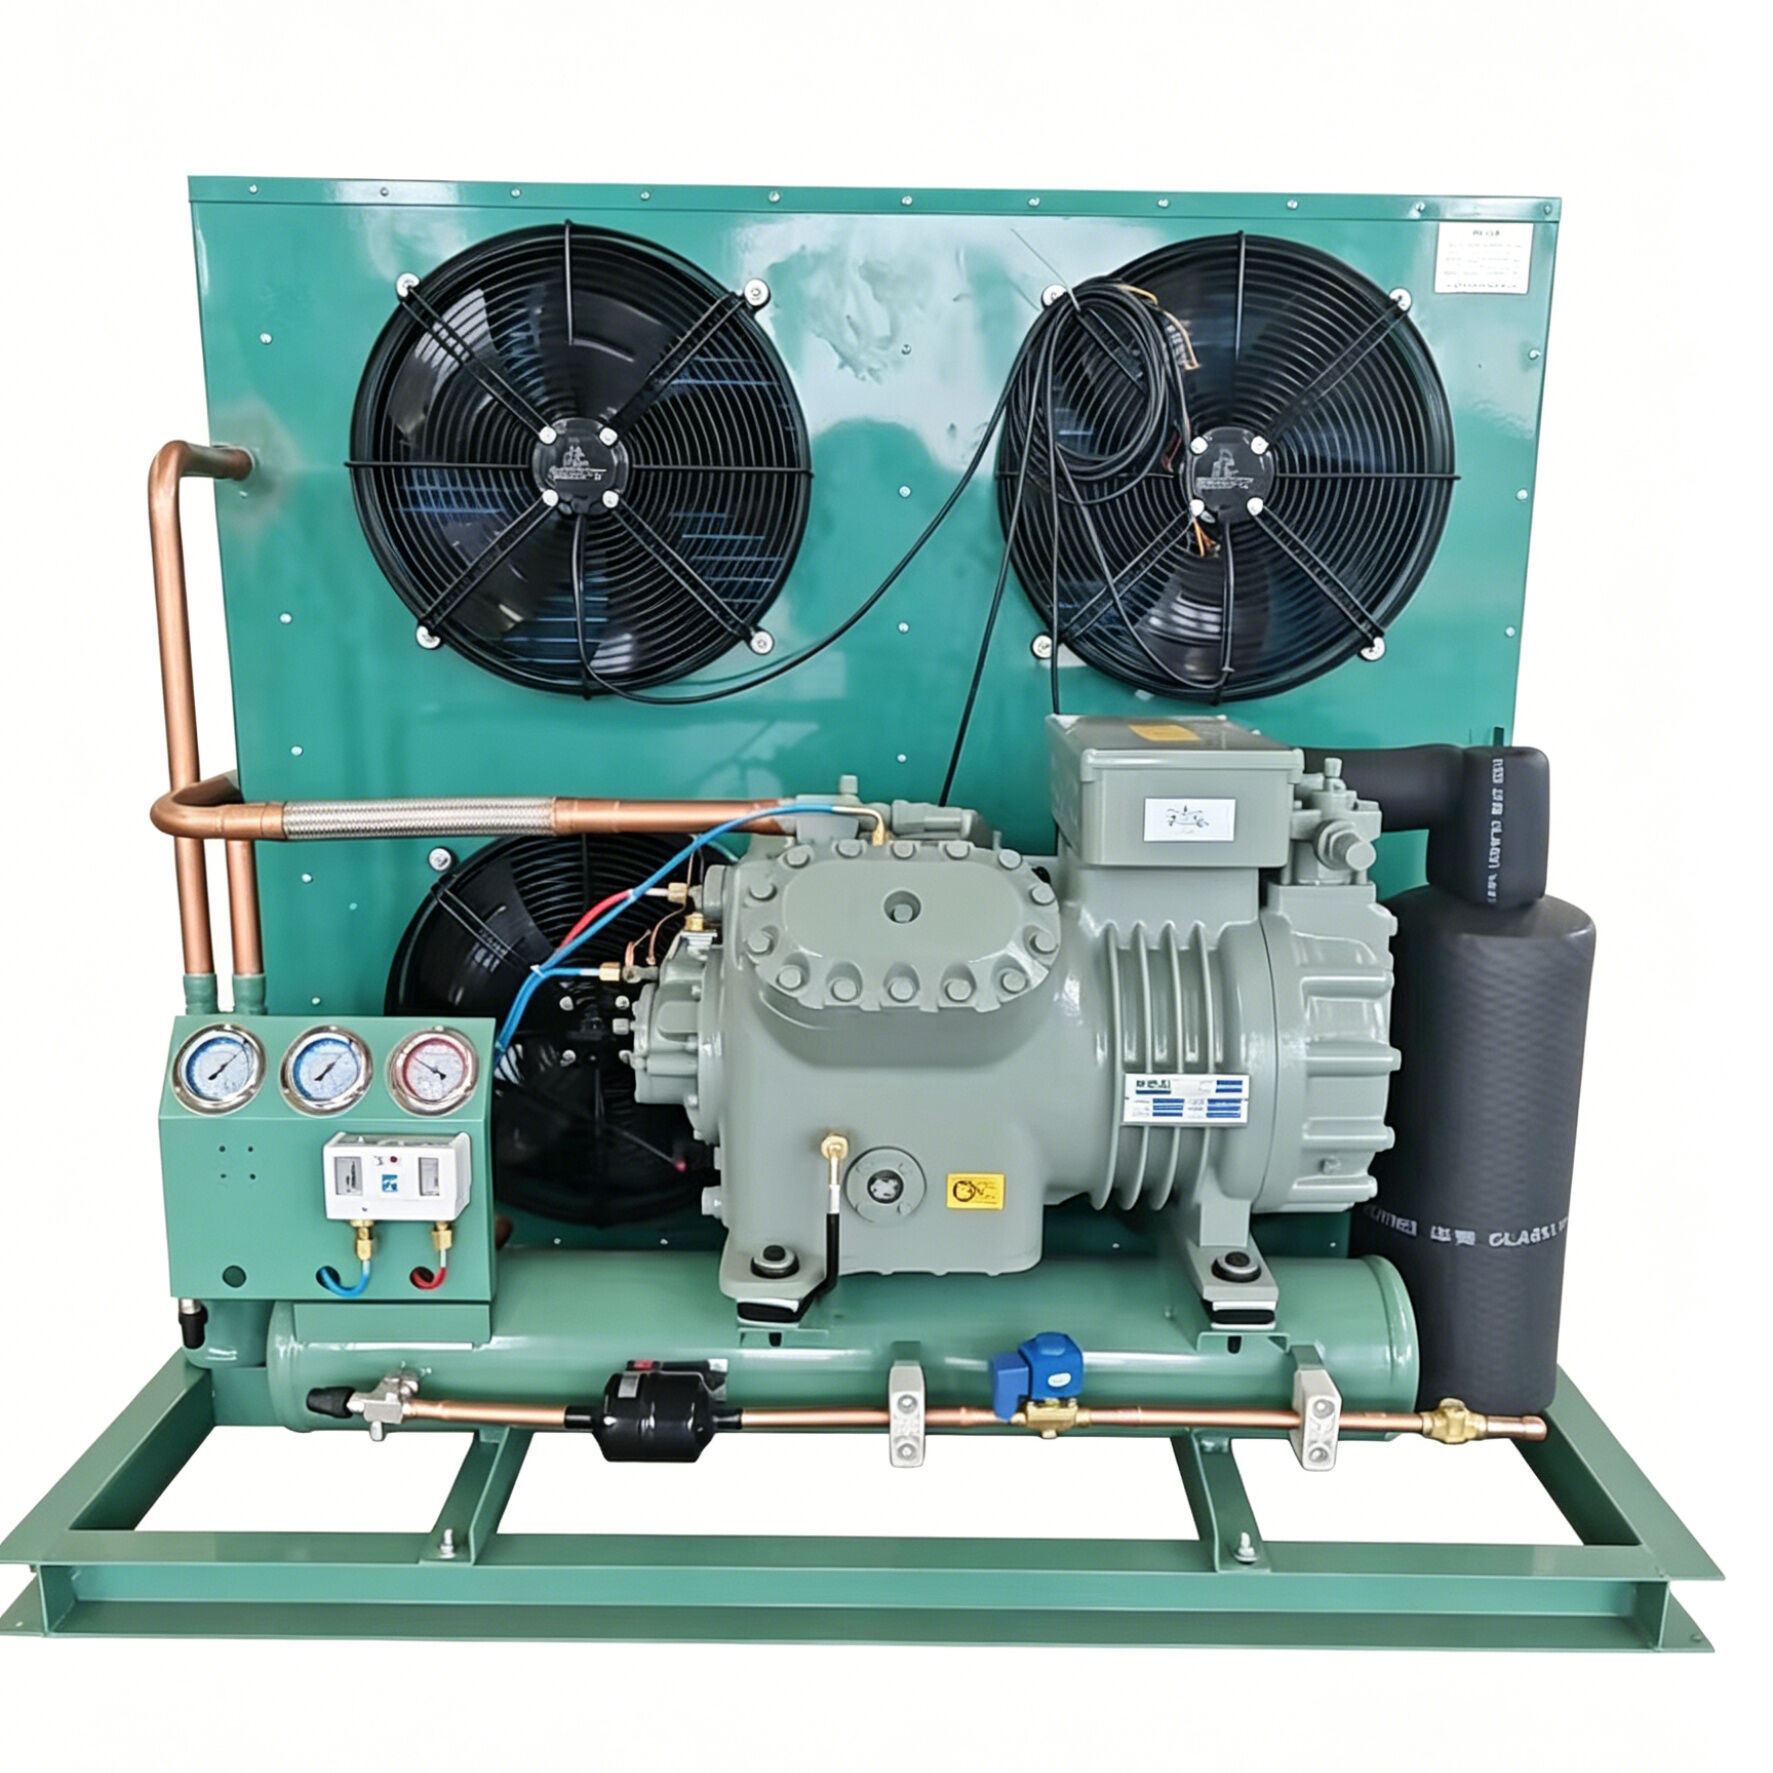
The quality h type condensing unit represents a sophisticated refrigeration solution engineered to deliver exceptional cooling performance across diverse commercial and industrial applications. This advanced system integrates a high-efficiency compressor, precision-engineered condenser coil, and intelligent control mechanisms within a compact H-shaped configuration that maximizes heat exchange efficiency while minimizing spatial requirements. The quality h type condensing unit operates by compressing refrigerant gas, facilitating heat rejection through the condenser, and maintaining optimal pressure levels throughout the refrigeration cycle. Its technological features include corrosion-resistant copper tubing, aluminum fin construction for enhanced thermal conductivity, and weather-resistant housing that ensures reliable operation in challenging environmental conditions. The unit incorporates advanced fan technology that optimizes airflow patterns, reducing energy consumption while maintaining consistent cooling capacity. Applications span from supermarket refrigeration systems and cold storage facilities to food processing plants, pharmaceutical manufacturing, and hospitality industry installations. The quality h type condensing unit accommodates various refrigerant types, including environmentally friendly options that comply with international environmental standards. Its modular design facilitates straightforward installation procedures and simplifies maintenance protocols, reducing operational downtime. Temperature control precision, noise reduction engineering, and vibration-dampening components make the quality h type condensing unit suitable for both indoor and outdoor installations where performance reliability and energy efficiency remain paramount considerations for facility managers and refrigeration specialists.
 EN