Evaporative Condensing Unit Factory Solutions

All Categories

evaporative condensing unit factory

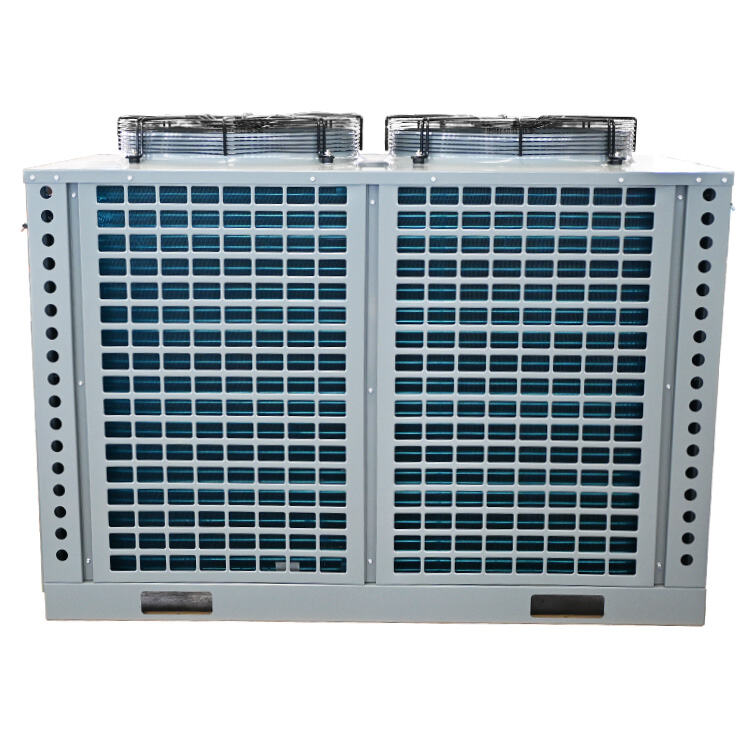
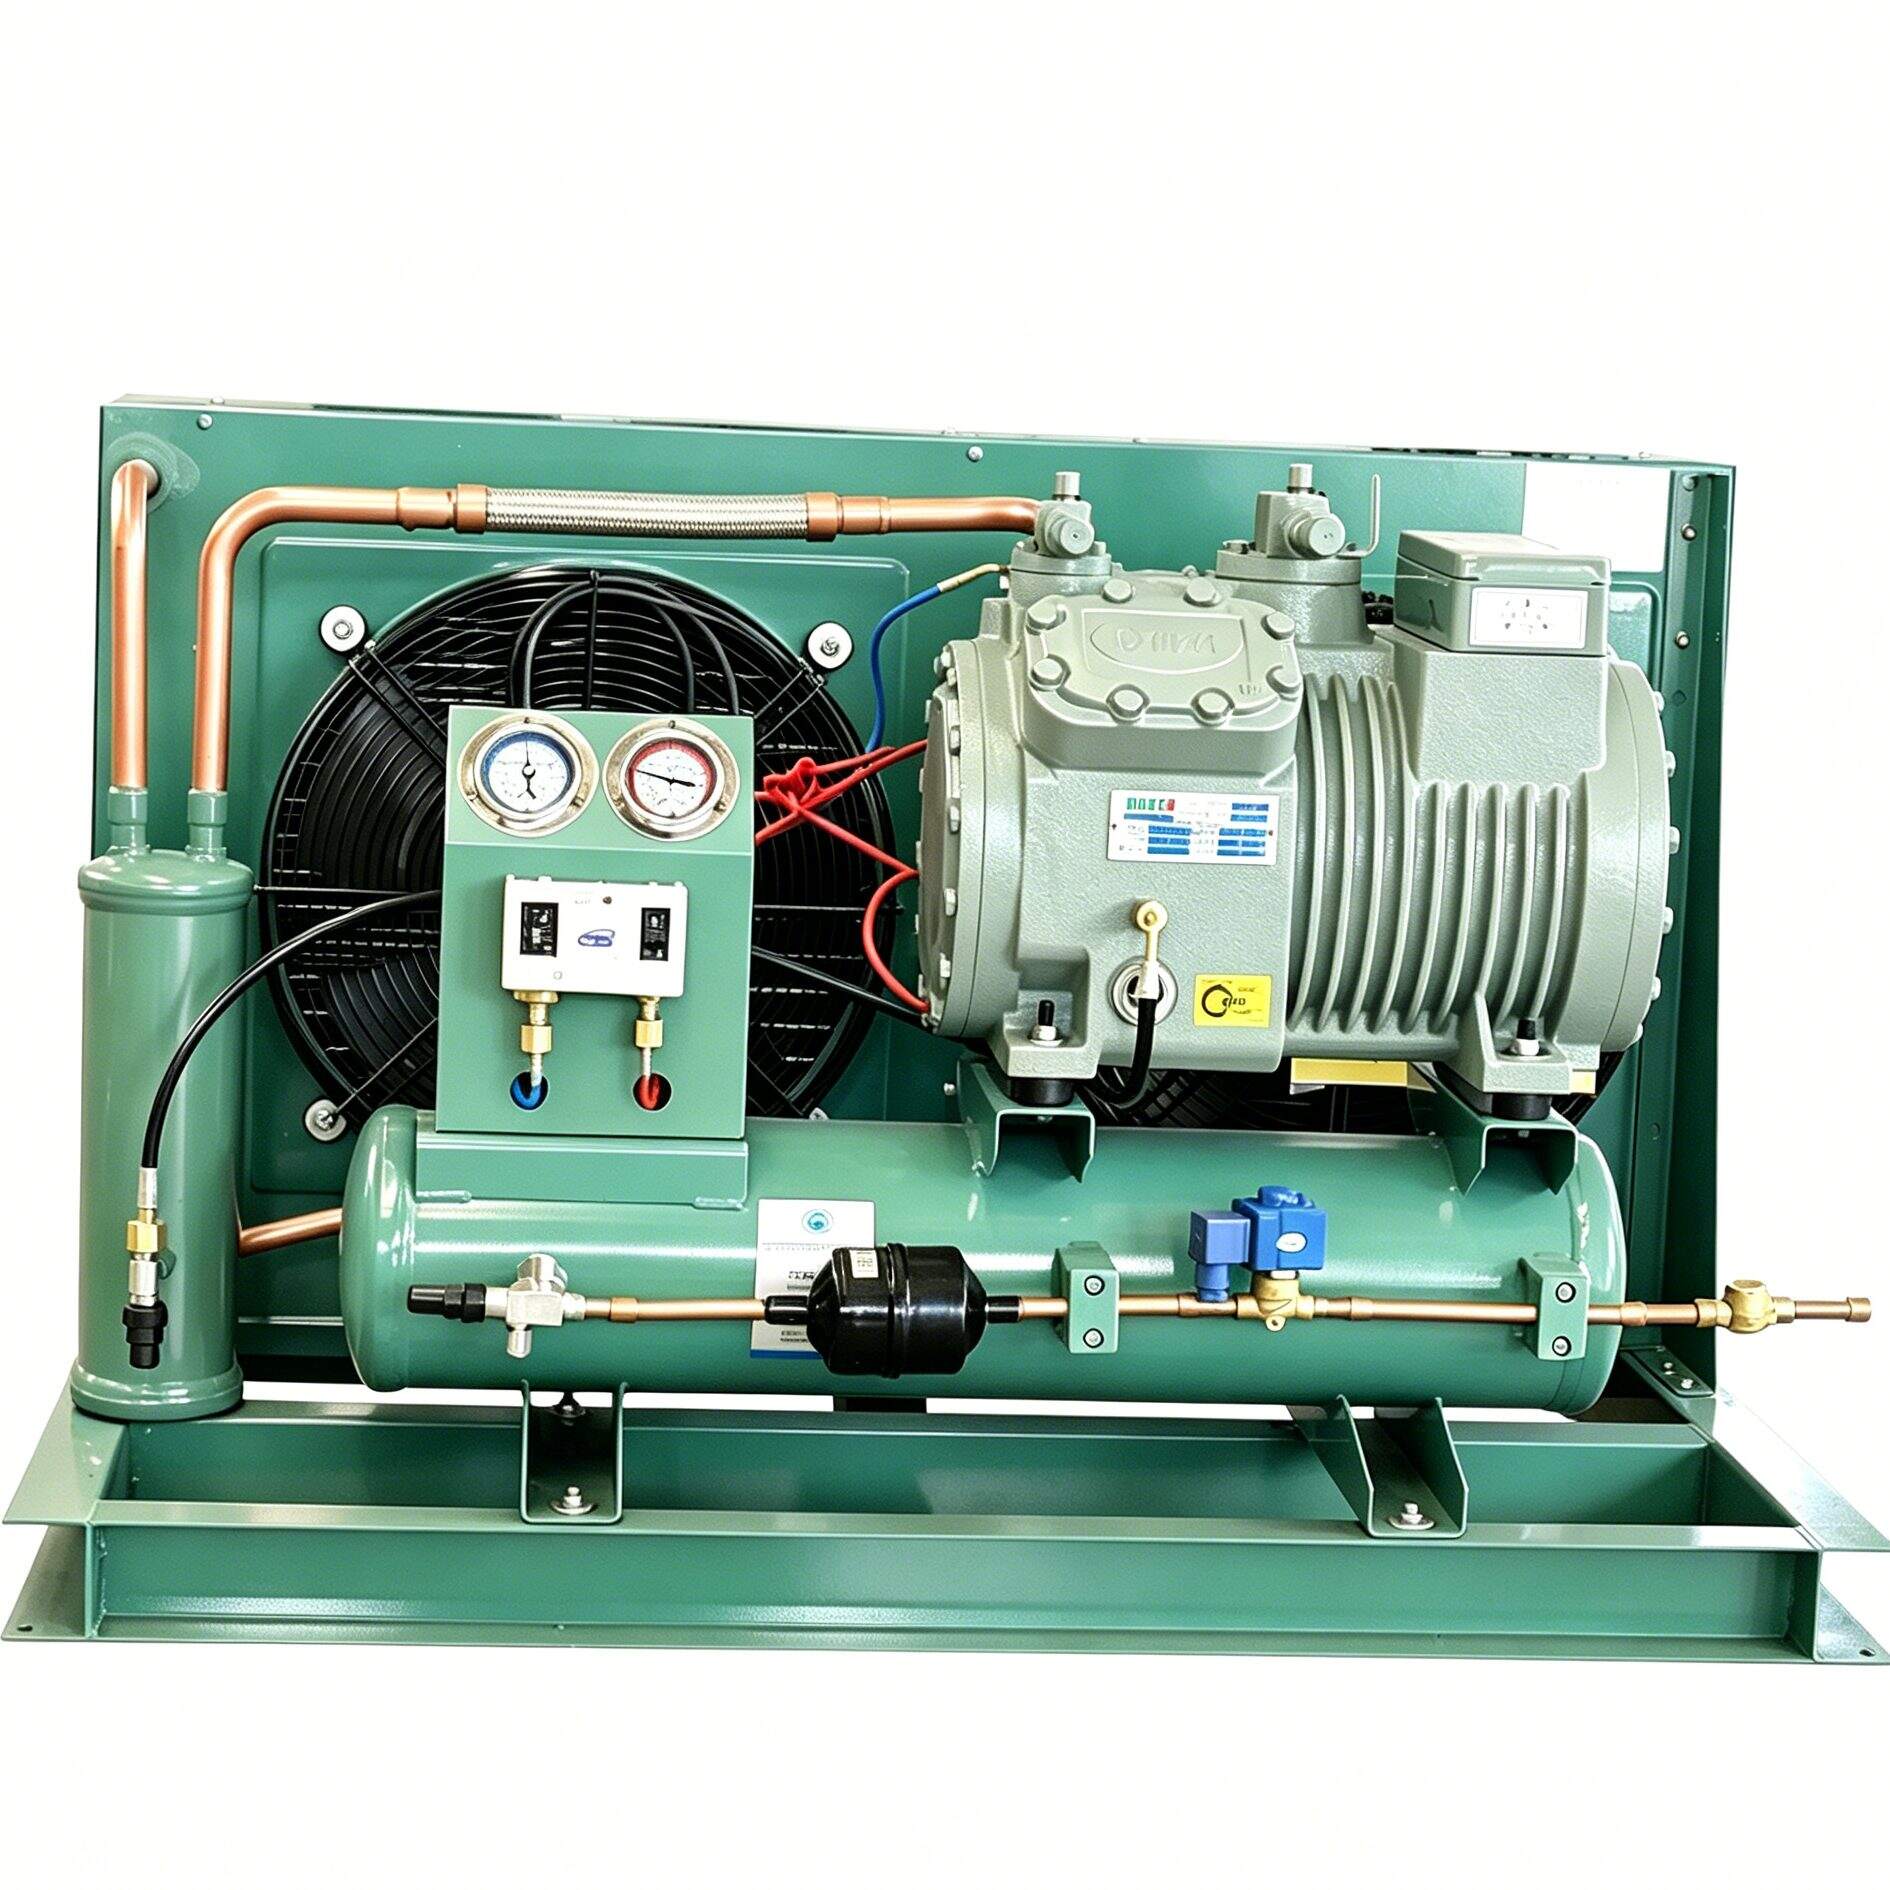
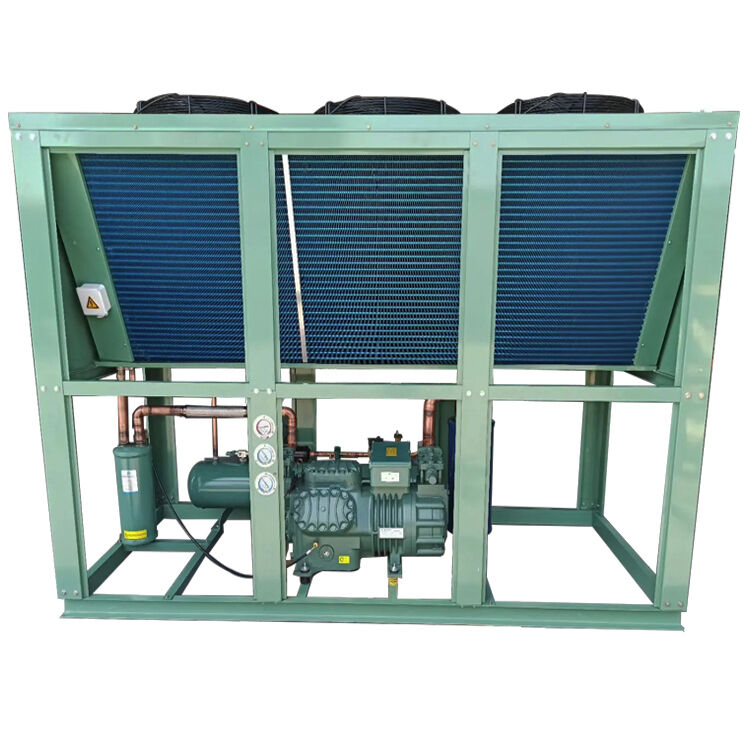
An evaporative condensing unit factory specializes in manufacturing advanced cooling systems that combine evaporation and condensation processes to achieve superior heat rejection efficiency. These facilities produce units designed for commercial refrigeration, industrial cooling applications, and HVAC systems where energy efficiency and environmental performance are critical. The main function of products from an evaporative condensing unit factory involves using water evaporation to cool refrigerant vapor, converting it back to liquid state while consuming significantly less energy than traditional air-cooled systems. Technological features include precision-engineered heat exchangers, high-efficiency spray systems, and integrated controls that optimize water usage and cooling performance. Modern evaporative condensing unit factory operations employ automated manufacturing processes, quality testing protocols, and sustainable production methods to ensure consistent product reliability. These units find applications across supermarkets, cold storage warehouses, food processing plants, pharmaceutical facilities, and data centers where maintaining precise temperatures is essential. The factory environment typically includes specialized fabrication areas, testing chambers, and quality assurance stations to verify each unit meets industry standards. Products from an evaporative condensing unit factory deliver cooling capacities ranging from small-scale commercial units to large industrial systems, with customization options available for specific operational requirements. The manufacturing process emphasizes durability, corrosion resistance, and ease of maintenance, ensuring long-term performance in diverse environmental conditions while reducing total cost of ownership for end users.
Popular Products

Choosing products from an evaporative condensing unit factory provides substantial cost savings through reduced energy consumption, typically achieving 30-50 percent lower electricity usage compared to conventional air-cooled alternatives. This efficiency translates directly into lower operational expenses, making these units financially attractive for businesses managing tight budget constraints. The water-based cooling mechanism operates more effectively in hot climates where air-cooled systems struggle, maintaining consistent performance even during peak summer temperatures. Buyers benefit from compact designs that require less installation space while delivering equivalent or superior cooling capacity, maximizing facility utilization. Environmental advantages include reduced carbon footprint and lower greenhouse gas emissions, helping organizations meet sustainability goals and comply with increasingly strict environmental regulations. The evaporative condensing unit factory produces equipment with longer operational lifespans due to components running at lower temperatures, reducing thermal stress and mechanical wear. Maintenance requirements are straightforward, with accessible components and simple servicing procedures that minimize downtime and reduce labor costs. These units operate more quietly than traditional systems, creating better working environments and satisfying noise ordinance requirements in urban settings. Water consumption remains economical despite the evaporative process, with modern designs incorporating recirculation systems and efficient nozzles. Application suitability extends across multiple industries, from food retail to pharmaceuticals, where reliable temperature control protects product quality and ensures regulatory compliance. Decision-makers appreciate the quick return on investment, typically recovering initial costs within two to four years through energy savings alone. The manufacturing expertise concentrated in an evaporative condensing unit factory ensures product consistency, technical support availability, and access to replacement parts throughout the equipment lifecycle.

Practical Tips

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

28

Feb

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

View More
Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

28

Feb

Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

View More
Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

28

Feb

Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

evaporative condensing unit factory

Advanced Energy Efficiency Technology

Advanced Energy Efficiency Technology

Products from an evaporative condensing unit factory incorporate cutting-edge energy-saving technology that fundamentally transforms cooling economics for commercial and industrial operations. The evaporative process leverages the natural cooling power of water evaporation, which requires far less electrical energy than forcing air across condenser coils. This physical advantage translates into measurable reductions in power consumption, with facilities reporting energy cost decreases of 35-45 percent annually after installation. The technology particularly excels in warm climates where traditional systems consume excessive electricity fighting against high ambient temperatures. Smart control systems integrated during manufacturing optimize fan speeds, water flow rates, and cycle timing based on real-time cooling demands, preventing energy waste during partial load conditions. The factory engineering approach ensures each component works synergistically to maximize coefficient of performance, delivering more cooling output per unit of energy input. This efficiency advantage compounds over the equipment's operational life, providing cumulative savings that substantially exceed initial investment costs while contributing to corporate sustainability objectives and reducing environmental impact.
Robust Manufacturing Quality Standards

Robust Manufacturing Quality Standards

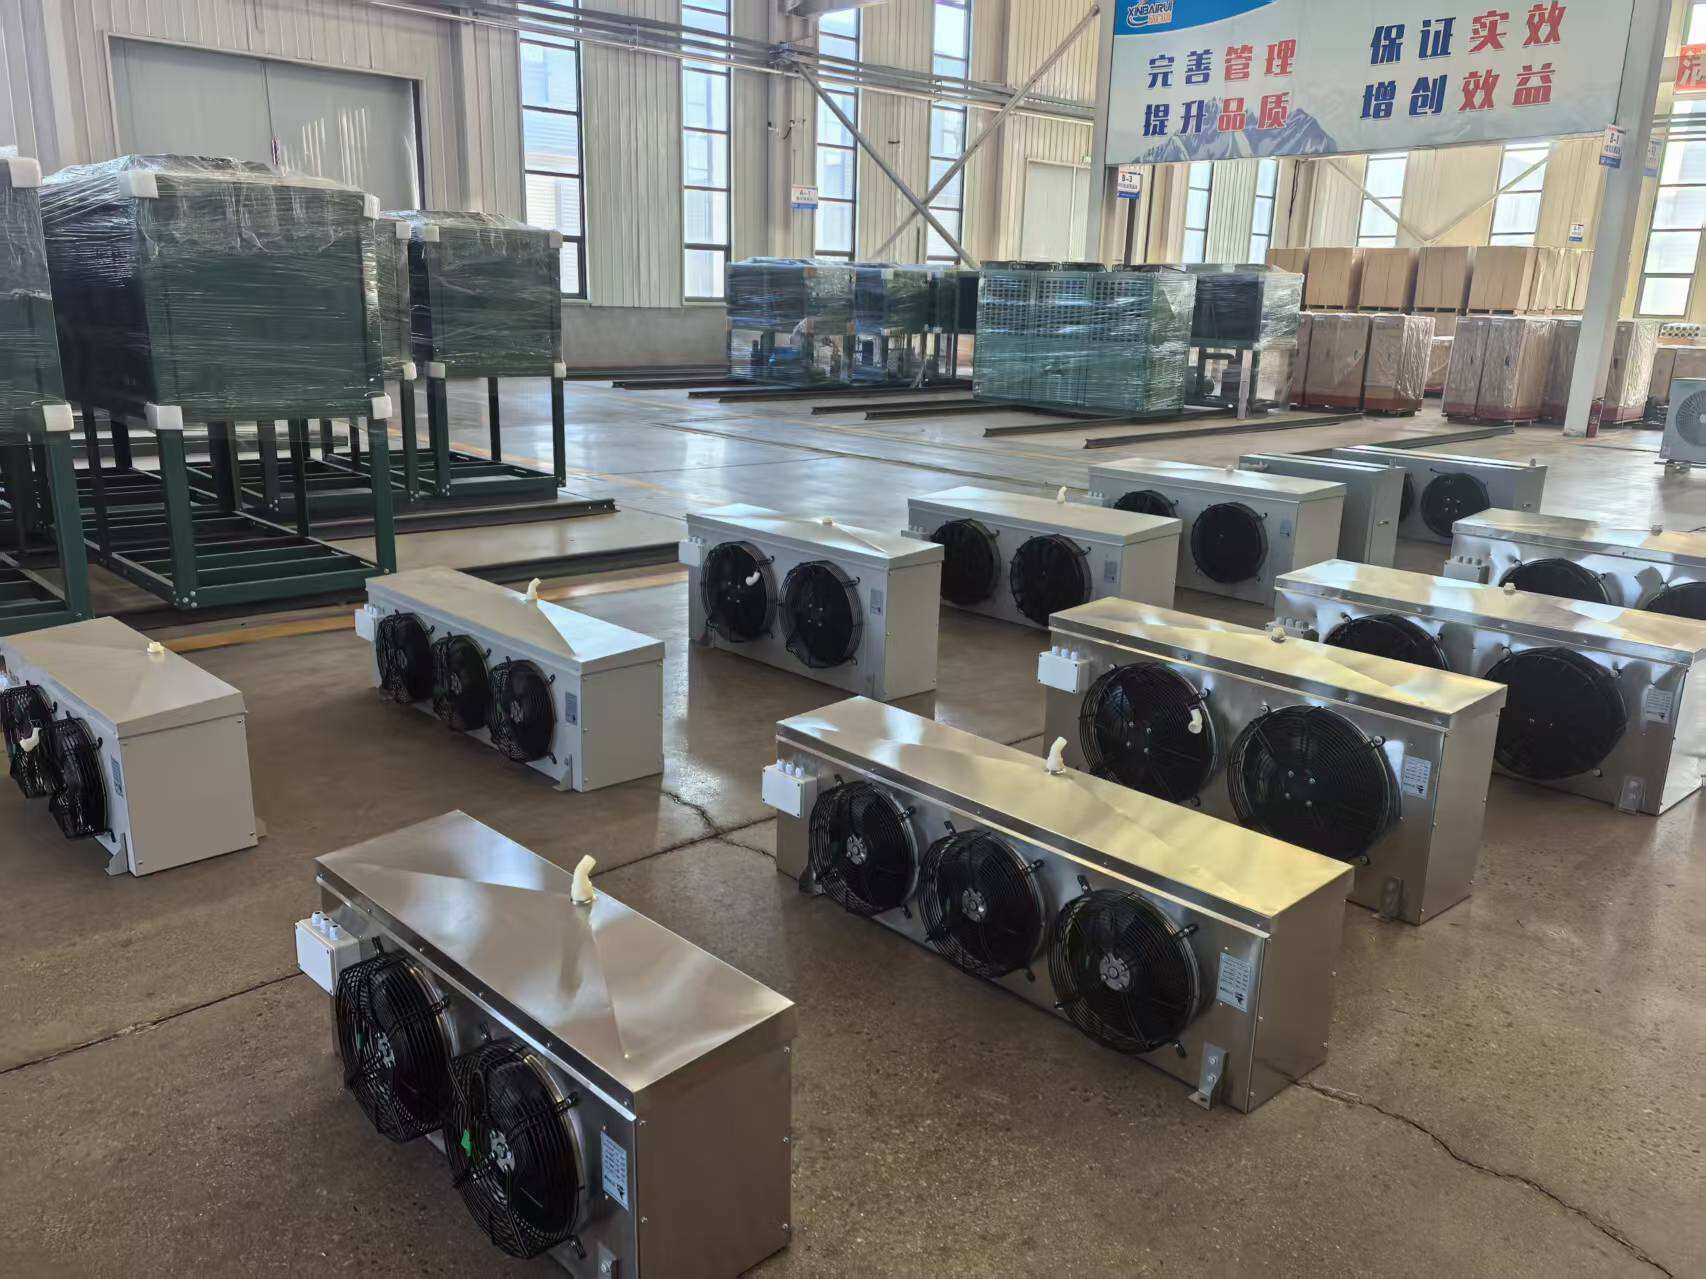
An evaporative condensing unit factory maintains rigorous quality control protocols throughout production, ensuring every unit meets exacting performance and durability standards before shipment. Manufacturing facilities employ precision welding techniques, corrosion-resistant materials, and multi-stage quality inspections to prevent defects and guarantee long-term reliability. The factory environment allows controlled assembly conditions that eliminate contamination risks and ensure proper component integration, advantages difficult to achieve with field-assembled systems. Automated testing procedures verify refrigerant circuit integrity, electrical safety, water distribution uniformity, and thermal performance against design specifications. This comprehensive quality assurance means customers receive equipment ready for immediate installation with minimal commissioning requirements. The standardized production processes characteristic of an evaporative condensing unit factory create consistency across units, simplifying maintenance planning and parts inventory management for operators running multiple systems. Factory testing identifies potential issues before deployment, reducing costly field failures and service calls. The manufacturing expertise concentrated in these specialized facilities translates into superior product reliability, with typical operational lifespans exceeding 15-20 years when properly maintained, protecting buyer investments and ensuring uninterrupted cooling performance.
Versatile Application Compatibility

Versatile Application Compatibility

The diverse product range emerging from an evaporative condensing unit factory addresses cooling requirements across numerous industries and operational contexts, providing solutions for both standard and specialized applications. Manufacturing flexibility allows customization of capacity ranges, physical configurations, and control interfaces to match specific facility requirements without expensive custom engineering. These units integrate seamlessly with existing refrigeration systems, offering retrofit compatibility that enables performance upgrades without complete system replacement. The evaporative condensing unit factory produces models suitable for rooftop installations, ground-level mounting, and indoor placement with proper ventilation, accommodating various architectural constraints. Application versatility extends from small retail refrigeration to large-scale industrial processes, with capacity options spanning several tons to hundreds of tons of cooling. The factory can configure units for different refrigerants, voltage requirements, and climate conditions, ensuring optimal performance regardless of geographic location or operational environment. This adaptability makes products from an evaporative condensing unit factory ideal for food service, healthcare, manufacturing, logistics, and hospitality sectors where reliable temperature control impacts product quality, operational efficiency, and regulatory compliance. The comprehensive application range reduces buyer risk by providing proven solutions backed by factory engineering expertise and technical support.
Evaporative Condensing Unit Factory Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
Evaporative Condensing Unit Factory Solutions

Copyright © 2026 Ningbo Lucky Star Import & Export Co., Ltd. All rights reserved.  -  Privacy policy