High Efficiency Hermetic Condensing Unit Guide

All Categories

high efficiency hermetic condensing unit

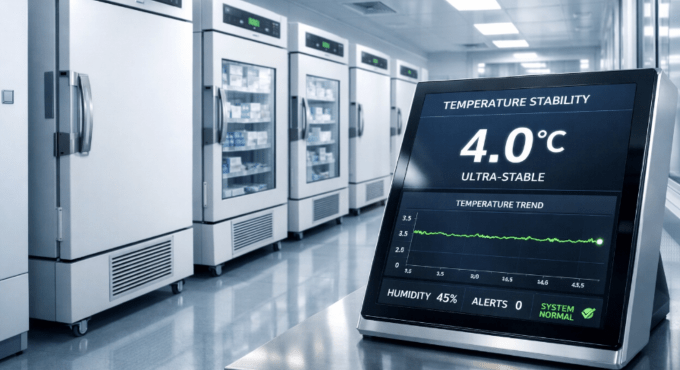
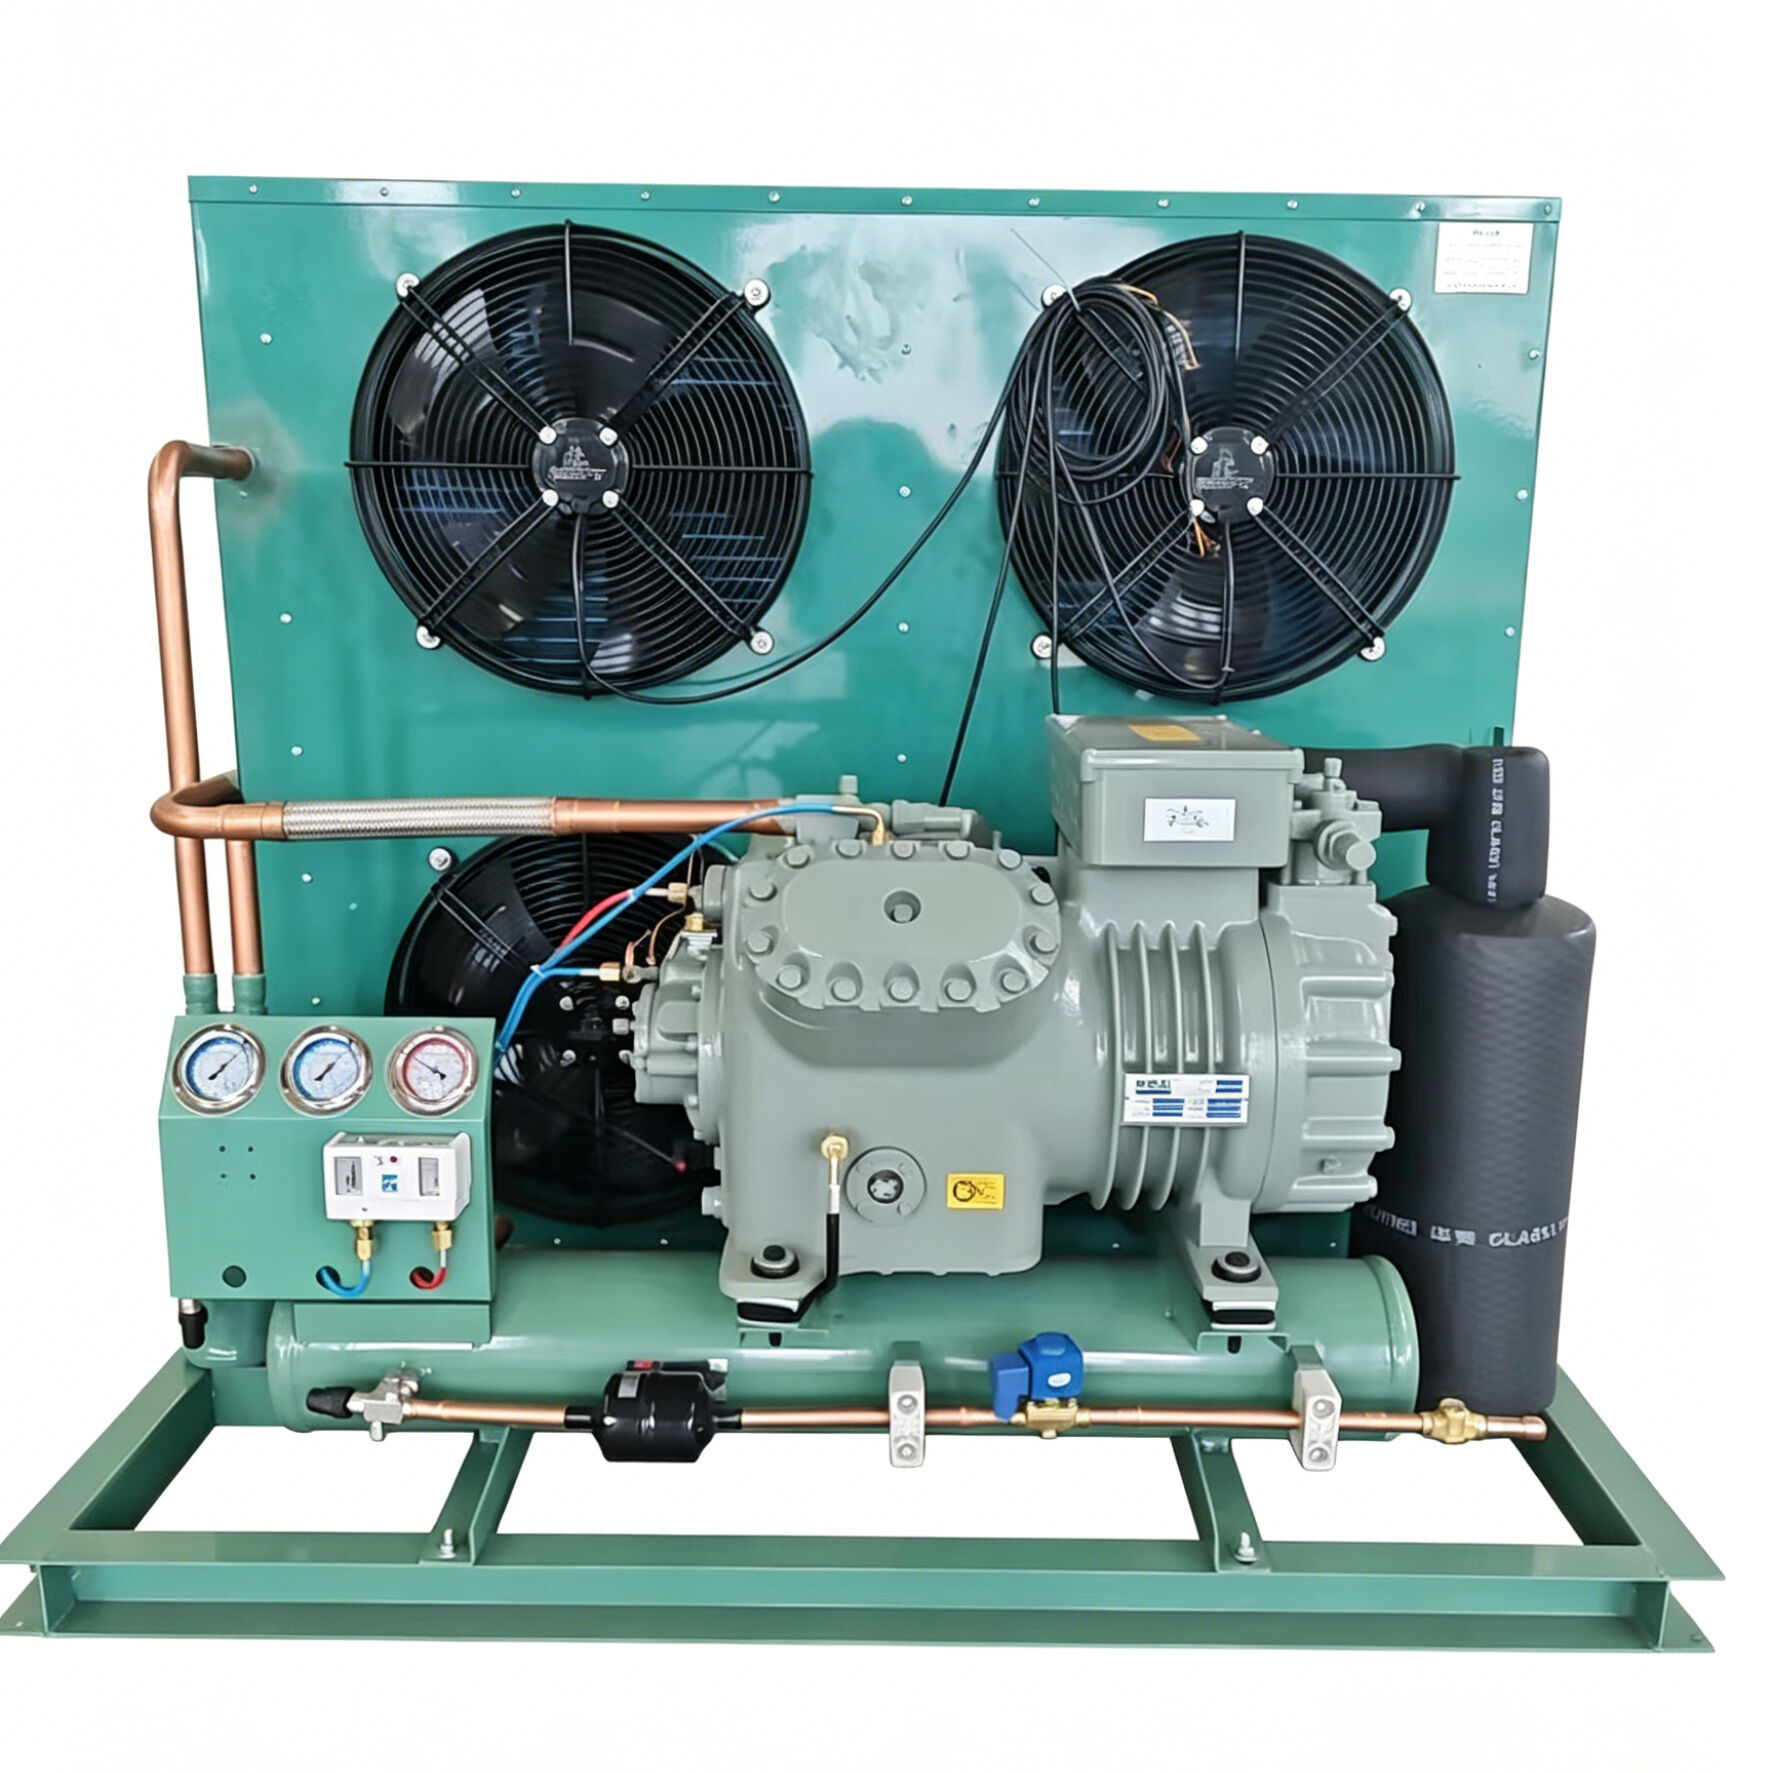
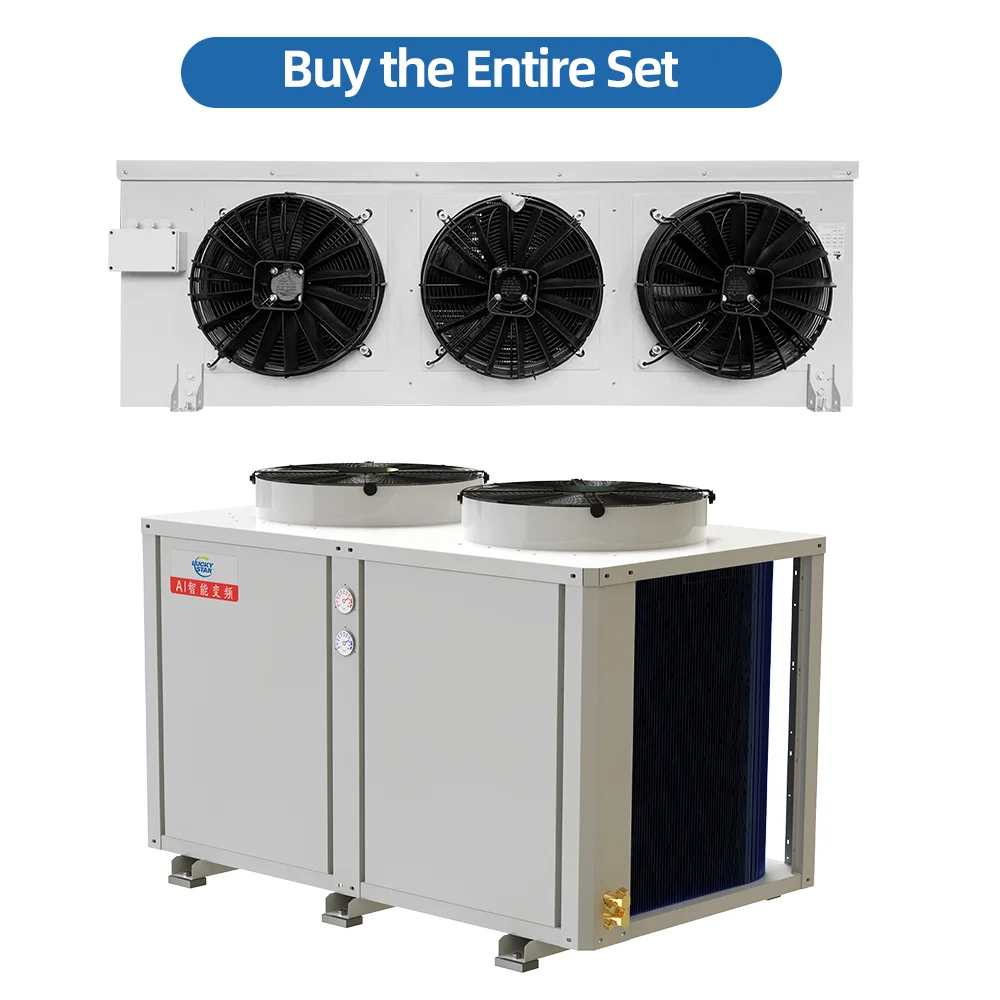
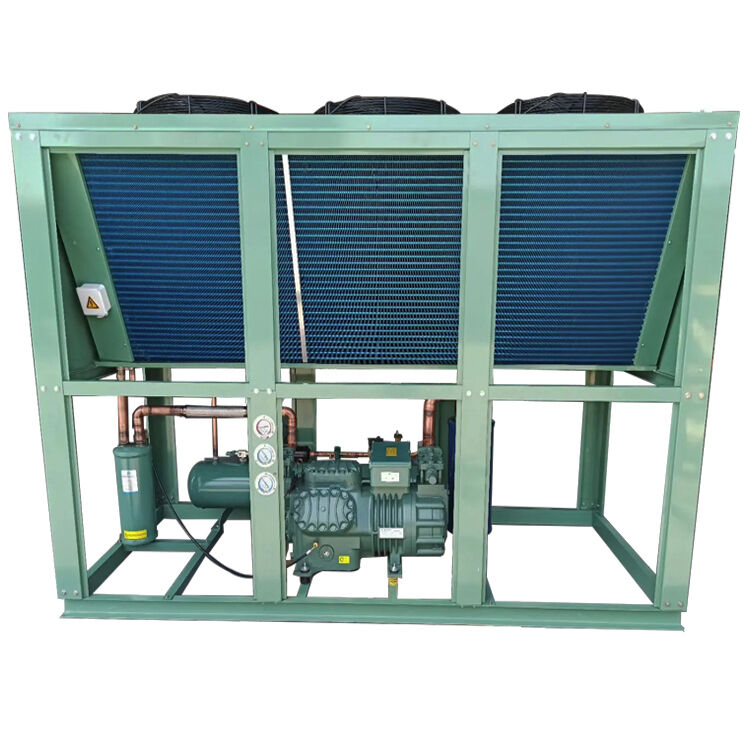
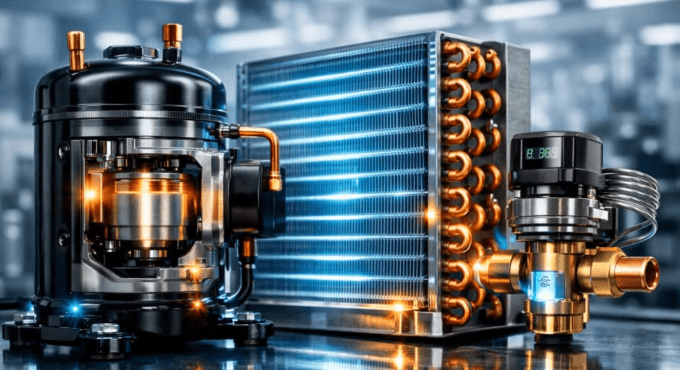
A high efficiency hermetic condensing unit represents a sophisticated refrigeration solution designed to deliver superior cooling performance while minimizing energy consumption. This integrated system combines a hermetically sealed compressor, condenser coil, cooling fan, and control components within a compact framework, creating a self-contained refrigeration powerhouse. The hermetic design ensures that the compressor motor and refrigerant circuit remain completely sealed from external contaminants, eliminating the risk of refrigerant leakage and extending operational lifespan significantly. These units function by compressing refrigerant gas to high pressure and temperature, then releasing heat through the condenser coil as ambient air passes over the fins. The high efficiency hermetic condensing unit achieves exceptional performance through advanced compressor technology, optimized heat exchanger designs, and intelligent control systems that adapt to varying load conditions. Primary applications span commercial refrigeration, cold storage facilities, food processing plants, pharmaceutical storage, supermarket display cases, walk-in coolers, and industrial climate control systems. The technological features include variable speed compressor operation, enhanced heat transfer surfaces, precision temperature control, and environmentally friendly refrigerant compatibility. Installation flexibility allows both indoor and outdoor mounting configurations, while the hermetic construction reduces maintenance requirements substantially. These units deliver consistent cooling capacity across diverse operating conditions, making them essential components in applications where temperature stability, energy efficiency, and reliability are paramount considerations for business operations and product preservation.
New Products

Investing in a high efficiency hermetic condensing unit delivers substantial cost savings through dramatically reduced electricity consumption, with modern designs achieving energy efficiency improvements of 30 to 50 percent compared to conventional systems. Your monthly operating expenses decrease significantly as these units consume less power while maintaining consistent cooling performance, directly improving your bottom line profitability. The hermetic compressor design eliminates shaft seals that typically wear and leak in open compressor systems, meaning you avoid refrigerant loss, costly recharge services, and environmental compliance issues. This sealed construction protects internal components from moisture, dust, and airborne contaminants that cause premature failure, extending equipment lifespan beyond 15 years with minimal maintenance intervention. You benefit from quieter operation due to advanced vibration dampening and sound insulation, creating more comfortable working environments in retail spaces, restaurants, and food service operations. The compact footprint maximizes usable space in your facility, while versatile mounting options accommodate challenging installation locations without sacrificing performance. Advanced control systems automatically adjust compressor speed and fan operation based on actual cooling demand, preventing energy waste during low-load periods and part-load conditions. You gain precise temperature control that protects valuable inventory, maintains product quality, and ensures regulatory compliance in temperature-sensitive applications. The high efficiency hermetic condensing unit operates reliably across wide ambient temperature ranges, maintaining performance during seasonal temperature fluctuations without manual adjustments. Reduced heat rejection compared to less efficient systems lowers the burden on facility air conditioning, creating additional indirect energy savings. Quick installation with pre-charged refrigerant circuits and factory-tested components minimizes downtime and gets your refrigeration system operational faster, reducing project costs and accelerating return on investment.

Latest News

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

28

Feb

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

View More
Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

28

Feb

Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

View More
Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

28

Feb

Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

high efficiency hermetic condensing unit

Advanced Energy Efficiency Technology

Advanced Energy Efficiency Technology

The high efficiency hermetic condensing unit incorporates cutting-edge compressor technology and optimized refrigeration cycle design to achieve unprecedented energy performance levels. Variable speed scroll or reciprocating compressors adjust capacity precisely to match cooling demand, eliminating the wasteful on-off cycling that plagues fixed-speed systems. Enhanced heat exchanger surfaces with micro-channel or enhanced tube designs maximize heat transfer efficiency, allowing smaller, lighter condensers to achieve the same cooling capacity as larger conventional units. Intelligent electronic expansion valves maintain optimal refrigerant flow under all operating conditions, ensuring the evaporator and condenser operate at peak efficiency continuously. High-efficiency motors with improved power factor and reduced electrical losses convert more input energy into useful cooling work rather than waste heat. The hermetic design itself contributes to efficiency by eliminating mechanical shaft seals that create friction losses and require parasitic oil pump operation. Advanced fan blade designs move greater air volumes with less energy input, while EC motor technology enables precise fan speed modulation. These combined technological innovations translate directly into lower operating costs, reduced environmental impact, and faster payback periods that make upgrading to high efficiency hermetic condensing units a financially compelling decision for facility managers and business owners seeking competitive advantages through operational excellence.
Superior Reliability and Longevity

Superior Reliability and Longevity

The hermetic construction of these condensing units provides unmatched reliability by completely sealing the compressor motor and refrigerant circuit from external environmental factors that compromise performance and shorten equipment life. Unlike open compressor designs with external motors connected through shaft seals, the high efficiency hermetic condensing unit eliminates potential leak paths, preventing refrigerant loss that degrades cooling capacity and creates expensive service calls. The sealed environment protects precision-machined compressor components from moisture intrusion that causes rust, corrosion, and bearing failure, while preventing dust and airborne particles from contaminating lubricating oil and scoring cylinder walls. Factory-sealed refrigerant circuits undergo rigorous pressure testing and quality assurance procedures before leaving the manufacturing facility, ensuring leak-free operation from initial startup. Vibration-isolated mounting and precision-balanced rotating assemblies minimize mechanical wear on bearings and internal components, extending service intervals and reducing unexpected breakdowns. Thermal overload protection and advanced monitoring systems prevent damage from abnormal operating conditions, automatically shutting down the unit before catastrophic failure occurs. The robust construction withstands harsh environmental conditions including temperature extremes, humidity, and corrosive atmospheres that would rapidly degrade less protected equipment. This exceptional reliability translates to continuous operation, minimal maintenance requirements, and reduced total cost of ownership throughout the equipment lifecycle, providing peace of mind and predictable operating expenses for demanding commercial and industrial refrigeration applications.
Versatile Application Compatibility

Versatile Application Compatibility

The high efficiency hermetic condensing unit adapts seamlessly to diverse refrigeration requirements across multiple industries and application types, offering flexible solutions for businesses with varied cooling needs. These units accommodate different refrigerant types including traditional HFCs and emerging low-global-warming-potential alternatives, ensuring compliance with evolving environmental regulations and future-proofing your refrigeration investment. Wide capacity ranges from fractional horsepower units for small display cases to multi-compressor rack systems for large cold storage warehouses allow specification of appropriately sized equipment for any project scale. Temperature control capabilities span medium-temperature applications for fresh food storage and high-temperature air conditioning down to low-temperature frozen food preservation at sub-zero conditions. The units integrate easily with existing refrigeration controls and building management systems through standard communication protocols, enabling centralized monitoring and optimization of multiple refrigeration circuits. Outdoor-rated versions withstand weather exposure and temperature extremes, while indoor models offer quieter operation for customer-facing retail environments. Mounting flexibility includes floor-mounted, wall-mounted, and rooftop configurations that accommodate space constraints and architectural requirements. The high efficiency hermetic condensing unit works effectively with various evaporator types including forced-air coils, plate freezers, and shell-and-tube heat exchangers, supporting specialized processes across food service, pharmaceutical, chemical, and industrial sectors. This adaptability reduces inventory complexity for contractors and facility managers while simplifying equipment selection, procurement, and long-term service support across multiple locations and applications.
High Efficiency Hermetic Condensing Unit Guide

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
High Efficiency Hermetic Condensing Unit Guide

Copyright © 2026 Ningbo Lucky Star Import & Export Co., Ltd. All rights reserved.  -  Privacy policy