Water Cooled Condensing Unit Factory Solutions

All Categories

water cooled condensing unit factory

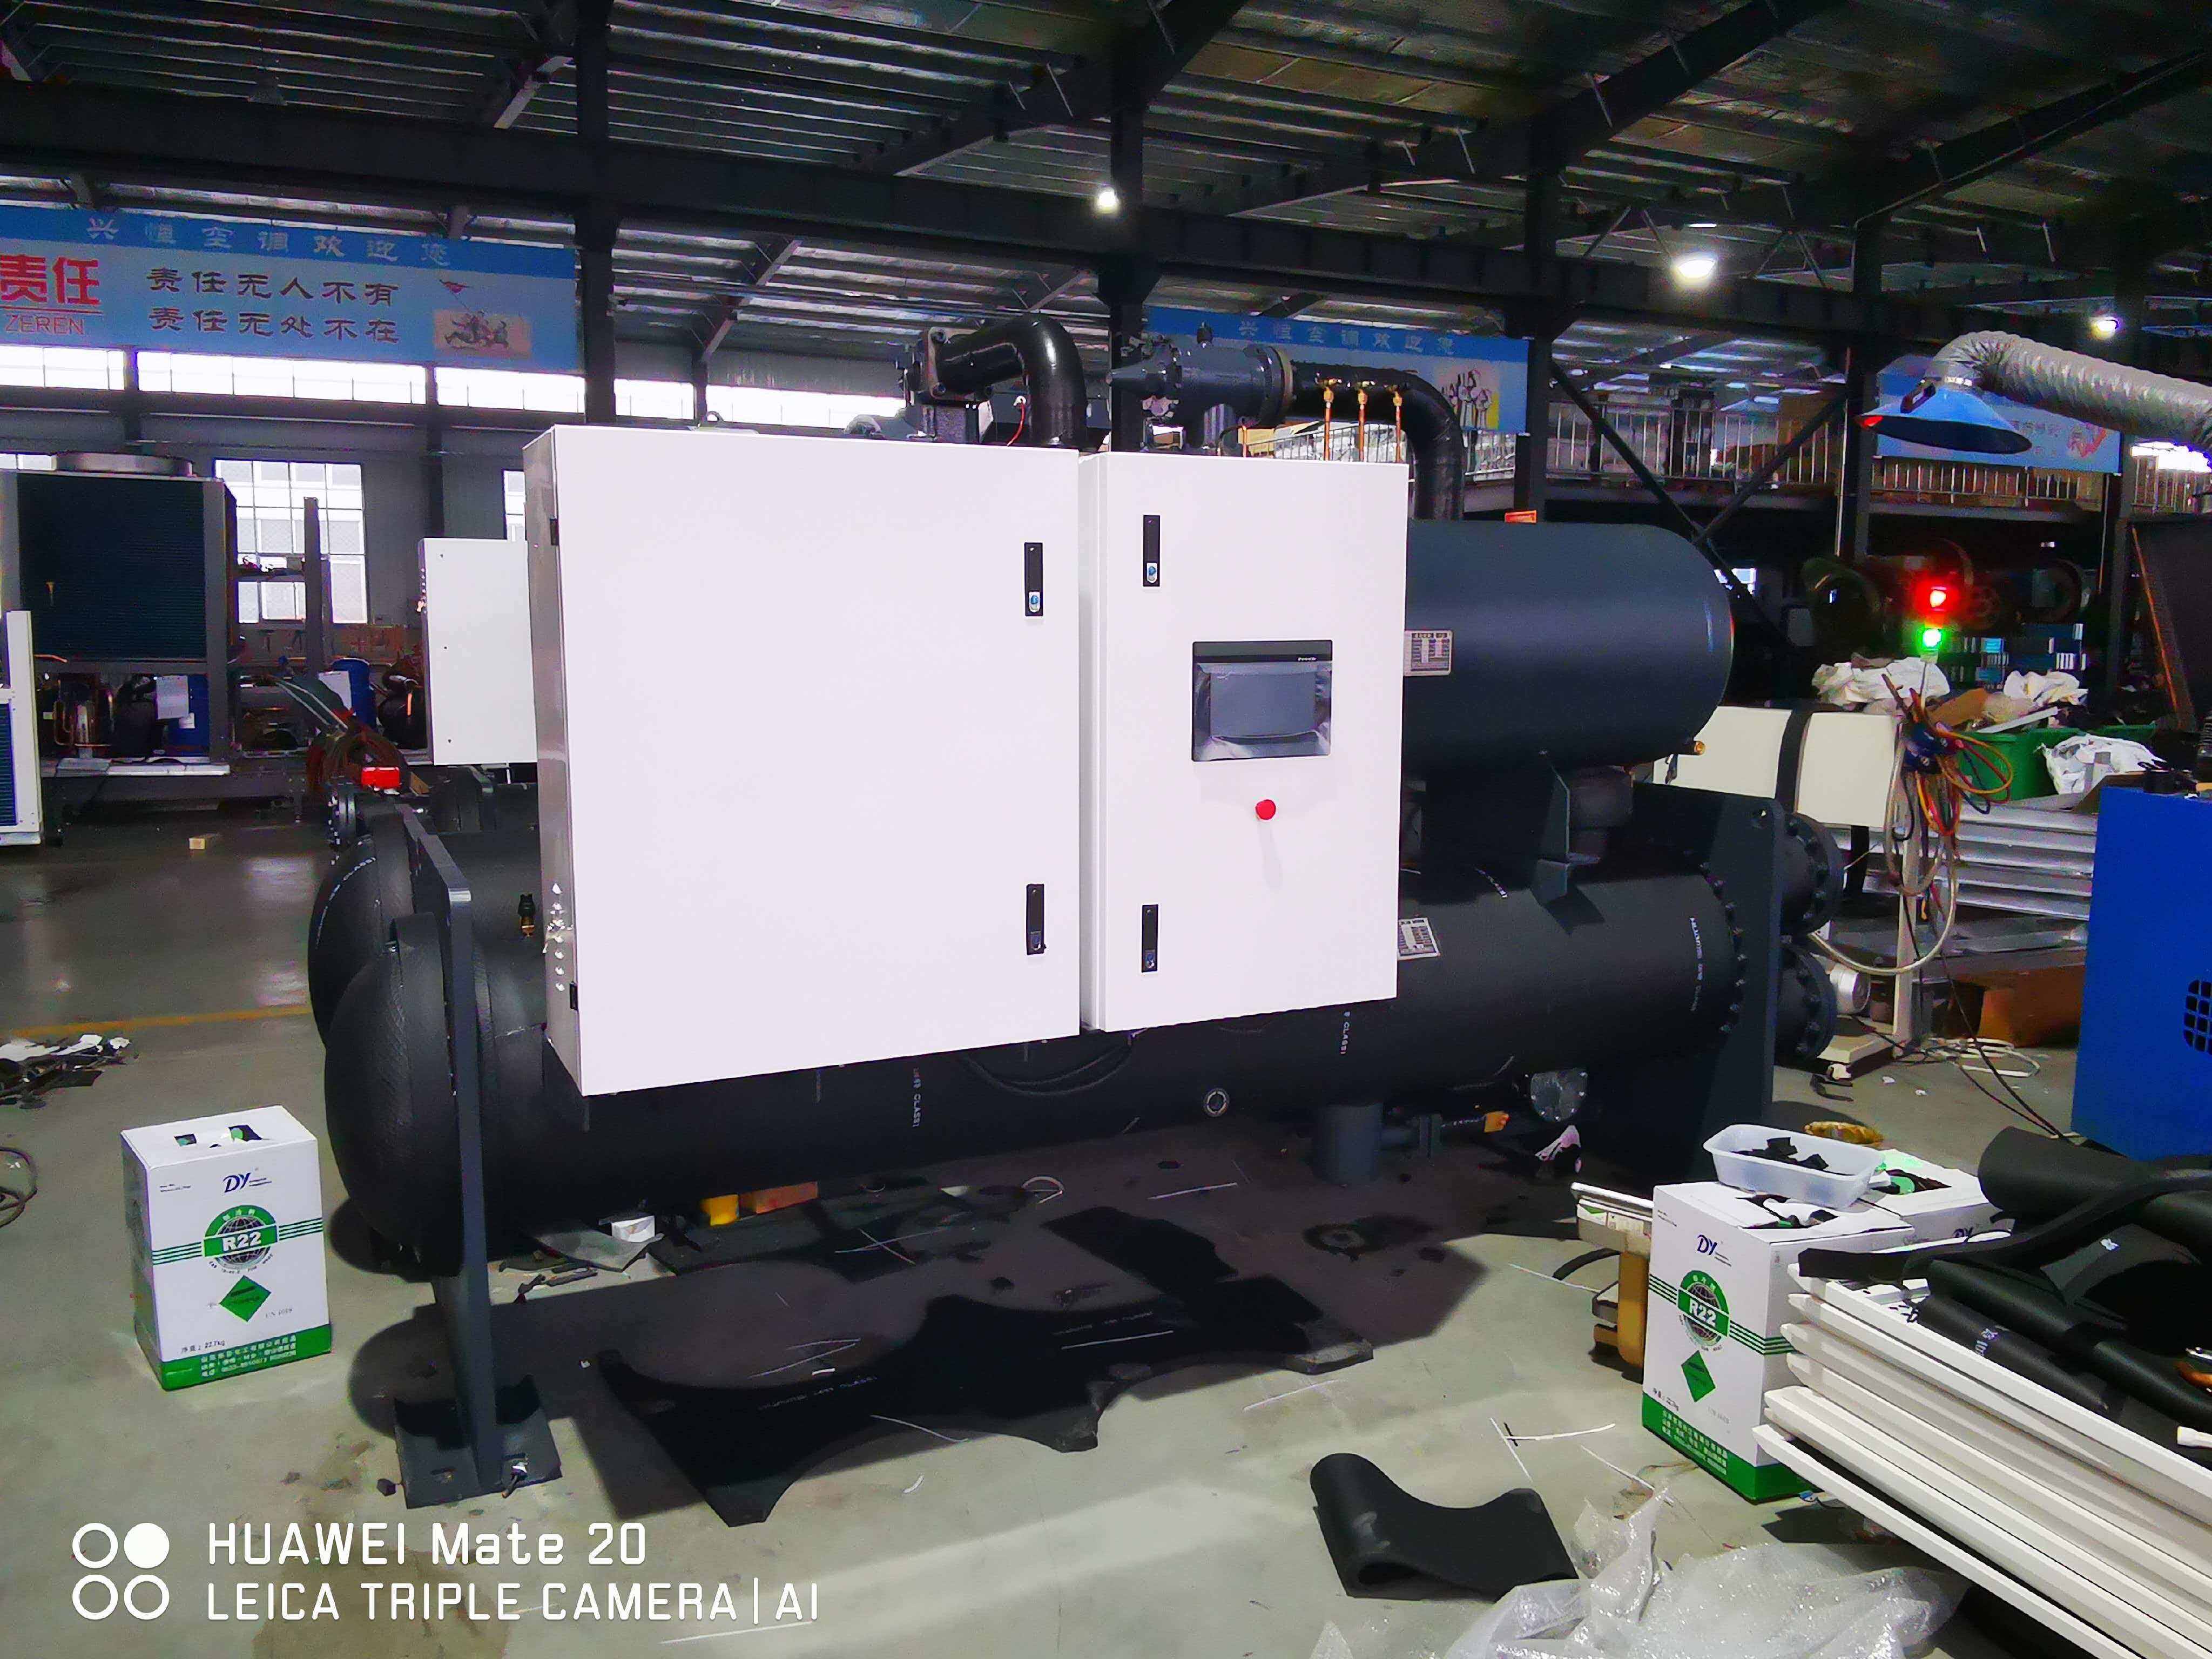
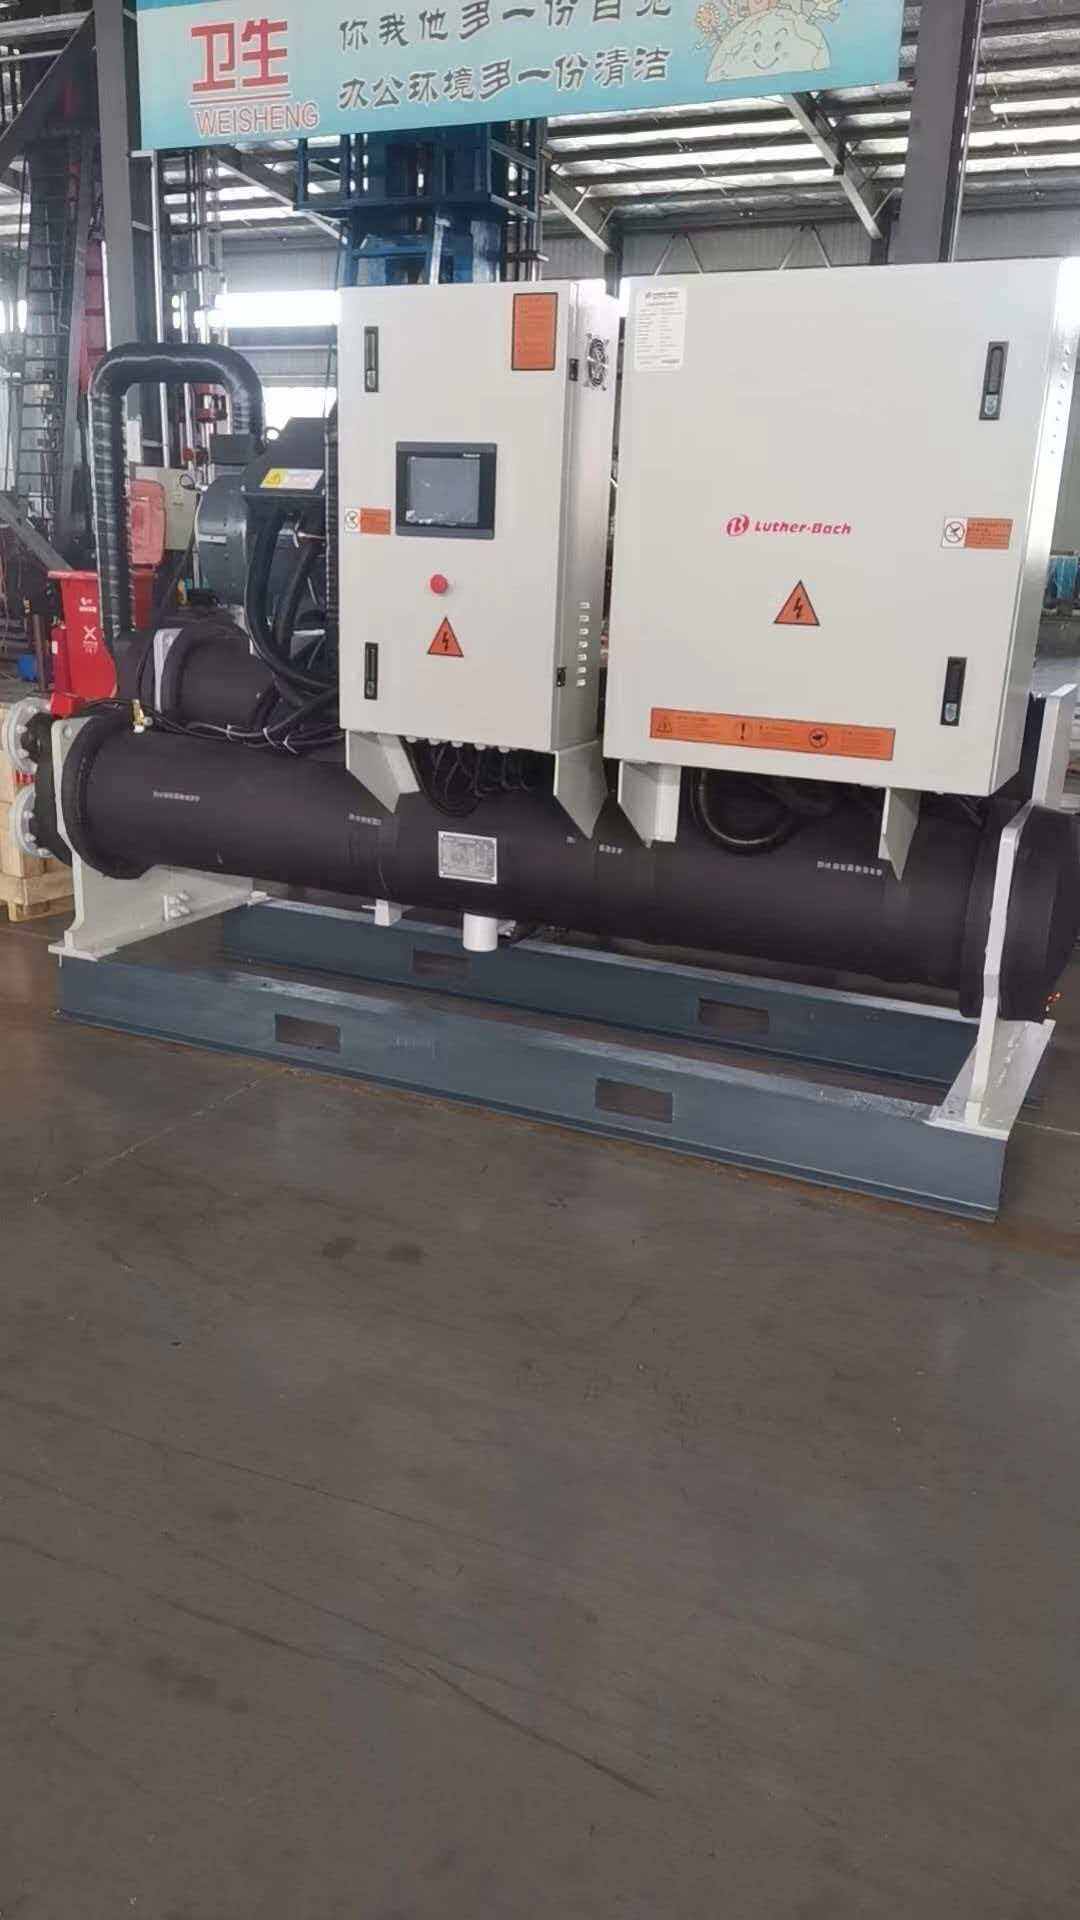
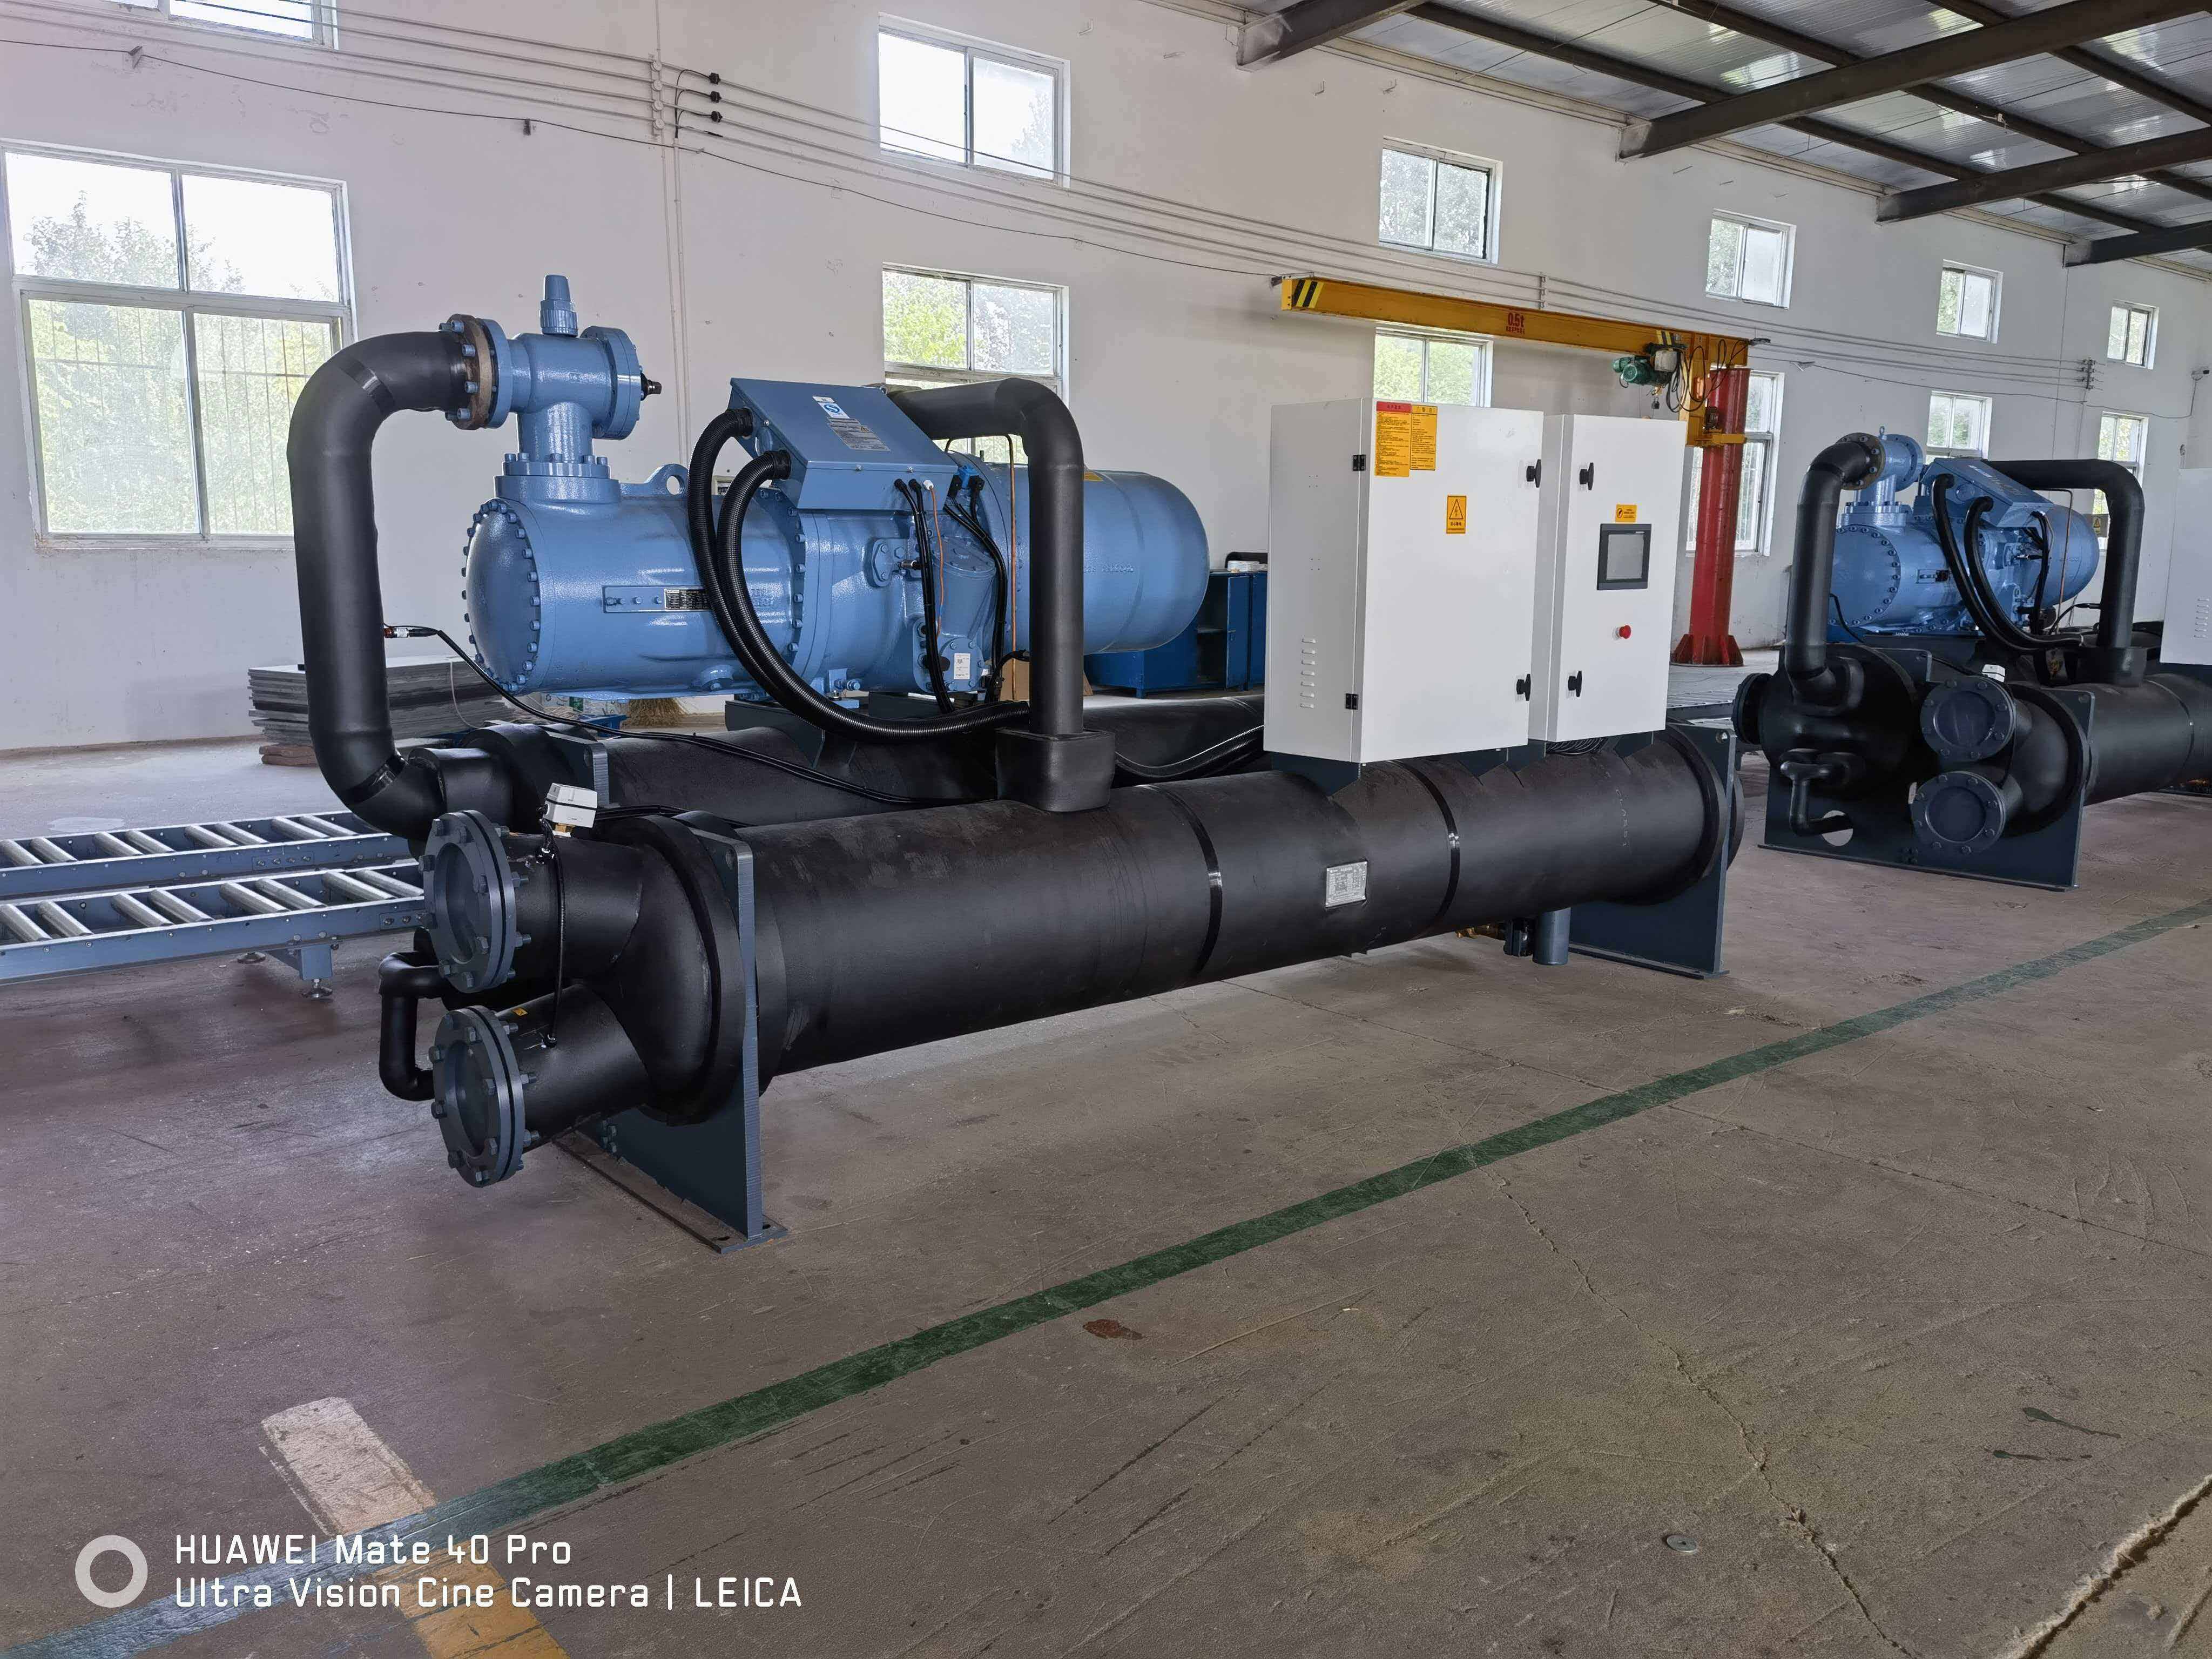
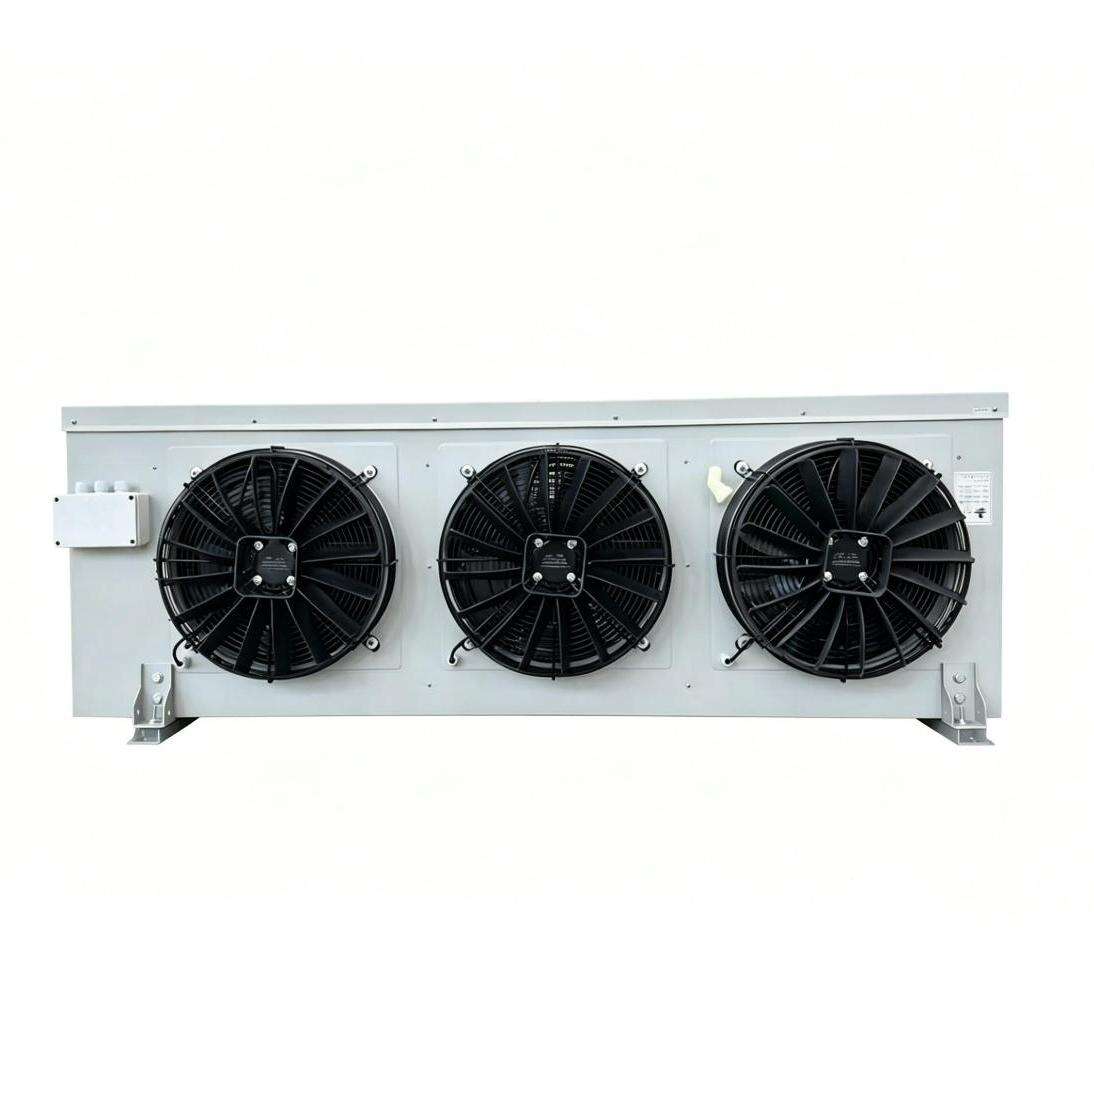
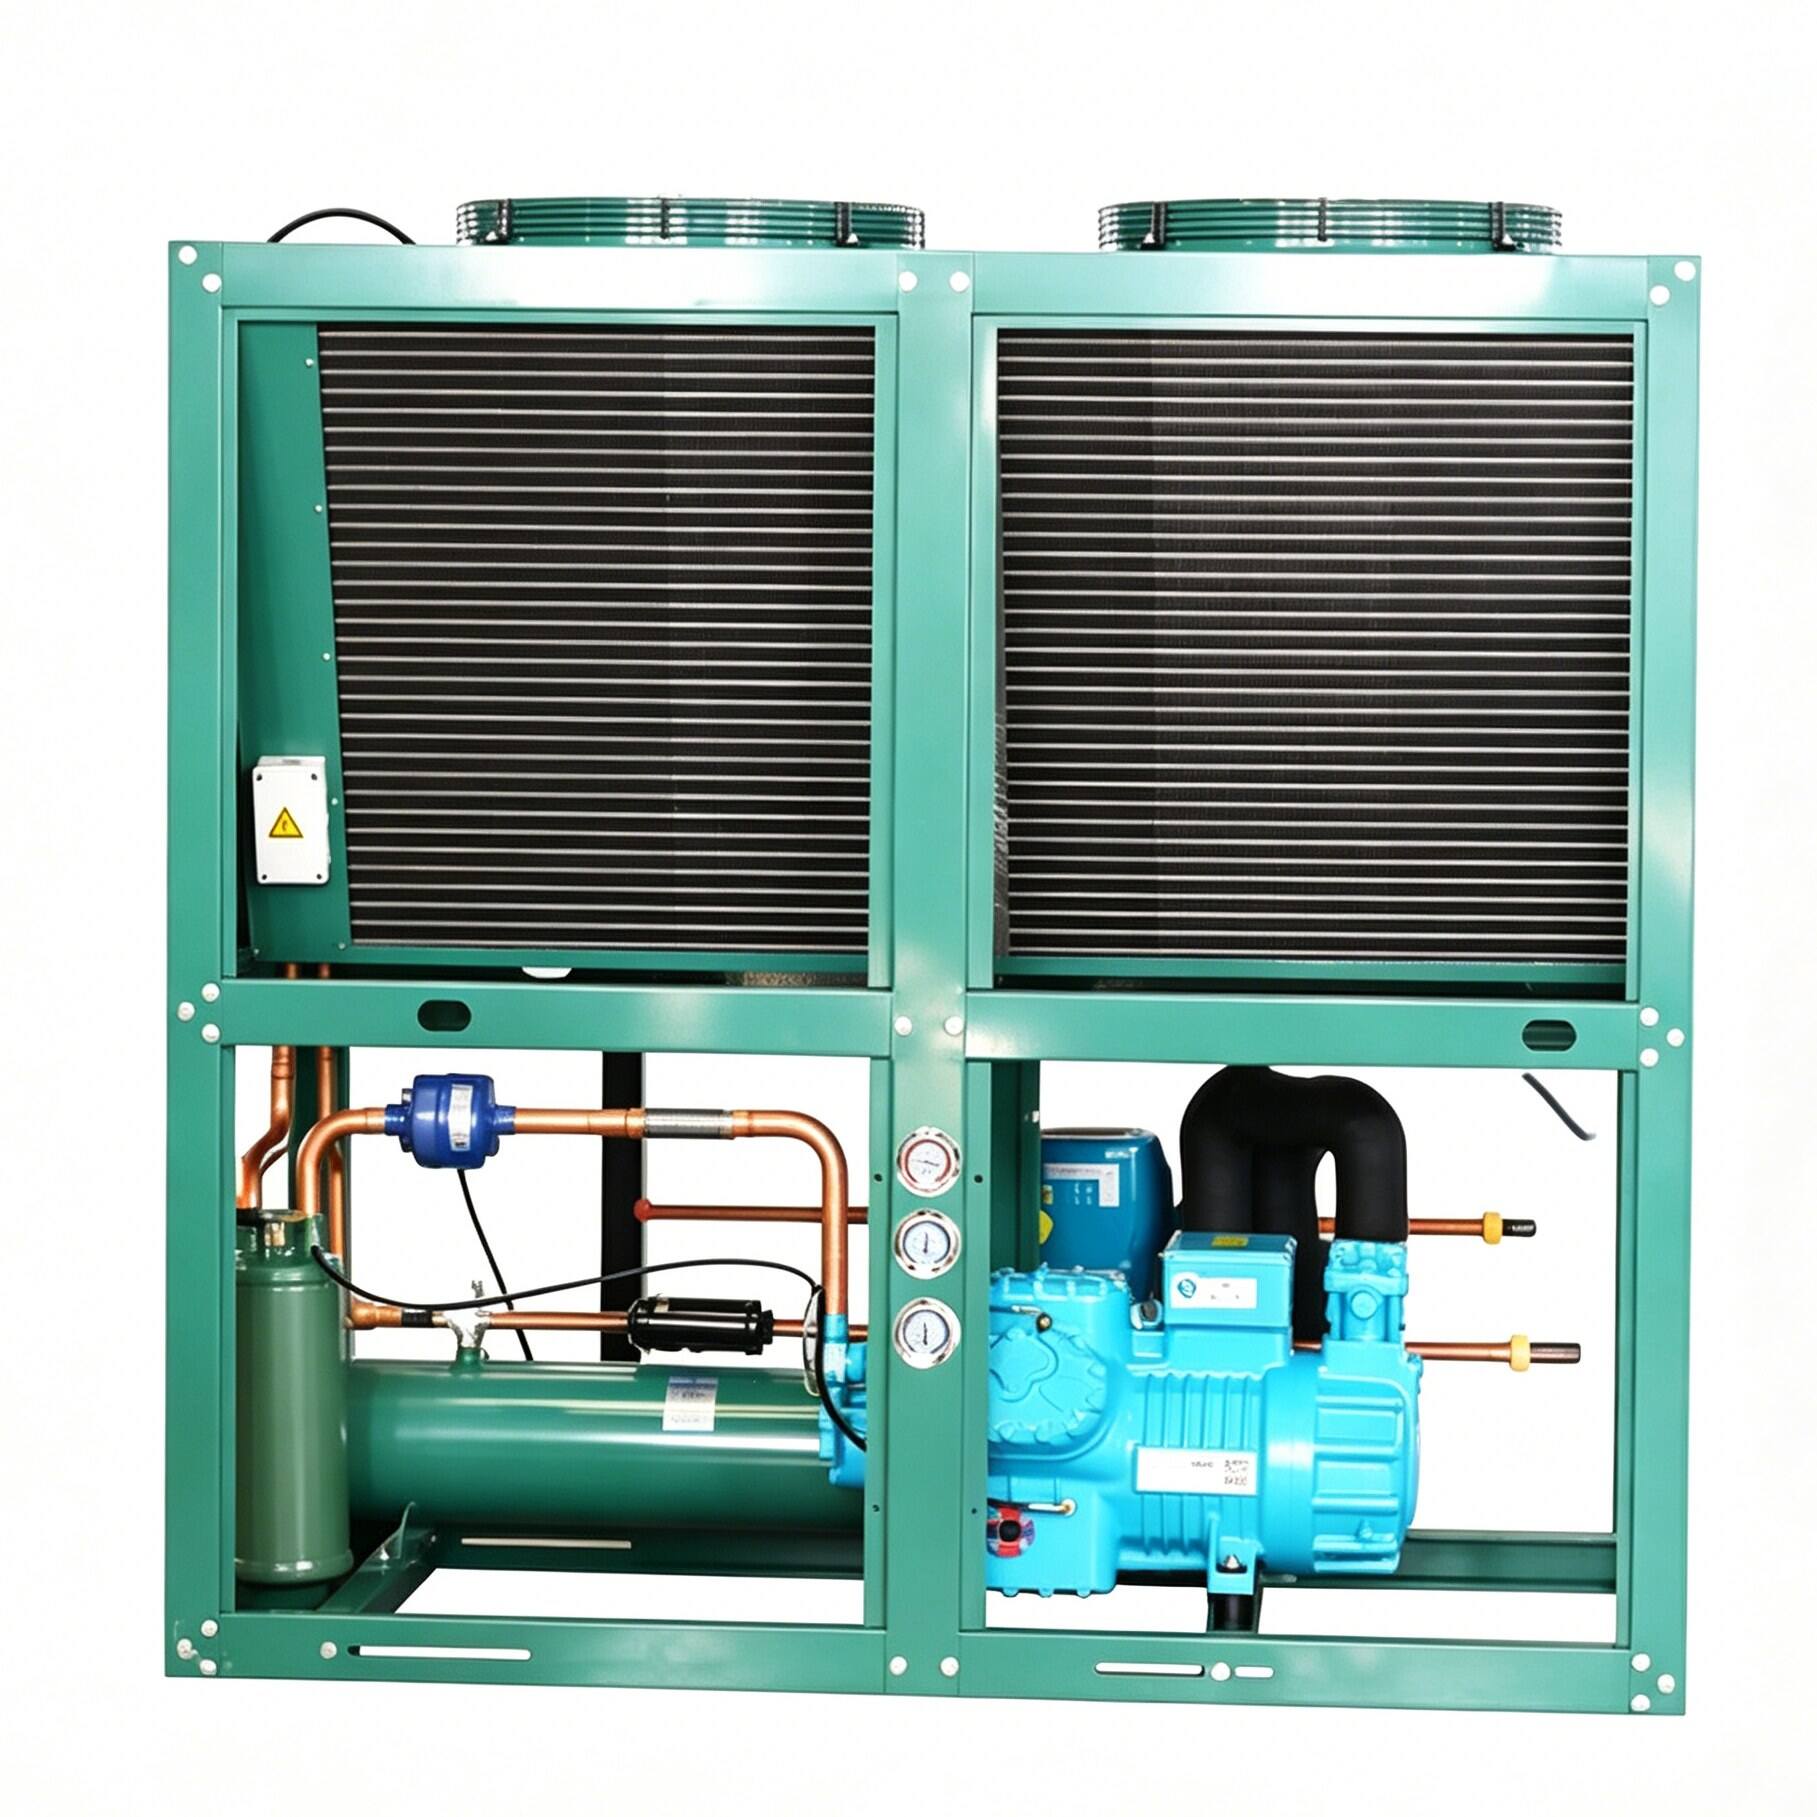
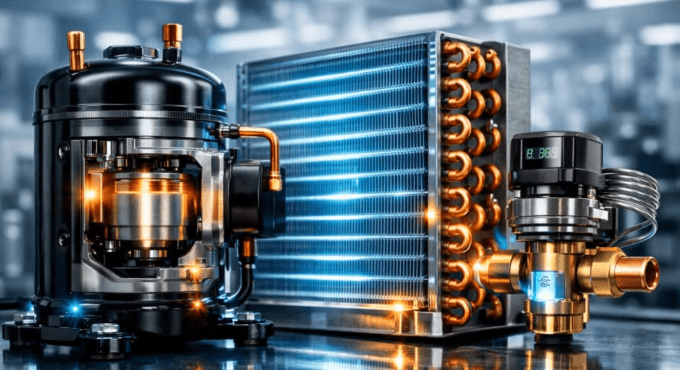
A water cooled condensing unit factory specializes in manufacturing advanced refrigeration equipment that uses water as the primary cooling medium to dissipate heat from refrigerant gases. These specialized manufacturing facilities produce condensing units integral to commercial refrigeration, industrial cooling systems, and HVAC applications. The main function of equipment from a water cooled condensing unit factory involves compressing refrigerant vapor, condensing it through water-cooled heat exchangers, and delivering high-pressure liquid refrigerant to evaporator systems. Modern factories incorporate cutting-edge production technologies including precision welding, automated assembly lines, computerized testing stations, and quality control systems that ensure every unit meets international standards. Technological features of products from a water cooled condensing unit factory include energy-efficient scroll or screw compressors, corrosion-resistant copper-nickel condenser coils, integrated water flow regulators, and smart control systems with remote monitoring capabilities. These units excel in applications where air cooling proves insufficient or impractical, such as food processing plants, pharmaceutical manufacturing, cold storage warehouses, chemical processing facilities, and large-scale commercial buildings. The factory environment emphasizes lean manufacturing principles, sustainable production methods, and continuous innovation to meet evolving market demands. Professional water cooled condensing unit factory operations maintain strict environmental controls, employ skilled technicians, and utilize premium-grade materials to produce reliable, long-lasting refrigeration solutions that deliver consistent performance across diverse industrial and commercial settings.
Popular Products

Choosing products from a professional water cooled condensing unit factory delivers substantial practical benefits for customers across multiple operational dimensions. First, these factories produce units with superior cooling efficiency compared to air-cooled alternatives, as water absorbs heat more effectively than air, resulting in lower energy consumption and reduced operational costs over the equipment lifecycle. Buyers gain immediate value through decreased electricity bills, often seeing energy savings of twenty to thirty percent in suitable applications. Second, equipment from an established water cooled condensing unit factory operates more quietly than air-cooled systems, eliminating outdoor noise pollution and making these units ideal for urban installations, noise-sensitive environments, and facilities with strict sound regulations. Third, the compact footprint of water-cooled units allows flexible installation in space-constrained locations where large air-cooled condensers cannot fit. Fourth, products from a quality-focused water cooled condensing unit factory demonstrate exceptional reliability in high ambient temperature conditions, maintaining consistent performance when air-cooled systems struggle during extreme weather. Fifth, these units require less frequent maintenance since water cooling prevents dust accumulation and reduces wear on mechanical components. Sixth, buyers benefit from customization options that reputable factories offer, including varied capacity ranges, voltage configurations, and specialized features tailored to specific industry requirements. Application suitability spans food service, healthcare, data centers, manufacturing, and process cooling where precision temperature control proves essential. Decision-useful context includes understanding that while initial investment may exceed air-cooled alternatives, total cost of ownership favors water-cooled systems in appropriate settings, particularly where cooling towers or city water connections already exist, making products from a water cooled condensing unit factory a smart long-term investment.

Latest News

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

28

Feb

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

View More
Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

28

Feb

Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

View More
Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

28

Feb

Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

water cooled condensing unit factory

Advanced Manufacturing Precision and Quality Assurance

Advanced Manufacturing Precision and Quality Assurance

A leading water cooled condensing unit factory distinguishes itself through rigorous manufacturing precision and comprehensive quality assurance protocols that guarantee product excellence. These facilities invest heavily in state-of-the-art production equipment including CNC machining centers for component fabrication, robotic welding systems that ensure consistent joint integrity, and automated leak detection stations that test every unit under extreme pressure conditions. The factory floor operates under ISO-certified quality management systems, with dedicated inspection teams monitoring critical parameters at each production stage. Every water-cooled condensing unit undergoes performance testing in specialized chambers that simulate real-world operating conditions, verifying cooling capacity, energy efficiency ratings, and noise levels before shipment. This meticulous approach eliminates defects, extends equipment lifespan, and provides customers with confidence that their investment will deliver reliable performance for years. Advanced factories also maintain material traceability systems, documenting component origins and manufacturing dates, which proves invaluable for maintenance planning and warranty administration. By prioritizing manufacturing excellence, a professional water cooled condensing unit factory ensures that customers receive equipment built to exacting standards, reducing downtime risks and maintenance expenses while maximizing operational productivity.
Customization Capabilities for Diverse Applications

Customization Capabilities for Diverse Applications

An experienced water cooled condensing unit factory offers extensive customization capabilities that address the unique requirements of different industries and applications. Unlike standardized production facilities, specialized factories employ engineering teams who collaborate with customers to modify unit specifications, including compressor types, condenser configurations, control system integration, and physical dimensions. This flexibility proves essential for businesses with non-standard cooling loads, unusual installation constraints, or specific regulatory compliance needs. For example, pharmaceutical manufacturers may require units with stainless steel construction and validated temperature stability, while food processors need equipment certified for sanitary environments with easy-clean surfaces. A capable water cooled condensing unit factory maintains relationships with component suppliers worldwide, enabling access to premium compressors, specialized refrigerants, and advanced control technologies. The customization process typically includes detailed consultation, engineering drawings for approval, prototype testing when needed, and thorough documentation of modifications. This personalized approach ensures that customers receive equipment perfectly matched to their operational requirements rather than compromising with off-the-shelf solutions. Additionally, factories offering customization services provide superior technical support, as their teams possess deep understanding of how modifications affect performance, making troubleshooting and future upgrades more efficient and cost-effective for customers.
Environmental Sustainability and Energy Efficiency Focus

Environmental Sustainability and Energy Efficiency Focus

Modern water cooled condensing unit factory operations prioritize environmental sustainability and energy efficiency throughout the manufacturing process and in final product performance. Leading factories implement green manufacturing practices including waste heat recovery systems, water recycling programs, and renewable energy utilization to minimize their environmental footprint. More importantly, the equipment these factories produce incorporates the latest energy-saving technologies such as variable-speed compressors that adjust output to match cooling demand, high-efficiency heat exchangers with enhanced surface geometries, and intelligent control systems that optimize operation based on real-time conditions. Products from an environmentally conscious water cooled condensing unit factory typically utilize low-global-warming-potential refrigerants that comply with international environmental regulations while maintaining excellent thermodynamic properties. Energy efficiency translates directly into customer benefits through reduced operating costs, lower carbon emissions, and eligibility for green building certifications and energy rebate programs. Many factories now offer units with integrated heat recovery options, allowing customers to capture waste heat for space heating or process applications, further improving overall system efficiency. By choosing equipment from a water cooled condensing unit factory committed to sustainability, customers align their operations with environmental responsibility goals while enjoying superior performance and economic advantages that energy-efficient refrigeration systems provide.
Water Cooled Condensing Unit Factory Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
Water Cooled Condensing Unit Factory Solutions

Copyright © 2026 Ningbo Lucky Star Import & Export Co., Ltd. All rights reserved.  -  Privacy policy