Commercial Kitchen Freezer Solutions

All Categories

commercial kitchen freezer

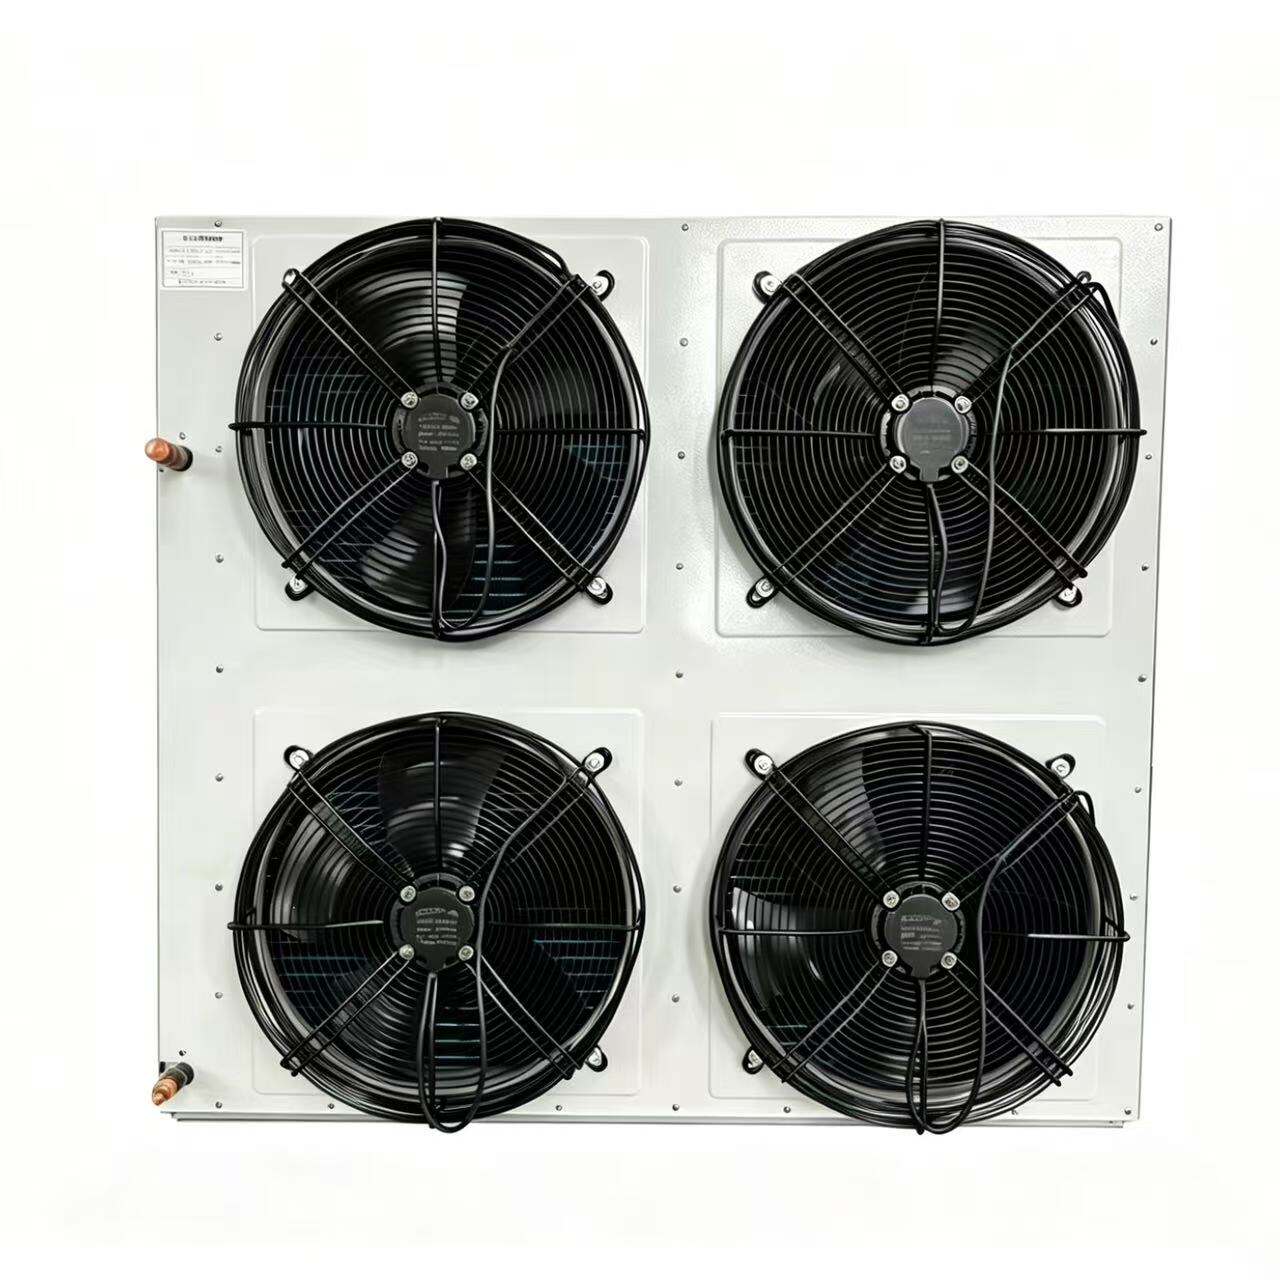
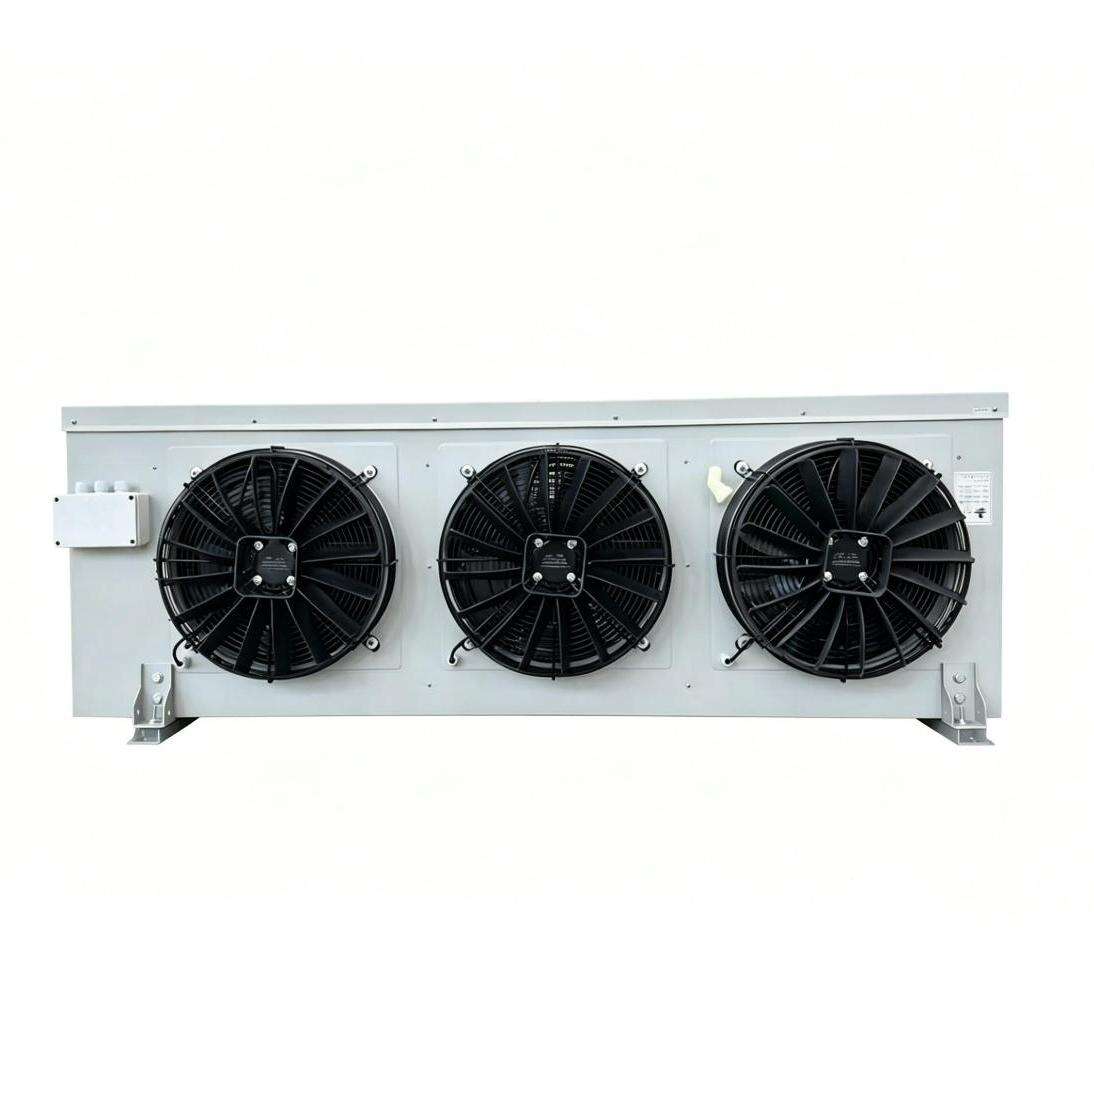
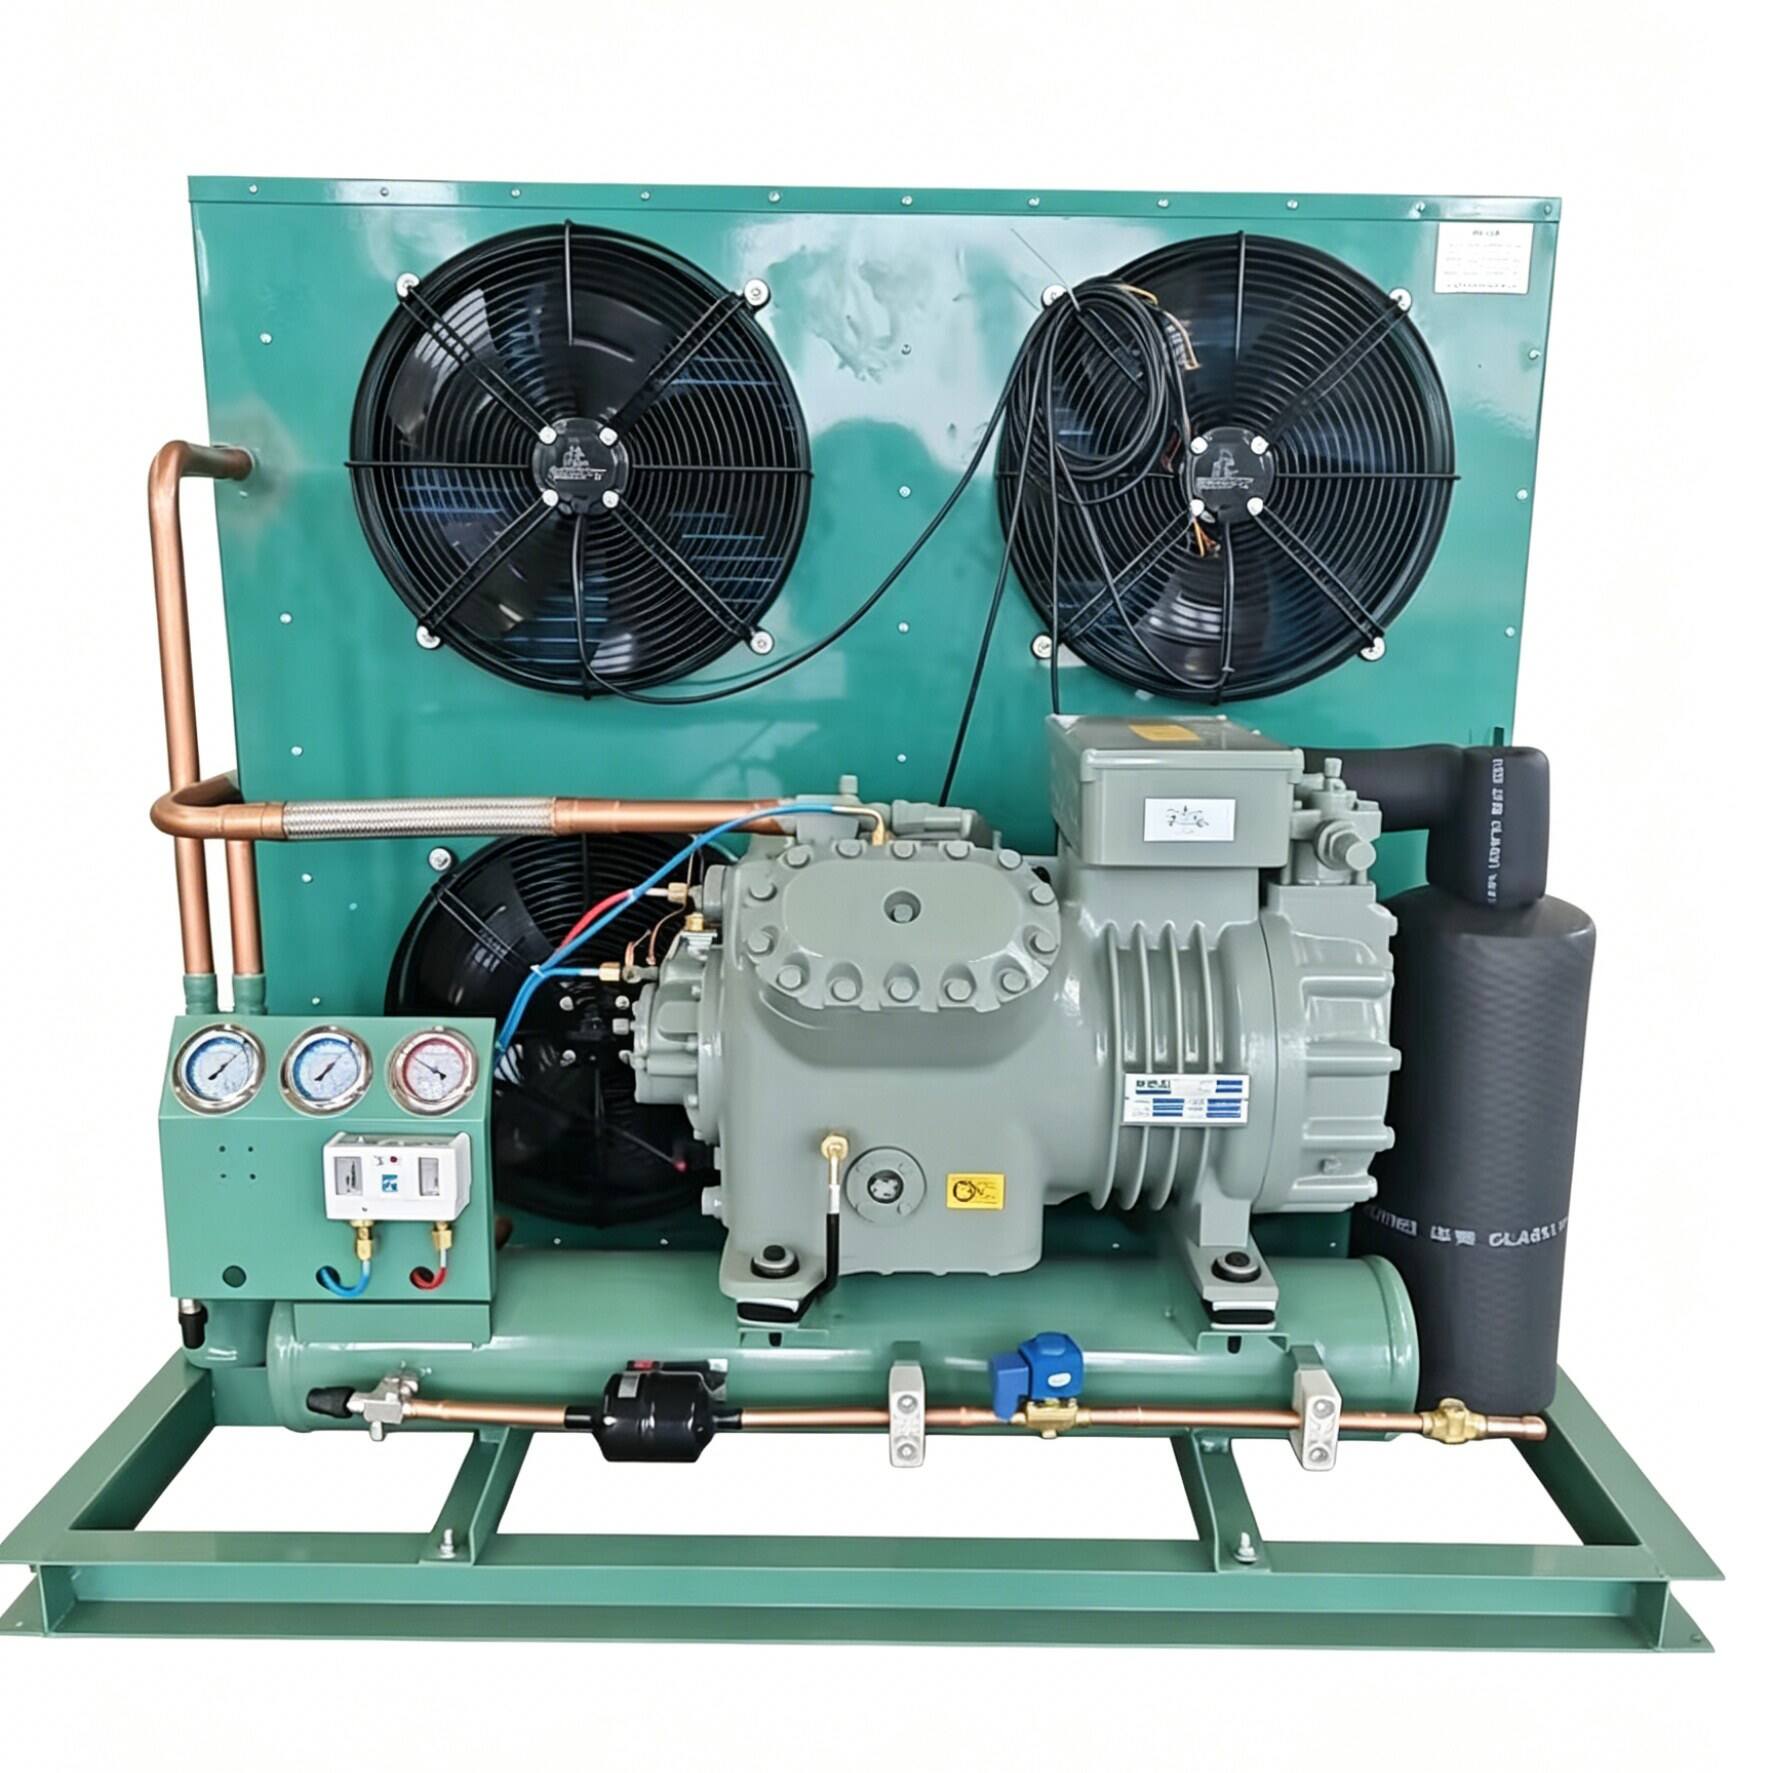
A commercial kitchen freezer is an essential piece of refrigeration equipment designed specifically for foodservice operations, restaurants, catering businesses, and hospitality establishments. This robust appliance provides reliable frozen storage for ingredients, prepared meals, and perishable goods at temperatures typically ranging from -10°F to 0°F. Commercial kitchen freezers are built with industrial-grade components to withstand the demanding conditions of busy kitchen environments, offering superior performance compared to residential models. These units come in various configurations including reach-in freezers, walk-in freezers, undercounter models, and chest freezers, each tailored to different space requirements and operational needs. The technological features of a commercial kitchen freezer include advanced refrigeration systems with powerful compressors, efficient insulation materials, and precise temperature controls that maintain consistent freezing conditions. Many models incorporate digital temperature displays, automatic defrost cycles, and alarm systems to alert staff of temperature fluctuations. The construction typically features stainless steel exteriors for durability and easy cleaning, along with self-closing doors and heavy-duty hinges. Applications span across all foodservice sectors, from fast-food chains storing frozen proteins and vegetables to bakeries preserving dough and desserts. Healthcare facilities, schools, and institutional kitchens rely on commercial kitchen freezers for bulk food storage and meal preparation planning, making them indispensable for any operation requiring dependable frozen food preservation at scale.
New Products

Investing in a commercial kitchen freezer delivers substantial value through extended food preservation that minimizes waste and reduces purchasing costs. By maintaining optimal freezing temperatures, these units keep ingredients fresh for months, allowing businesses to buy in bulk and take advantage of wholesale pricing while ensuring food safety compliance. The energy-efficient design of modern commercial kitchen freezers translates to lower utility bills despite continuous operation, with improved insulation and eco-friendly refrigerants delivering sustainable performance. Operational benefits include faster temperature recovery after door openings, ensuring stored products remain frozen even during peak service hours when staff frequently access inventory. The spacious interior organization with adjustable shelving maximizes storage capacity, enabling efficient inventory management and quick product retrieval that speeds up kitchen workflows. Commercial kitchen freezers are built for durability, featuring heavy-duty construction that withstands constant use in demanding environments, resulting in longer equipment lifespan and reduced replacement costs. These freezers accommodate diverse applications, from storing raw proteins and seafood to preserving prepared dishes and frozen desserts, making them suitable for restaurants, catering operations, grocery stores, and institutional kitchens. The precise temperature consistency prevents freezer burn and maintains product quality, protecting your investment in premium ingredients. Easy-to-clean surfaces and removable components simplify sanitation procedures, helping establishments meet health department standards. The reliable performance of a commercial kitchen freezer provides peace of mind, knowing that inventory remains safely frozen overnight and during weekends, eliminating concerns about spoilage. For decision-making purposes, these freezers offer flexible sizing options that fit various kitchen layouts, from compact undercounter units for limited spaces to expansive walk-in models for high-volume operations, ensuring every business finds the perfect match for their storage requirements.

Practical Tips

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

28

Feb

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

View More
Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

28

Feb

Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

View More
Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

28

Feb

Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

commercial kitchen freezer

Advanced Temperature Management Technology

Advanced Temperature Management Technology

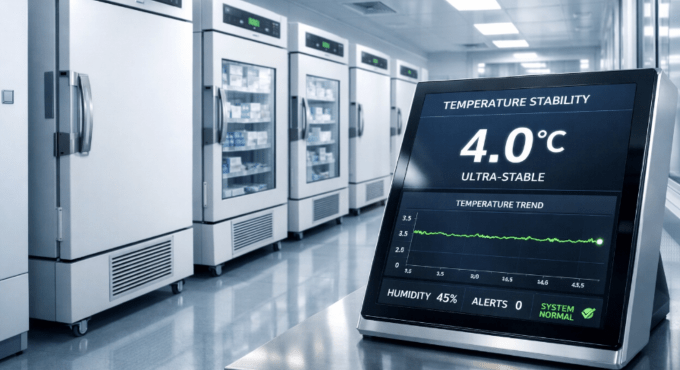
Modern commercial kitchen freezers incorporate sophisticated temperature management systems that ensure consistent freezing performance throughout the entire storage compartment. These units feature microprocessor-controlled thermostats that monitor internal conditions continuously, making automatic adjustments to maintain the ideal temperature range regardless of external factors or door openings. The advanced refrigeration technology includes powerful compressors paired with optimized evaporator coils that provide rapid cooldown and quick temperature recovery, essential for busy kitchen operations where staff frequently access frozen inventory. Digital displays offer real-time temperature readings, allowing managers to verify proper operation at a glance and maintain detailed logs for food safety compliance. Many commercial kitchen freezer models include built-in alarm systems that immediately alert staff to temperature deviations, power failures, or door-ajar situations, preventing potential product loss before it occurs. This proactive monitoring protects valuable inventory and ensures regulatory compliance. The intelligent defrost cycles automatically activate during low-usage periods, preventing ice buildup without disrupting operations or compromising product quality. This advanced temperature management technology ultimately delivers superior product preservation, operational reliability, and the confidence that frozen goods remain in optimal condition around the clock.
Exceptional Storage Capacity and Organization

Exceptional Storage Capacity and Organization

A commercial kitchen freezer maximizes usable storage space through intelligent interior design that accommodates high-volume inventory requirements. The thoughtfully engineered shelving systems feature heavy-duty coated wire or solid shelves that support substantial weight while allowing proper air circulation around stored products, ensuring uniform freezing throughout the compartment. Adjustable shelf configurations enable customization based on specific inventory needs, whether storing large bulk containers, sheet pans, or smaller packaged items. The vertical storage optimization makes efficient use of available floor space, particularly valuable in commercial kitchens where square footage comes at a premium. Many models include door shelving and compartments that provide additional storage for frequently accessed items, improving workflow efficiency during service periods. The spacious interior allows organized inventory rotation following first-in-first-out protocols, reducing waste and ensuring product freshness. Commercial kitchen freezers designed for specific applications, such as pizza preparation or bakery operations, offer specialized storage solutions with features like tray slides or pan racks. The generous capacity reduces the need for multiple units, consolidating frozen storage into a single reliable appliance that simplifies inventory management. This exceptional storage capability combined with smart organization features helps foodservice operations maintain comprehensive frozen inventories while keeping products easily accessible and properly arranged for efficient kitchen operations.
Durable Construction for Demanding Environments

Durable Construction for Demanding Environments

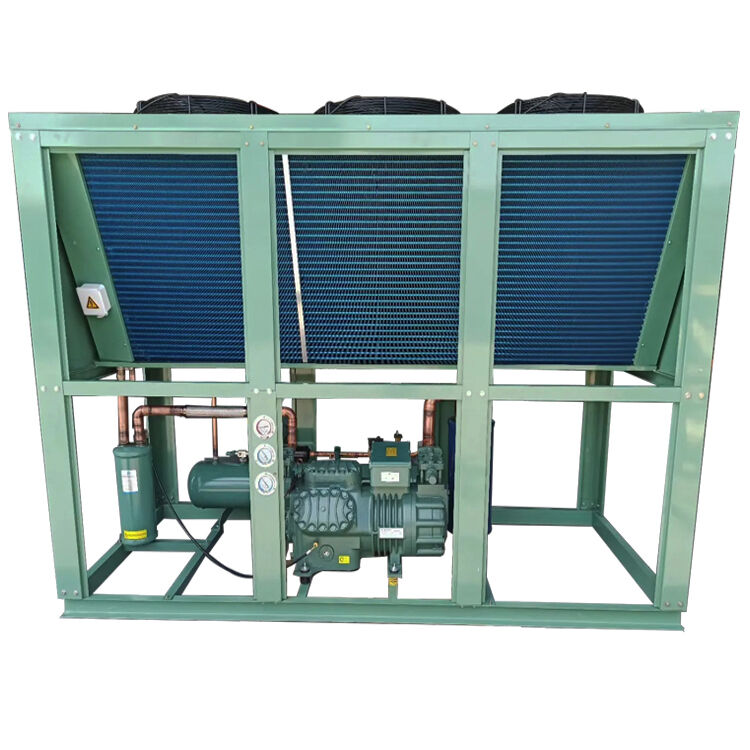
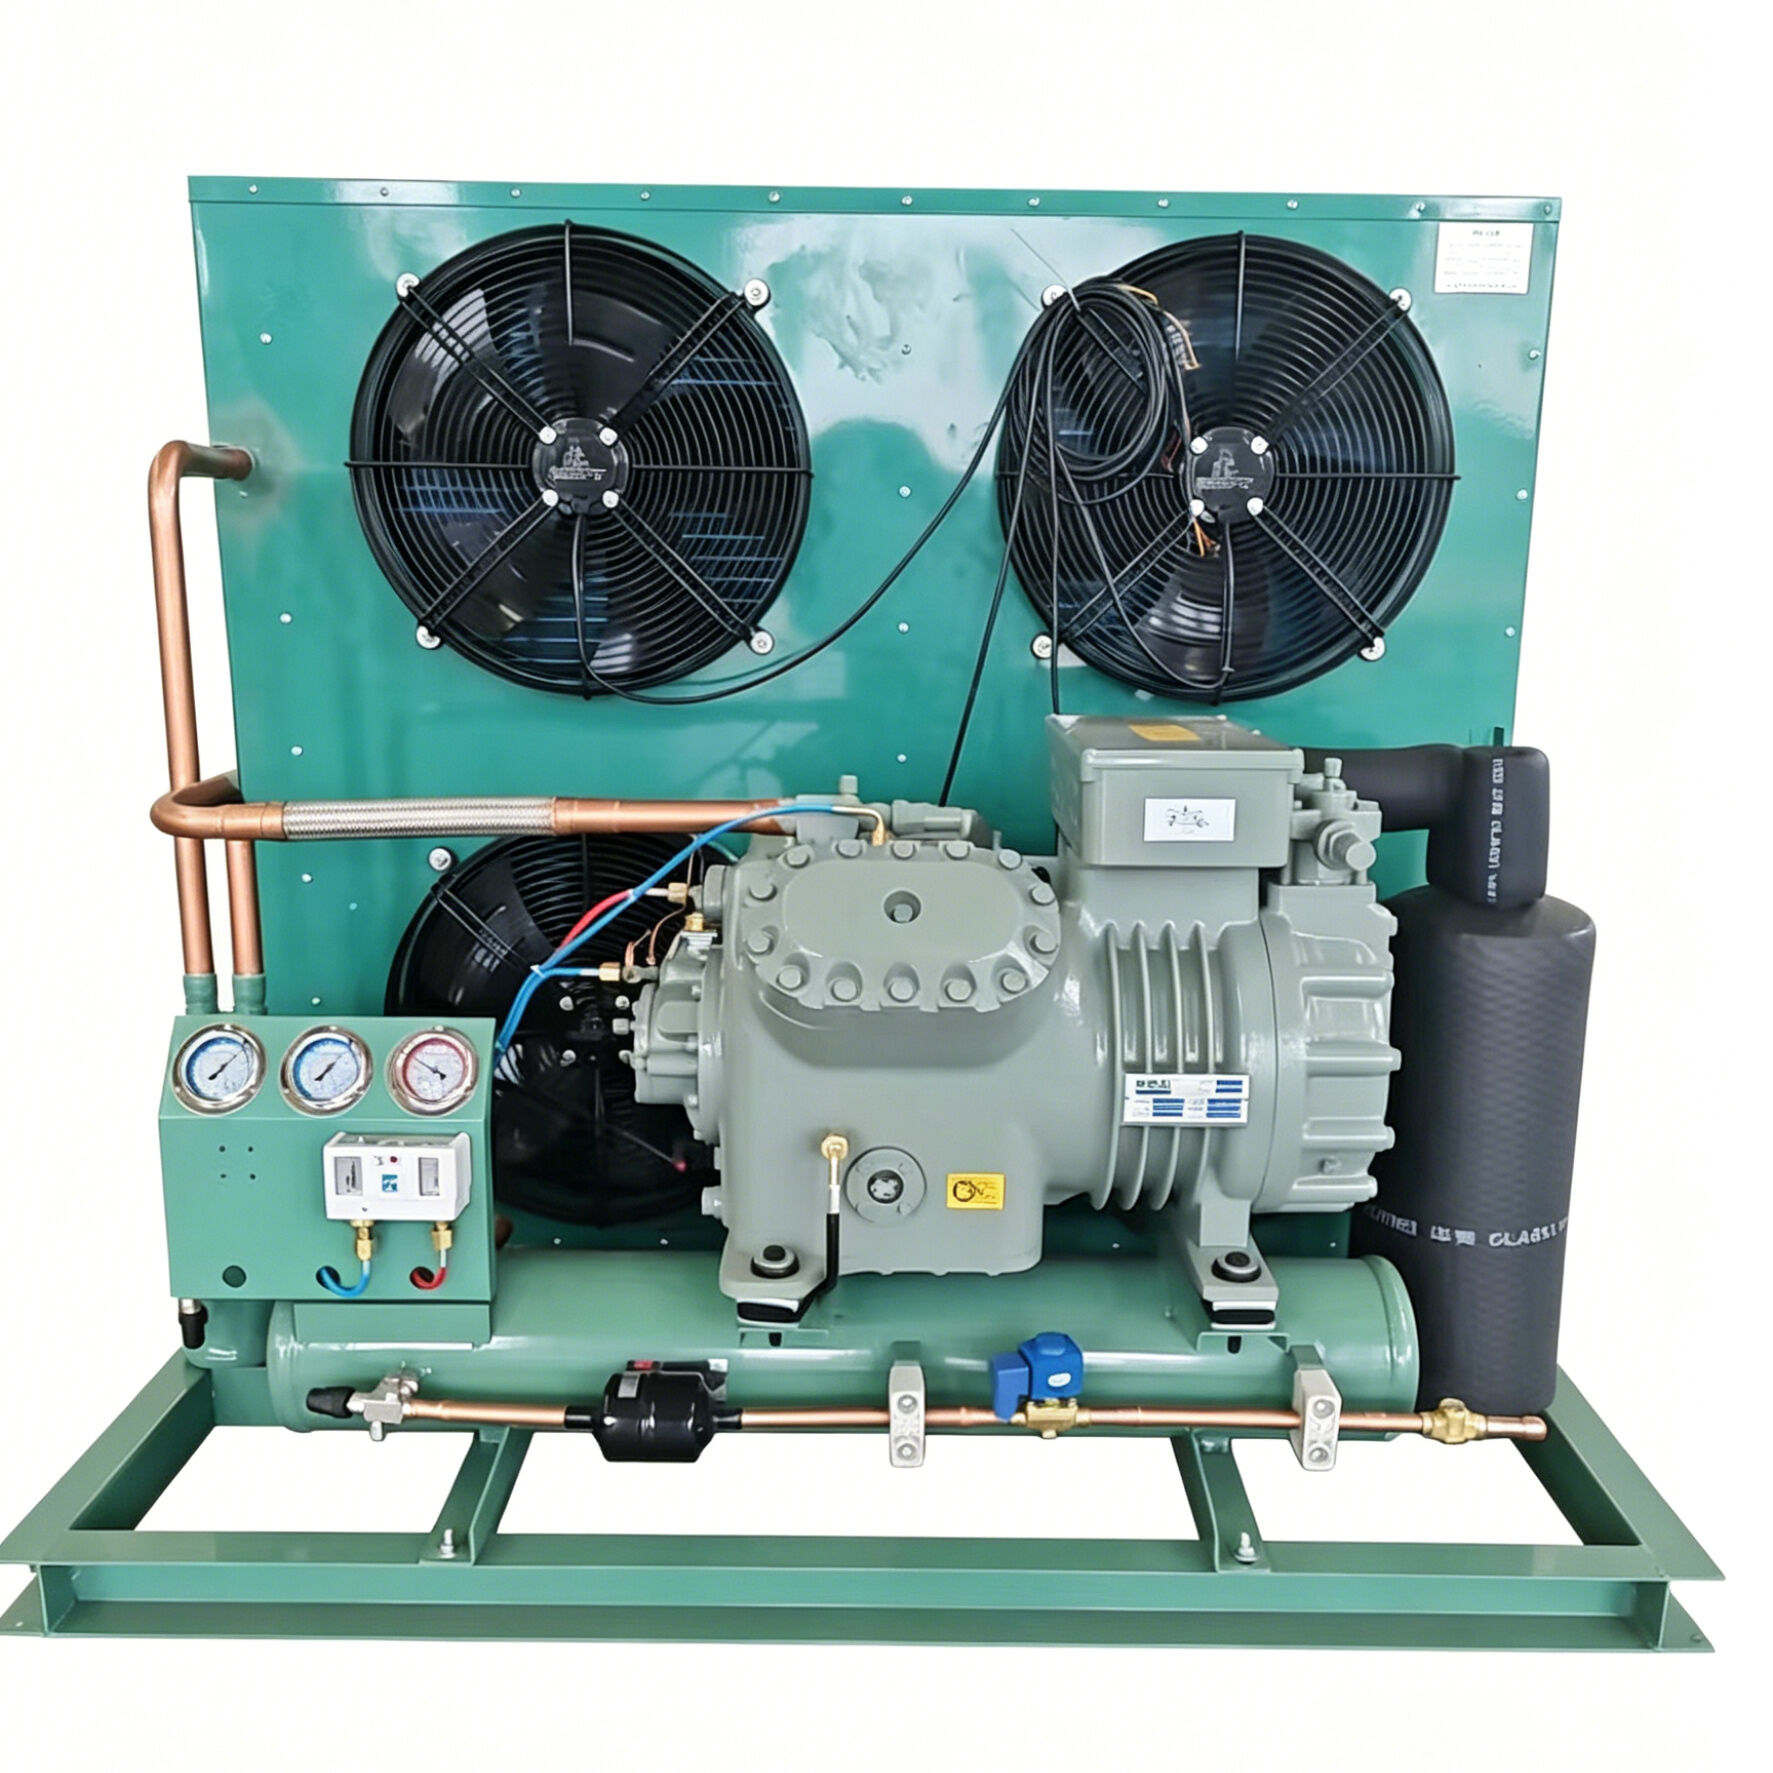
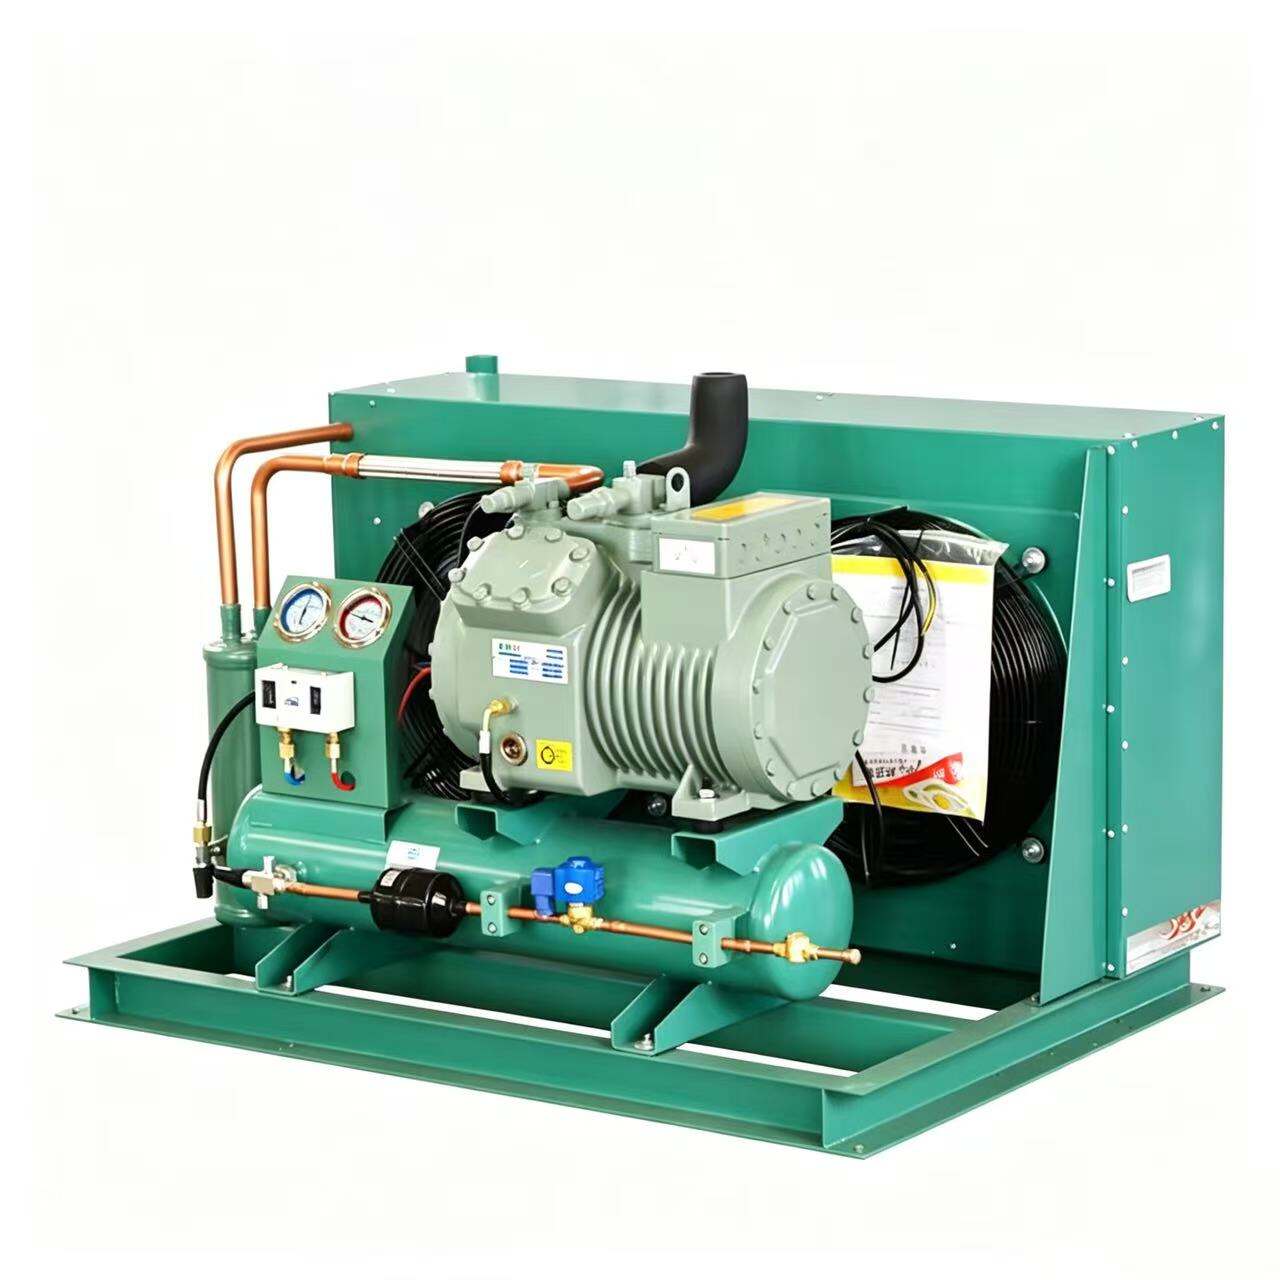
Commercial kitchen freezers are engineered with industrial-grade materials and construction methods that ensure longevity in the harsh conditions of professional foodservice environments. The exterior typically features corrosion-resistant stainless steel that withstands repeated cleaning with commercial sanitizers, maintains an attractive appearance, and resists dents and scratches from daily kitchen activities. Heavy-duty insulation, often several inches thick with high-density foam, provides exceptional thermal retention that reduces energy consumption while maintaining stable internal temperatures. The robust door systems incorporate commercial-grade hinges designed for thousands of opening cycles, self-closing mechanisms that prevent accidental temperature loss, and magnetic or cam-lift gaskets that create airtight seals to maximize efficiency. The reinforced floor construction in walk-in commercial kitchen freezer models supports heavy traffic and loaded carts without damage. Internally, the units feature corrosion-resistant aluminum or stainless steel liners that facilitate cleaning and resist bacterial growth, contributing to food safety. The commercial-grade refrigeration components, including hermetically sealed compressors and oversized condensers, deliver reliable performance year after year with minimal maintenance requirements. This durable construction represents a long-term investment that reduces total cost of ownership through extended equipment life, fewer repairs, and consistent performance that keeps operations running smoothly regardless of daily demands placed on the unit.
Commercial Kitchen Freezer Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
Commercial Kitchen Freezer Solutions

Copyright © 2026 Ningbo Lucky Star Import & Export Co., Ltd. All rights reserved.  -  Privacy policy