Industrial Cold Room Solutions & Benefits

All Categories

industrial cold room

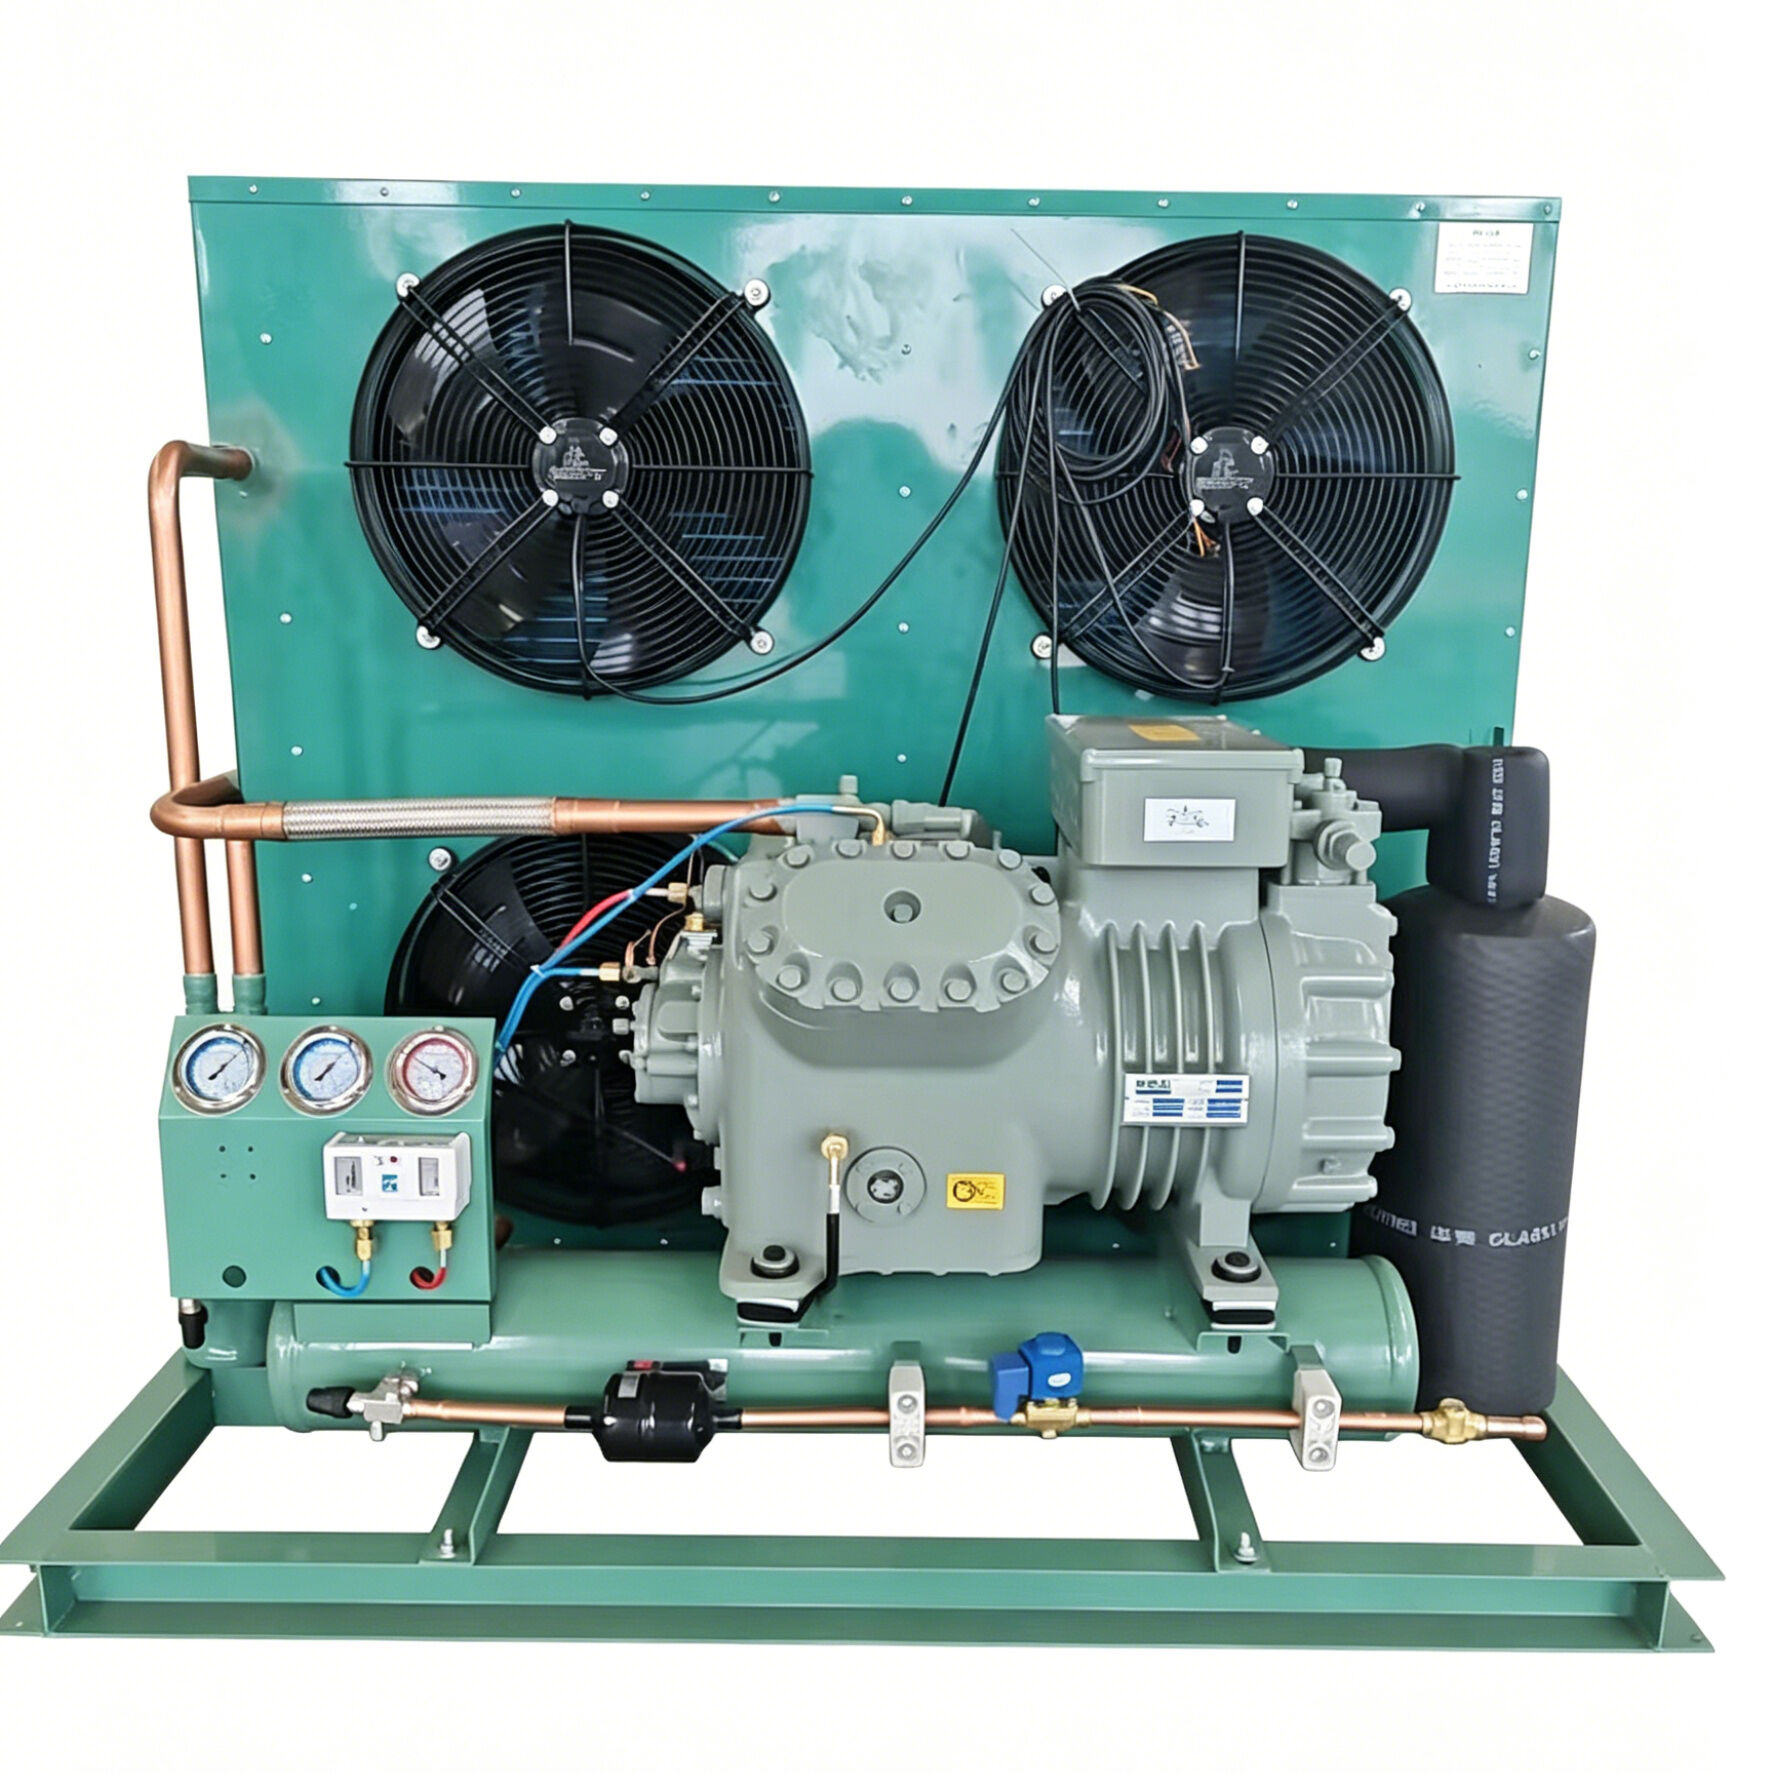
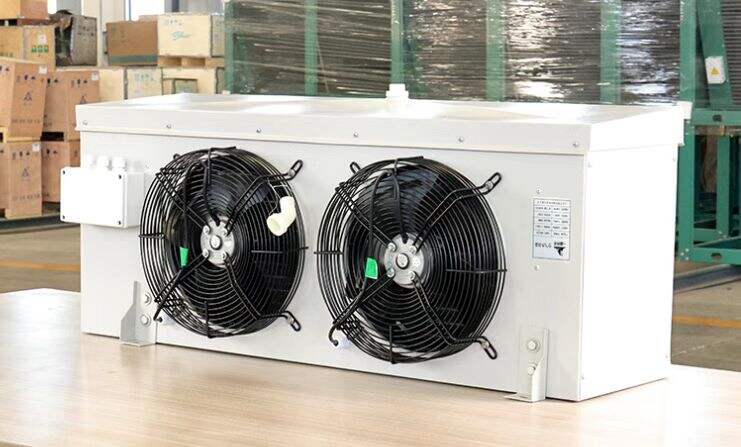
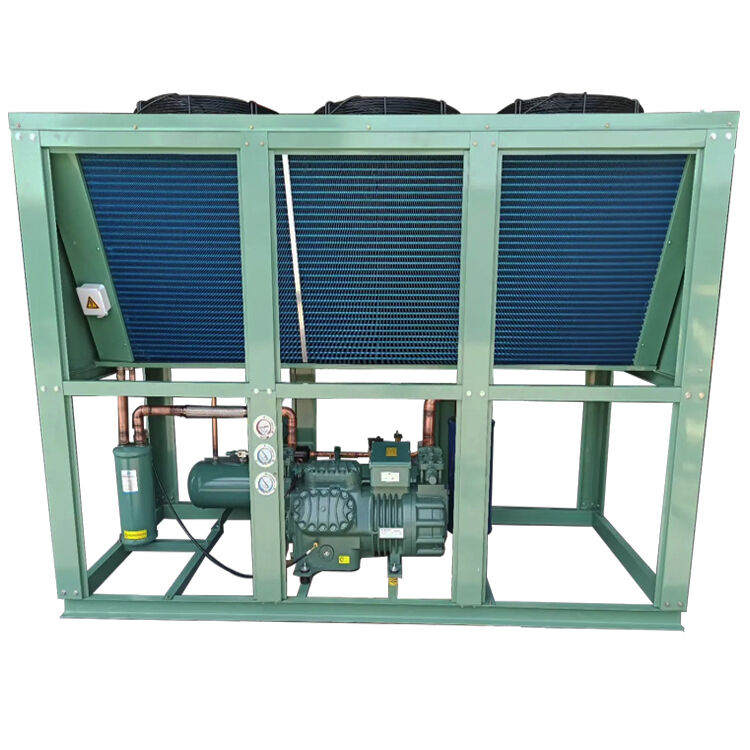
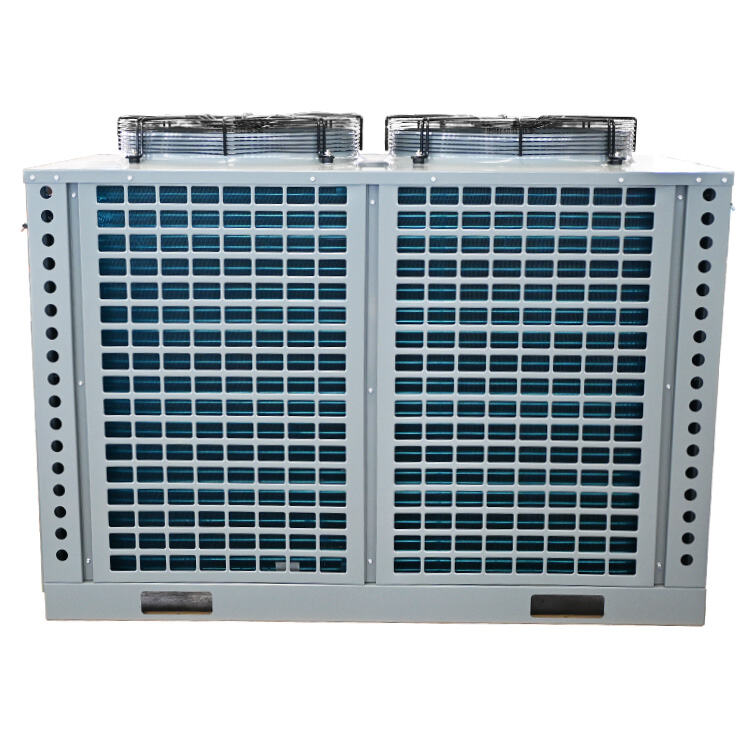
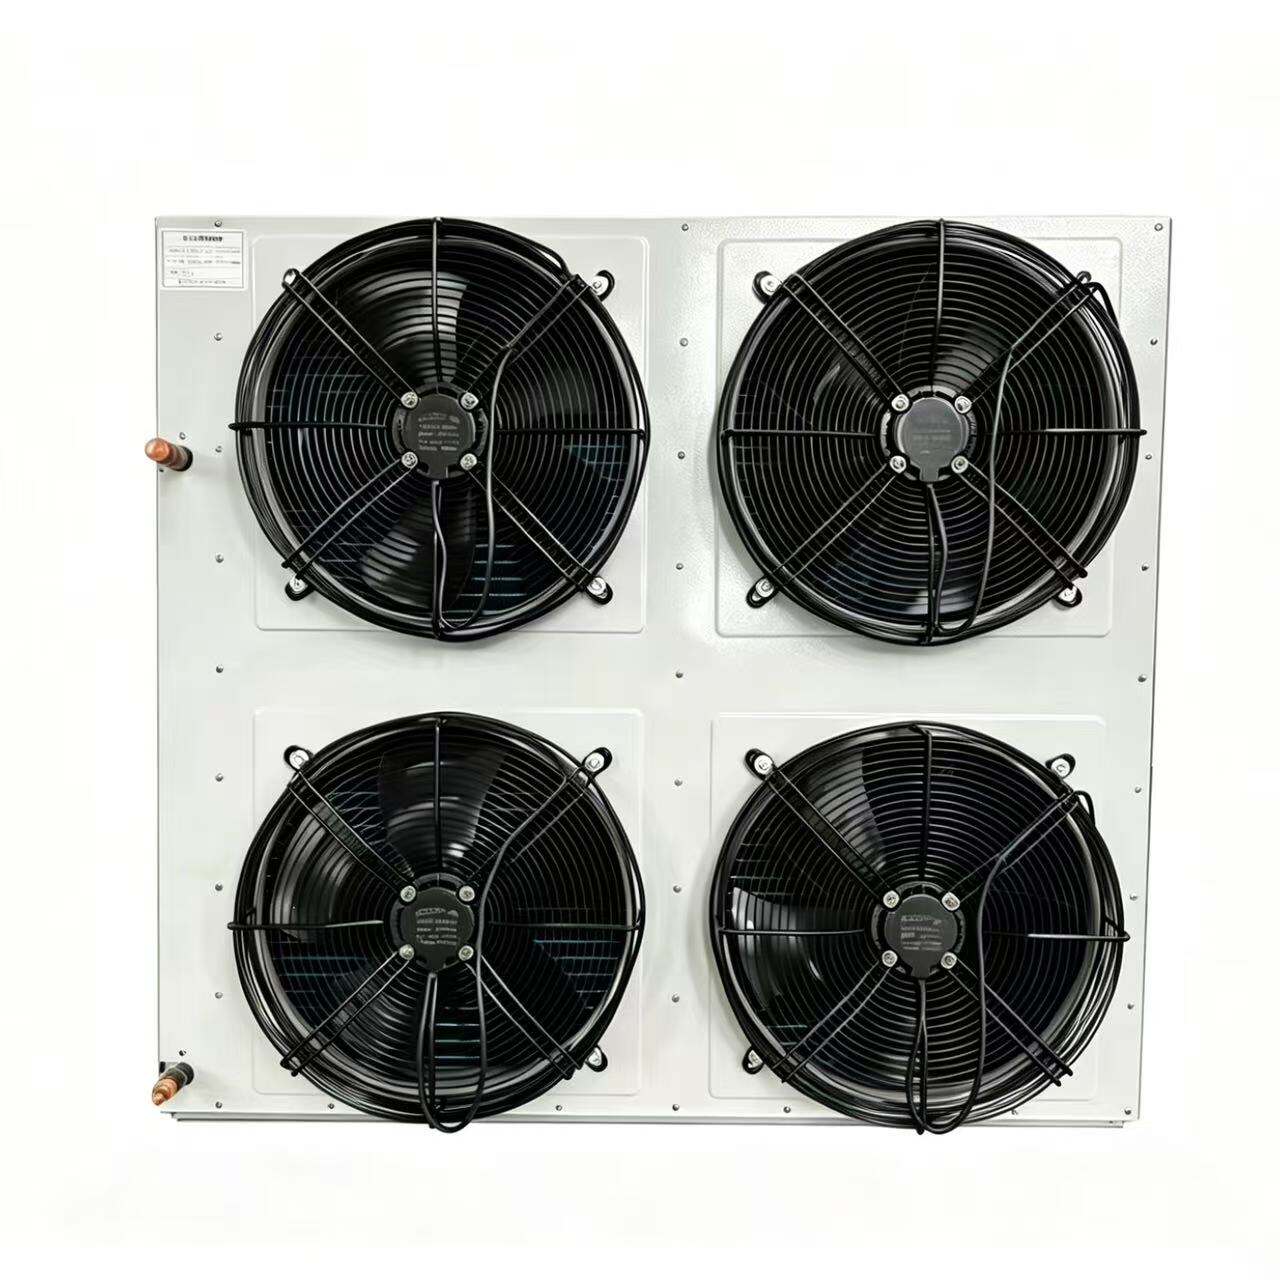
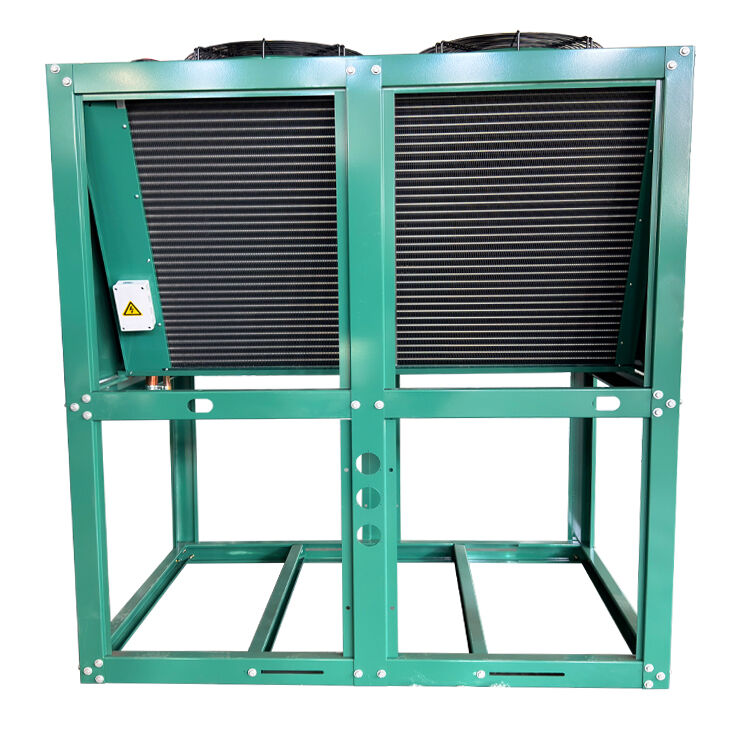
An industrial cold room is a large-scale refrigerated storage facility designed to maintain consistently low temperatures for preserving perishable goods, raw materials, and temperature-sensitive products. These specialized chambers utilize advanced cooling systems, insulated panels, and precise temperature controls to create optimal storage environments across various industries. The industrial cold room serves as a critical infrastructure component for businesses requiring reliable cold chain management, from food processing plants to pharmaceutical manufacturers. The main function revolves around preserving product quality, extending shelf life, and preventing spoilage through controlled refrigeration. Technological features include high-density polyurethane or polystyrene insulation panels, industrial-grade refrigeration units, automated temperature monitoring systems, and energy-efficient compressors. Many modern installations incorporate smart sensors, humidity controls, and backup power systems to ensure uninterrupted operation. Applications span multiple sectors including food and beverage storage, meat processing facilities, dairy production, seafood preservation, pharmaceutical storage, chemical manufacturing, and agricultural product handling. The industrial cold room can be customized in various sizes, from small walk-in units to massive warehouse-scale installations covering thousands of square feet. Temperature ranges vary based on application requirements, with some units maintaining temperatures between zero to five degrees Celsius for general refrigeration, while others achieve minus eighteen to minus twenty-five degrees Celsius for frozen storage. This versatility makes the industrial cold room an indispensable asset for businesses prioritizing product integrity and regulatory compliance.
New Product Recommendations

Investing in an industrial cold room delivers substantial operational benefits that directly impact your bottom line. Temperature precision ensures products maintain their quality specifications throughout storage, reducing waste from spoilage and extending usable inventory lifecycles. This translates to measurable cost savings as you minimize product losses and maximize sellable inventory. Energy efficiency represents another practical advantage, with modern systems consuming significantly less power than older refrigeration methods while delivering superior performance. The insulated construction retains cold air effectively, reducing the workload on compressors and lowering monthly utility expenses. Businesses report energy cost reductions of twenty to thirty percent compared to conventional cooling solutions. Scalability offers flexibility as your operations grow, allowing you to expand storage capacity without rebuilding entire facilities. Modular panel construction enables straightforward expansion projects that accommodate increasing inventory demands. The industrial cold room adapts to diverse product requirements, supporting multiple temperature zones within a single facility for storing different product categories simultaneously. This versatility eliminates the need for separate storage buildings, optimizing facility footprint and reducing real estate costs. Compliance assurance provides peace of mind, as properly maintained units help meet food safety regulations, pharmaceutical storage standards, and industry-specific quality requirements. Documentation capabilities through automated monitoring systems create audit trails that satisfy regulatory inspections. Durability ensures long-term value, with quality installations operating reliably for fifteen to twenty years with proper maintenance. The robust construction withstands demanding industrial environments, heavy traffic, and frequent door access without compromising temperature stability. Return on investment typically occurs within three to five years through combined savings from reduced spoilage, lower energy costs, and improved operational efficiency. These practical advantages make the industrial cold room a strategic investment for businesses committed to quality preservation and sustainable growth.

Practical Tips

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

28

Feb

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

View More
Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

28

Feb

Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

View More
Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

28

Feb

Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

industrial cold room

Advanced Temperature Control Technology

Advanced Temperature Control Technology

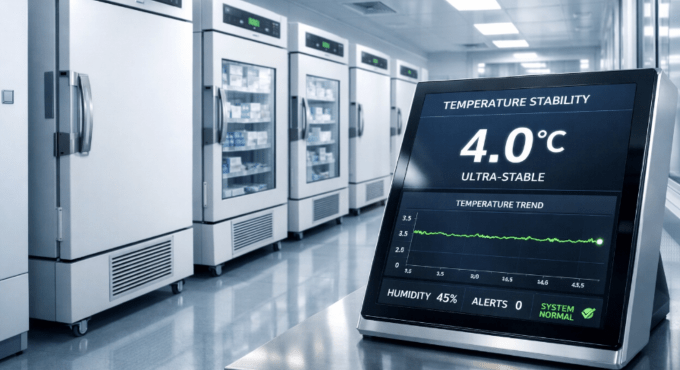
The industrial cold room incorporates sophisticated temperature management systems that maintain precise environmental conditions regardless of external weather fluctuations or internal loading patterns. Digital controllers continuously monitor chamber temperatures with accuracy within half a degree, automatically adjusting compressor operation to compensate for any deviations. This precision proves essential for products requiring strict temperature maintenance, such as vaccines, biological samples, fresh produce, and premium food items. The technology includes multiple sensors positioned throughout the storage space, ensuring uniform temperature distribution without hot or cold spots that could compromise product quality. Automatic defrost cycles prevent ice buildup that reduces efficiency, while safety alarms immediately alert operators to any temperature excursions beyond acceptable ranges. Remote monitoring capabilities allow managers to track conditions from mobile devices, receiving instant notifications about potential issues before they affect stored inventory. This proactive approach prevents costly product losses and demonstrates due diligence during regulatory audits. The advanced control systems also generate detailed temperature logs automatically, creating comprehensive documentation that satisfies traceability requirements across pharmaceutical, food safety, and quality management standards.
Superior Insulation and Energy Efficiency

Superior Insulation and Energy Efficiency

The industrial cold room features high-performance insulation technology that dramatically reduces energy consumption while maintaining stable internal temperatures. Premium polyurethane foam panels, typically ranging from seventy-five to one hundred fifty millimeters thick, create an effective thermal barrier that minimizes heat transfer between the refrigerated space and ambient environment. This exceptional insulation capability allows refrigeration systems to operate less frequently, reducing wear on mechanical components and extending equipment lifespan. The cam-lock panel assembly system ensures tight seals at panel joints, eliminating air infiltration that forces cooling systems to work harder. Energy-efficient LED lighting consumes minimal power while providing excellent visibility, and insulated doors with high-quality gaskets prevent cold air escape during access. Many installations achieve energy performance ratings that qualify for utility rebates and green building certifications, further enhancing return on investment. The combination of superior insulation and efficient refrigeration technology can reduce operational costs by thousands of dollars annually compared to poorly insulated alternatives. Environmental benefits include lower carbon footprints and reduced refrigerant usage, aligning operations with sustainability initiatives. Businesses benefit from predictable energy expenses, protection against utility rate increases, and enhanced corporate responsibility profiles that appeal to environmentally conscious customers and stakeholders.
Customizable Design for Diverse Applications

Customizable Design for Diverse Applications

The industrial cold room offers unmatched flexibility through customizable configurations that address specific operational requirements across different industries and storage needs. Design options include various chamber sizes from compact units of ten square meters to expansive facilities exceeding one thousand square meters, accommodating businesses at every scale. Temperature ranges can be specified based on product requirements, supporting everything from cool storage at two degrees Celsius for fresh produce to deep freeze conditions at minus thirty degrees Celsius for long-term frozen goods preservation. Interior layouts can be optimized with adjustable shelving systems, pallet racking configurations, or open floor plans for bulk storage, maximizing space utilization according to inventory characteristics. Special features such as dual-temperature zones, rapid cooling capabilities, humidity controls, and specialized flooring for heavy forklift traffic can be integrated during design. The modular construction allows phased installation, letting businesses start with essential capacity and expand systematically as demand increases without disrupting existing operations. Doorway configurations including sliding doors, hinged doors, or strip curtains can be selected based on traffic patterns and accessibility requirements. This customization ensures the industrial cold room integrates seamlessly into existing facilities, complementing workflow patterns and enhancing operational efficiency rather than forcing businesses to adapt processes around inflexible infrastructure.
Industrial Cold Room Solutions & Benefits

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
Industrial Cold Room Solutions & Benefits

Copyright © 2026 Ningbo Lucky Star Import & Export Co., Ltd. All rights reserved.  -  Privacy policy