Air Cooled Condensing Unit Factory Solutions

All Categories

air cooled condensing unit factory

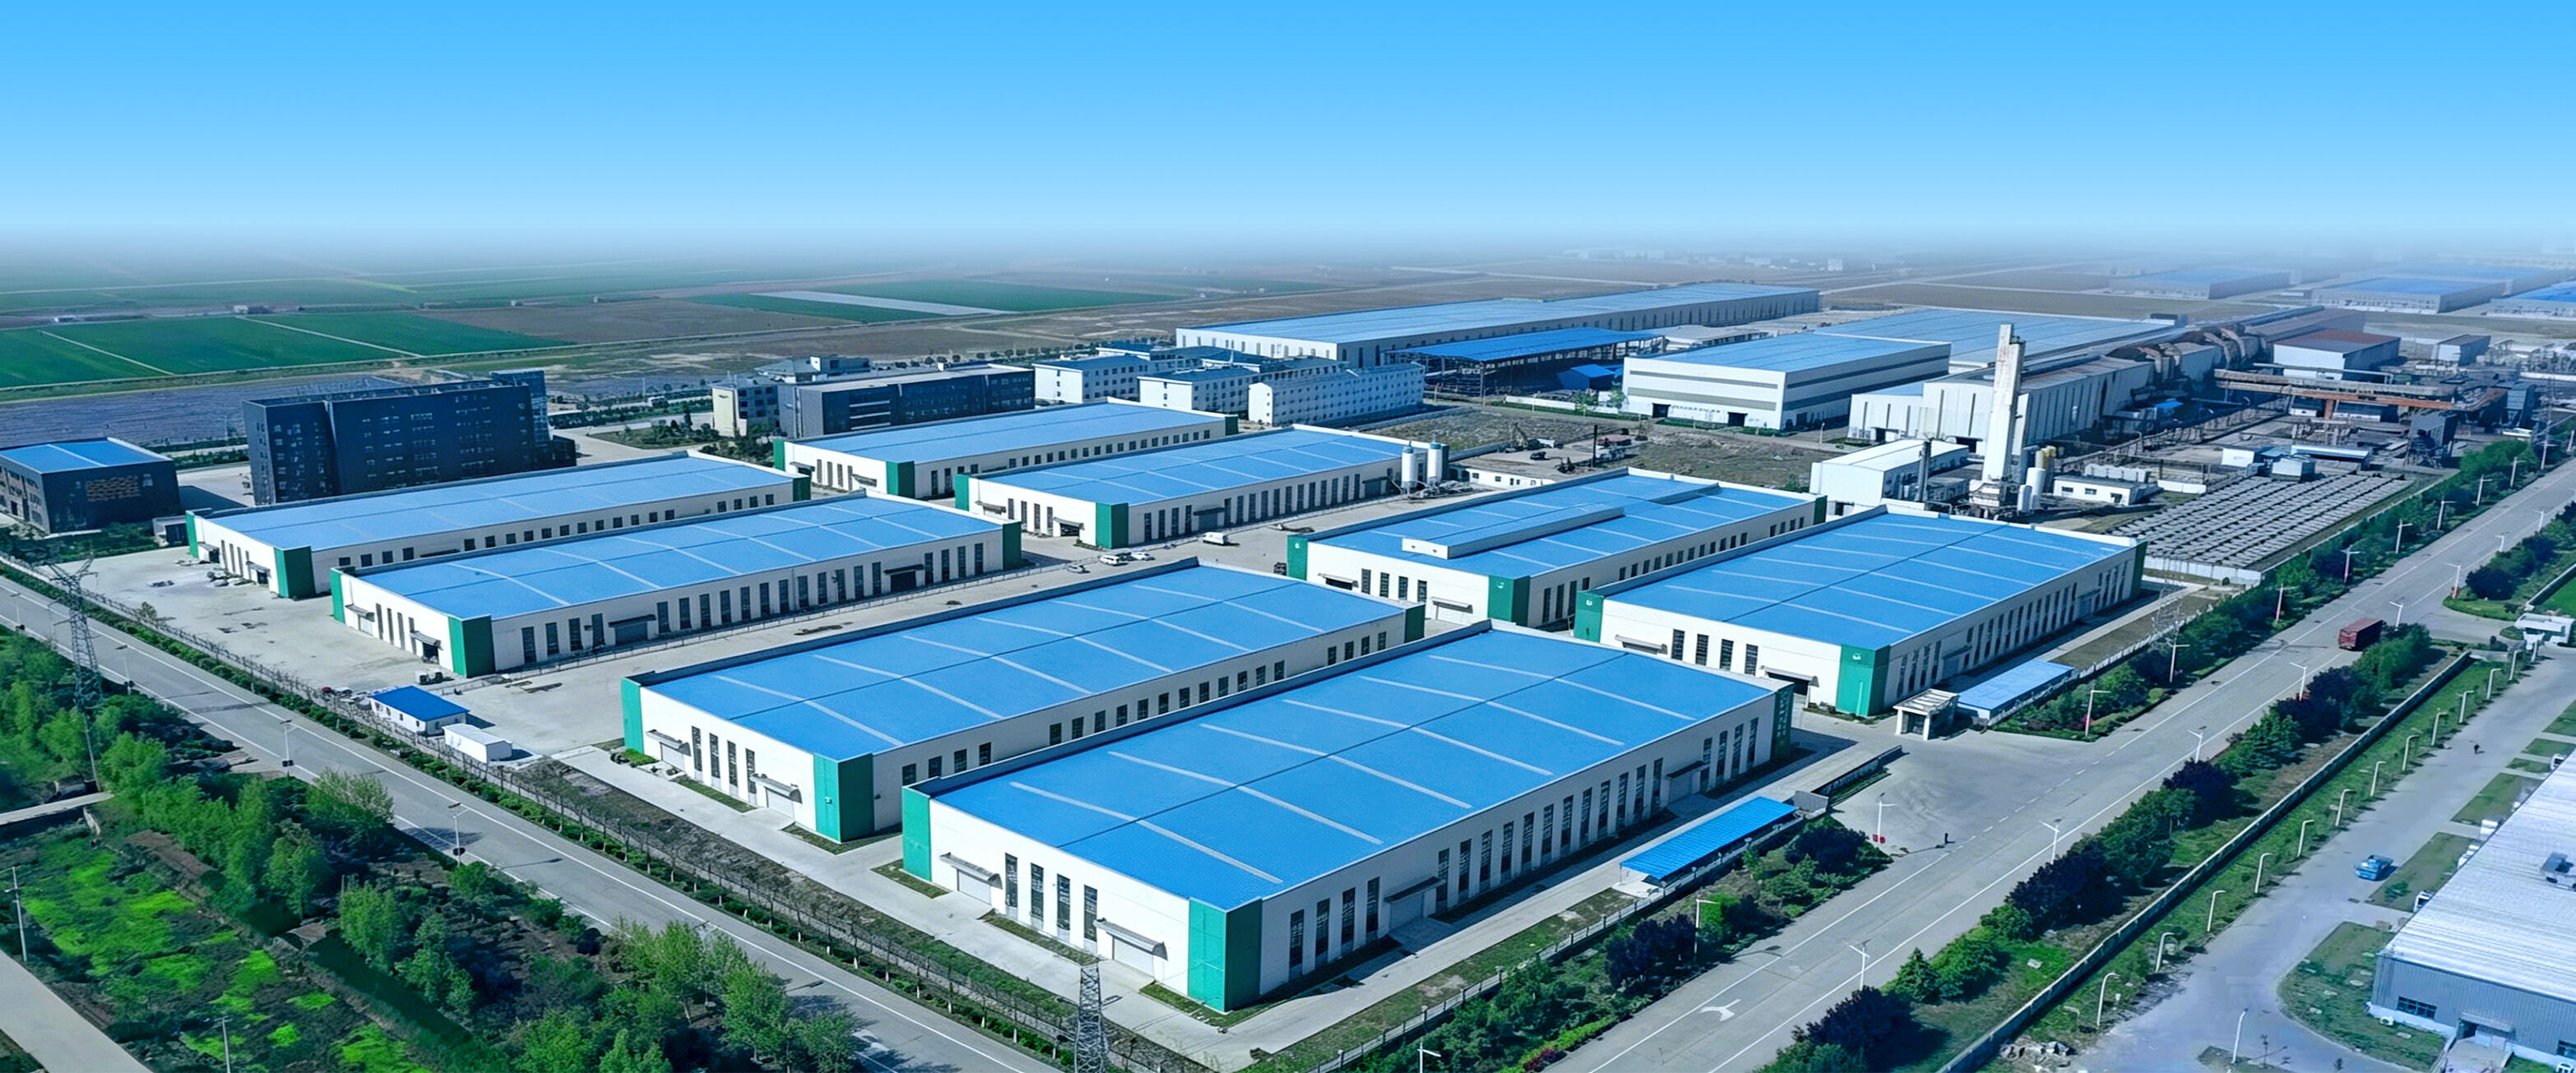
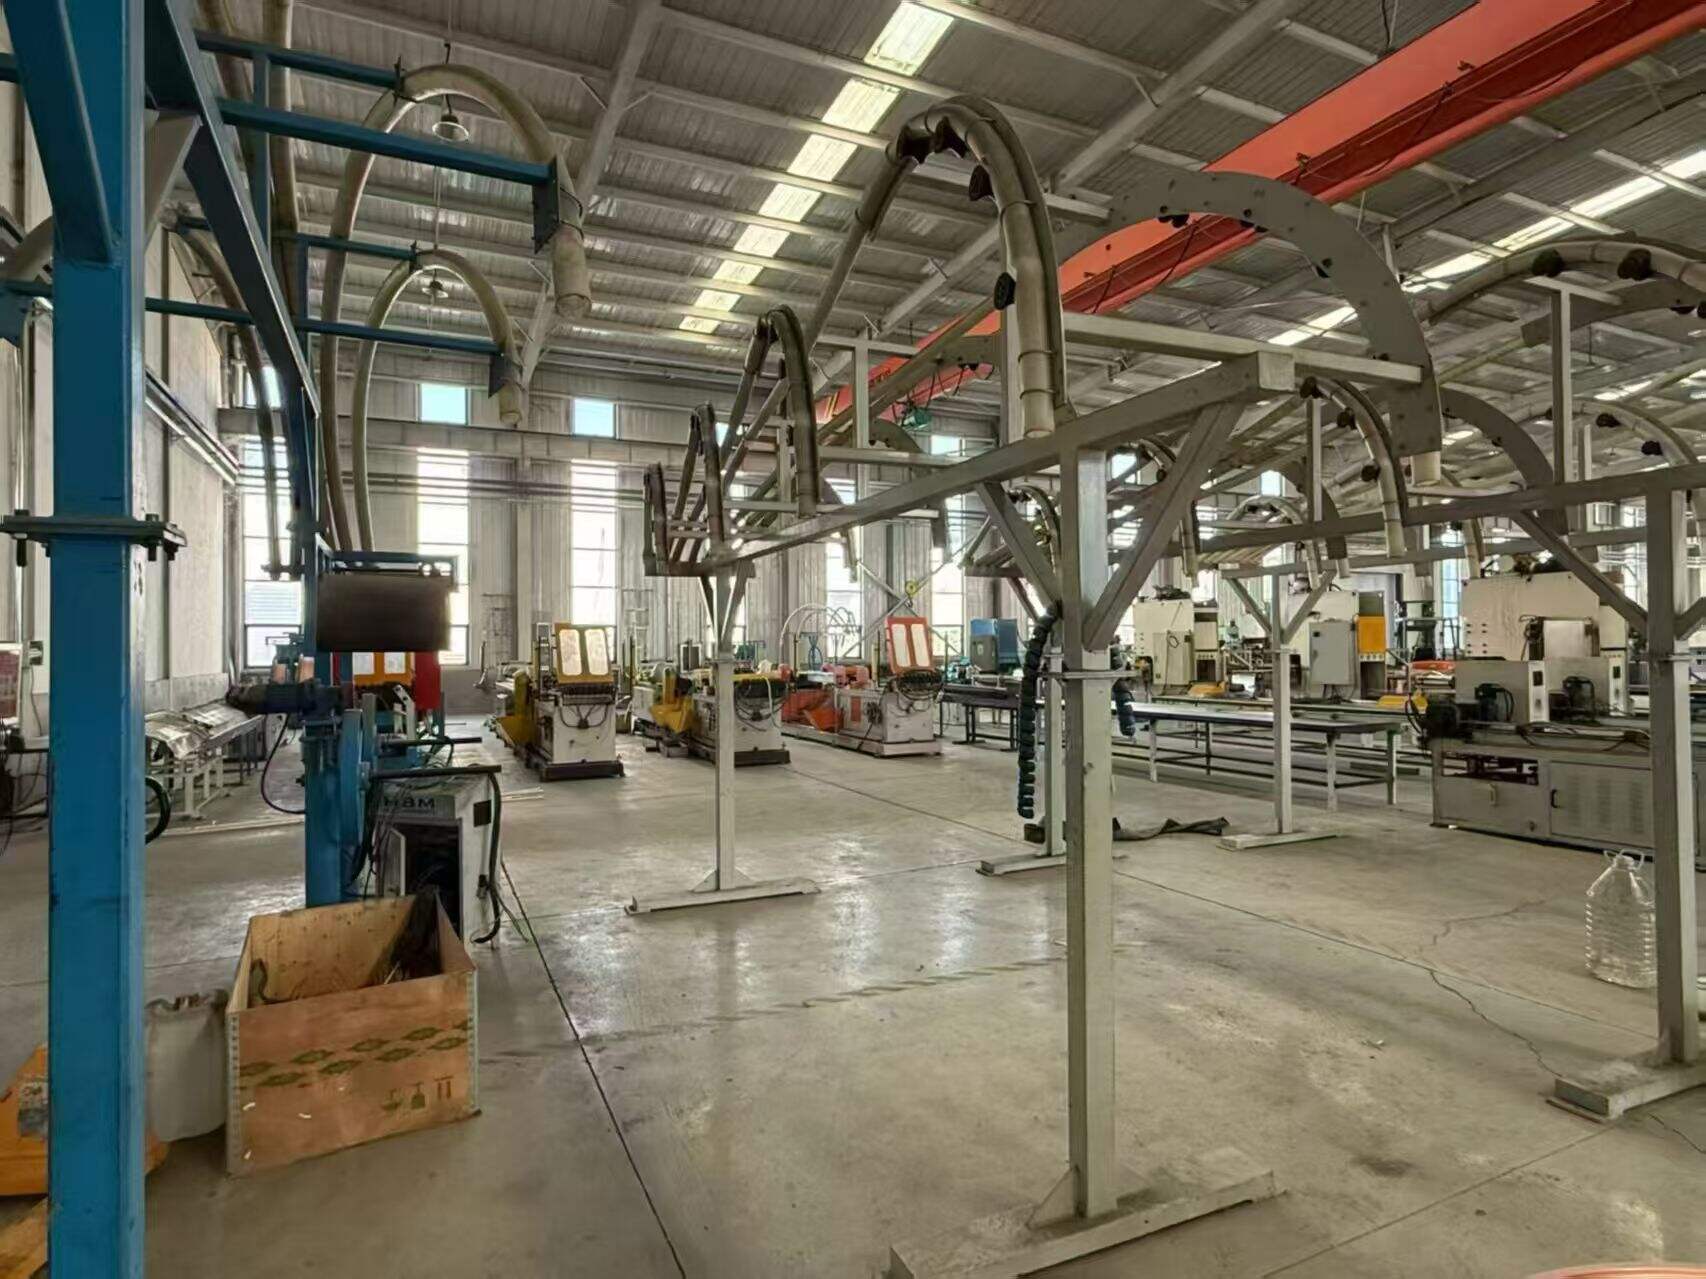
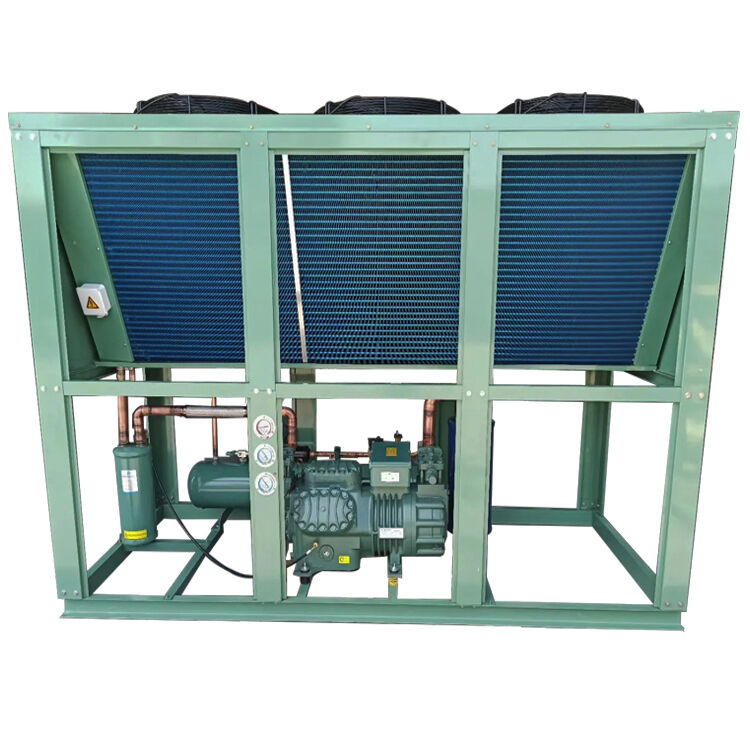
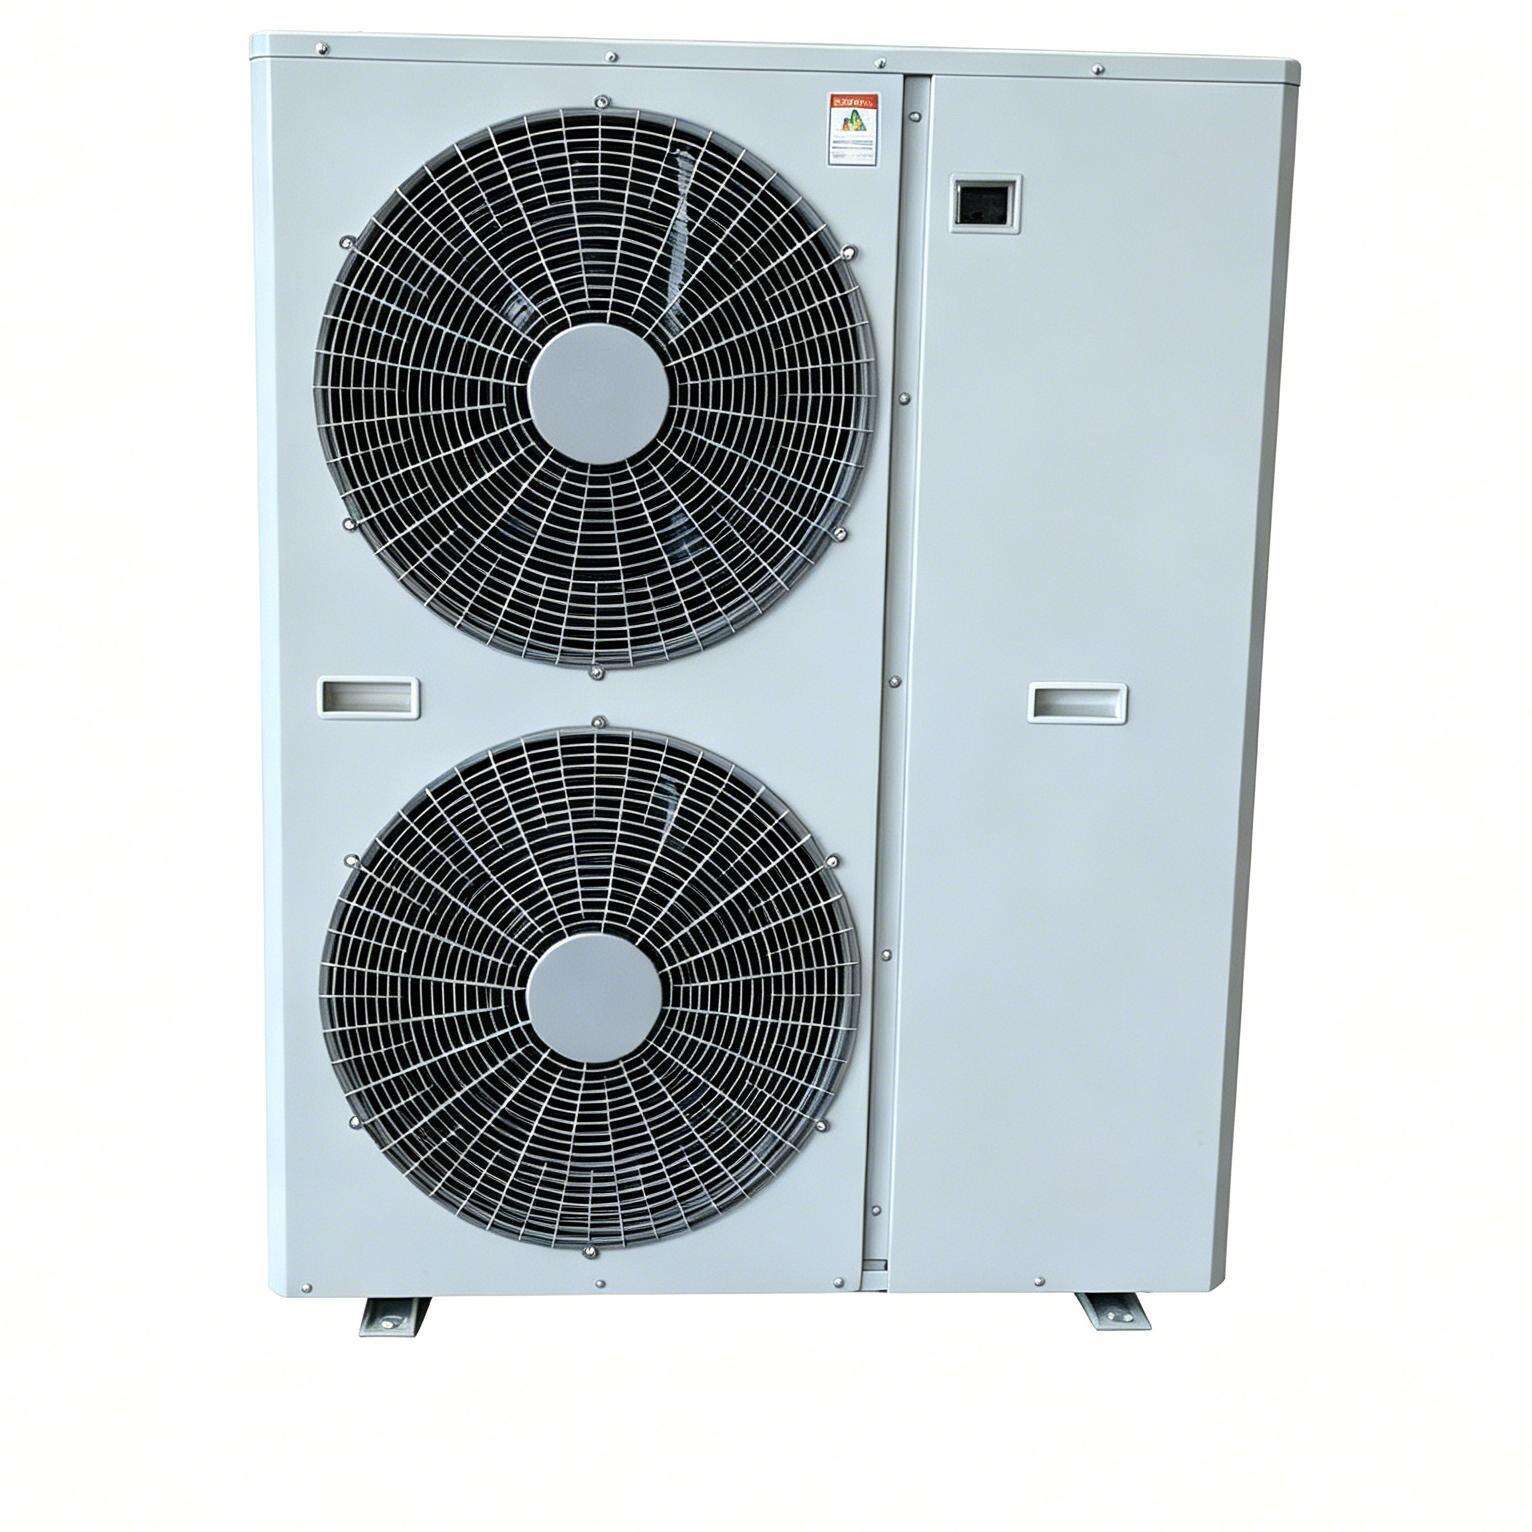
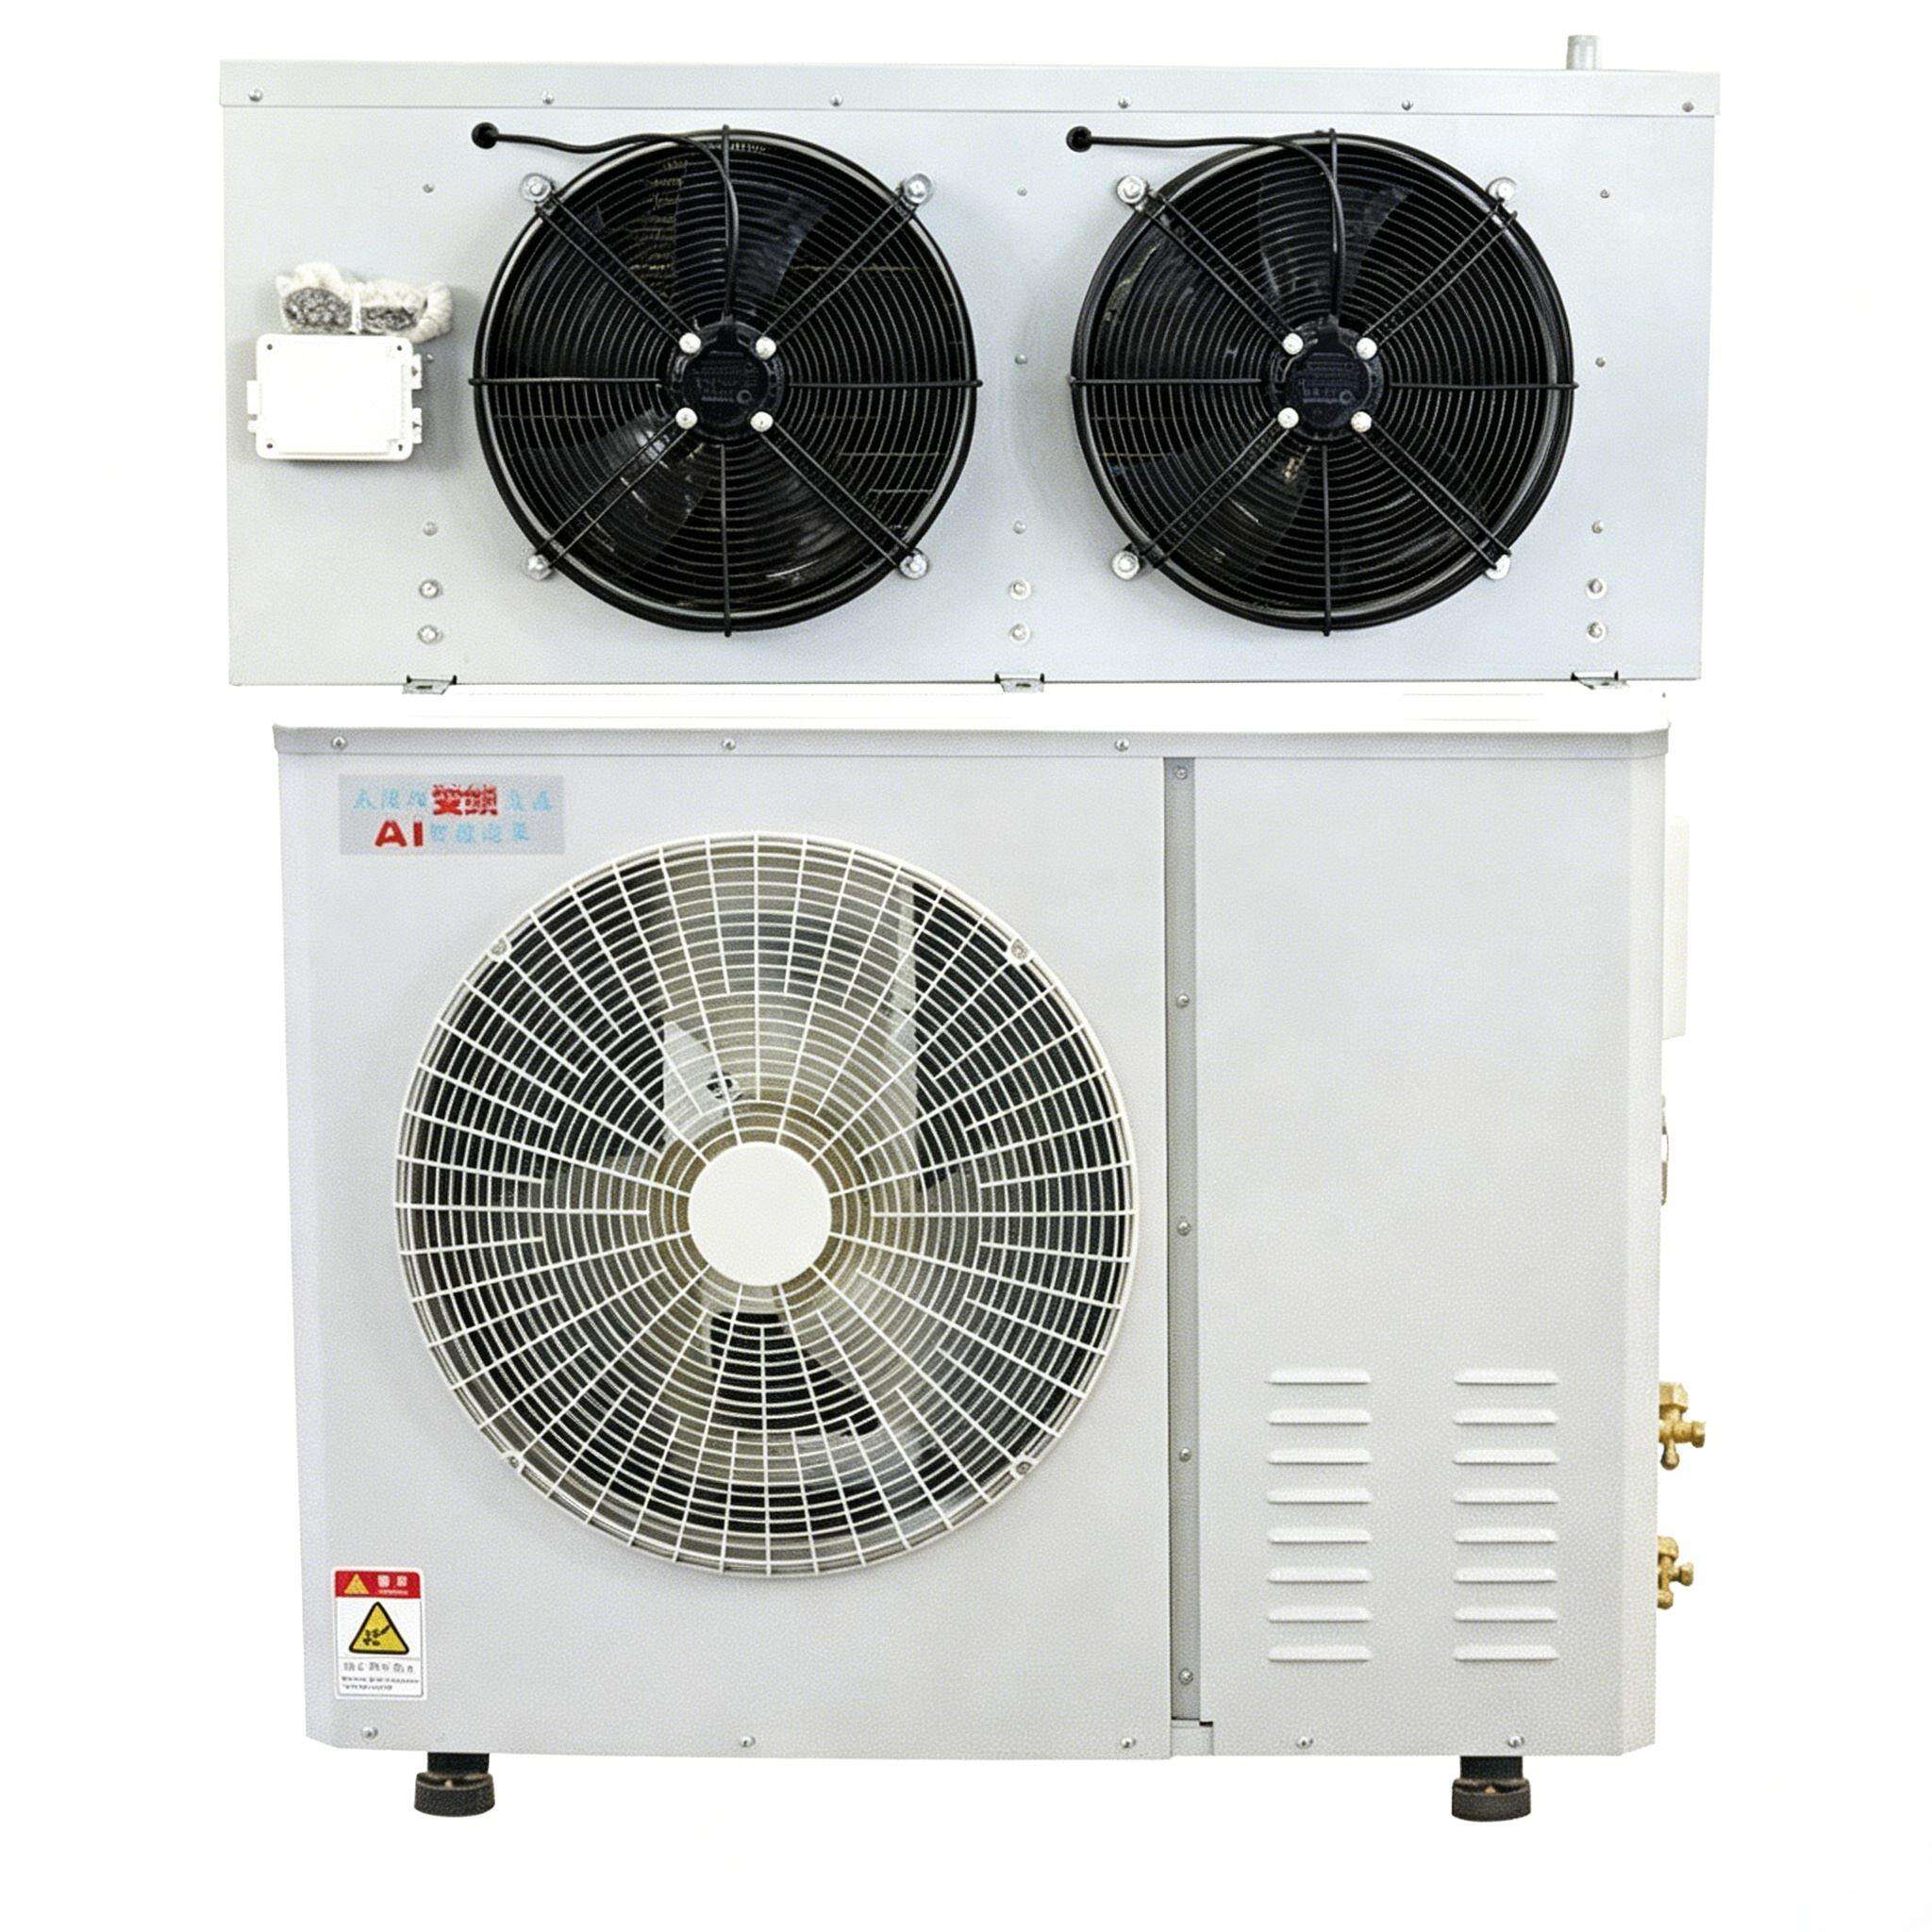
An air cooled condensing unit factory specializes in manufacturing refrigeration systems that reject heat through ambient air circulation rather than water cooling methods. These facilities produce complete condensing units comprising compressors, condenser coils, fans, motors, and control systems integrated into compact assemblies. The air cooled condensing unit factory employs advanced fabrication techniques including precision welding, copper tube bending, aluminum fin processing, and automated assembly lines to ensure consistent product quality. Main functions include heat rejection from refrigeration cycles, pressure regulation, and refrigerant management across diverse cooling applications. Technological features incorporate variable speed drives, intelligent defrost systems, environmentally friendly refrigerants, and modular designs that simplify installation and maintenance. Production processes within an air cooled condensing unit factory utilize computer-aided design software, robotic welding stations, vacuum brazing equipment, and comprehensive testing chambers that simulate extreme operating conditions. Applications span commercial refrigeration including supermarkets and convenience stores, industrial process cooling, HVAC systems for buildings, cold storage warehouses, food processing facilities, and pharmaceutical manufacturing environments. The air cooled condensing unit factory implements rigorous quality control protocols including pressure testing, leak detection, electrical safety verification, and performance validation under varying ambient temperatures. Modern facilities prioritize energy efficiency optimization, noise reduction engineering, corrosion-resistant materials, and compliance with international refrigeration standards to deliver reliable cooling solutions for global markets.
Popular Products

Choosing products from an air cooled condensing unit factory delivers significant operational benefits that directly impact your bottom line. These units eliminate water consumption entirely, reducing utility costs and environmental impact while avoiding scaling and water treatment expenses associated with water-cooled systems. Installation simplicity stands out as buyers appreciate plug-and-play designs requiring minimal infrastructure modifications, saving thousands in construction costs compared to cooling tower installations. The air cooled condensing unit factory builds equipment with accessibility in mind, positioning components for straightforward maintenance that your technicians can perform without specialized training, reducing downtime and service expenses. Energy efficiency improvements translate to lower electricity bills as modern units incorporate variable speed technology that adjusts cooling capacity to actual demand rather than running at full power continuously. Application suitability extends across climates and industries because these units operate independently of water availability, making them ideal for remote locations, urban environments with water restrictions, and facilities requiring rapid deployment. Durability engineering ensures extended service life through corrosion-resistant coatings, robust fan motors, and quality compressors that withstand harsh outdoor conditions. The air cooled condensing unit factory designs modular systems allowing capacity expansion by adding units rather than replacing entire systems, protecting your capital investment as business grows. Noise management technologies benefit operations in noise-sensitive environments through sound-attenuating fan designs and vibration isolation. Flexibility in refrigerant options means compliance with evolving environmental regulations without equipment obsolescence. Decision-makers value predictable performance across temperature ranges as these factories test units under extreme conditions, guaranteeing reliable operation during peak cooling demands when your business depends on uninterrupted refrigeration.

Practical Tips

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

28

Feb

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

View More
Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

28

Feb

Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

View More
Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

28

Feb

Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

air cooled condensing unit factory

Advanced Manufacturing Precision and Quality Control

Advanced Manufacturing Precision and Quality Control

The air cooled condensing unit factory implements state-of-the-art manufacturing processes that guarantee exceptional product reliability and performance consistency. Automated production lines incorporate robotic welding systems that create leak-proof refrigerant circuits with precision impossible through manual fabrication, eliminating weak points that cause premature failures. Computer numerical control machinery shapes heat exchanger components to exact specifications, maximizing surface area contact and thermal transfer efficiency. Each unit undergoes multiple quality checkpoints including helium leak testing capable of detecting microscopic imperfections, high-voltage dielectric testing ensuring electrical safety, and run-testing under simulated load conditions that verify proper operation before shipping. The factory maintains climate-controlled assembly environments preventing contamination and moisture ingress that compromise refrigerant purity. Material traceability systems track every component from raw material certification through final assembly, enabling rapid issue resolution and continuous improvement. Investment in advanced testing equipment including infrared thermography, vibration analysis tools, and sound measurement chambers ensures products meet stringent performance specifications. This manufacturing excellence translates to lower warranty claims, extended equipment lifespan, and peace of mind for buyers investing in critical refrigeration infrastructure.
Energy Efficiency and Environmental Sustainability

Energy Efficiency and Environmental Sustainability

Products from an air cooled condensing unit factory incorporate cutting-edge energy-saving technologies that substantially reduce operational costs while supporting environmental responsibility goals. Variable frequency drives modulate compressor and fan speeds dynamically, matching cooling output precisely to thermal load requirements rather than cycling on-off inefficiently, achieving energy savings of twenty to forty percent compared to fixed-speed alternatives. Advanced heat exchanger designs featuring optimized fin geometries and enhanced tube surfaces improve heat rejection efficiency, allowing smaller, lighter units that consume less power while delivering equivalent cooling capacity. The factory engineers units for low-GWP refrigerants including R-448A, R-449A, and R-513A that minimize environmental impact without sacrificing performance, future-proofing your investment against regulatory phase-outs. Intelligent defrost algorithms monitor actual frost accumulation rather than running time-based cycles, reducing unnecessary energy consumption during defrost operations. Microchannel condenser technology available from leading air cooled condensing unit factory facilities reduces refrigerant charge by up to fifty percent while improving efficiency and lowering leak potential. Energy management systems provide real-time monitoring and optimization recommendations, empowering facility managers to maximize efficiency through data-driven decisions that compound savings over equipment lifetime.
Customization Capabilities and Application Versatility

Customization Capabilities and Application Versatility

An established air cooled condensing unit factory offers extensive customization options that address unique operational requirements across diverse industries and climates. Engineering teams collaborate with buyers to specify compressor configurations, from single reciprocating units for small applications to multiple scroll or screw compressors for large-capacity installations requiring redundancy. Custom coil designs accommodate extreme ambient conditions, with options including oversized condensers for high-temperature environments, epoxy-coated fins for corrosive atmospheres, and specialized materials for marine applications. The factory provides voltage and frequency variations matching global electrical standards, simplifying international deployment and equipment sourcing. Control system integration capabilities allow seamless connection with building management systems, remote monitoring platforms, and existing automation infrastructure through standard protocols. Mounting configurations adapt to space constraints with vertical, horizontal, and rooftop designs that optimize available installation areas. Sound attenuation packages address noise-sensitive applications through acoustic enclosures, low-RPM fan options, and vibration isolation without compromising cooling performance. The air cooled condensing unit factory maintains flexible production scheduling accommodating urgent replacement needs and large project phasing requirements, supporting your operational continuity and project timelines regardless of procurement complexity or geographic location.
Air Cooled Condensing Unit Factory Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
Air Cooled Condensing Unit Factory Solutions

Copyright © 2026 Ningbo Lucky Star Import & Export Co., Ltd. All rights reserved.  -  Privacy policy