Commercial Hermetic Condensing Unit Solutions

All Categories

commercial hermetic condensing unit

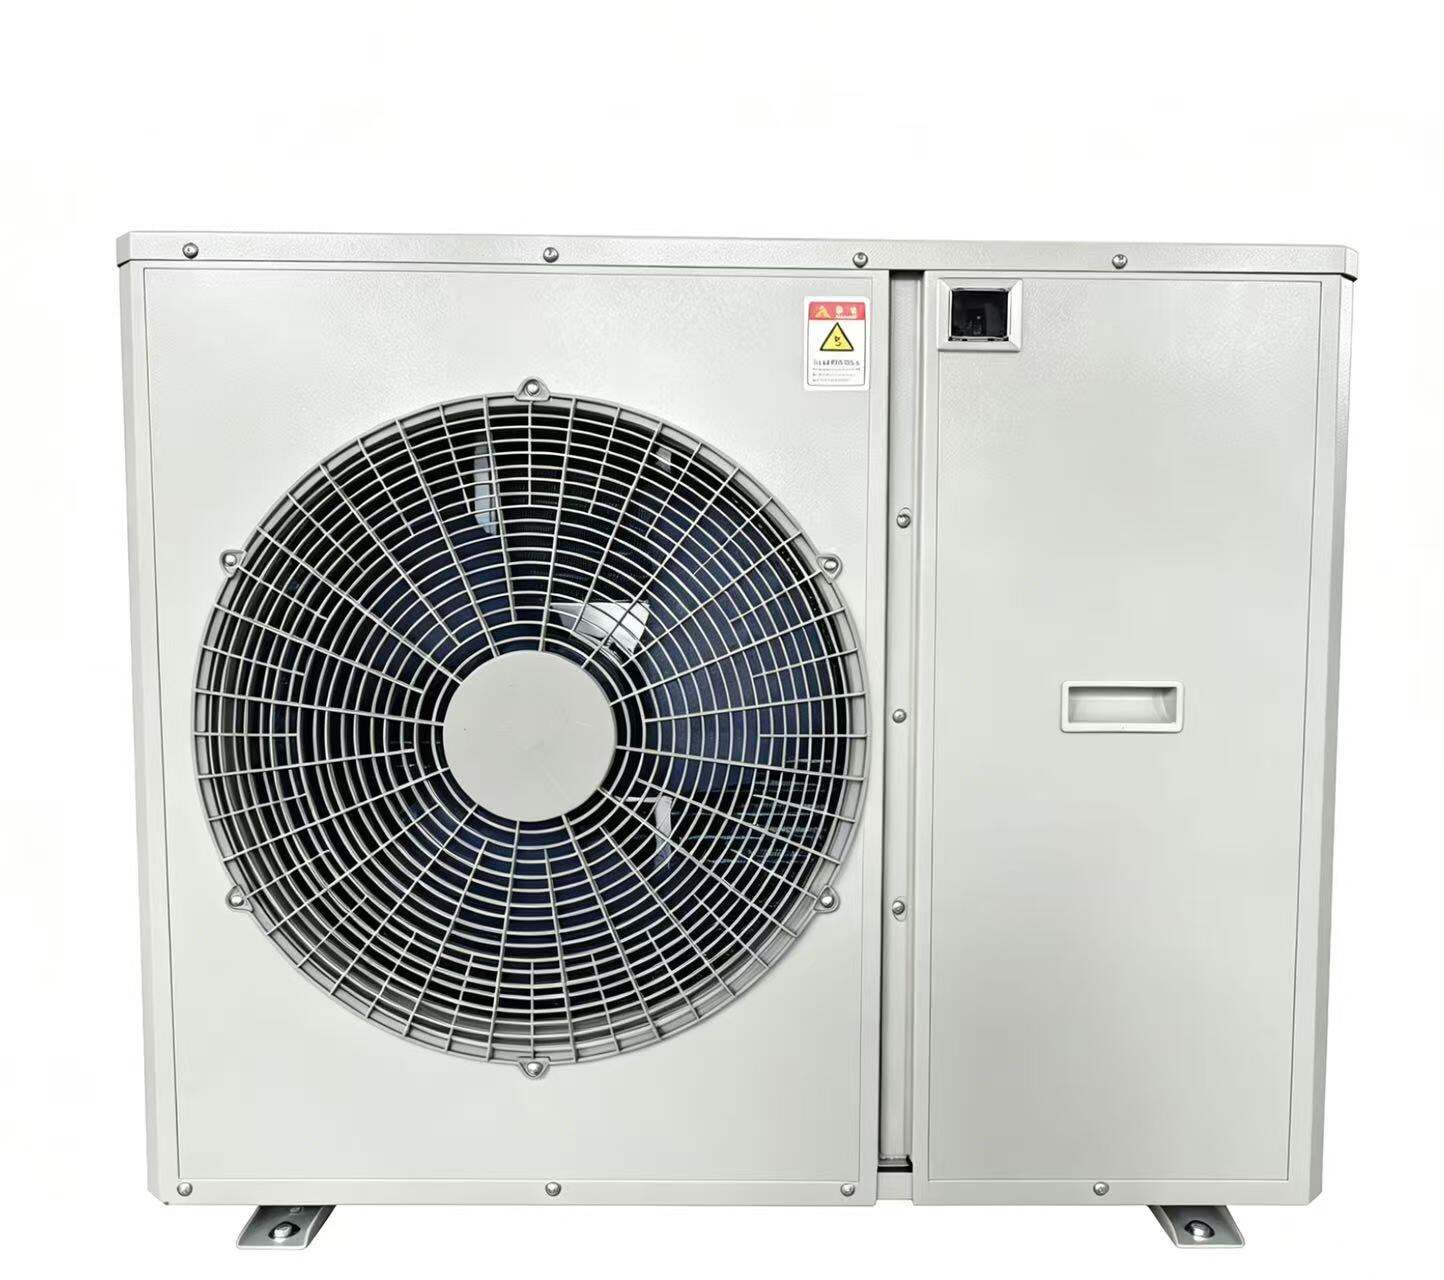
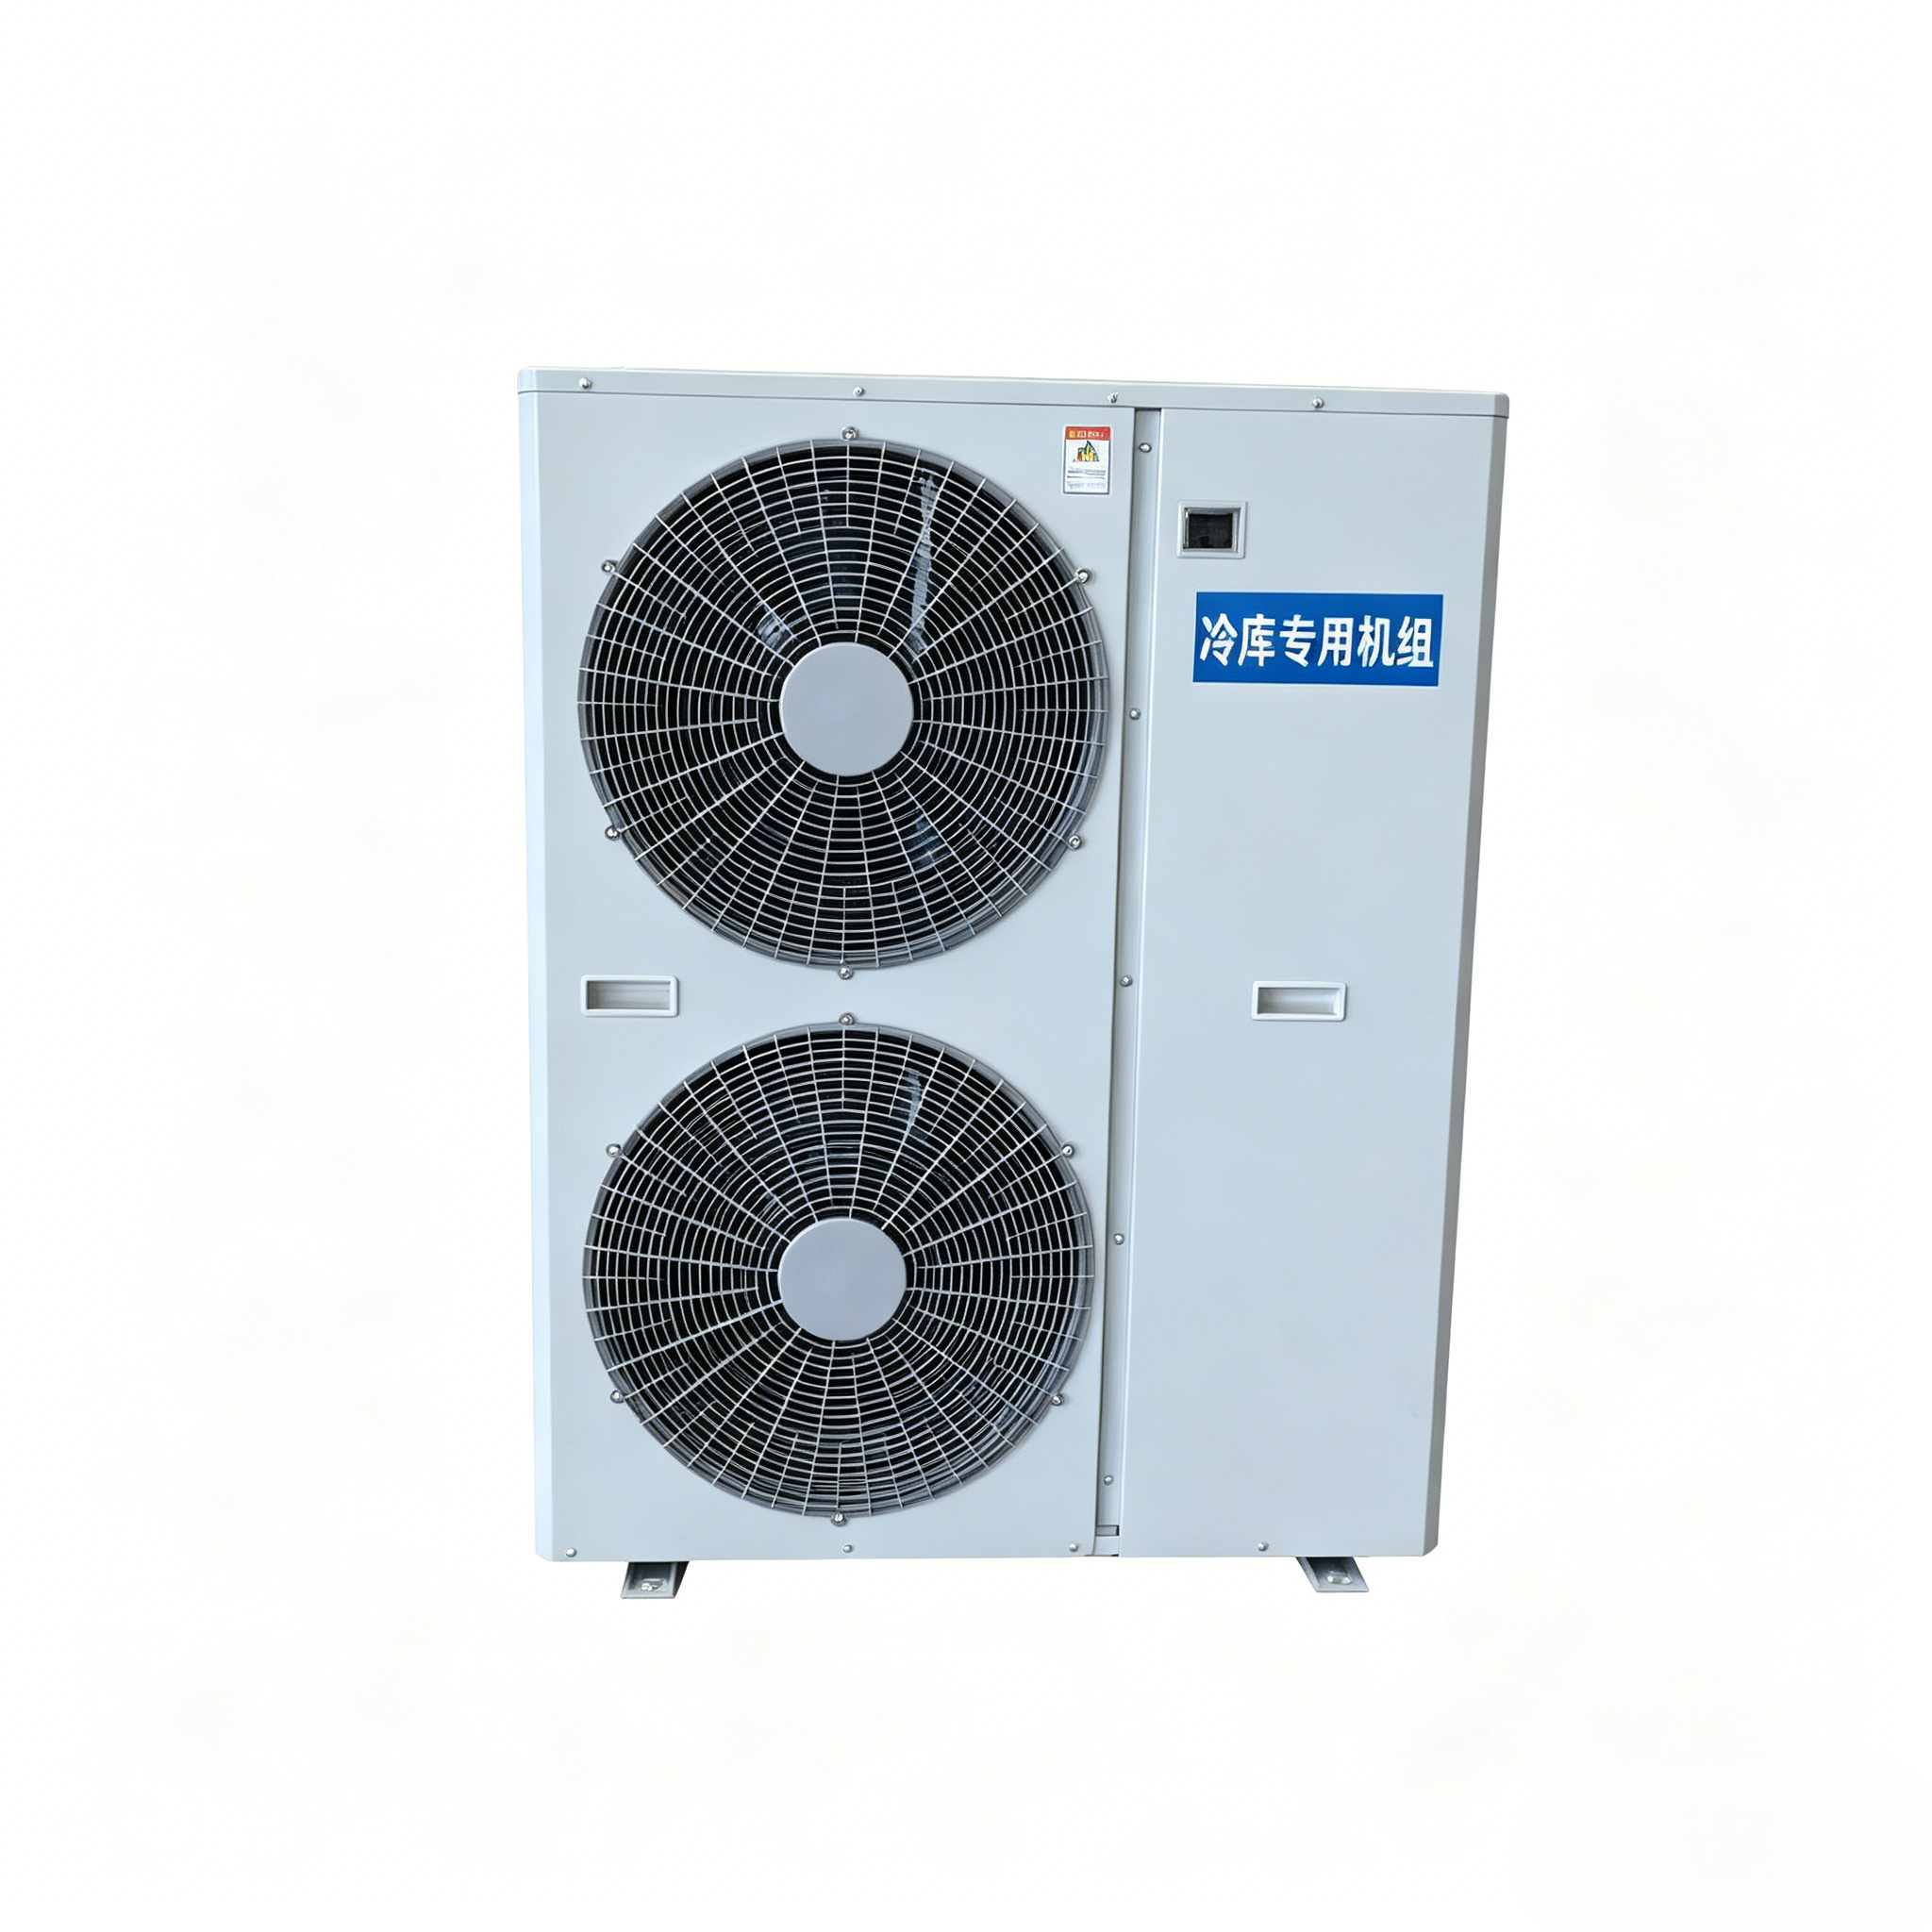
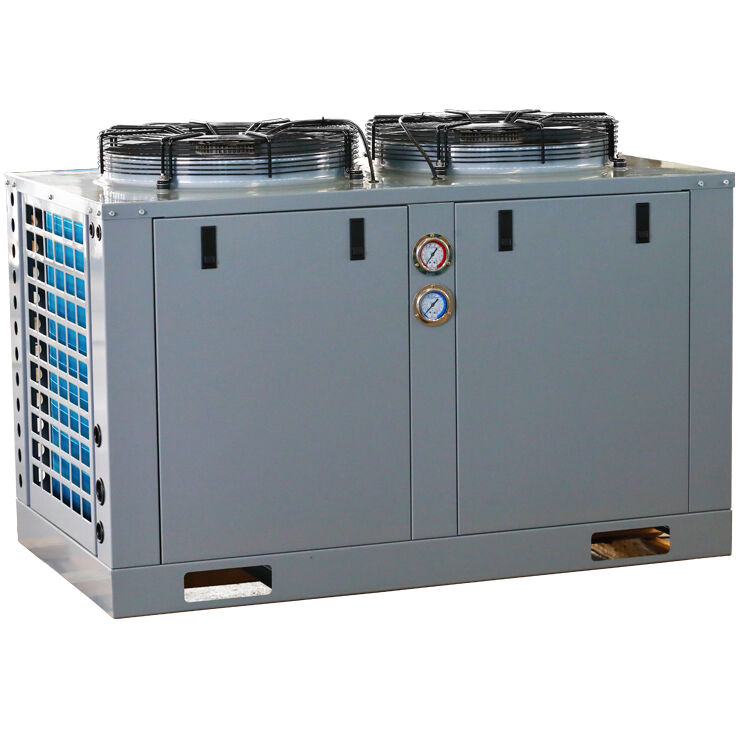
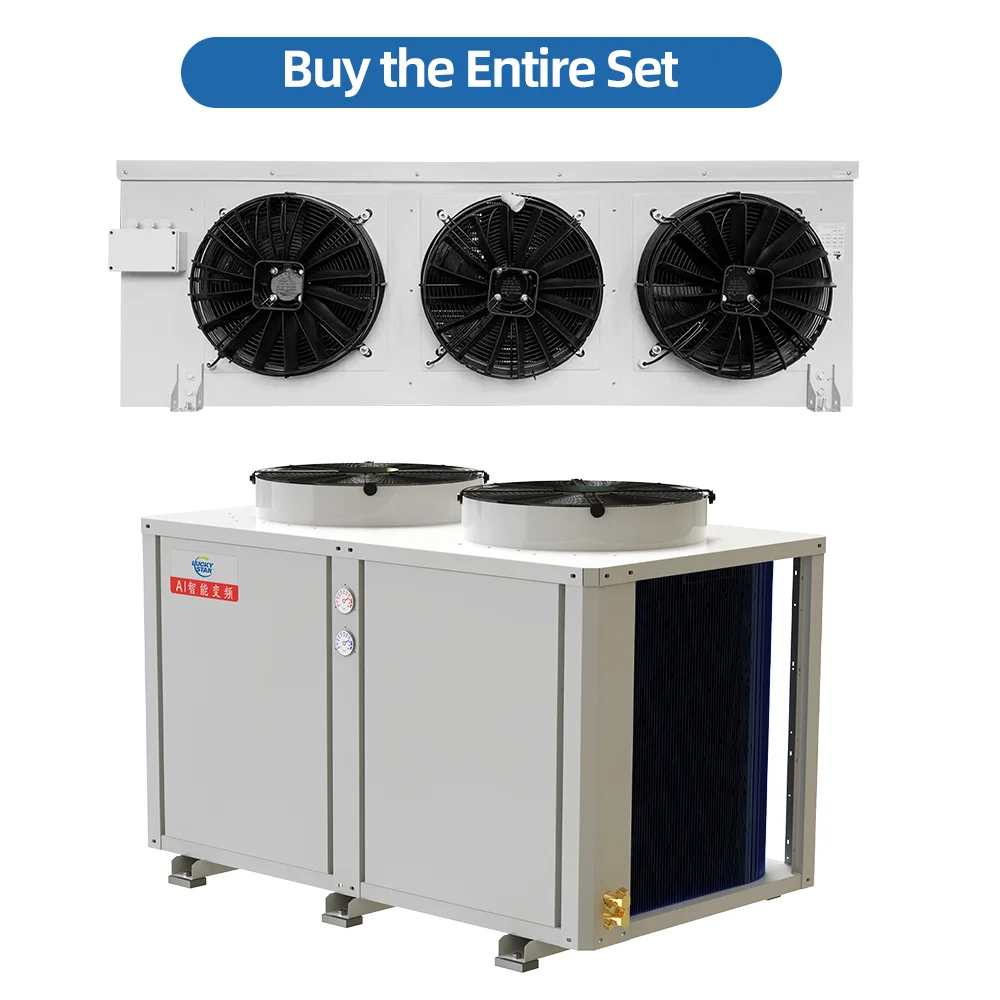
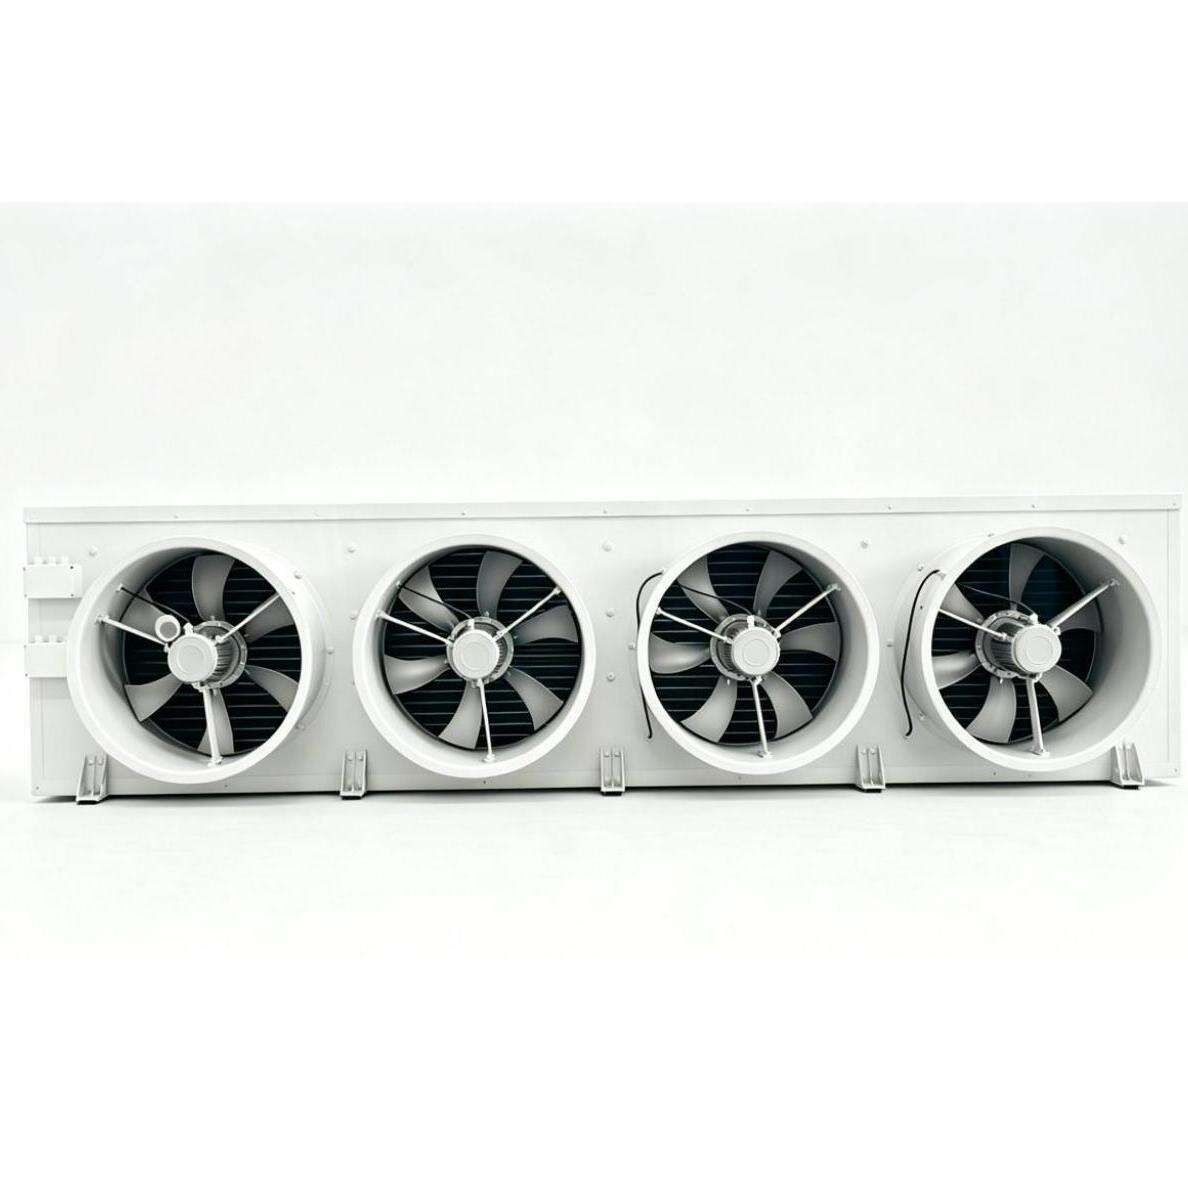
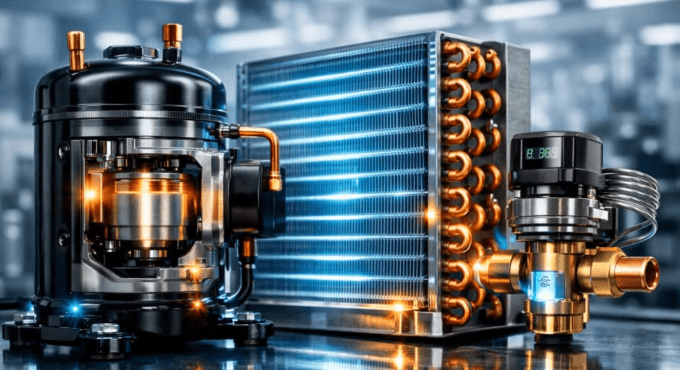
A commercial hermetic condensing unit is an essential refrigeration component designed to provide reliable cooling performance for various commercial applications. This self-contained system integrates a hermetically sealed compressor, condenser coil, fan motor, and controls into one compact assembly. The hermetic design ensures that the refrigerant and lubricating oil remain sealed within the system, preventing leaks and contamination while maximizing operational efficiency. Commercial hermetic condensing units are engineered to handle demanding cooling requirements in supermarkets, restaurants, convenience stores, cold storage facilities, and food processing plants. The primary function is to compress refrigerant vapor, reject heat through the condenser, and circulate refrigerant to evaporator coils located in refrigerated spaces. These units utilize advanced compression technology that maintains consistent temperature control while minimizing energy consumption. The condenser section employs forced-air cooling with strategically positioned fans that dissipate heat efficiently, ensuring optimal performance even in challenging ambient conditions. Modern commercial hermetic condensing units feature robust construction with corrosion-resistant materials, ensuring longevity in harsh environments. They incorporate sophisticated control systems that monitor operating parameters, provide diagnostic feedback, and enable seamless integration with building management systems. The hermetic compressor design eliminates the need for external shaft seals, significantly reducing maintenance requirements and extending service life. Available in various capacities ranging from fractional horsepower to multi-compressor configurations, these units offer flexible solutions for different cooling loads and application requirements, making them indispensable for commercial refrigeration infrastructure.
New Product Recommendations

Investing in a commercial hermetic condensing unit delivers substantial practical benefits that directly impact your bottom line and operational efficiency. The hermetically sealed compressor design eliminates refrigerant leakage concerns, reducing costly refrigerant replacement expenses and ensuring environmental compliance with increasingly stringent regulations. This sealed construction also prevents moisture and contaminants from entering the system, which means fewer breakdowns, extended equipment lifespan, and reduced maintenance costs over time. Energy efficiency represents another significant advantage, as modern commercial hermetic condensing units incorporate advanced compressor technology and optimized heat exchange surfaces that consume less electricity while delivering consistent cooling performance. Lower energy consumption translates directly into reduced utility bills, particularly important for businesses operating multiple refrigeration systems around the clock. The compact, integrated design simplifies installation, requiring less space and fewer connection points compared to open-type systems, which reduces initial installation costs and allows flexible placement even in space-constrained environments. Operational reliability stands out as a key benefit, with hermetic units operating quieter and smoother than alternative designs, minimizing disruption to customer-facing areas in retail and food service establishments. The self-contained nature means fewer external components that could fail, enhancing overall system dependability. These units adapt well to diverse applications, from walk-in coolers and freezers to display cases and processing equipment, providing versatile solutions that accommodate changing business needs. The integrated control systems offer user-friendly operation with digital displays, automated defrost cycles, and remote monitoring capabilities that enable proactive maintenance scheduling. This combination of cost savings, reliability, efficiency, and adaptability makes the commercial hermetic condensing unit an intelligent investment for businesses prioritizing long-term value and uninterrupted refrigeration performance.

Tips And Tricks

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

28

Feb

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

View More
Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

28

Feb

Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

View More
Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

28

Feb

Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

commercial hermetic condensing unit

Superior Hermetic Sealing Technology

Superior Hermetic Sealing Technology

The cornerstone feature of the commercial hermetic condensing unit lies in its advanced hermetic sealing technology that completely encloses the compressor motor and pump mechanism within a welded steel shell. This engineering approach eliminates all external shaft penetrations, creating an impenetrable barrier that locks refrigerant and lubricating oil inside while keeping moisture, dirt, and atmospheric contaminants outside. Unlike semi-hermetic or open compressors that rely on mechanical seals prone to wear and leakage, the hermetic design provides permanent protection throughout the unit's operational life. This sealed environment preserves refrigerant charge integrity, ensuring consistent system performance without the gradual efficiency degradation associated with refrigerant loss. The absence of external seals also eliminates a common maintenance requirement and potential failure point, reducing service calls and associated downtime costs. For business owners, this translates into predictable operational expenses and confidence that refrigeration systems will maintain product temperatures reliably. The hermetic construction also supports environmental responsibility by preventing refrigerant emissions that contribute to ozone depletion and climate change, helping businesses meet sustainability goals and regulatory compliance requirements while protecting valuable inventory from temperature excursions caused by system failures.
Energy-Efficient Performance Optimization

Energy-Efficient Performance Optimization

Modern commercial hermetic condensing units incorporate cutting-edge energy efficiency technologies that significantly reduce operational costs while maintaining superior cooling capacity. High-efficiency compressors utilize precision-engineered scroll or rotary designs that minimize friction losses and optimize compression cycles, converting electrical input into cooling output more effectively than older reciprocating models. Enhanced condenser coil geometry with increased surface area and optimized fin spacing maximizes heat rejection efficiency, allowing the unit to operate at lower condensing temperatures and pressures, which directly reduces compressor workload and energy consumption. Variable-speed fan motors adjust airflow based on ambient conditions and cooling demand, eliminating the energy waste associated with constant-speed operation during partial load conditions. Advanced electronic expansion valves precisely meter refrigerant flow to match real-time cooling requirements, preventing the efficiency losses caused by improper superheat settings in traditional thermostatic expansion valves. Intelligent control algorithms continuously monitor system parameters and automatically adjust operating conditions to maintain peak efficiency across varying load profiles. These combined technologies can reduce energy consumption by twenty to forty percent compared to conventional units, delivering substantial utility cost savings that accumulate significantly over the equipment's fifteen to twenty-year service life, making energy-efficient commercial hermetic condensing units a financially prudent choice for cost-conscious operators.
Robust Construction and Application Versatility

Robust Construction and Application Versatility

The commercial hermetic condensing unit features industrial-grade construction engineered to withstand demanding commercial environments while offering exceptional application flexibility. Heavy-gauge steel cabinets with powder-coated finishes provide superior corrosion resistance against moisture, salt spray, and chemical exposure common in food service and processing facilities. Reinforced mounting bases minimize vibration transmission, reducing noise levels and preventing structural fatigue in long-term installations. All-weather construction with IP-rated electrical enclosures enables reliable outdoor installation, expanding placement options and eliminating the need for dedicated mechanical rooms in space-limited facilities. The modular design accommodates various evaporator configurations, allowing a single condensing unit to serve multiple refrigerated spaces or different temperature zones through appropriate evaporator selection. Capacity options ranging from small fractional horsepower units for under-counter refrigerators to large multi-compressor rack systems for supermarket applications ensure appropriate sizing for any commercial refrigeration requirement. Universal refrigerant compatibility with R-404A, R-448A, R-449A, and R-290 options provides flexibility to meet regional regulations and environmental preferences. Factory testing and quality assurance protocols guarantee reliable operation from initial startup, while standardized replacement parts ensure service availability throughout the equipment lifecycle. This combination of durable construction and adaptable design makes the commercial hermetic condensing unit suitable for restaurants, grocery stores, hospitals, laboratories, pharmaceutical facilities, and industrial cold storage operations.
Commercial Hermetic Condensing Unit Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
Commercial Hermetic Condensing Unit Solutions

Copyright © 2026 Ningbo Lucky Star Import & Export Co., Ltd. All rights reserved.  -  Privacy policy