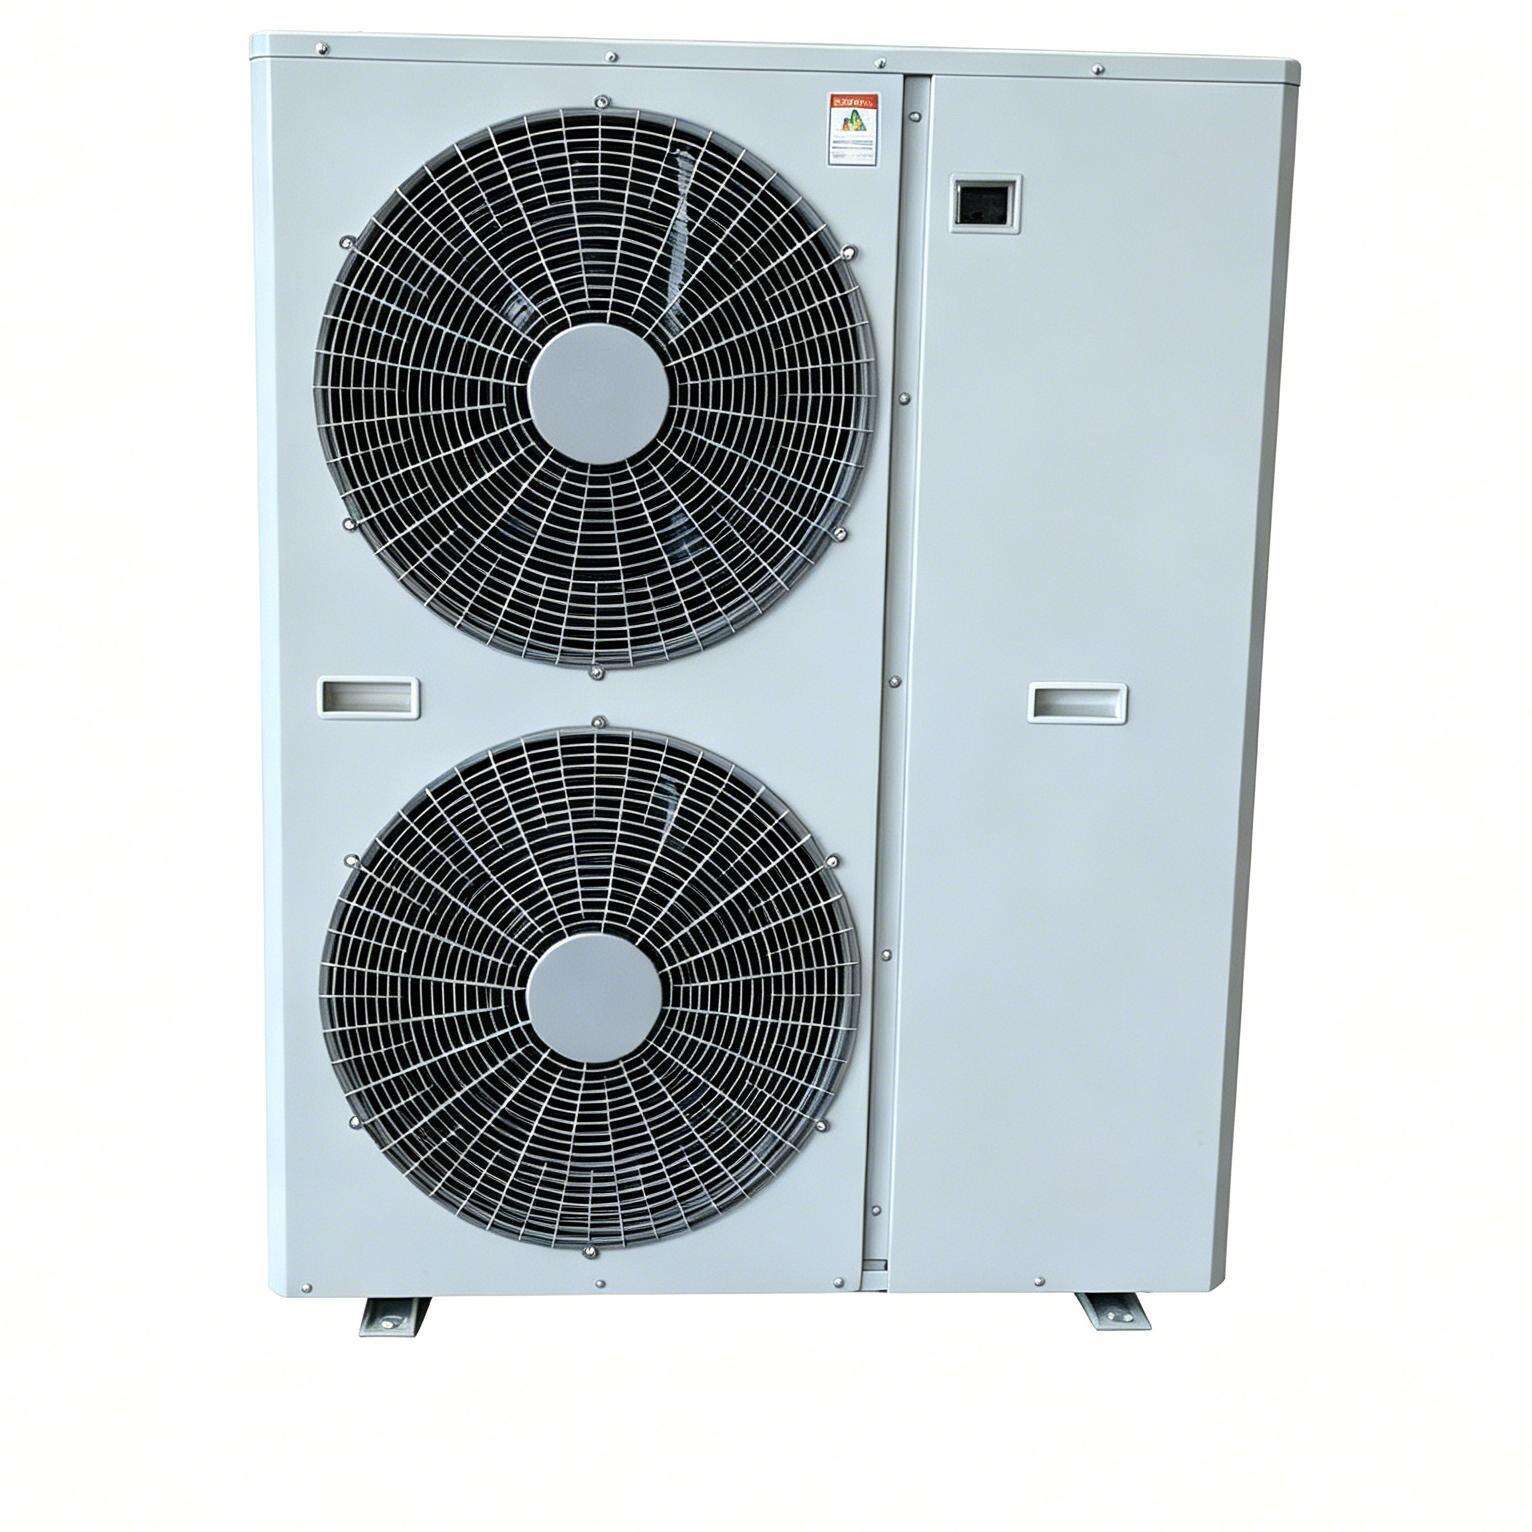
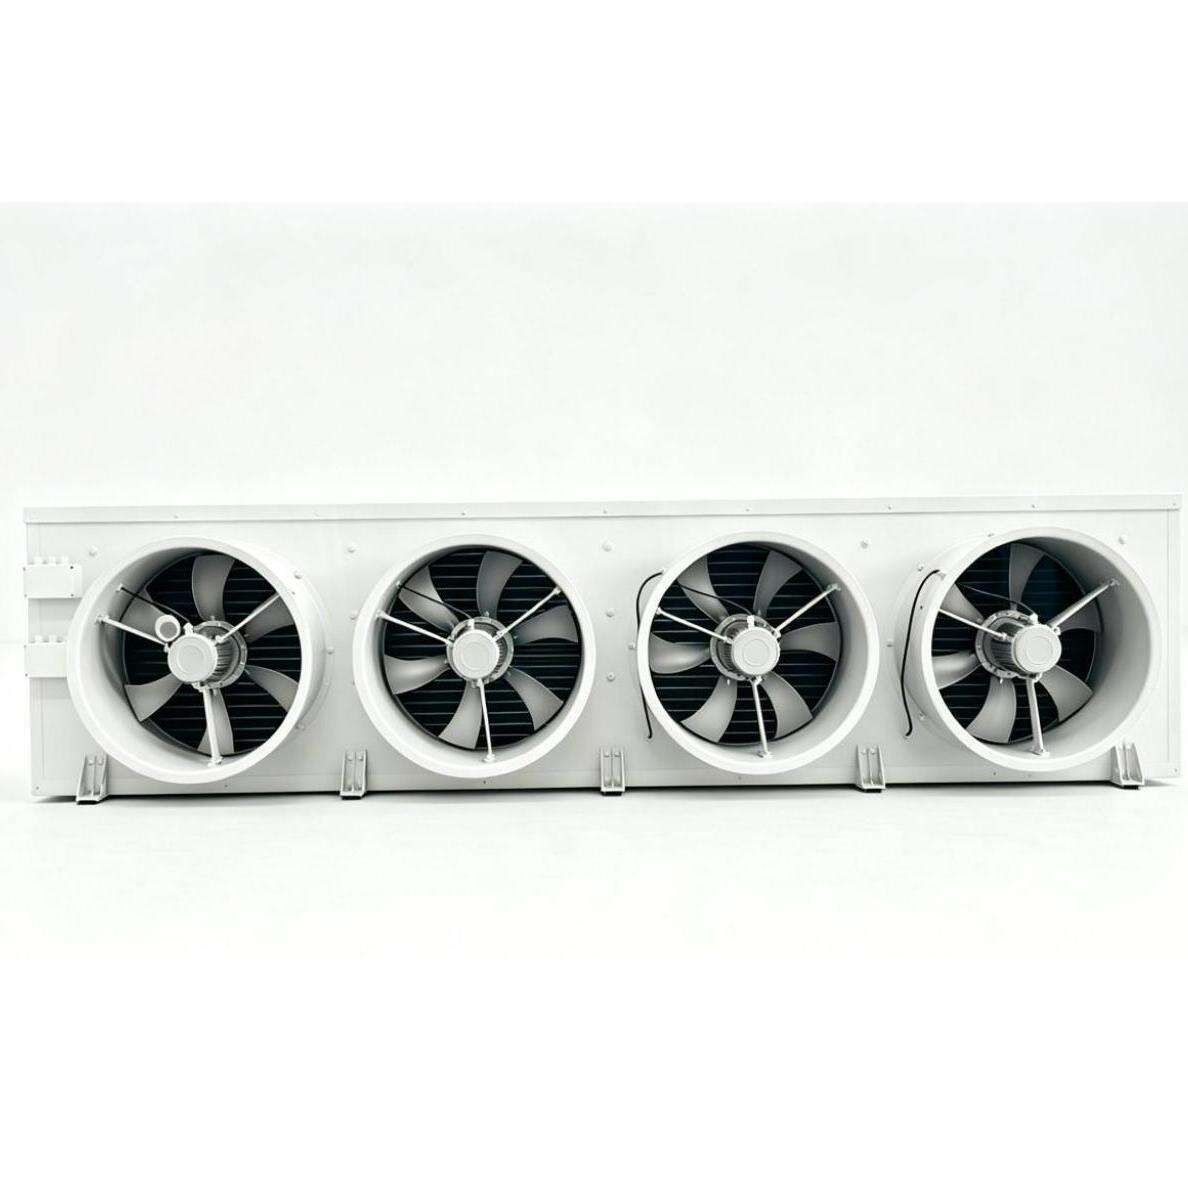
heavy duty semi hermetic condensing unit
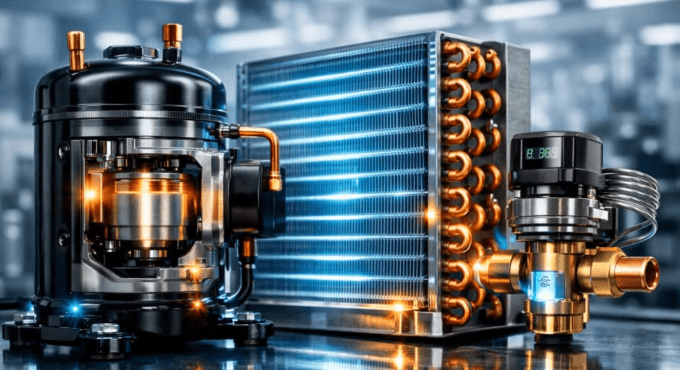
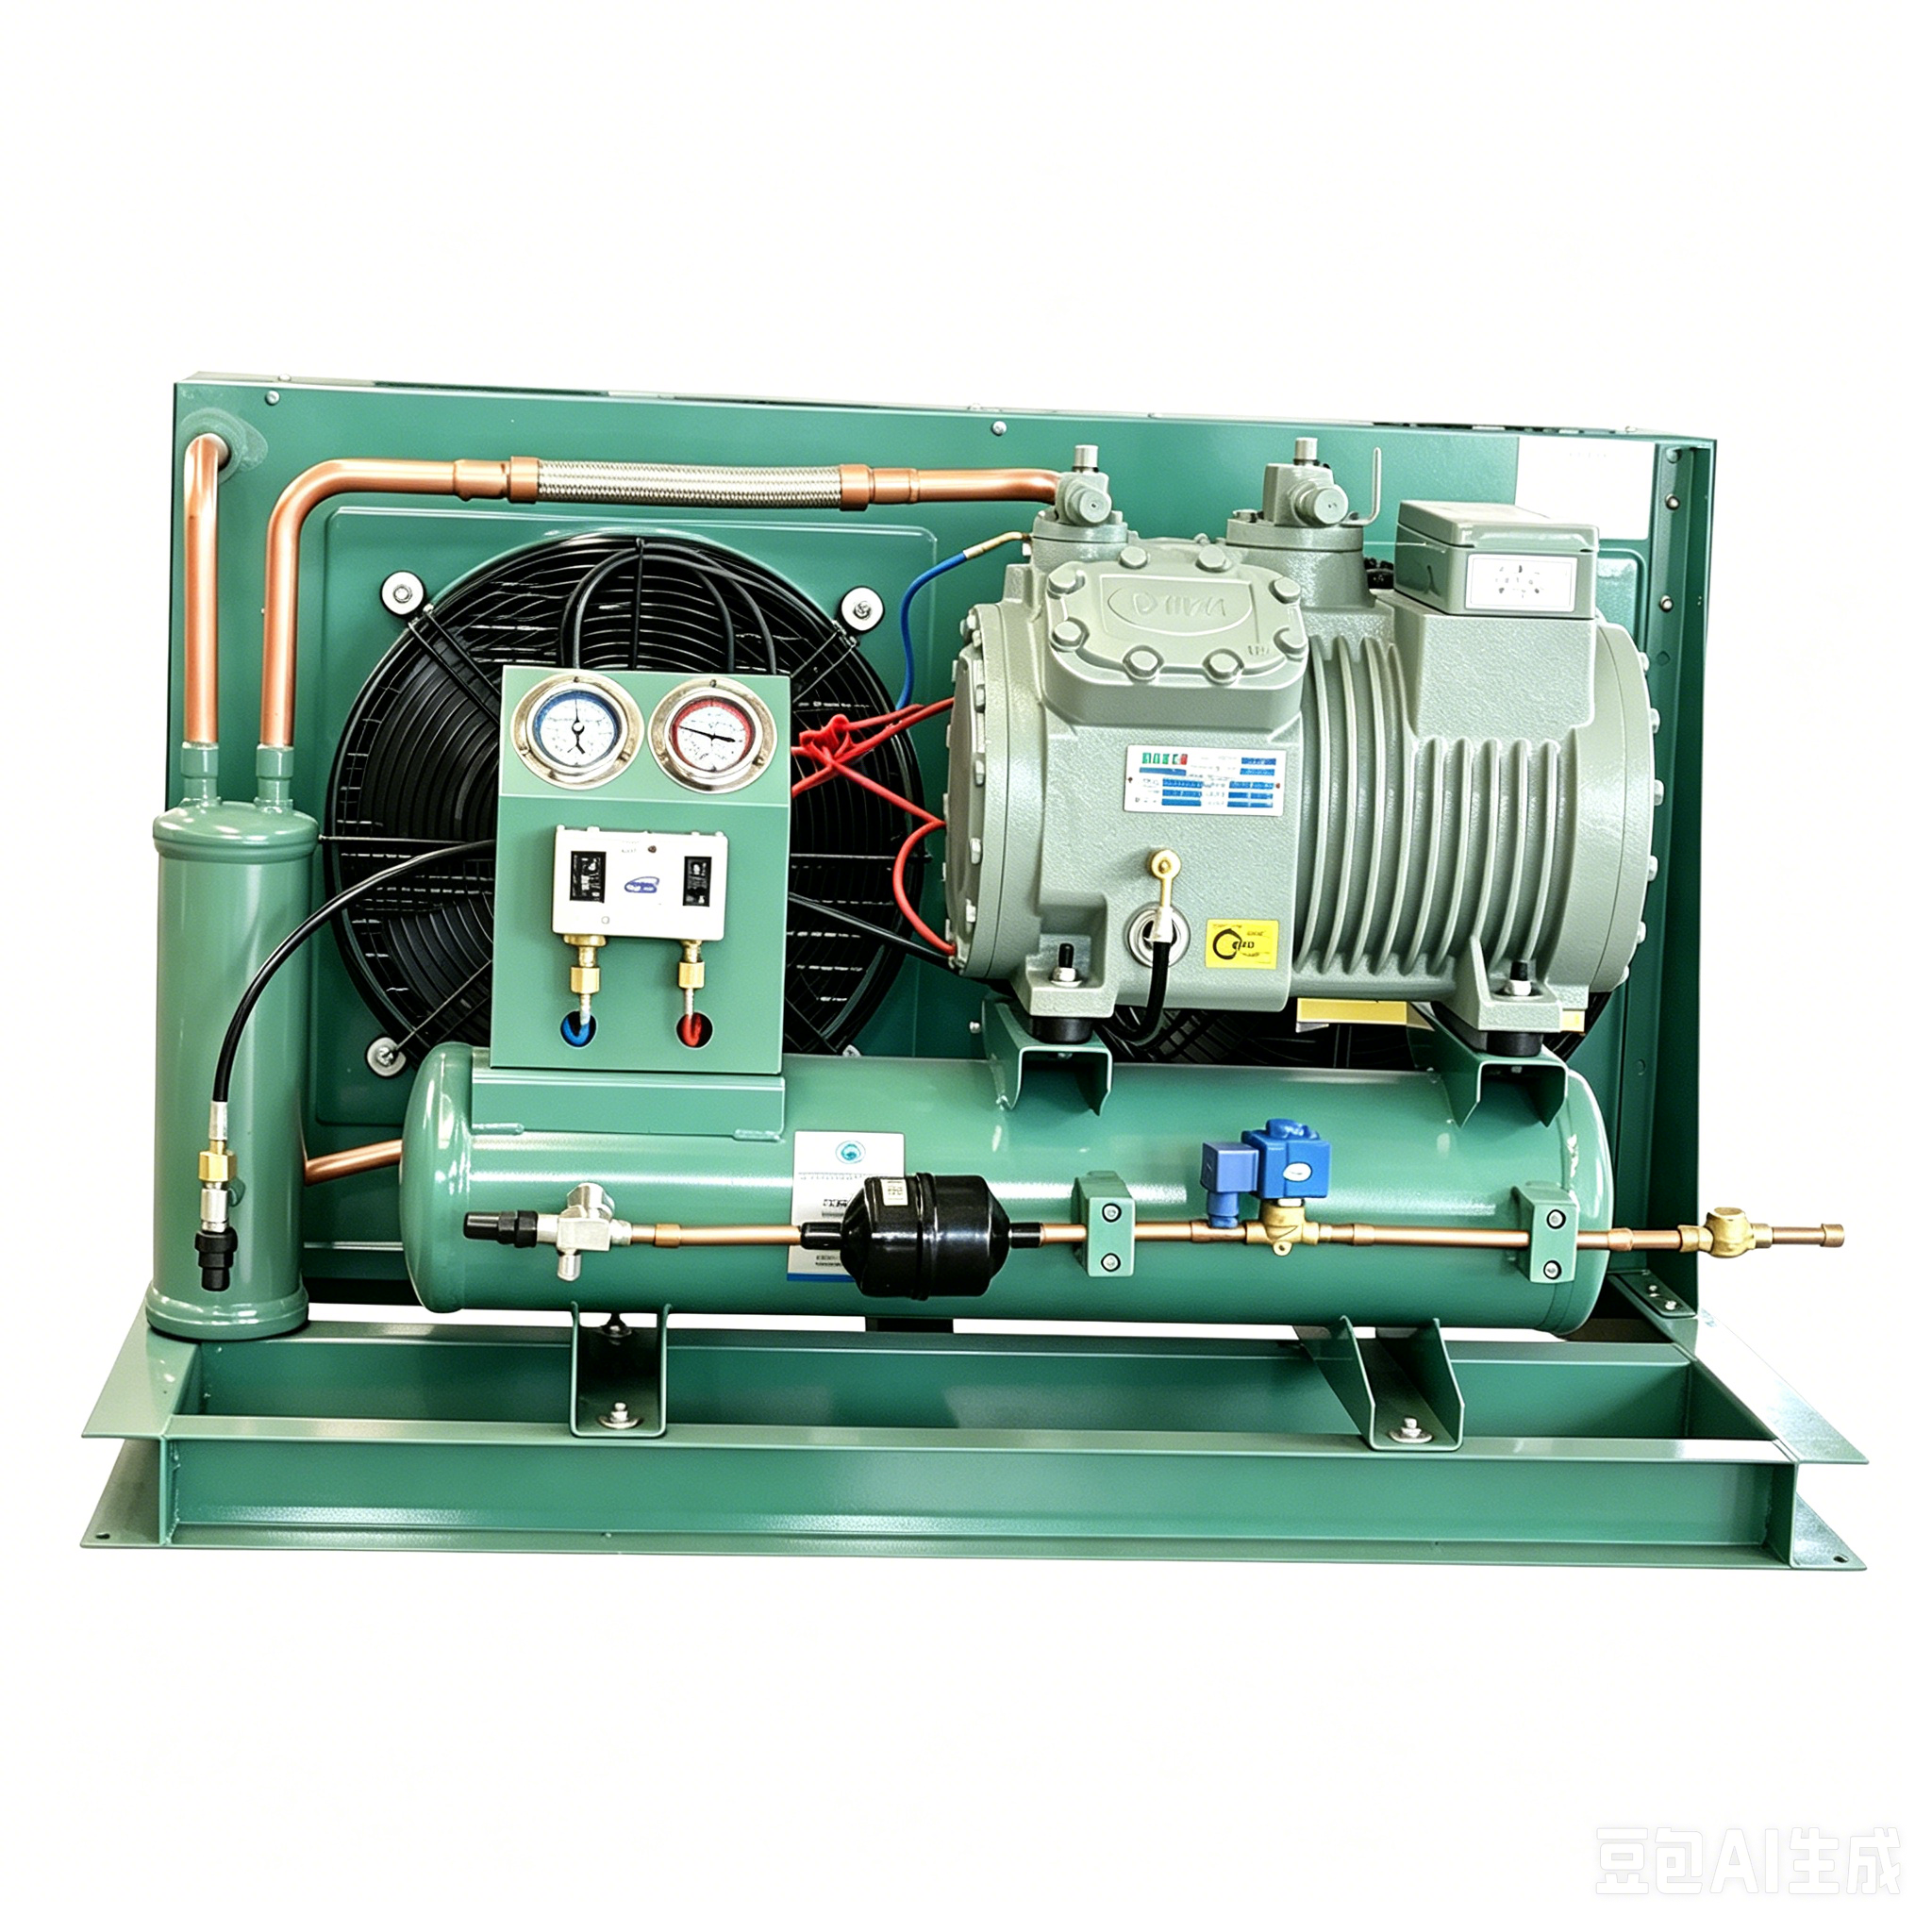
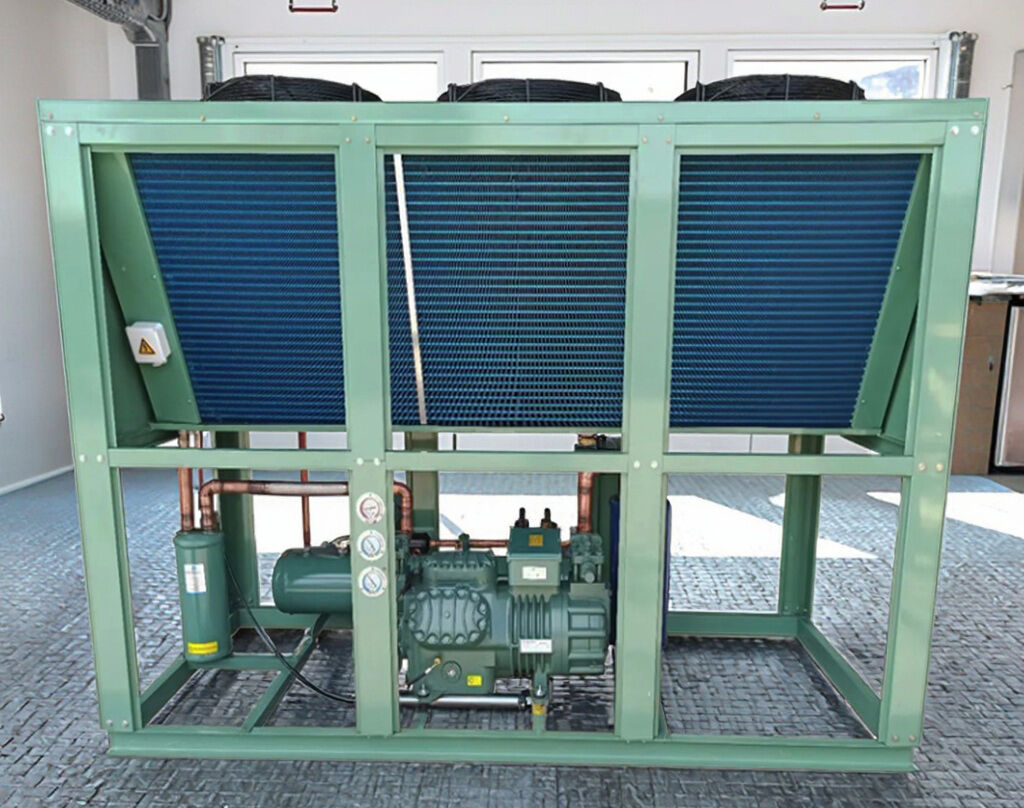
The heavy duty semi hermetic condensing unit represents a robust refrigeration solution engineered for demanding commercial and industrial cooling applications. This advanced system combines a semi-hermetic compressor with essential components including a condenser coil, receiver tank, and control systems, all mounted on a durable frame. The heavy duty semi hermetic condensing unit delivers reliable performance in environments requiring continuous operation and high cooling capacities. Its semi-hermetic design allows for serviceability while maintaining protection against contaminants, making it ideal for cold storage facilities, food processing plants, and large-scale commercial refrigeration systems. The unit operates by compressing refrigerant gas, condensing it into liquid form through heat exchange, and circulating it efficiently throughout the cooling system. Built with industrial-grade materials and precision engineering, the heavy duty semi hermetic condensing unit withstands harsh operating conditions while maintaining consistent temperature control. These systems typically feature copper tube aluminum fin condensers optimized for heat dissipation, along with advanced motor protection and control mechanisms. The modular construction facilitates installation and maintenance, while the robust framework ensures stability during operation. Available in various capacities and configurations, the heavy duty semi hermetic condensing unit can be customized to meet specific cooling requirements, accommodating different refrigerants and operating temperatures. This versatility makes it an essential component for businesses requiring dependable refrigeration performance with long-term operational efficiency and reduced downtime.

 EN