High Quality H Type Condensing Unit Solutions

All Categories

high quality h type condensing unit

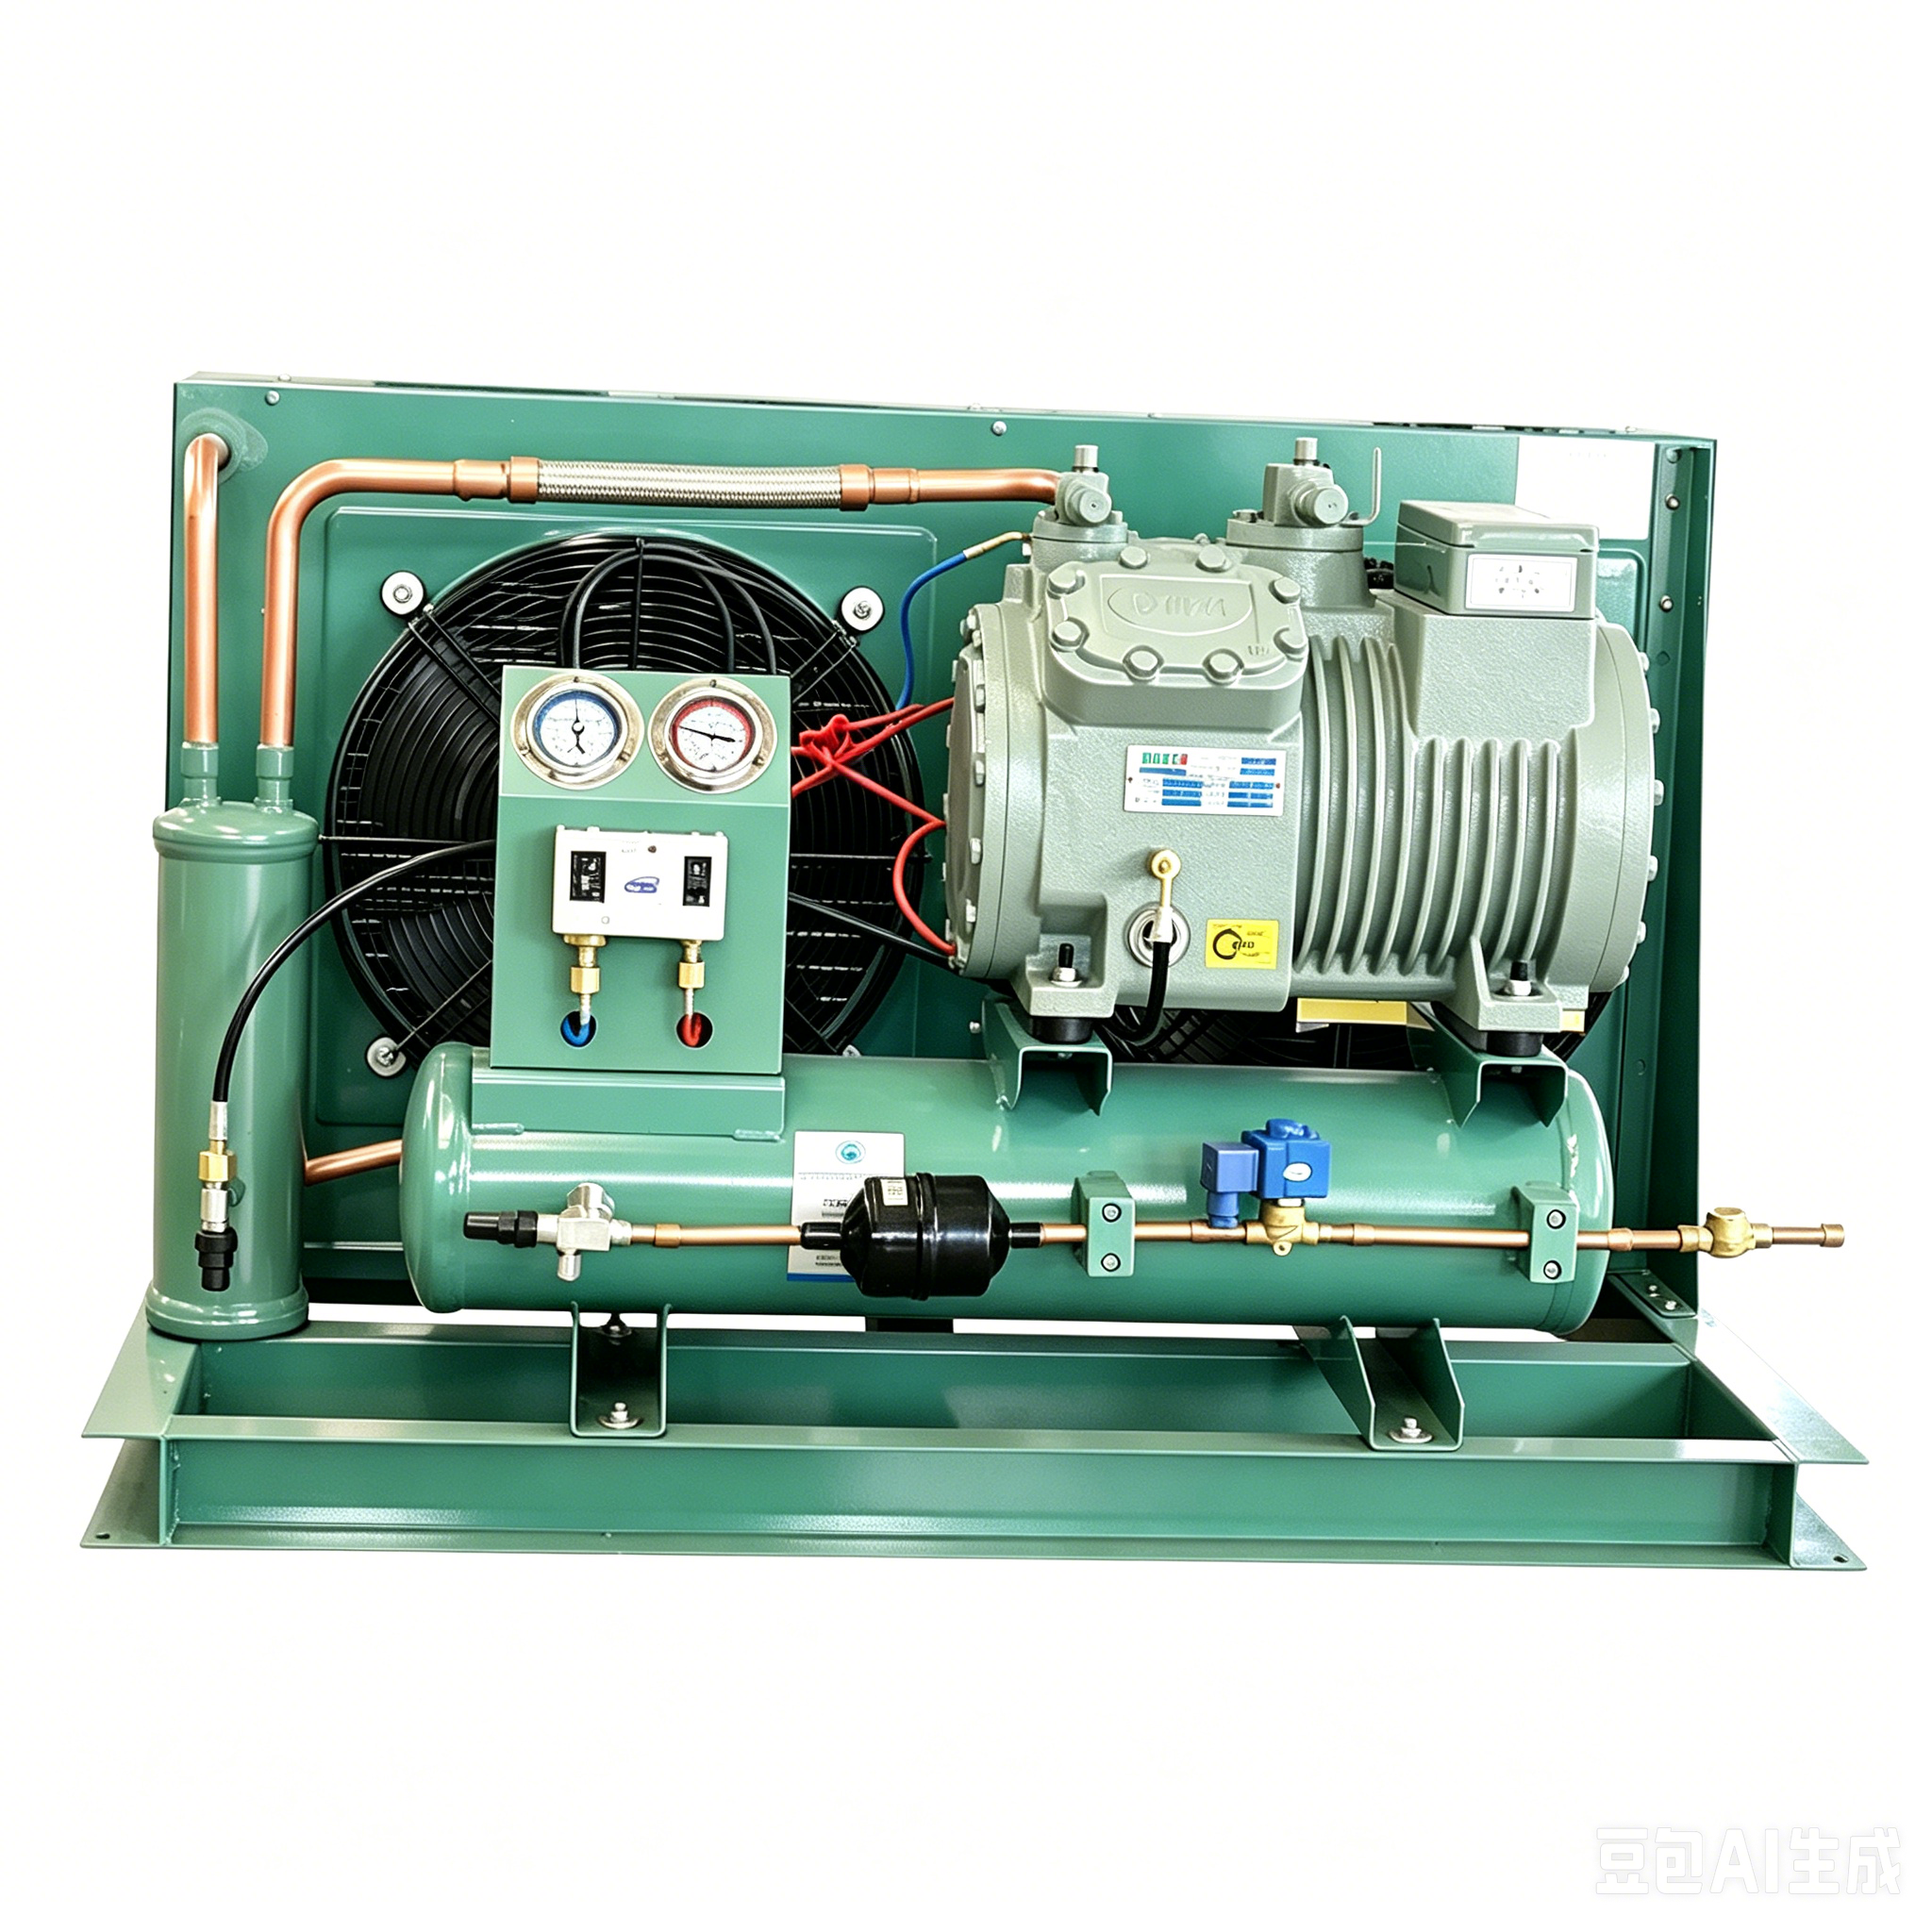
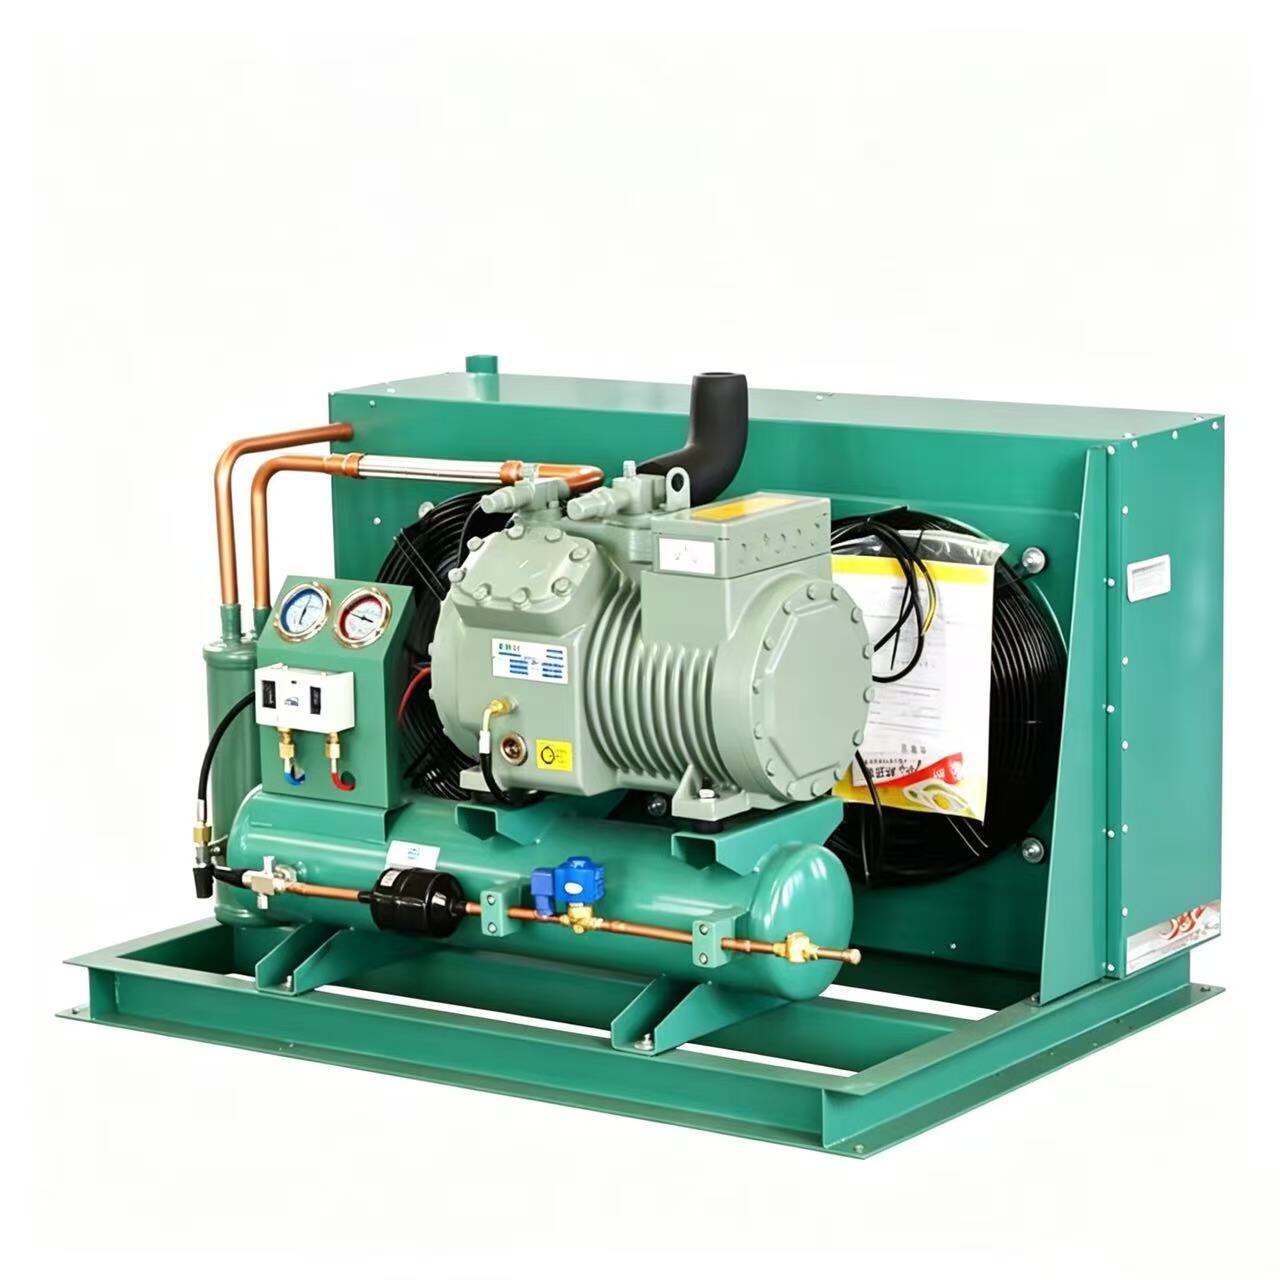
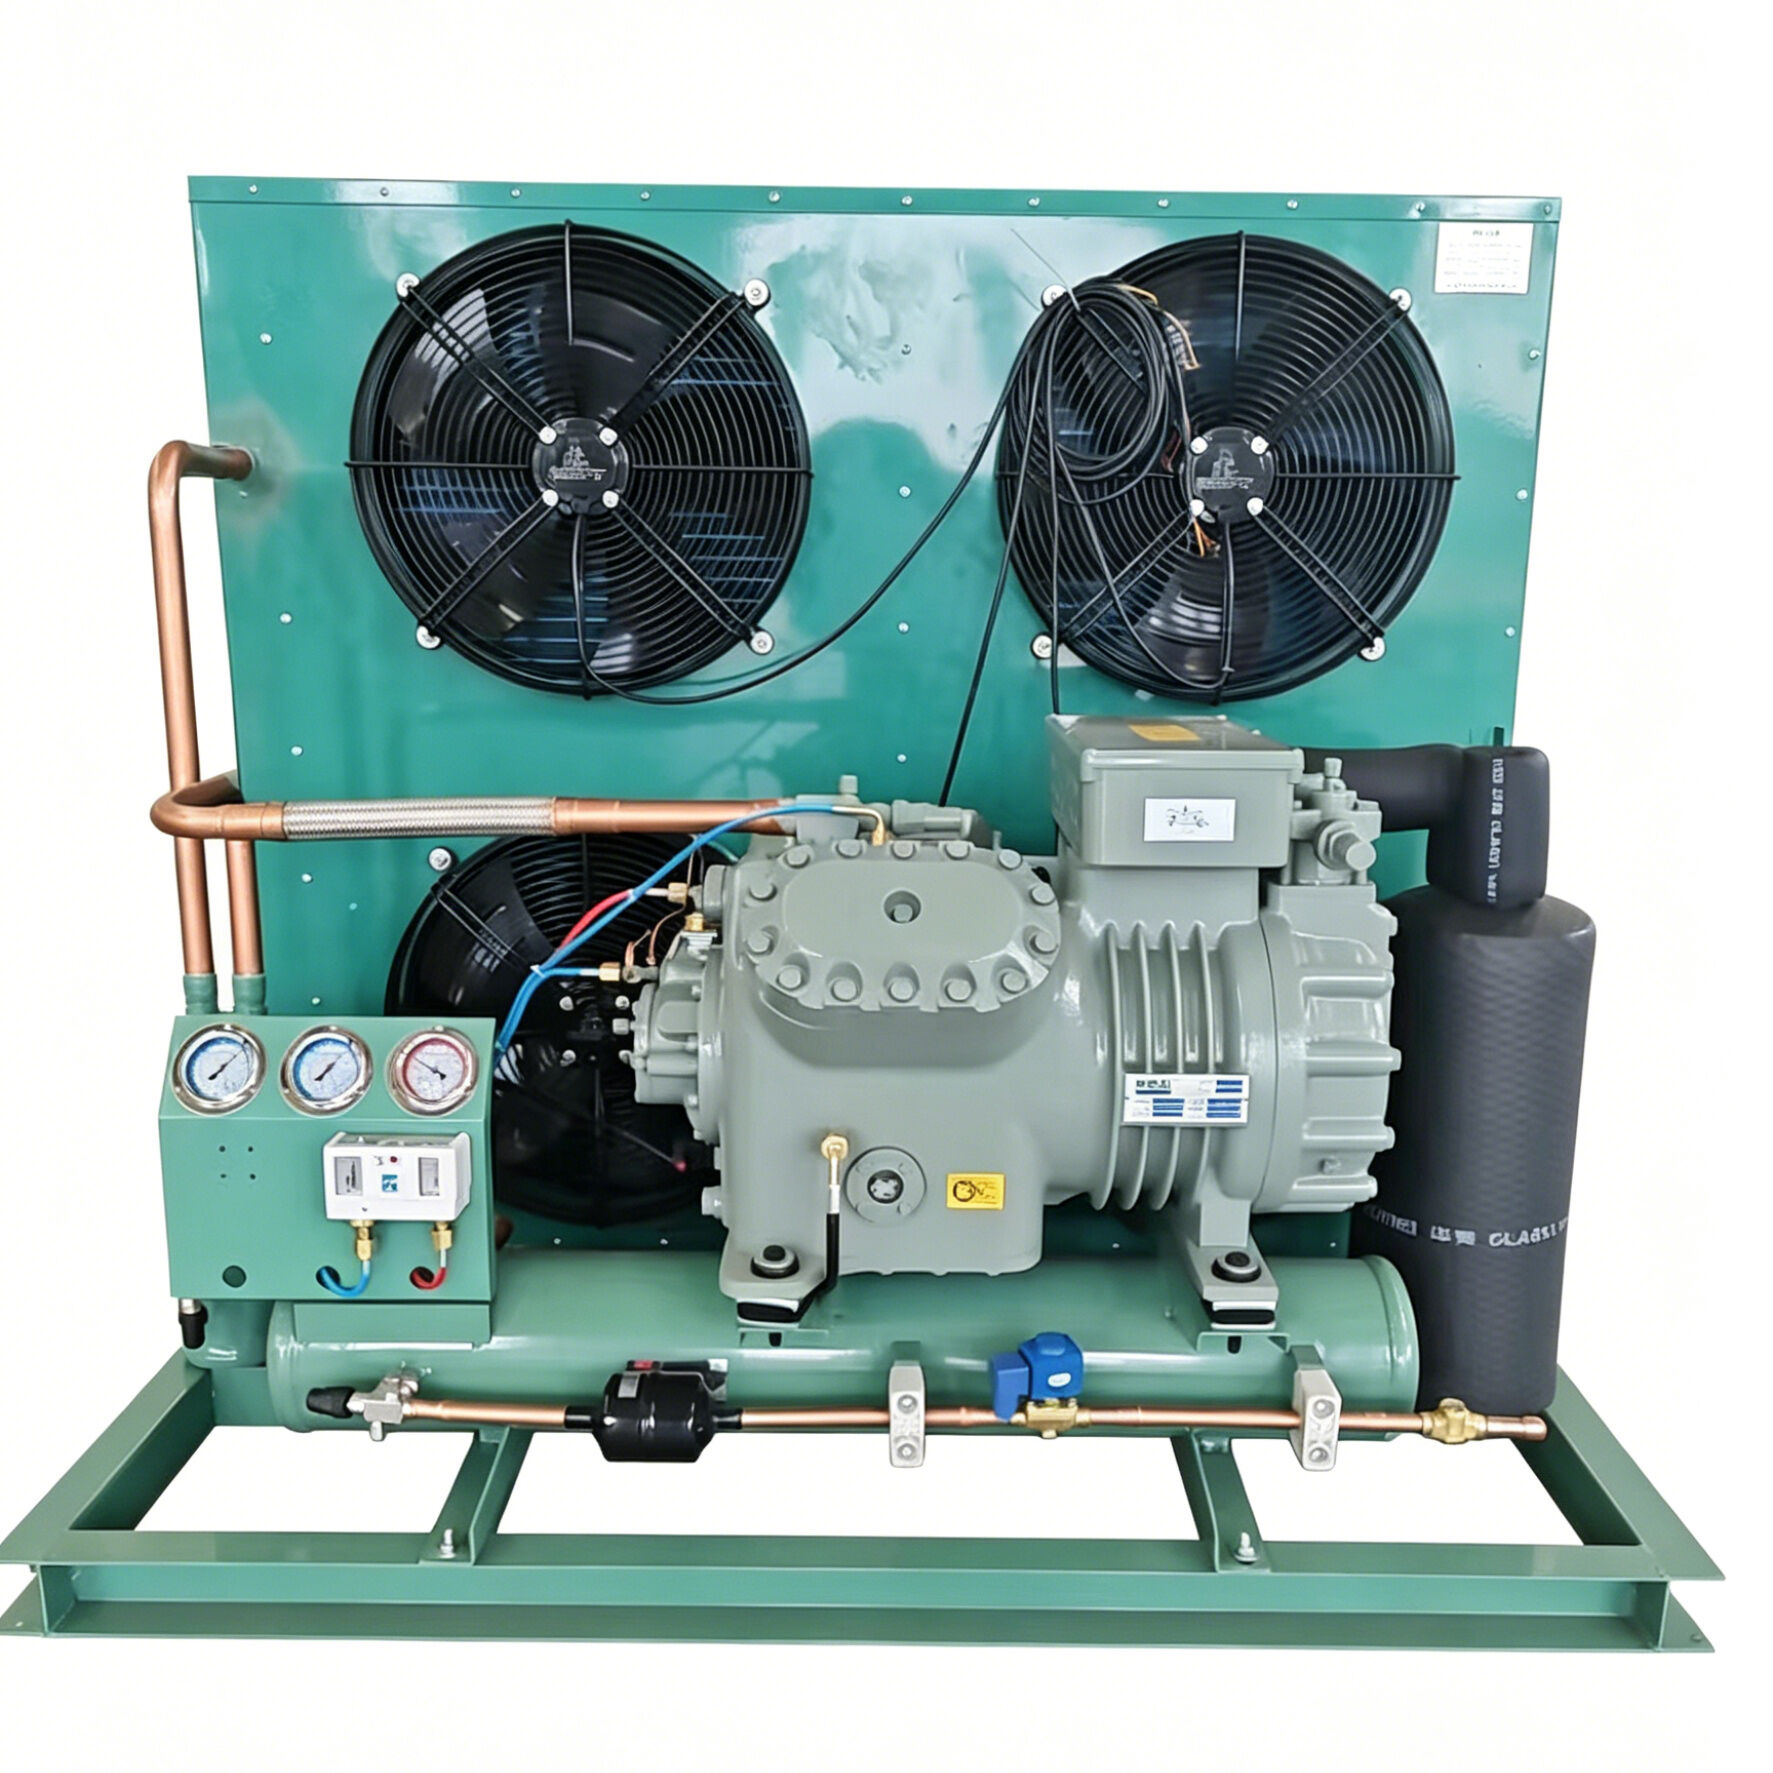
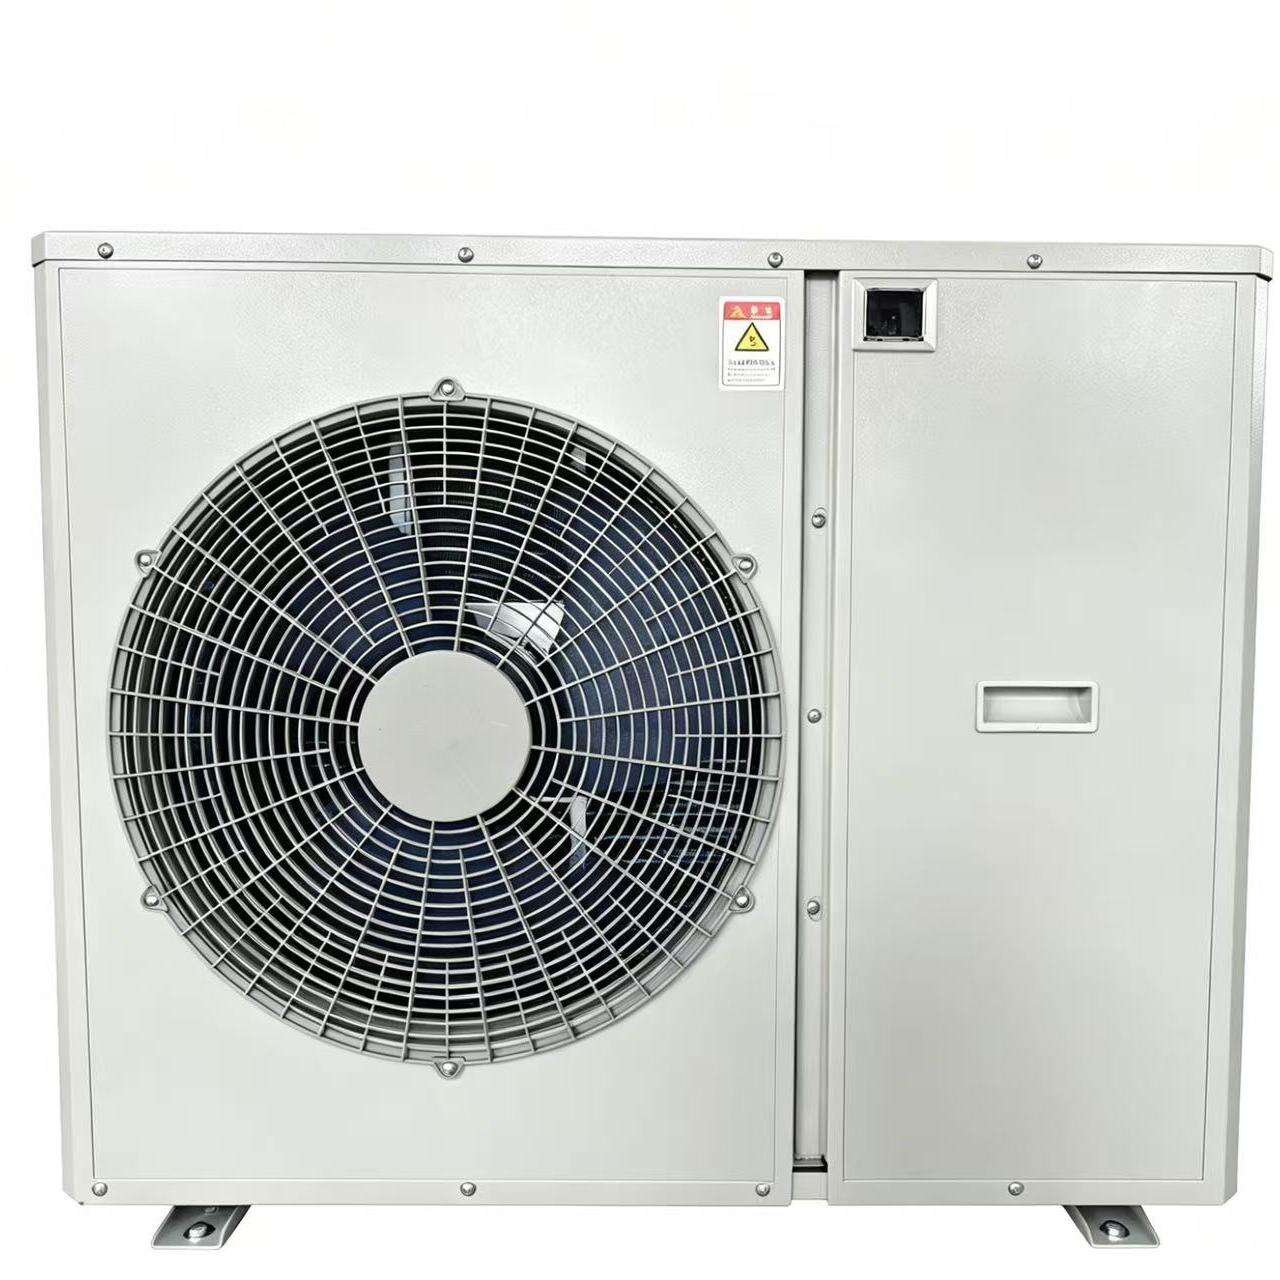
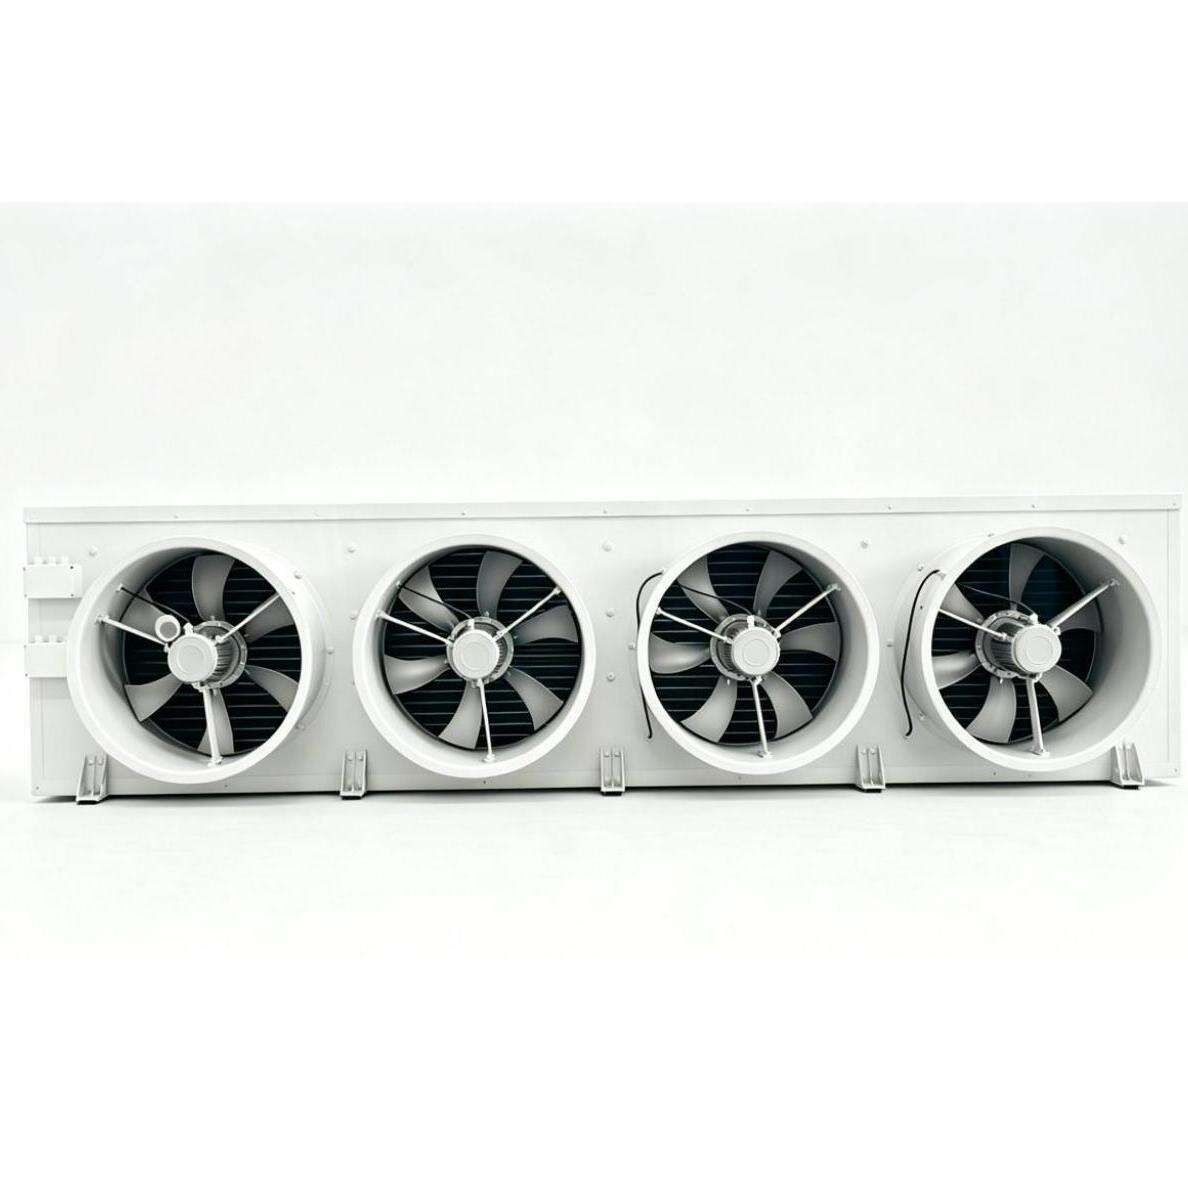
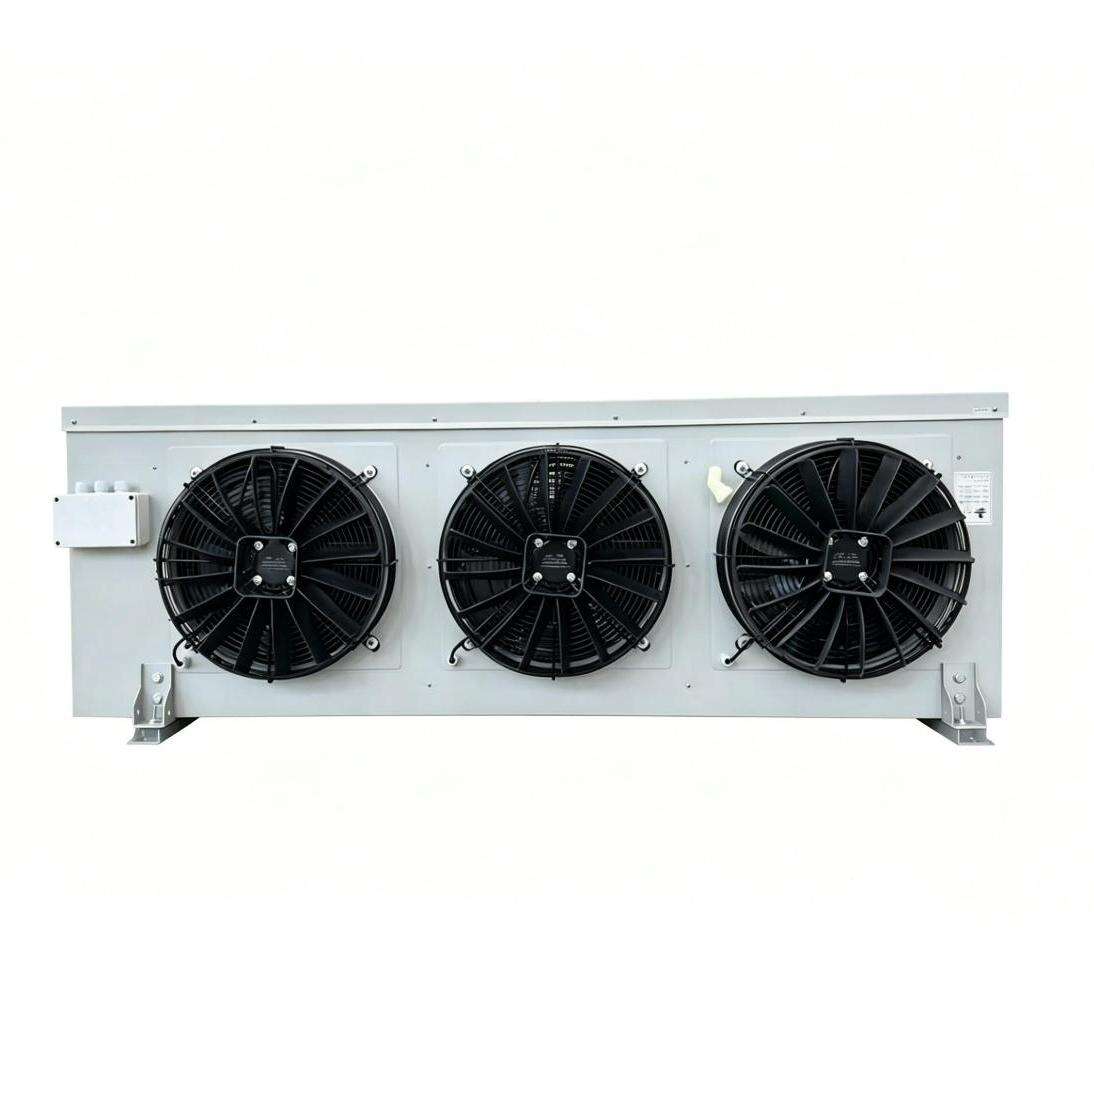
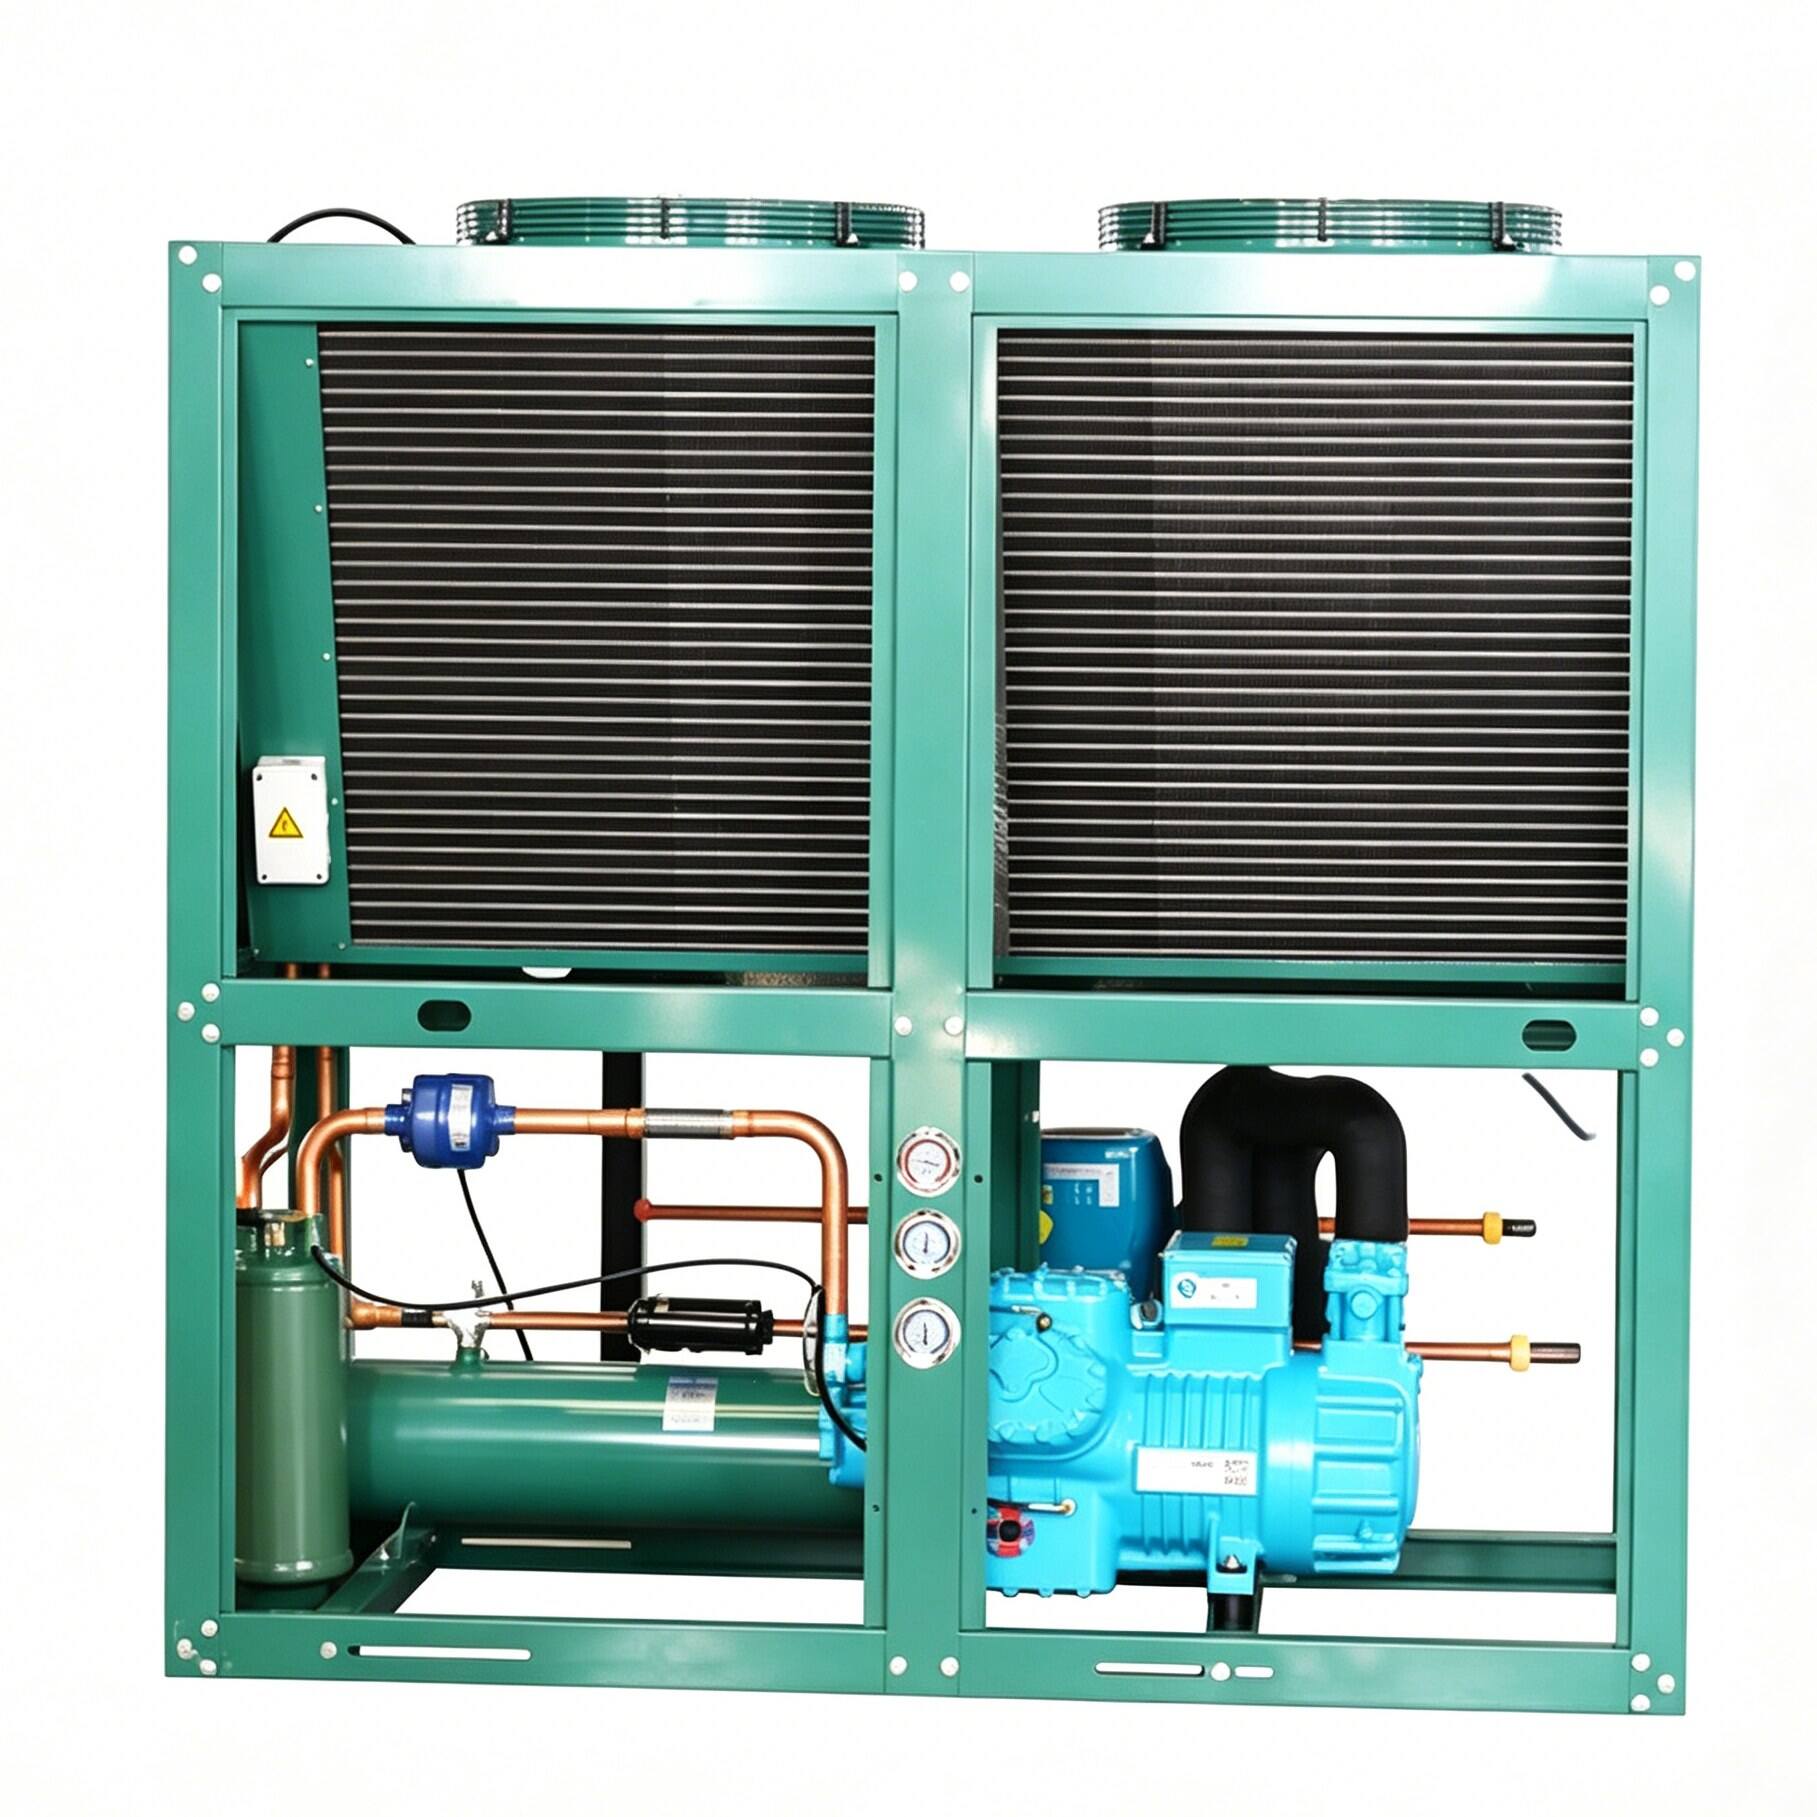
The high quality h type condensing unit represents an advanced refrigeration solution designed to deliver superior cooling performance across commercial and industrial applications. This sophisticated system combines a hermetically sealed compressor, fin-and-tube condenser coil, receiver tank, and precision controls into a compact, pre-assembled configuration. The H-type design features a distinctive horizontal layout that optimizes airflow dynamics while minimizing the installation footprint, making it ideal for space-constrained environments. Engineered with premium components and rigorous manufacturing standards, the high quality h type condensing unit ensures reliable operation in demanding conditions. Its primary function centers on heat rejection, where refrigerant vapor from evaporators is compressed, condensed back to liquid state, and circulated through cooling systems efficiently. Technological features include multi-speed fan motors that adjust cooling capacity based on ambient temperature fluctuations, corrosion-resistant copper tubing with aluminum fins for enhanced heat transfer, and advanced motor protection devices that prevent electrical failures. The unit operates seamlessly with various refrigerants including R404A, R134a, and eco-friendly alternatives, supporting sustainability initiatives. Applications span cold storage warehouses, supermarket refrigeration systems, food processing facilities, pharmaceutical storage, and industrial process cooling. The high quality h type condensing unit excels in both new installations and retrofit projects, offering versatility through customizable configurations that accommodate different cooling loads from small retail displays to large-scale cold chain operations, ensuring consistent temperature control and operational efficiency.
New Product Recommendations

Investing in a high quality h type condensing unit delivers tangible operational and financial benefits that directly impact your bottom line. First, energy efficiency stands as a primary advantage, with optimized compressor technology and intelligent fan control reducing electricity consumption by up to thirty percent compared to conventional units, translating to significant cost savings over the product lifecycle. The robust construction using premium materials ensures extended service life, often exceeding fifteen years with proper maintenance, which reduces replacement frequency and capital expenditure. Installation simplicity represents another practical benefit, as the pre-assembled design eliminates complex on-site assembly, cutting installation time by half and reducing labor costs substantially. The compact horizontal configuration of the high quality h type condensing unit allows flexible placement options, whether mounted on rooftops, exterior walls, or ground-level platforms, maximizing usable interior space for revenue-generating activities. Operational reliability is enhanced through built-in protection systems including high-pressure cutouts, thermal overload protection, and vibration dampening mounts that minimize downtime and emergency repair expenses. Maintenance accessibility is thoughtfully designed with service panels positioned for easy inspection and component replacement, reducing technician time on-site and associated costs. The unit operates quietly due to sound-dampening features, making it suitable for noise-sensitive environments like urban retail locations or residential proximity installations. Adaptability across temperature ranges means the high quality h type condensing unit performs consistently whether in tropical heat or temperate climates, providing application suitability for global markets. Furthermore, compatibility with modern monitoring systems enables remote diagnostics and performance tracking, empowering facility managers with data-driven insights for proactive maintenance scheduling and optimal performance management.

Latest News

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

28

Feb

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

View More
Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

28

Feb

Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

View More
Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

28

Feb

Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

high quality h type condensing unit

Advanced Heat Exchange Technology

Advanced Heat Exchange Technology

The high quality h type condensing unit incorporates state-of-the-art heat exchange technology that maximizes thermal transfer efficiency while minimizing energy consumption. The condenser coil features precisely engineered copper tubing with optimized diameter and wall thickness, wound through high-density aluminum fins that are mechanically bonded for superior heat conduction. This configuration creates an expanded surface area that accelerates heat dissipation from refrigerant to ambient air, reducing condensing temperature and pressure. The result is improved compressor efficiency and reduced electrical demand throughout operation. Advanced computational fluid dynamics guided the fin spacing and pattern design, ensuring optimal airflow distribution across the entire coil surface without dead zones or turbulence that would compromise performance. The axial fan system is strategically positioned to draw air uniformly through the condenser, with blade geometry engineered to move maximum air volume at minimal noise levels. This sophisticated heat exchange design enables the high quality h type condensing unit to maintain stable performance even during peak ambient temperature conditions, preventing system overload and ensuring consistent refrigeration capacity when your business needs it most.
Intelligent Control and Monitoring Capabilities

Intelligent Control and Monitoring Capabilities

Modern refrigeration demands smart technology, and the high quality h type condensing unit delivers through integrated intelligent control systems that optimize performance automatically. The microprocessor-based controller continuously monitors critical parameters including suction pressure, discharge pressure, refrigerant temperature, and ambient conditions, making real-time adjustments to fan speed and compressor operation. This dynamic response maintains optimal efficiency across varying load conditions, preventing energy waste during low-demand periods while ensuring adequate capacity during peak requirements. Digital temperature sensors provide precision feedback with accuracy within half a degree, enabling tight temperature control essential for sensitive products. The control system includes programmable defrost cycles, automatic capacity staging for multi-compressor configurations, and comprehensive fault diagnostics that identify issues before they cause system failure. Communication protocols allow integration with building management systems, enabling facility-wide monitoring from centralized control rooms. Operators receive instant alerts about abnormal conditions via multiple channels, facilitating rapid response that minimizes product loss and downtime. Historical data logging captures performance trends, supporting predictive maintenance strategies and warranty compliance documentation. This intelligent approach transforms the high quality h type condensing unit from a simple cooling device into a strategic asset that actively contributes to operational excellence.
Durable Construction for Long-Term Reliability

Durable Construction for Long-Term Reliability

Exceptional durability distinguishes the high quality h type condensing unit from economy alternatives, with construction quality that withstands harsh operating environments year after year. The frame utilizes heavy-gauge galvanized steel with powder-coat finish that resists corrosion from moisture, salt air, and chemical exposure common in industrial settings. All fasteners are stainless steel, eliminating rust-related failures that plague lesser units. The compressor, selected from tier-one manufacturers, features reinforced internal components and advanced lubrication systems that ensure reliable operation through millions of cycles. Electrical components are housed in weather-sealed enclosures rated for outdoor exposure, with conduit entries designed to prevent moisture ingress that causes short circuits and control failures. Refrigerant connections employ brazed joints rather than mechanical fittings, eliminating leak points that compromise system integrity. Vibration isolation mounts constructed from industrial-grade elastomers absorb compressor pulsations, protecting structural components and extending bearing life. The condenser coil receives a protective coating that prevents oxidation and maintains heat transfer efficiency throughout the service life. Quality assurance testing subjects every high quality h type condensing unit to rigorous performance verification before shipment, including leak testing, electrical safety checks, and operational run-in under load conditions, ensuring that only units meeting stringent standards reach customers.
High Quality H Type Condensing Unit Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
High Quality H Type Condensing Unit Solutions

Copyright © 2026 Ningbo Lucky Star Import & Export Co., Ltd. All rights reserved.  -  Privacy policy