Liquid Evaporator Systems: Efficient Solutions

All Categories

liquid evaporator

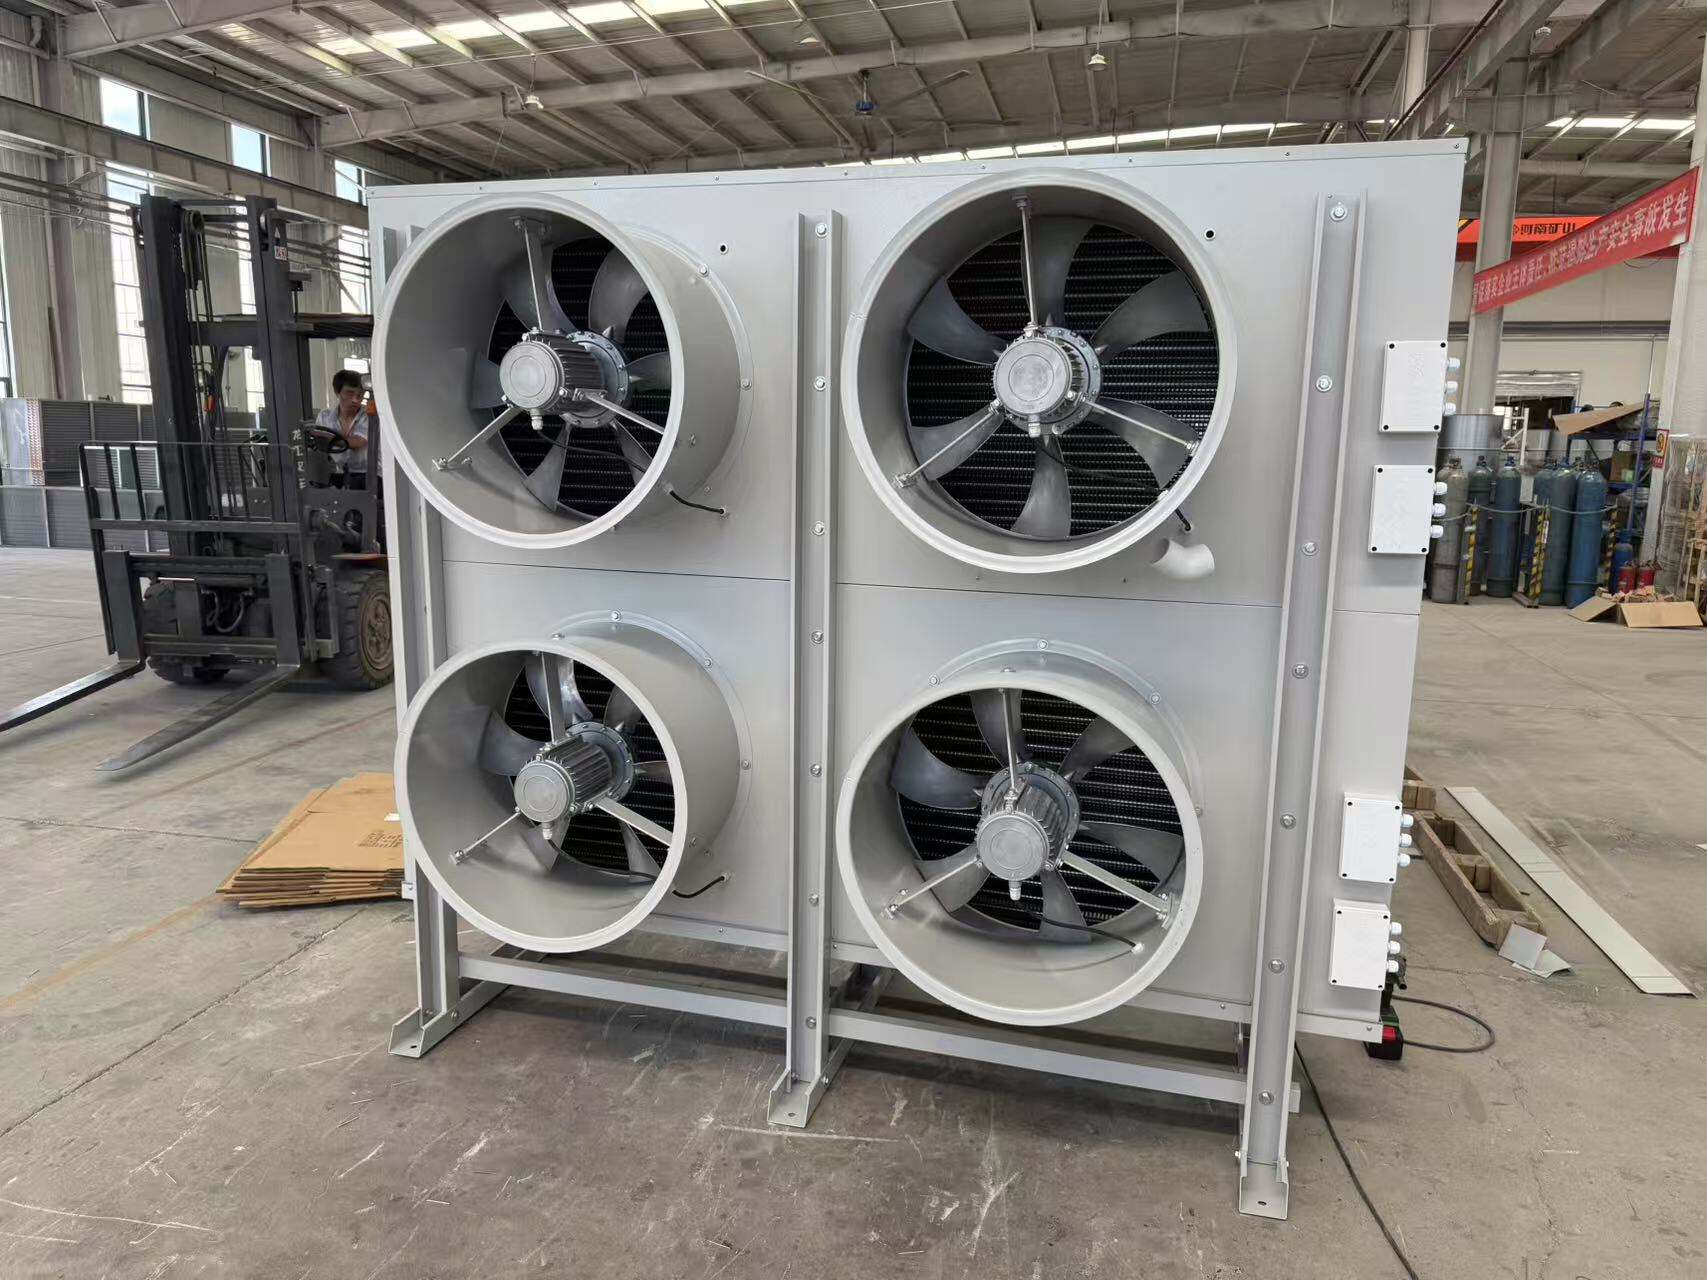
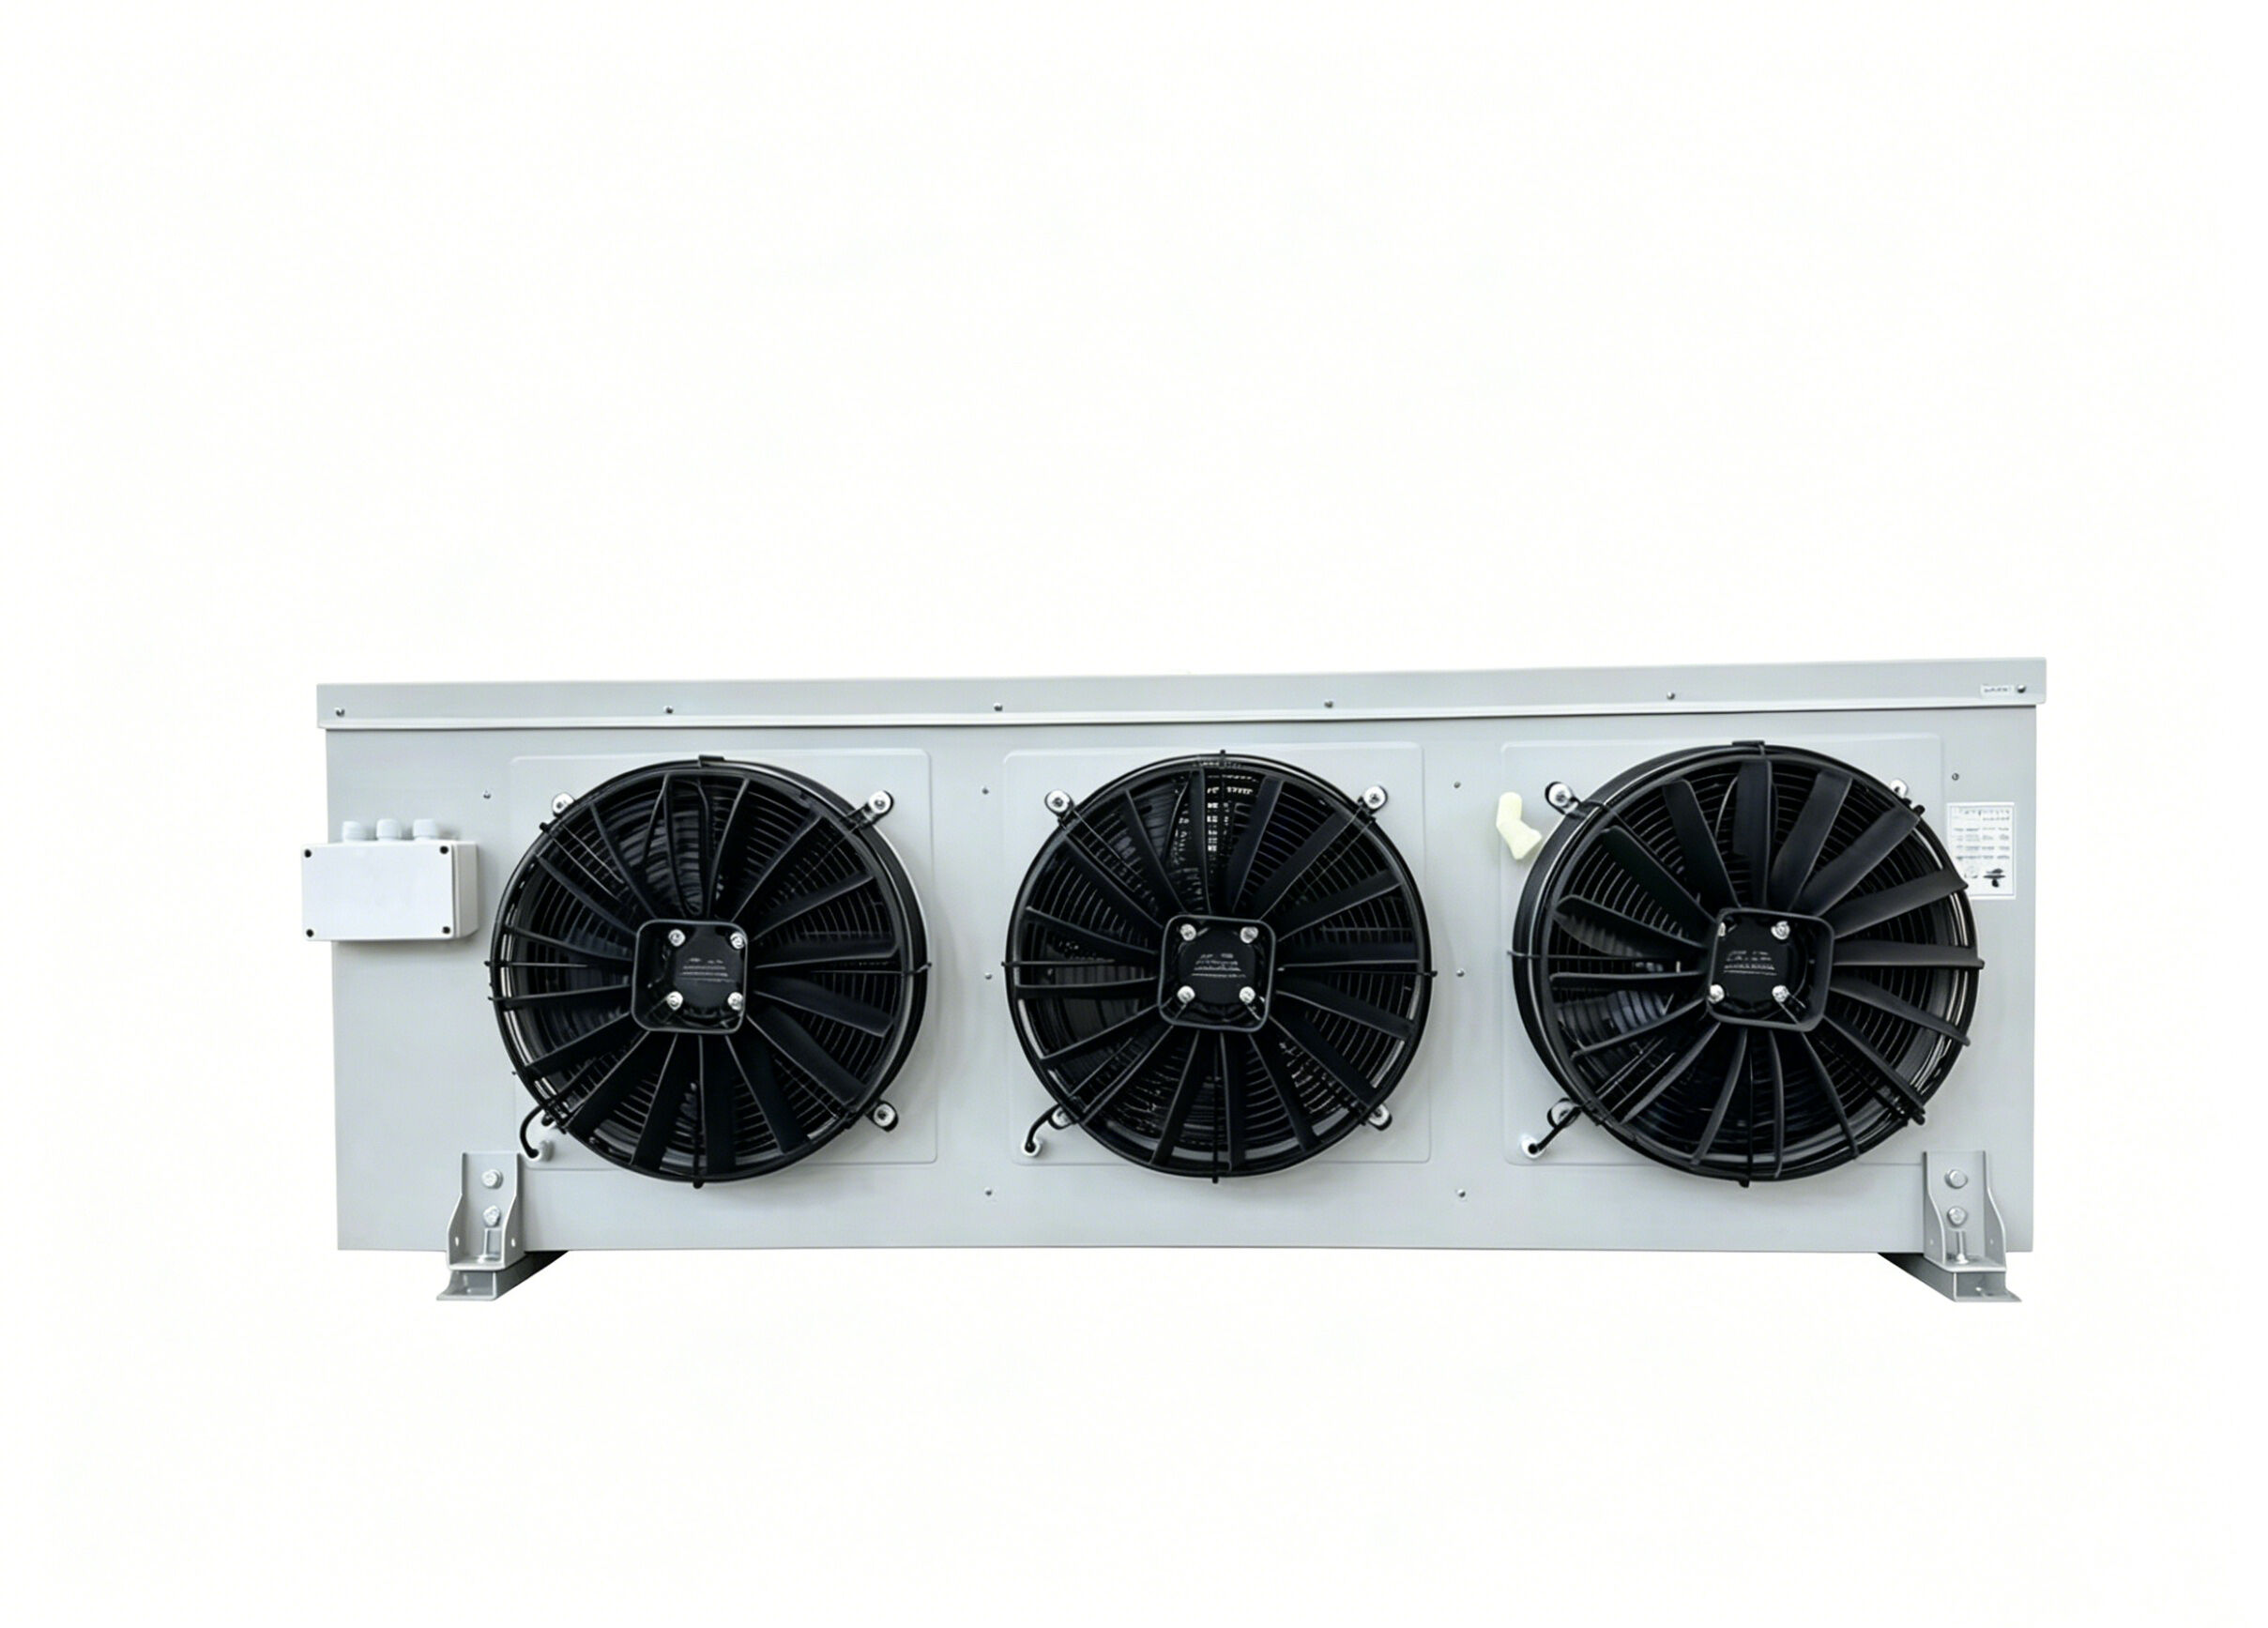
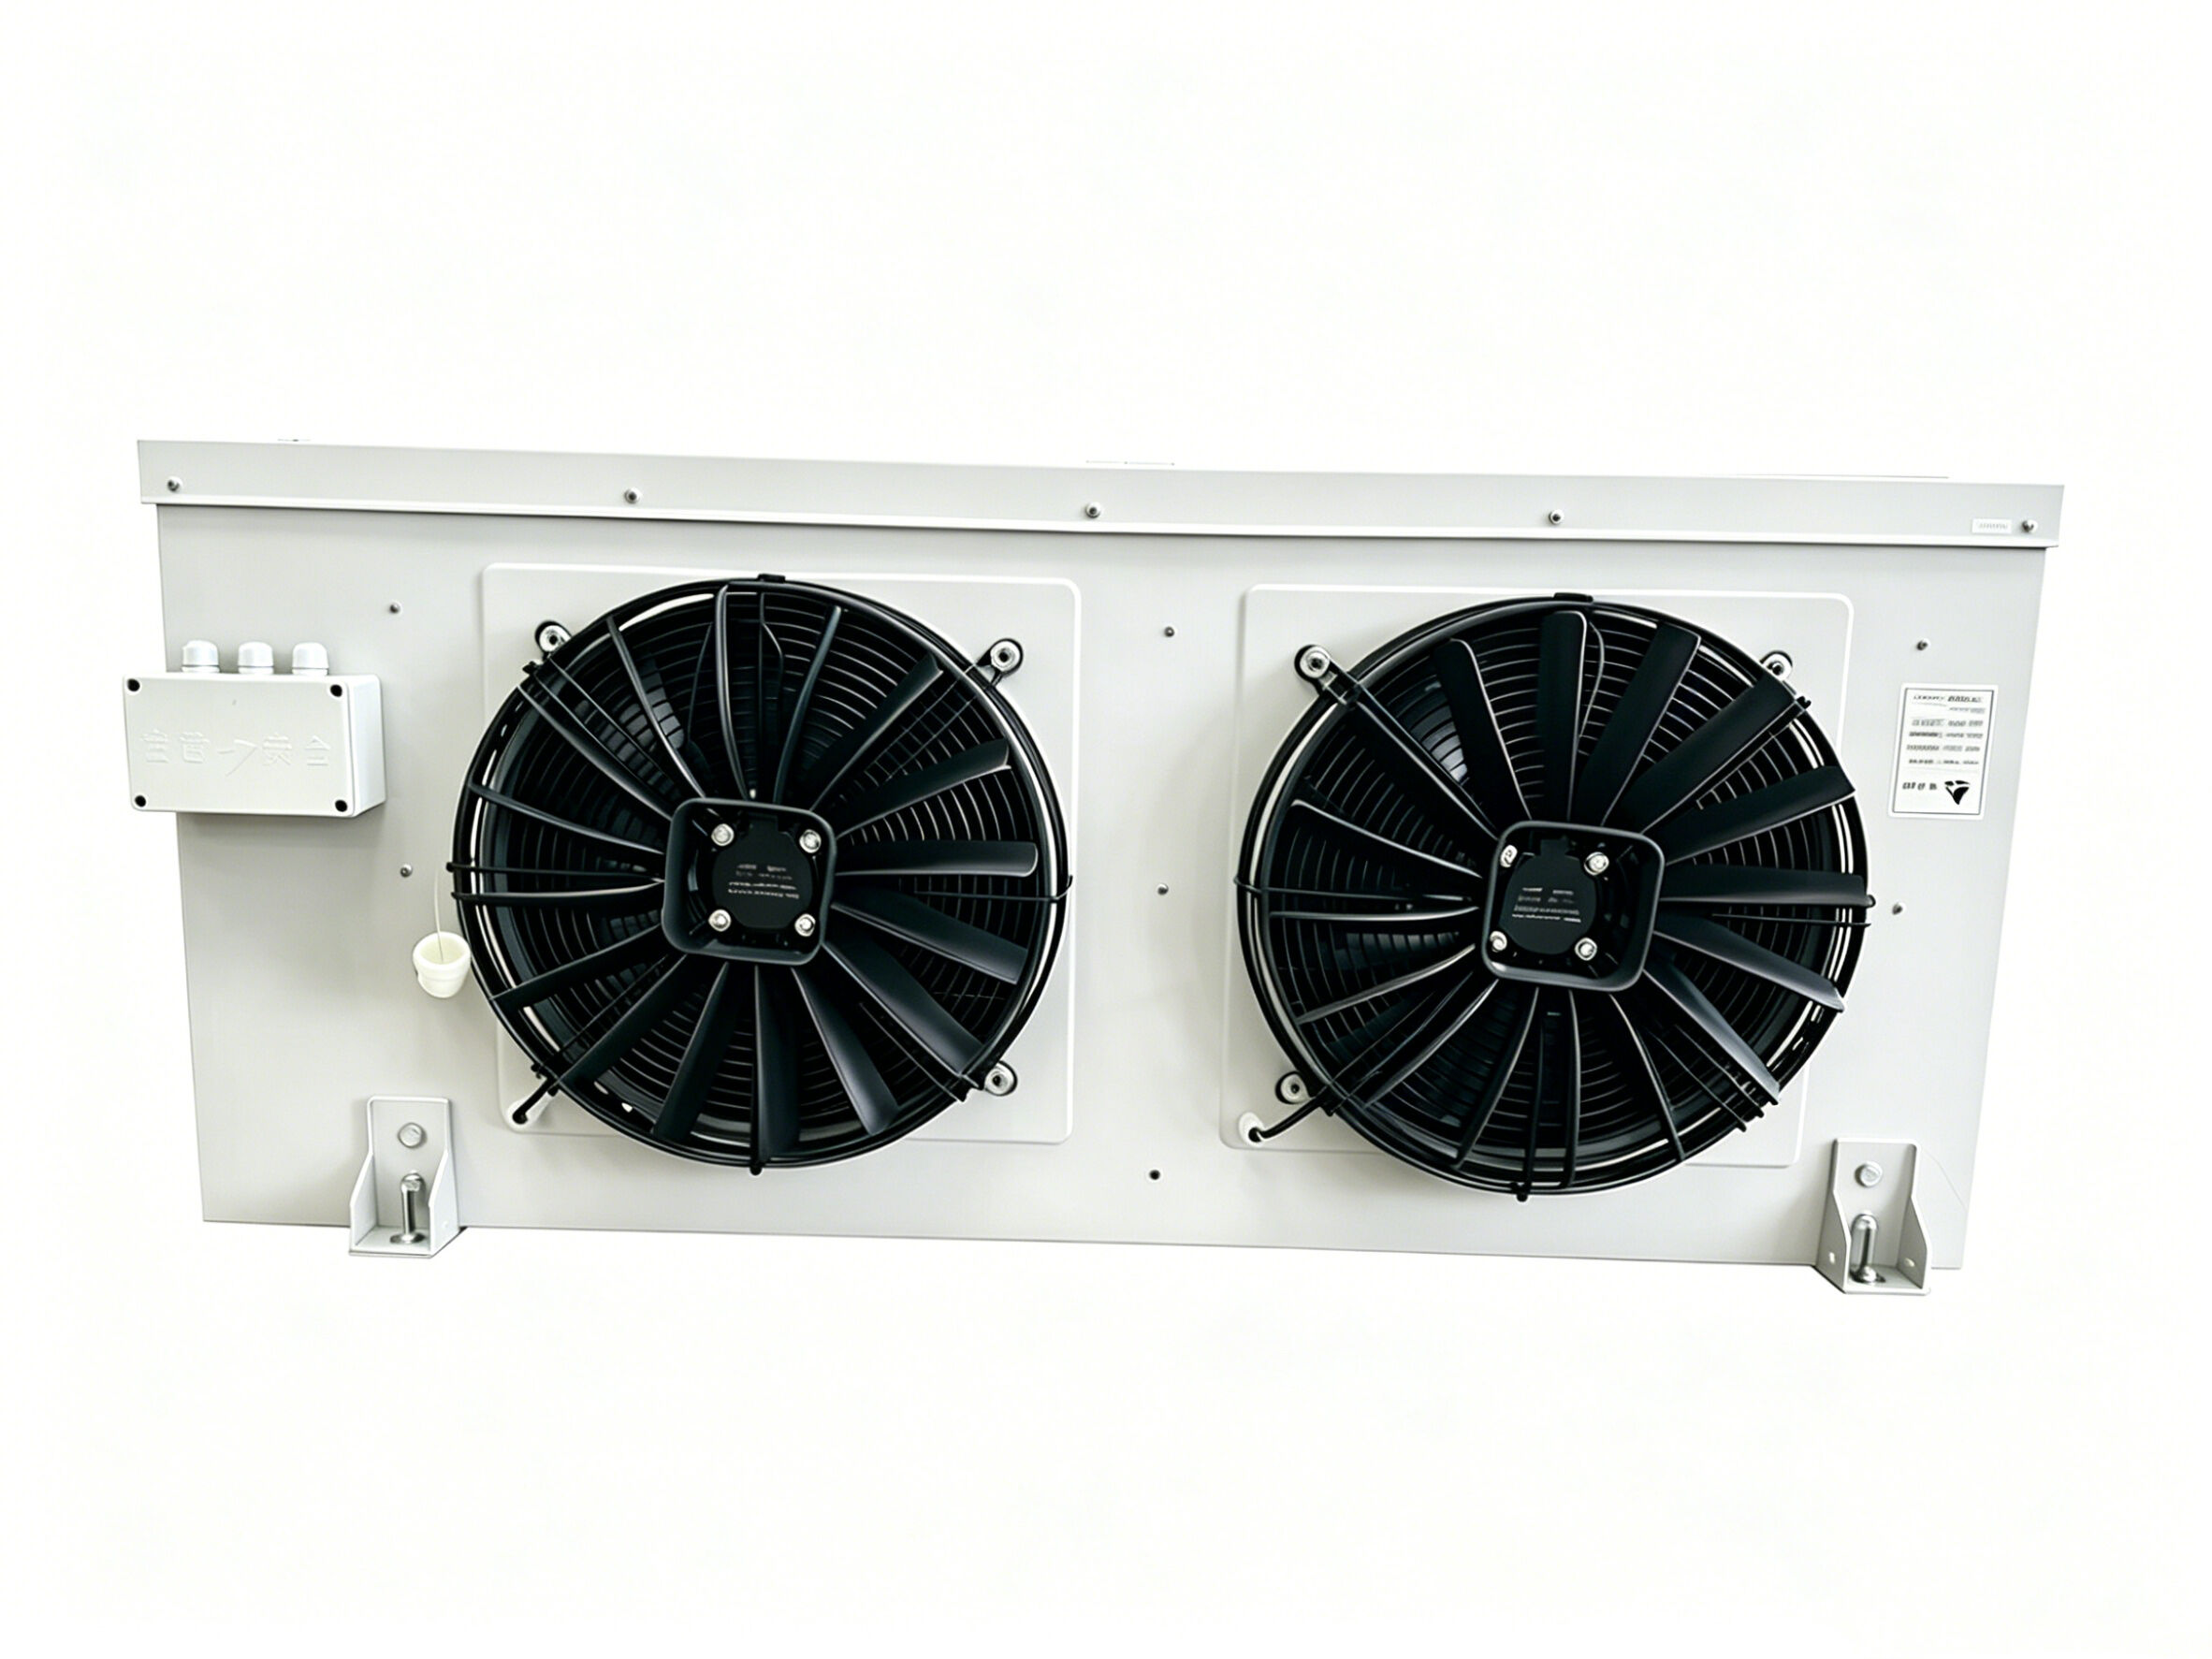
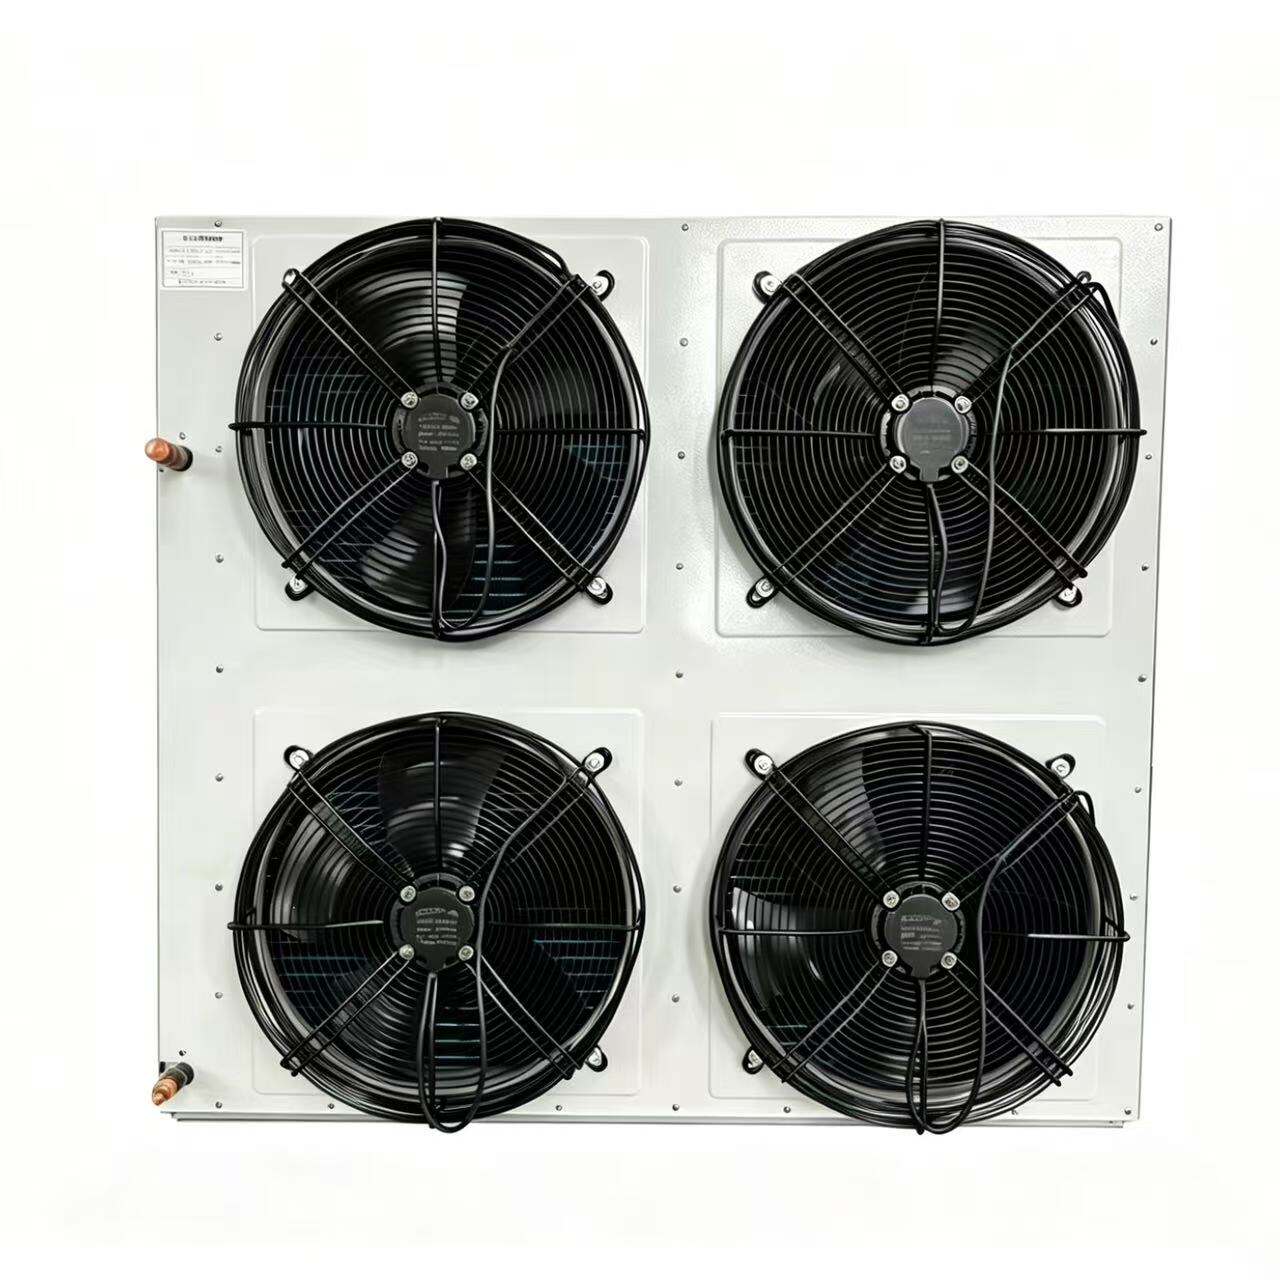
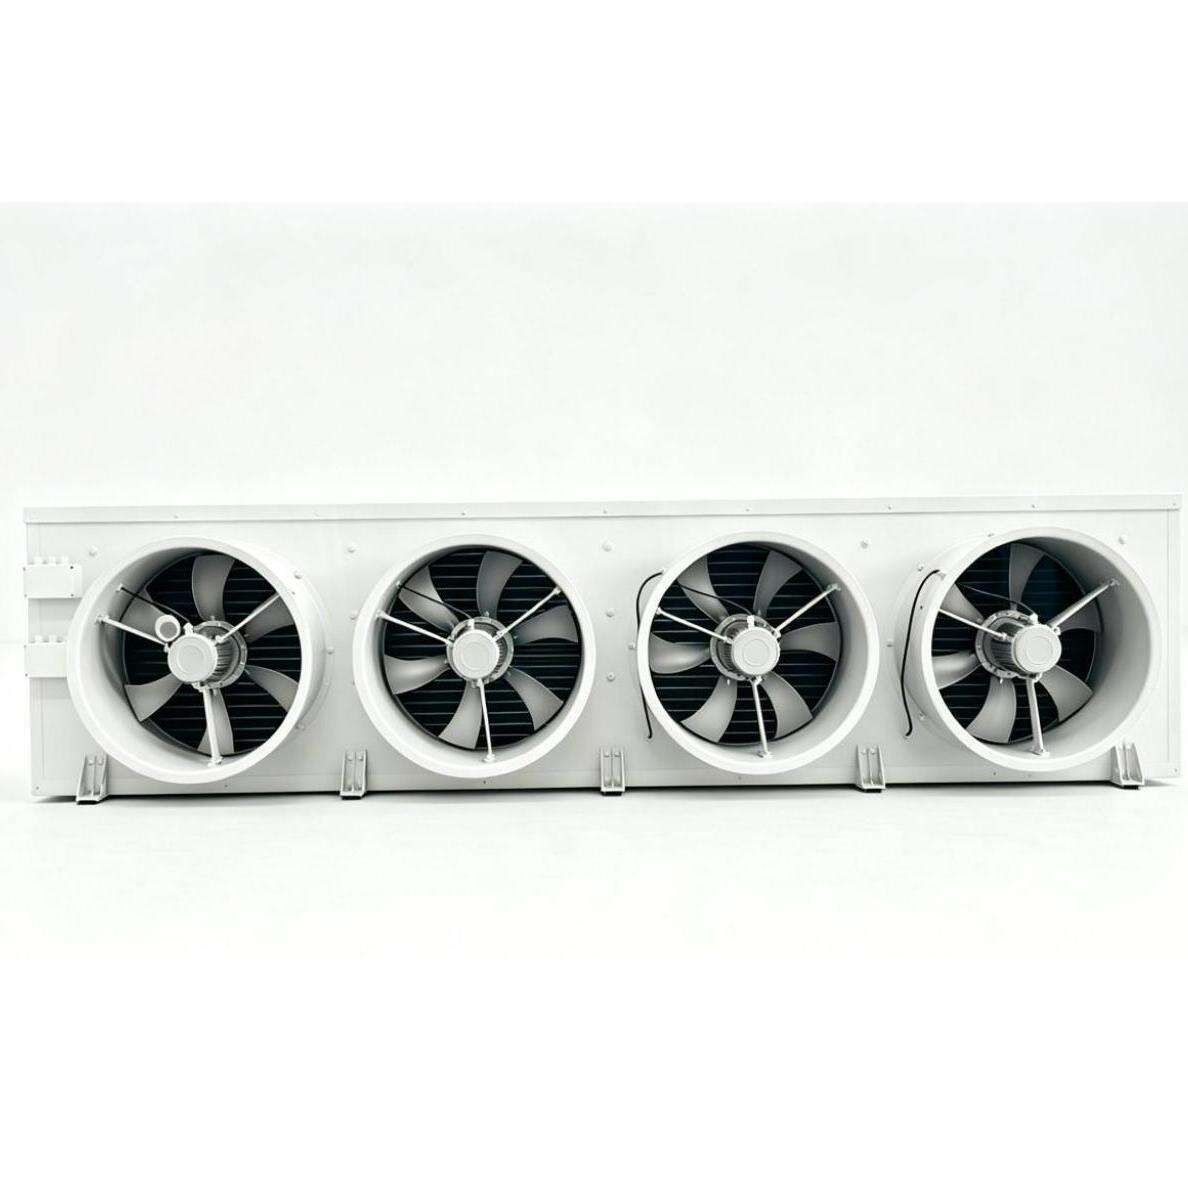
A liquid evaporator is an essential industrial device designed to convert liquid substances into vapor through controlled heating processes. This sophisticated equipment plays a critical role in numerous manufacturing and processing operations where concentration, purification, or separation of liquids is required. The liquid evaporator functions by applying thermal energy to liquid materials, causing them to vaporize while leaving behind concentrated residues or allowing for vapor collection and condensation. Modern liquid evaporator systems incorporate advanced heat transfer mechanisms, precise temperature controls, and energy-efficient designs to optimize performance across diverse applications. These systems are engineered with various configurations including falling film, rising film, forced circulation, and natural circulation models to accommodate different liquid properties and processing requirements. The technological features of a liquid evaporator encompass automated control systems, corrosion-resistant materials, efficient heat exchangers, and safety mechanisms that ensure reliable continuous operation. Applications span multiple industries including chemical processing, pharmaceutical manufacturing, food and beverage production, wastewater treatment, and desalination plants. In chemical plants, the liquid evaporator concentrates solutions and recovers solvents. Pharmaceutical facilities utilize these systems for API concentration and solvent recovery. Food processors employ liquid evaporator technology for juice concentration, dairy processing, and sugar refining. Environmental applications include zero liquid discharge systems and brine concentration. The versatility and efficiency of liquid evaporator technology make it indispensable for operations requiring precise liquid-to-vapor phase transitions with minimal energy consumption and maximum product quality preservation.
Popular Products

Investing in a liquid evaporator delivers substantial operational benefits that directly impact your bottom line and production efficiency. These systems significantly reduce energy costs through heat recovery mechanisms and optimized thermal efficiency, allowing you to process larger volumes while consuming less power compared to traditional evaporation methods. The liquid evaporator minimizes waste disposal expenses by concentrating liquid streams to smaller volumes, reducing transportation and treatment costs for residual materials. You gain precise control over concentration levels, ensuring consistent product quality and meeting exact specifications every production run. The closed-system design of most liquid evaporator units prevents product contamination and volatile compound losses, preserving valuable materials and maintaining workplace safety standards. Operational flexibility stands out as a key advantage, as these systems handle varying feed rates and composition changes without compromising performance or requiring extensive reconfiguration. Maintenance requirements remain minimal due to robust construction and fewer moving parts, translating to reduced downtime and lower long-term ownership costs. The compact footprint of modern liquid evaporator designs saves valuable floor space in your facility while delivering high throughput capacity. Automated controls reduce labor requirements and human error, allowing operators to manage multiple processes simultaneously with confidence. Environmental compliance becomes easier as the liquid evaporator helps you meet discharge regulations and sustainability goals through efficient resource utilization. The scalability of these systems supports business growth, accommodating increased production demands without requiring complete equipment replacement. Quick return on investment results from combined savings in energy, waste handling, labor, and improved product recovery rates. Whether you operate in pharmaceuticals, chemicals, food processing, or environmental management, a liquid evaporator provides the reliability, efficiency, and performance your operations demand for competitive advantage in today's market.

Practical Tips

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

28

Feb

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

View More
Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

28

Feb

Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

View More
Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

28

Feb

Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

liquid evaporator

Advanced Energy Efficiency Technology

Advanced Energy Efficiency Technology

The liquid evaporator incorporates cutting-edge energy recovery systems that dramatically reduce operational costs while maintaining exceptional processing performance. Multiple-effect configurations allow vapor from one stage to provide heating for subsequent stages, cascading thermal energy through the system and achieving energy consumption rates up to seventy percent lower than single-effect designs. Mechanical vapor recompression technology further enhances efficiency by compressing vapor to higher temperatures and pressures, enabling its reuse as a heating medium without requiring additional external energy sources. Plate heat exchangers maximize heat transfer surface area within compact spaces, ensuring rapid and uniform temperature distribution throughout the liquid phase. Thermal insulation systems minimize heat losses to the environment, keeping energy focused where it delivers processing value. Intelligent control algorithms continuously optimize operating parameters based on real-time conditions, automatically adjusting heating rates, pressure levels, and flow patterns to maintain peak efficiency regardless of feed variations. This sophisticated energy management transforms the liquid evaporator into a sustainable processing solution that reduces your carbon footprint while delivering superior economic performance and supporting corporate environmental responsibility initiatives.
Superior Material Compatibility and Versatility

Superior Material Compatibility and Versatility

The liquid evaporator demonstrates exceptional versatility through its ability to handle diverse liquid types ranging from highly corrosive chemicals to sensitive biological compounds without compromising material integrity or product quality. Construction materials including stainless steel grades, titanium, Hastelloy, and specialized coatings provide resistance against aggressive substances, ensuring long service life even in demanding applications. Sanitary designs with polished surfaces and clean-in-place capabilities make the liquid evaporator ideal for pharmaceutical and food processing where hygiene standards are paramount. The system accommodates liquids with varying viscosities, from water-thin solutions to moderately viscous fluids, through adjustable circulation rates and appropriate evaporator configurations. Temperature-sensitive products benefit from vacuum operation capabilities that enable evaporation at reduced temperatures, preventing thermal degradation of heat-labile compounds such as proteins, vitamins, and flavor components. Fouling-resistant designs incorporate features like high-velocity liquid films and turbulence-promoting internals that minimize deposit formation on heat transfer surfaces, extending cleaning intervals and maintaining consistent performance. Whether processing aggressive acids, alkaline solutions, organic solvents, biological extracts, or aqueous solutions, the liquid evaporator provides the material compatibility and operational flexibility essential for diverse industrial applications across multiple sectors.
Precision Control and Process Integration

Precision Control and Process Integration

Modern liquid evaporator systems feature sophisticated automation and control capabilities that enable seamless integration into complex production environments while delivering unprecedented process precision. Programmable logic controllers coordinate all system functions, monitoring dozens of parameters simultaneously including temperatures, pressures, flow rates, concentration levels, and equipment status indicators. Real-time data acquisition systems provide operators with comprehensive process visibility through intuitive graphical interfaces, enabling informed decision-making and rapid response to changing conditions. Automatic feed-forward and feedback control loops maintain target concentration levels within tight tolerances despite variations in feed composition or flow rates, ensuring consistent output quality. Safety interlocks and alarm systems protect equipment and personnel by detecting abnormal conditions and initiating appropriate responses before problems escalate. The liquid evaporator connects seamlessly with upstream and downstream processes through standardized communication protocols, enabling coordinated operation across entire production lines. Remote monitoring capabilities allow technical specialists to assess performance, diagnose issues, and optimize settings from anywhere, reducing response times and minimizing production disruptions. Built-in data logging and reporting functions document all process parameters for quality assurance, regulatory compliance, and continuous improvement initiatives. This comprehensive control architecture transforms the liquid evaporator into an intelligent processing node that enhances overall plant efficiency and product consistency.
Liquid Evaporator Systems: Efficient Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
Liquid Evaporator Systems: Efficient Solutions

Copyright © 2026 Ningbo Lucky Star Import & Export Co., Ltd. All rights reserved.  -  Privacy policy