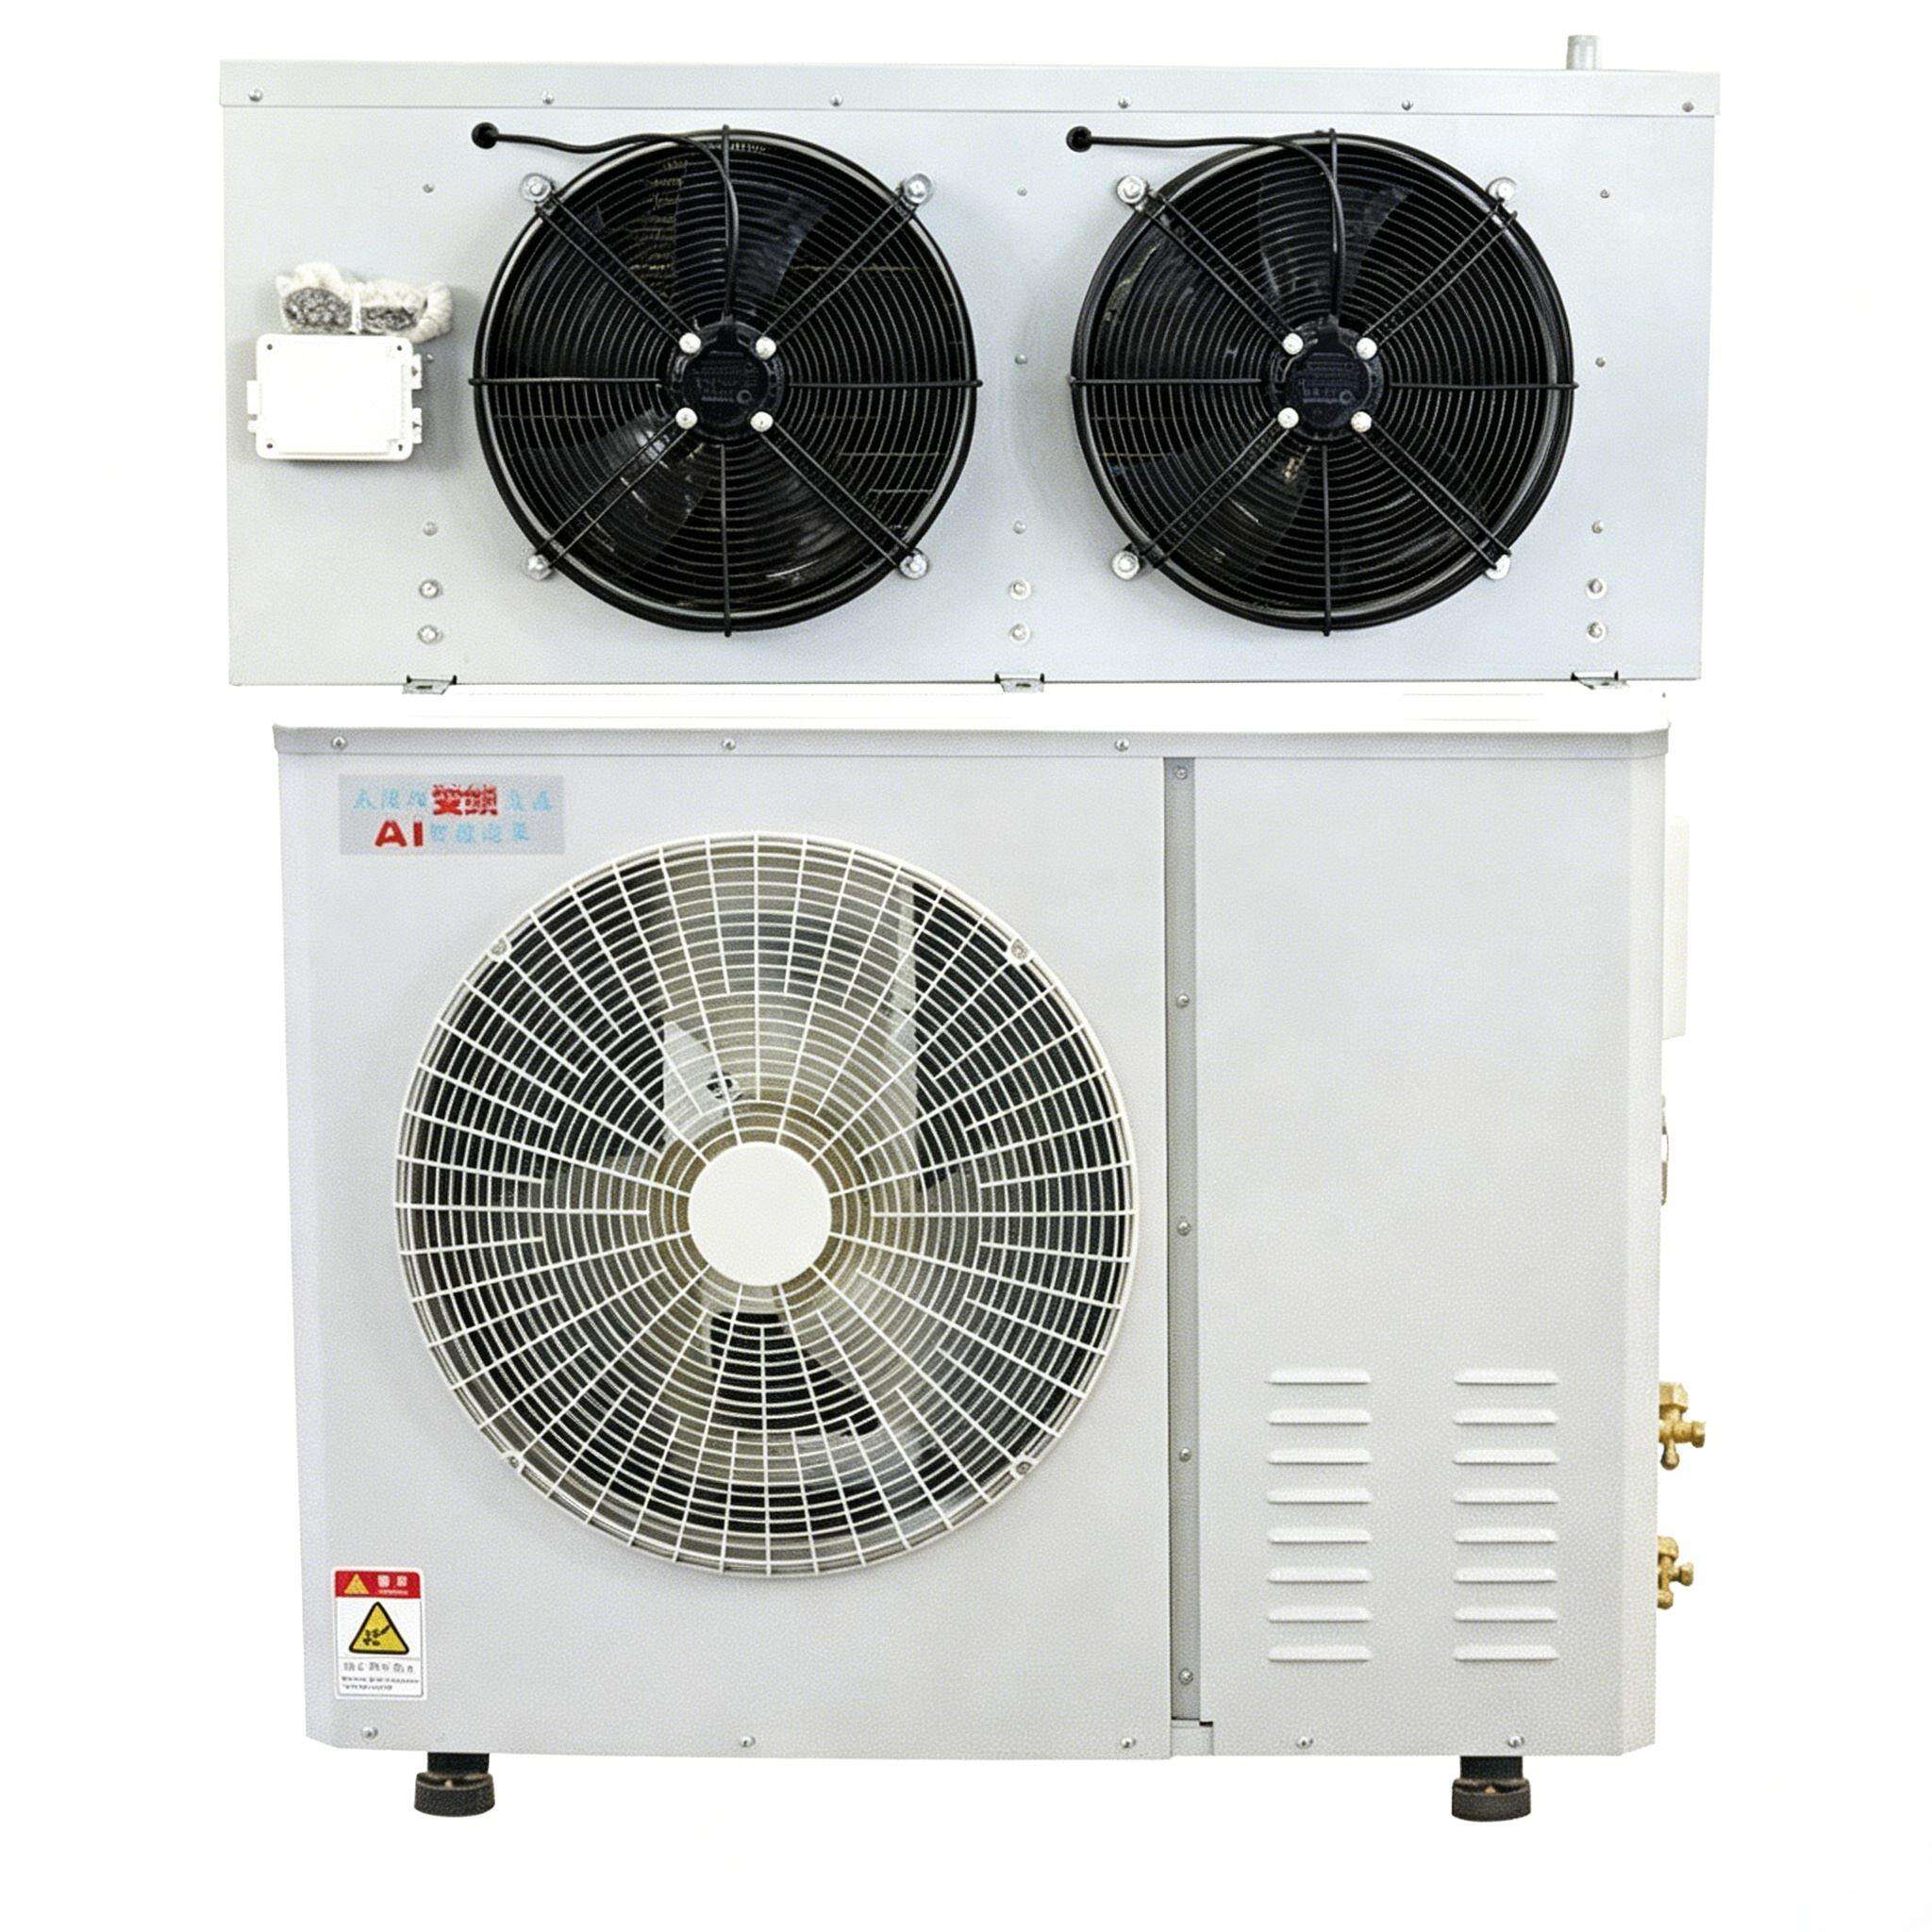
Hermetic Condensing Unit Factory Solutions

All Categories

hermetic condensing unit factory

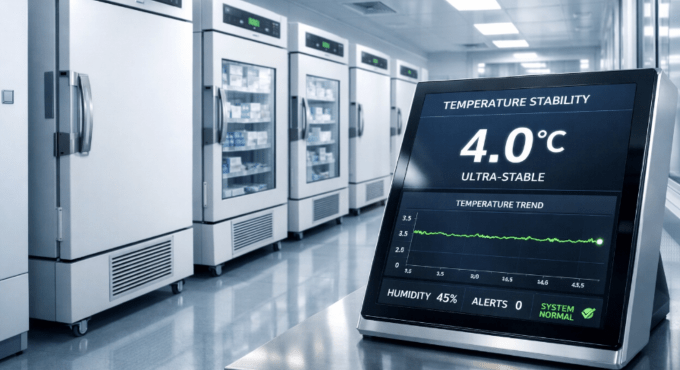
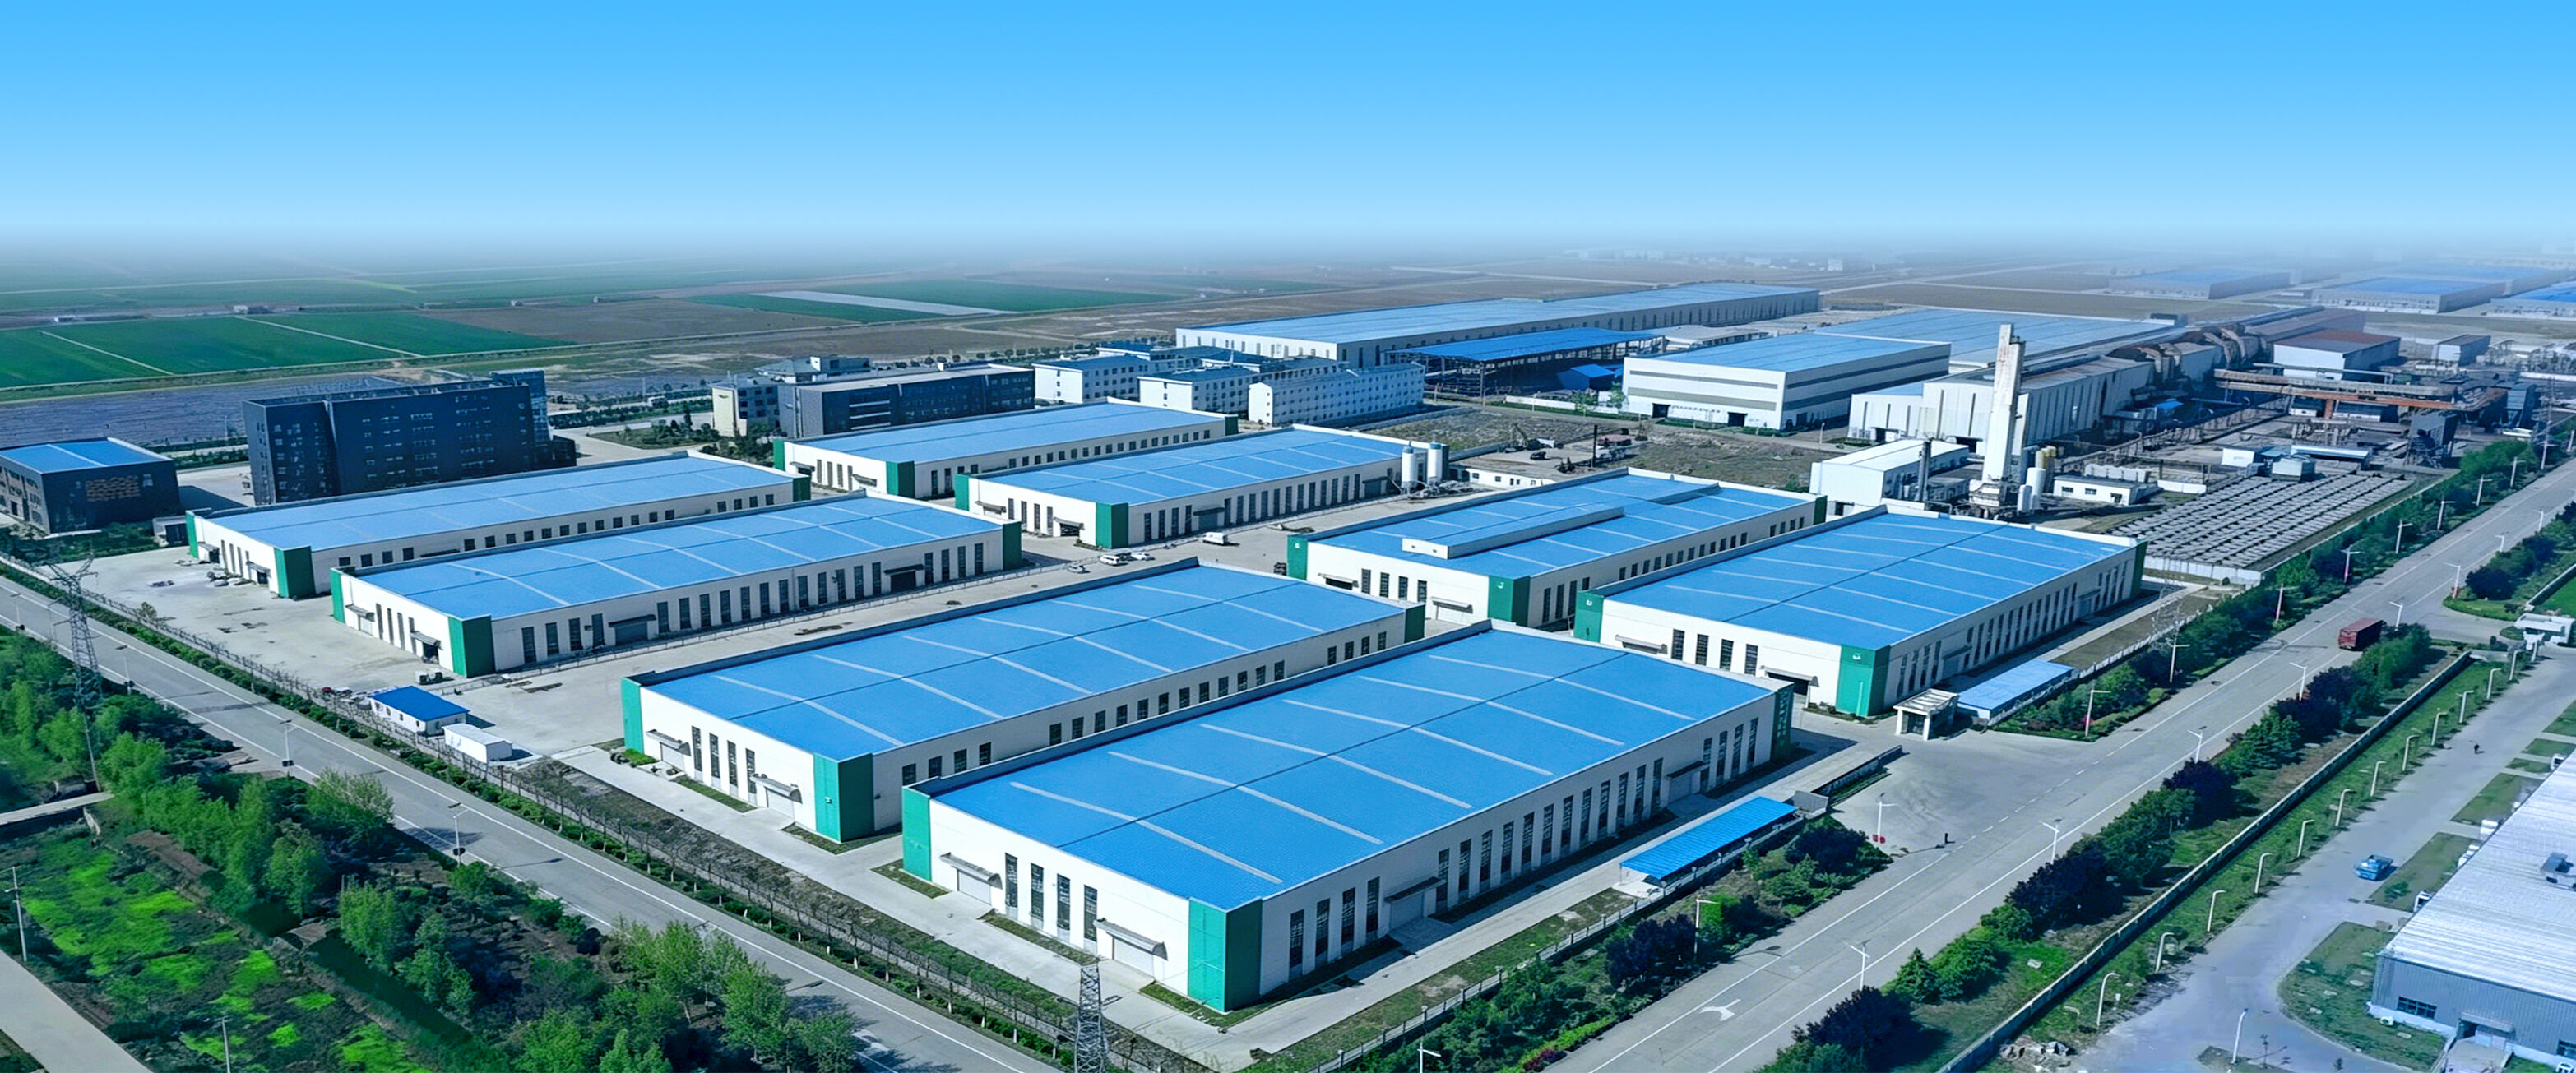
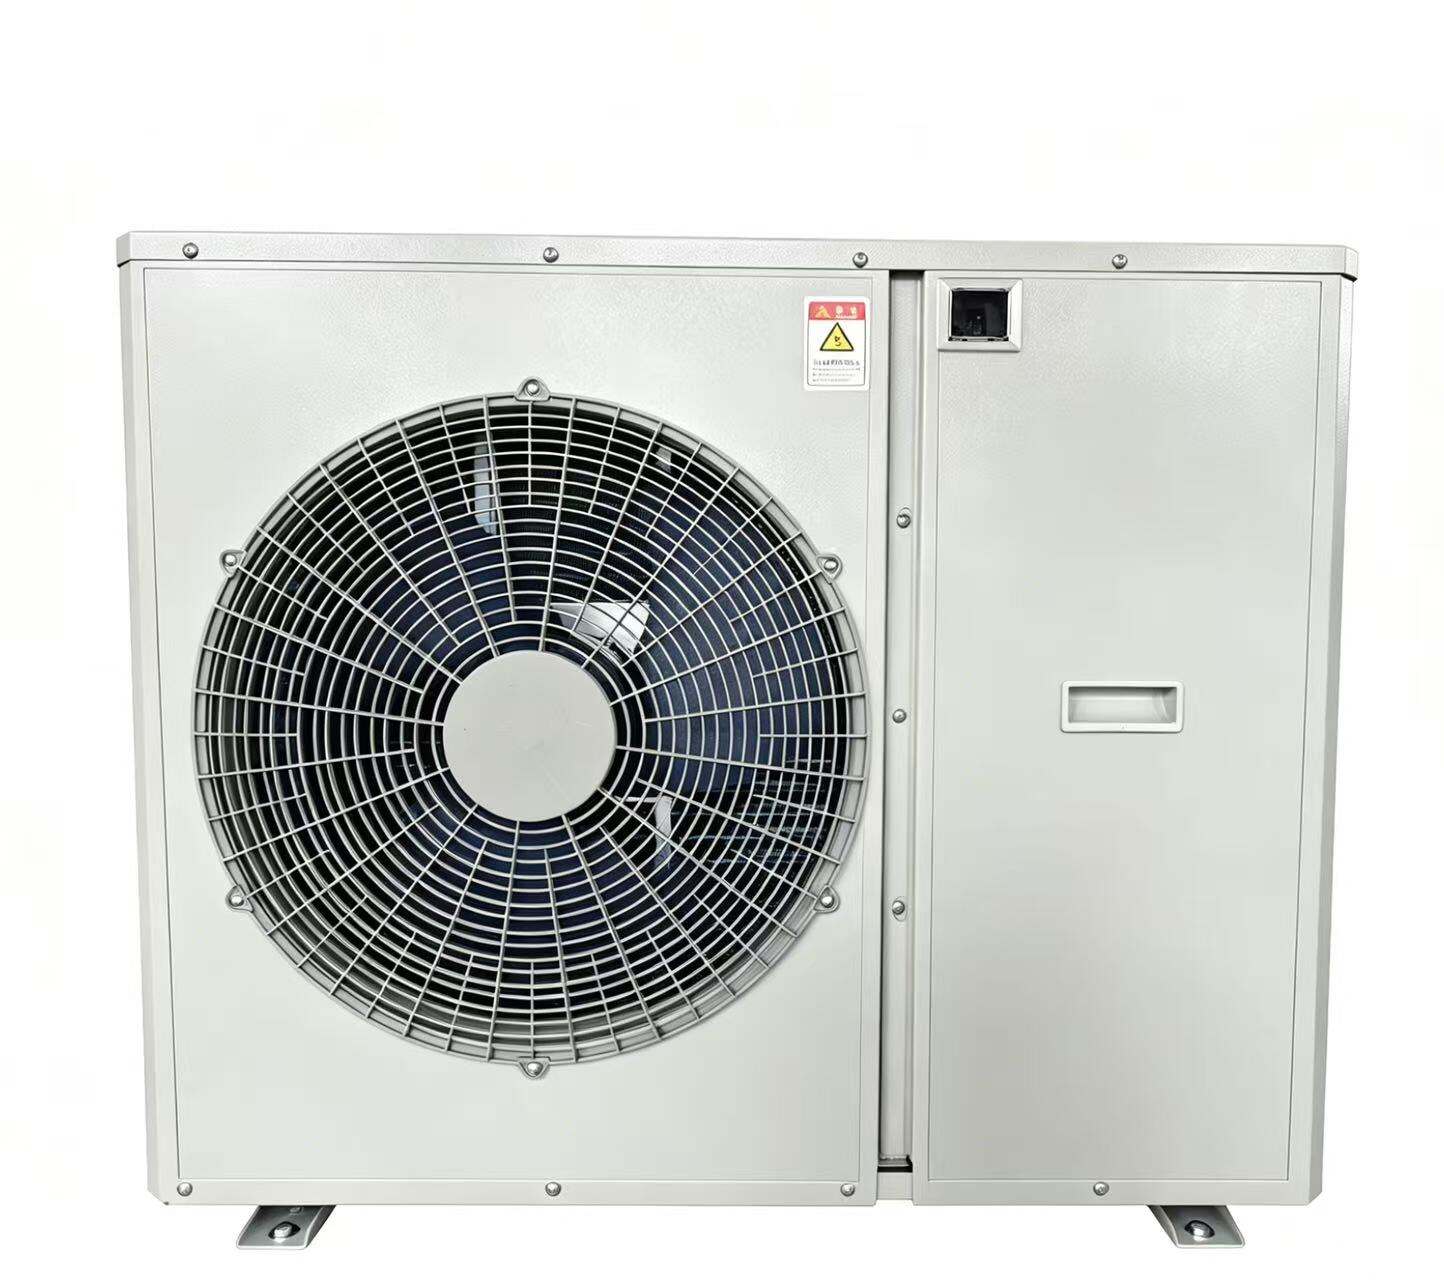
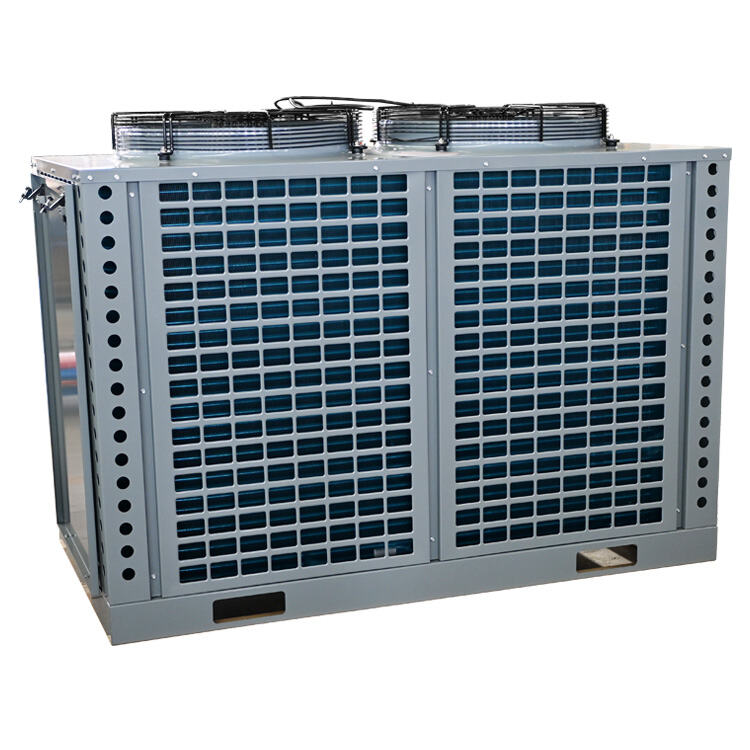
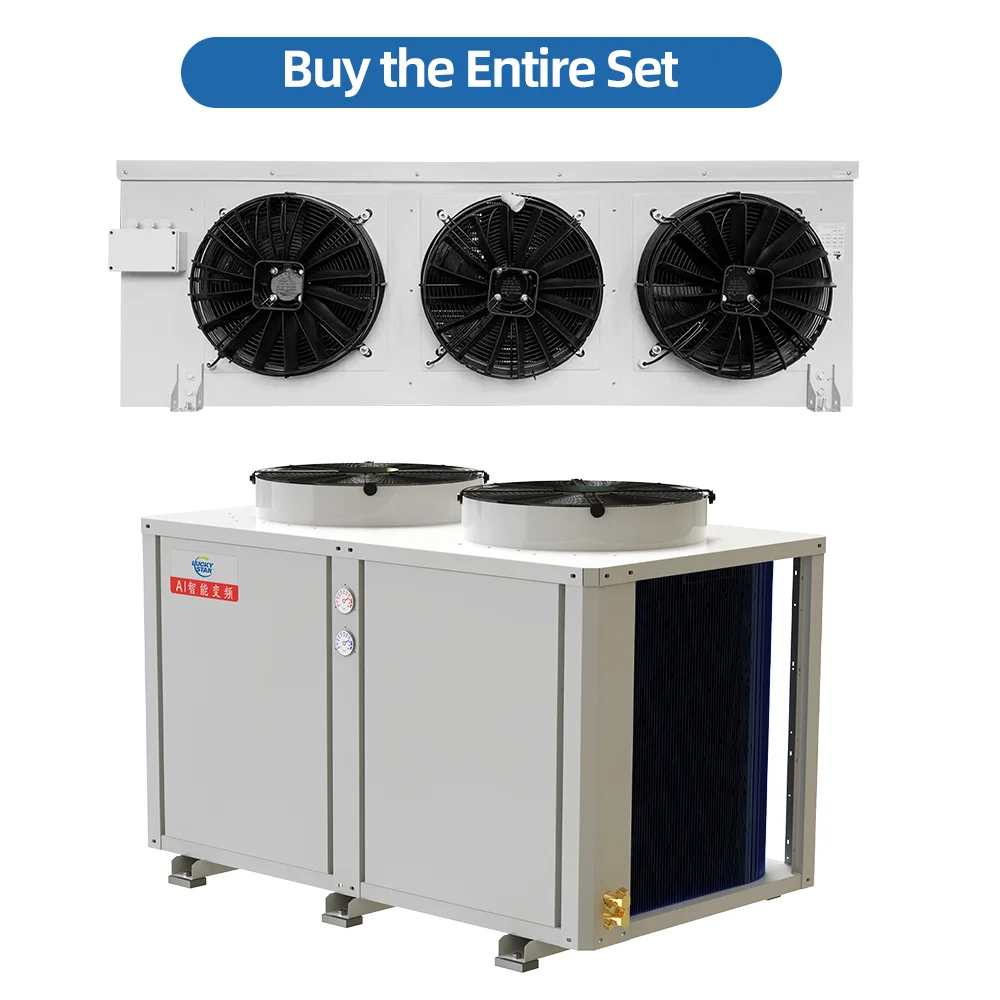
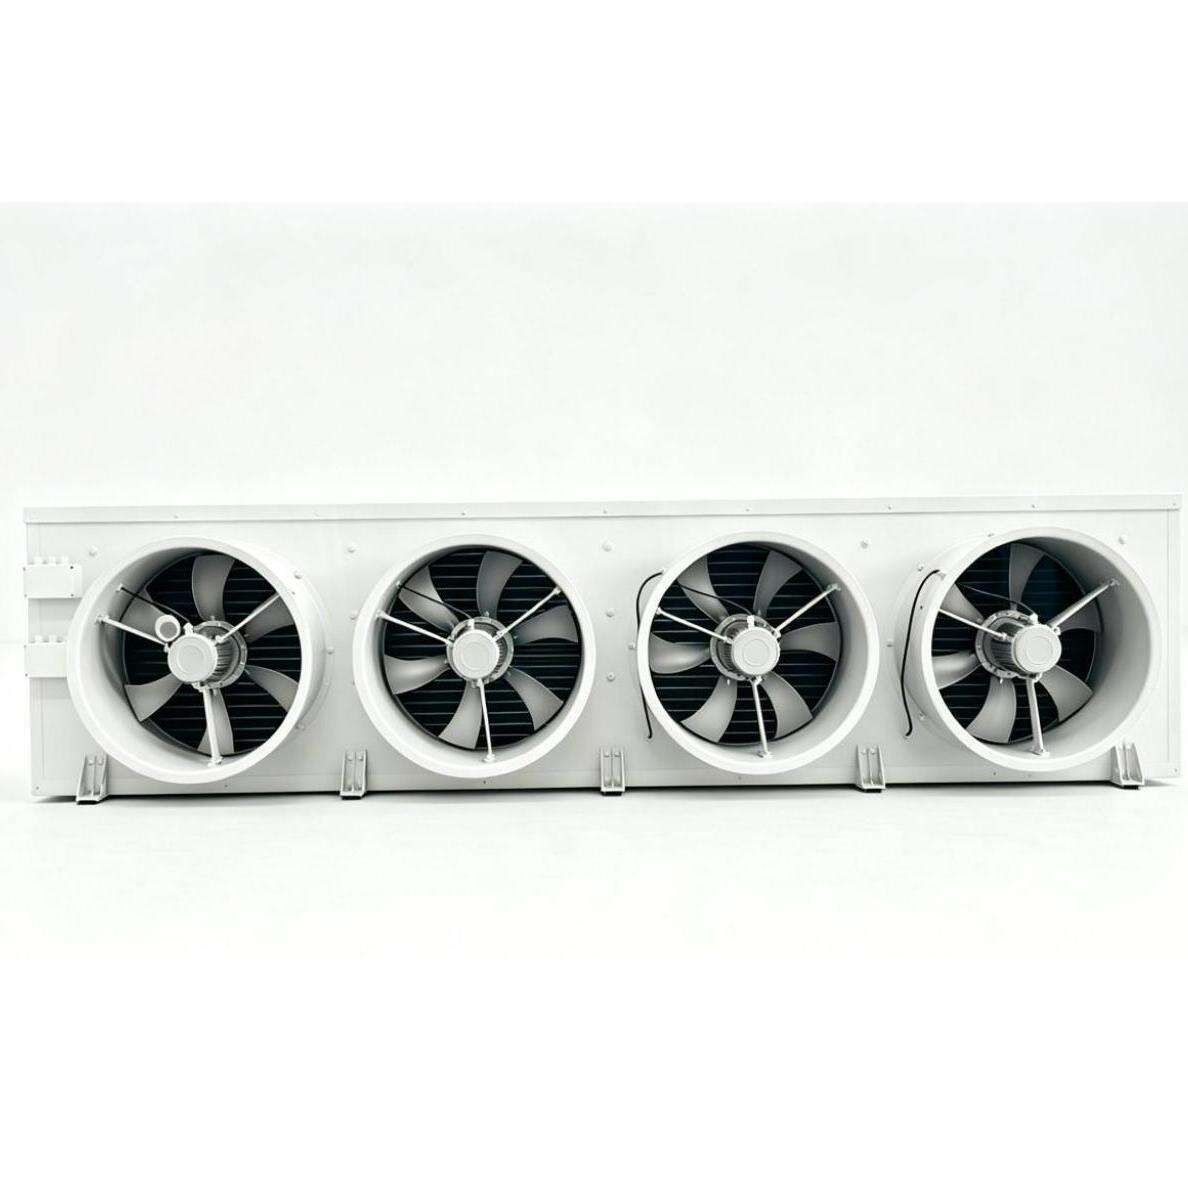
A hermetic condensing unit factory specializes in manufacturing sealed refrigeration systems that integrate compressors, condensers, and related components into compact, efficient cooling solutions. These factories produce units where the compressor motor and pump are enclosed in a welded steel shell, eliminating the need for external shaft seals and preventing refrigerant leakage. The hermetic condensing unit factory employs advanced production lines equipped with precision welding, vacuum testing, and automated assembly systems to ensure consistent quality. Main functions include compressing refrigerant gas, dissipating heat through condenser coils, and maintaining optimal pressure levels for refrigeration cycles. Technological features encompass hermetically sealed designs that enhance reliability, copper tube condenser configurations for superior heat exchange, and integrated electrical controls for seamless operation. Manufacturing processes at a hermetic condensing unit factory involve rigorous quality control protocols, including pressure testing, performance verification, and environmental compliance checks. These units find extensive applications across commercial refrigeration, cold storage warehouses, supermarket display cases, industrial cooling systems, air conditioning installations, and food processing facilities. The hermetic condensing unit factory serves diverse markets by offering customizable capacities ranging from small residential units to large commercial systems, ensuring optimal performance across various temperature requirements and operational demands.
New Product Recommendations

Choosing products from a hermetic condensing unit factory delivers significant practical benefits that directly impact your operational efficiency and bottom line. The sealed design eliminates refrigerant leaks, reducing maintenance costs and ensuring consistent cooling performance over extended periods. You receive units that operate quietly, making them ideal for noise-sensitive environments like restaurants, hotels, and retail spaces where customer comfort matters. Energy efficiency stands out as a major advantage, with modern manufacturing techniques producing units that consume less electricity while delivering powerful cooling, directly lowering your utility bills. The hermetic condensing unit factory implements strict quality standards, meaning you get reliable equipment that minimizes downtime and avoids costly emergency repairs. Installation becomes straightforward because these pre-assembled units arrive ready to connect, saving labor time and reducing installation expenses. Durability proves exceptional since the sealed construction protects internal components from dust, moisture, and contaminants that typically shorten equipment lifespan. You gain operational flexibility through various capacity options, allowing precise matching to your specific cooling requirements without oversizing or undersizing. The compact footprint of units from a hermetic condensing unit factory maximizes usable space in your facility, particularly valuable in urban locations where square footage commands premium prices. Environmental responsibility comes standard, as sealed systems prevent harmful refrigerant emissions and comply with international environmental regulations. Technical support and replacement parts remain readily available, ensuring long-term serviceability. Decision-makers appreciate the transparent specifications and performance data that facilitate accurate system planning and budget forecasting, making procurement processes smoother and more predictable.

Practical Tips

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

28

Feb

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

View More
Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

28

Feb

Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

View More
Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

28

Feb

Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

hermetic condensing unit factory

Advanced Sealed Manufacturing Technology

Advanced Sealed Manufacturing Technology

The hermetic condensing unit factory utilizes state-of-the-art welding and sealing technologies that set industry benchmarks for reliability and performance. Specialized robotic welding systems create perfectly uniform seals around compressor housings, eliminating potential leak points that compromise traditional open systems. This manufacturing precision ensures that refrigerant remains contained throughout the unit's operational life, preventing environmental contamination and maintaining consistent system pressure. Advanced vacuum testing equipment verifies seal integrity on every unit before shipment, guaranteeing that only flawless products reach customers. The factory employs metallurgical experts who select optimal steel grades and thicknesses for housing components, balancing weight considerations with structural integrity requirements. Automated assembly lines maintain strict tolerances during component integration, ensuring perfect alignment between compressors, motors, and mounting systems. Quality control stations monitor critical parameters including vibration levels, electrical continuity, and thermal performance, identifying any deviations before units leave production. This technological sophistication translates into products that deliver exceptional reliability, reduced maintenance requirements, and extended service life, providing customers with superior value and peace of mind throughout years of continuous operation.
Comprehensive Customization Capabilities

Comprehensive Customization Capabilities

A hermetic condensing unit factory offers extensive customization options that address specific application requirements across diverse industries and operating conditions. Engineering teams collaborate with clients to specify precise cooling capacities, voltage configurations, refrigerant types, and mounting arrangements that match unique installation environments. Custom condenser coil designs optimize heat rejection for ambient temperature ranges from arctic cold storage to tropical climates, ensuring consistent performance regardless of location. The factory maintains flexibility in electrical specifications, producing units compatible with various power standards worldwide, facilitating international deployment without compatibility concerns. Specialized treatments including corrosion-resistant coatings, vibration dampening systems, and enhanced insulation packages accommodate challenging operational environments such as coastal installations, high-humidity areas, or industrial settings with airborne contaminants. Clients benefit from prototype development services that allow testing customized configurations before committing to full production runs, minimizing risk and ensuring optimal performance. Technical documentation packages include detailed specifications, installation guidelines, and maintenance protocols tailored to each customized unit, supporting efficient deployment and ongoing operations. This customer-focused approach from the hermetic condensing unit factory enables businesses to obtain precisely engineered solutions rather than compromising with standard offerings, maximizing efficiency and return on investment.
Sustainable Production and Environmental Compliance

Sustainable Production and Environmental Compliance

Modern hermetic condensing unit factory operations prioritize environmental sustainability through responsible manufacturing practices and eco-friendly product designs. Production facilities implement energy-efficient manufacturing processes, utilizing renewable energy sources and waste heat recovery systems that minimize carbon footprints during production. The factory adheres to international environmental standards including RoHS compliance, ensuring products contain no hazardous substances that could harm ecosystems or human health. Refrigerant selection focuses on low global warming potential options, positioning products ahead of regulatory curves and protecting customers from future compliance issues. Recycling programs reclaim metals, plastics, and other materials from production waste streams, diverting materials from landfills and conserving natural resources. Water conservation systems within the hermetic condensing unit factory reduce consumption during testing and cleaning operations, addressing growing concerns about freshwater scarcity. Product lifecycle considerations guide design decisions, emphasizing component recyclability and facilitating end-of-life disassembly for material recovery. Energy efficiency testing ensures manufactured units exceed minimum performance standards, helping end-users reduce operational emissions throughout product lifespans. Transparent environmental reporting provides customers with carbon footprint data and sustainability metrics, supporting corporate responsibility initiatives and green building certifications. These comprehensive environmental commitments demonstrate that the hermetic condensing unit factory balances commercial success with planetary stewardship, delivering products that perform excellently while respecting environmental limits.
Hermetic Condensing Unit Factory Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
Hermetic Condensing Unit Factory Solutions

Copyright © 2026 Ningbo Lucky Star Import & Export Co., Ltd. All rights reserved.  -  Privacy policy