Hermetic Condensing Unit Manufacturer Solutions

All Categories

hermetic condensing unit manufacturer

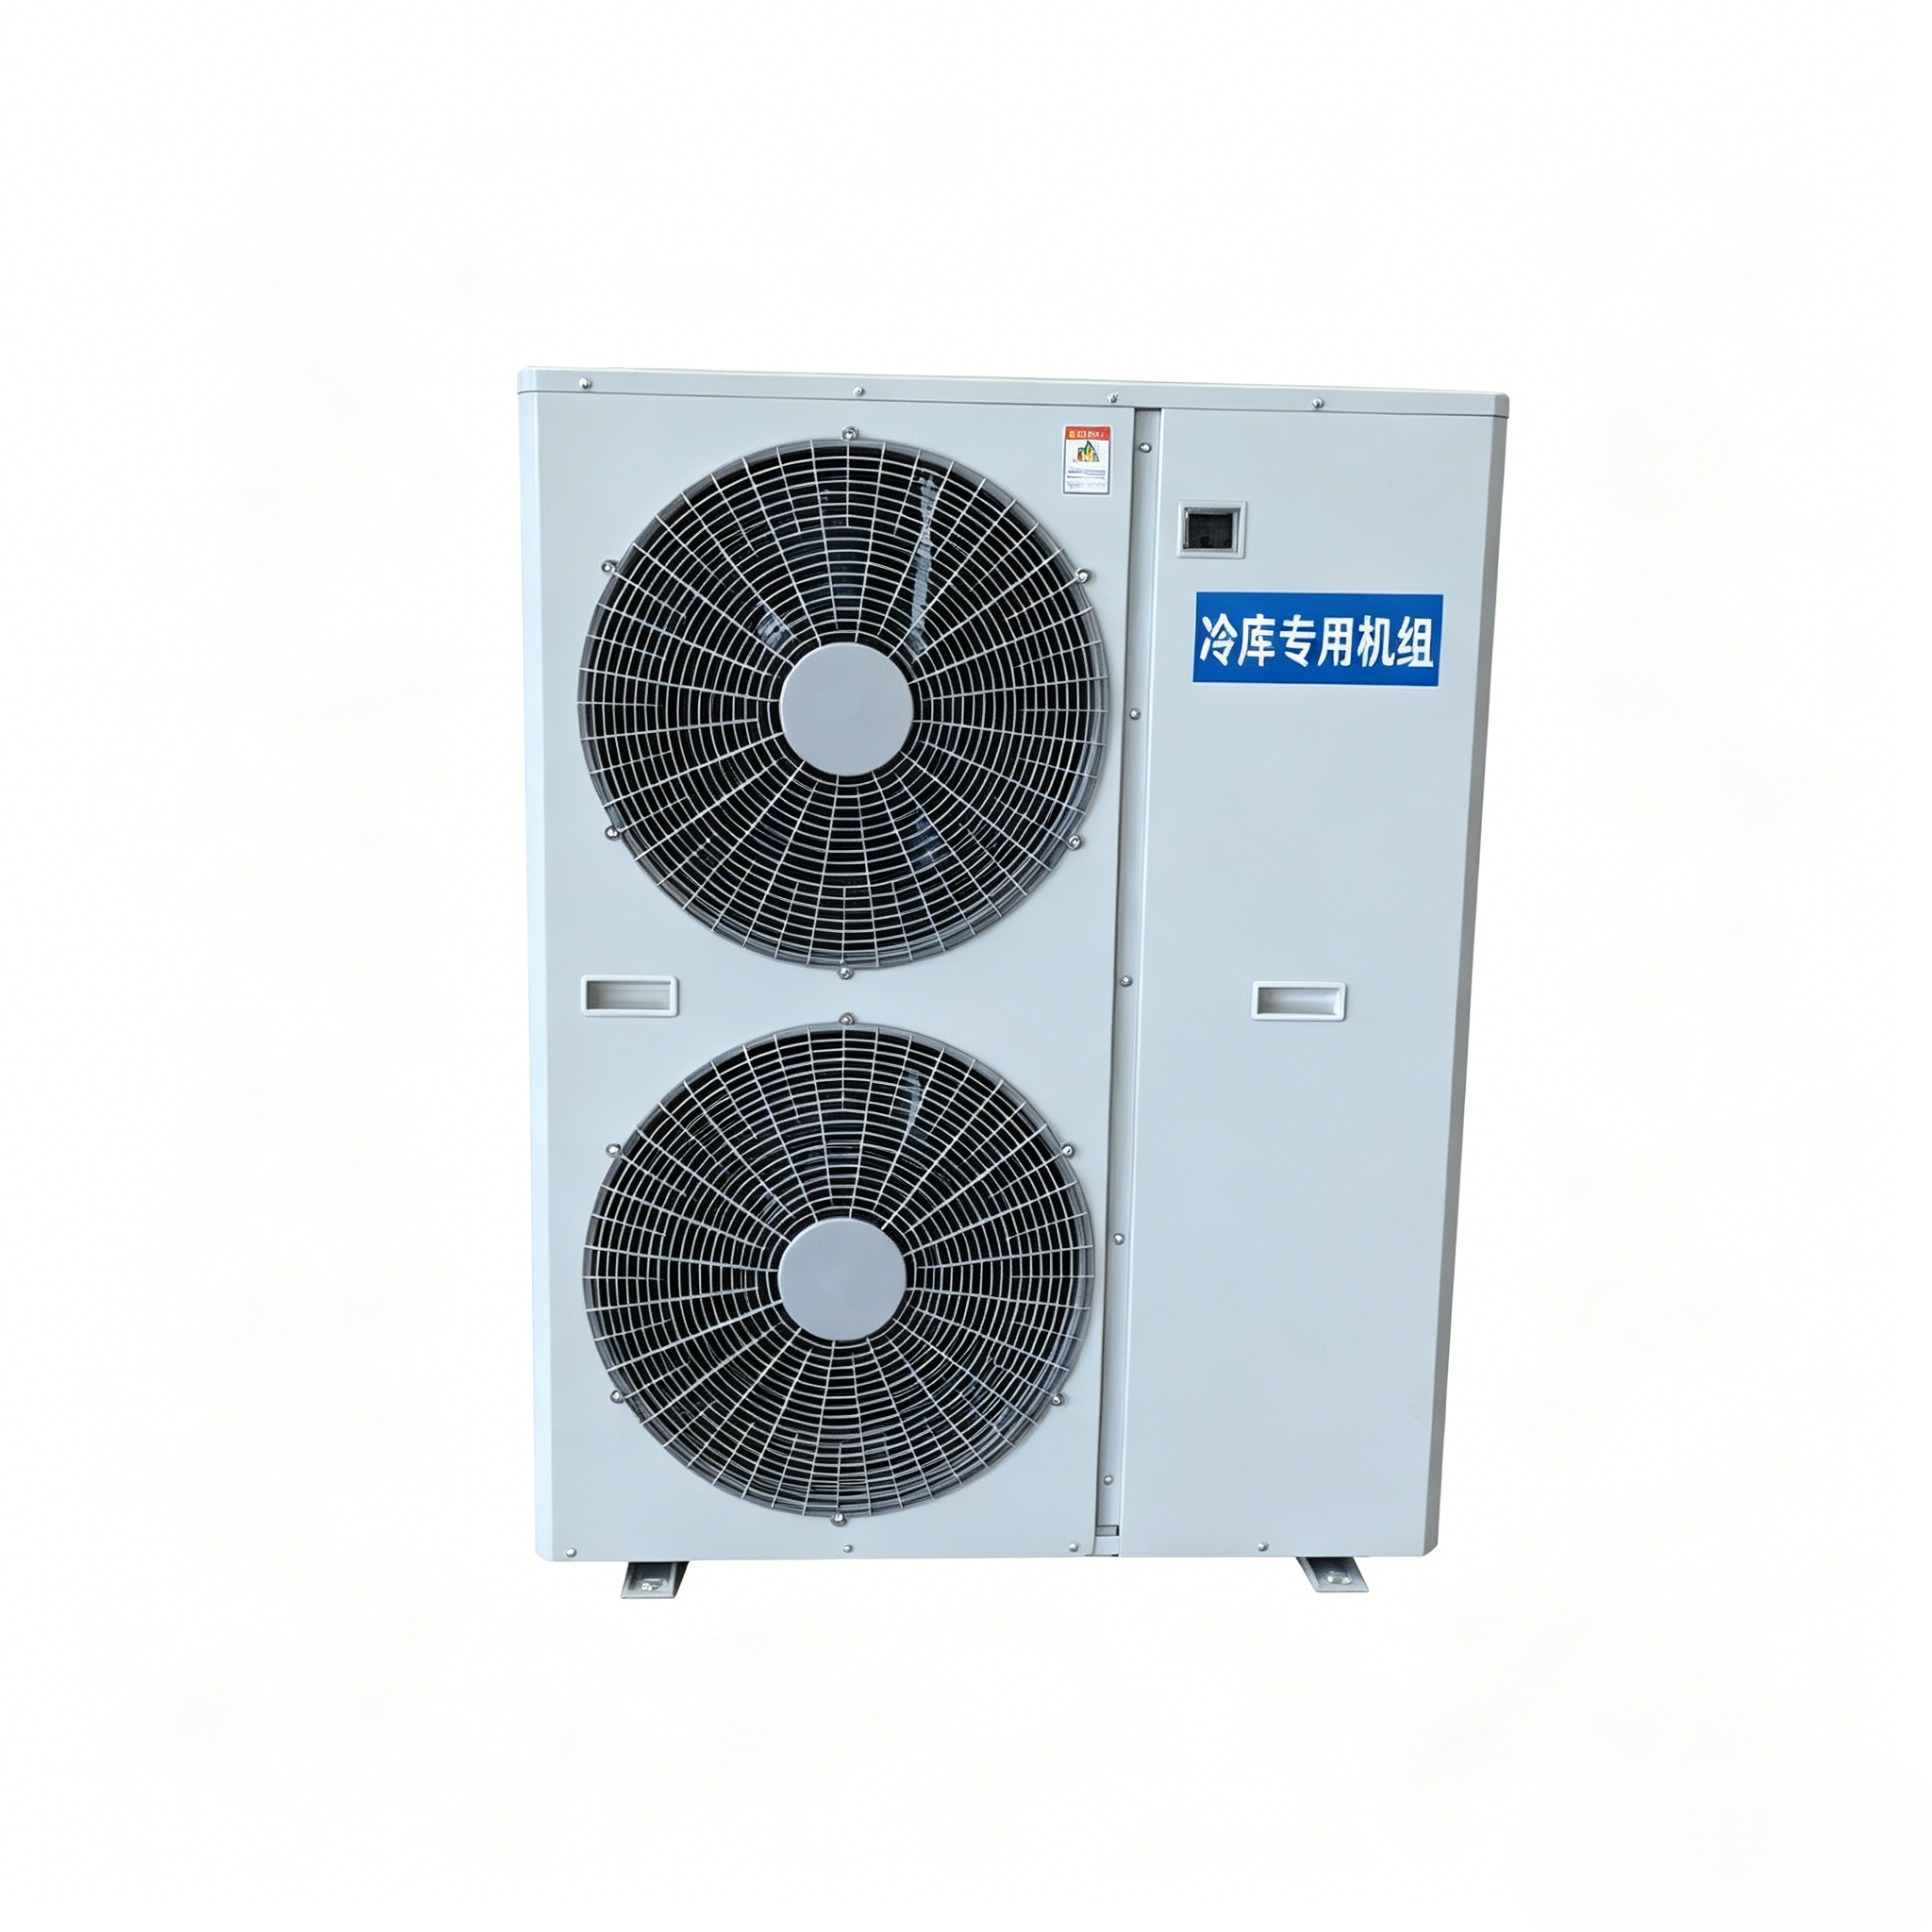
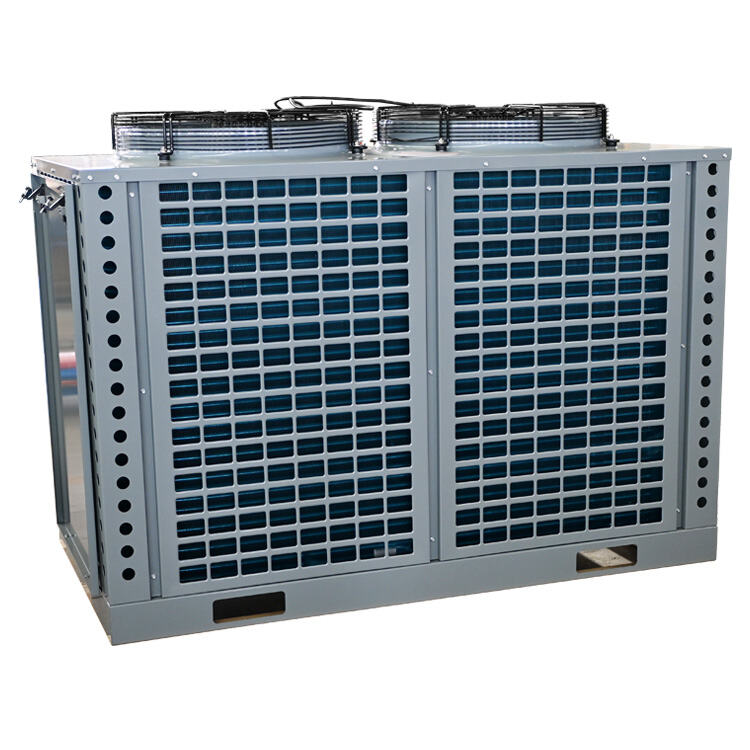
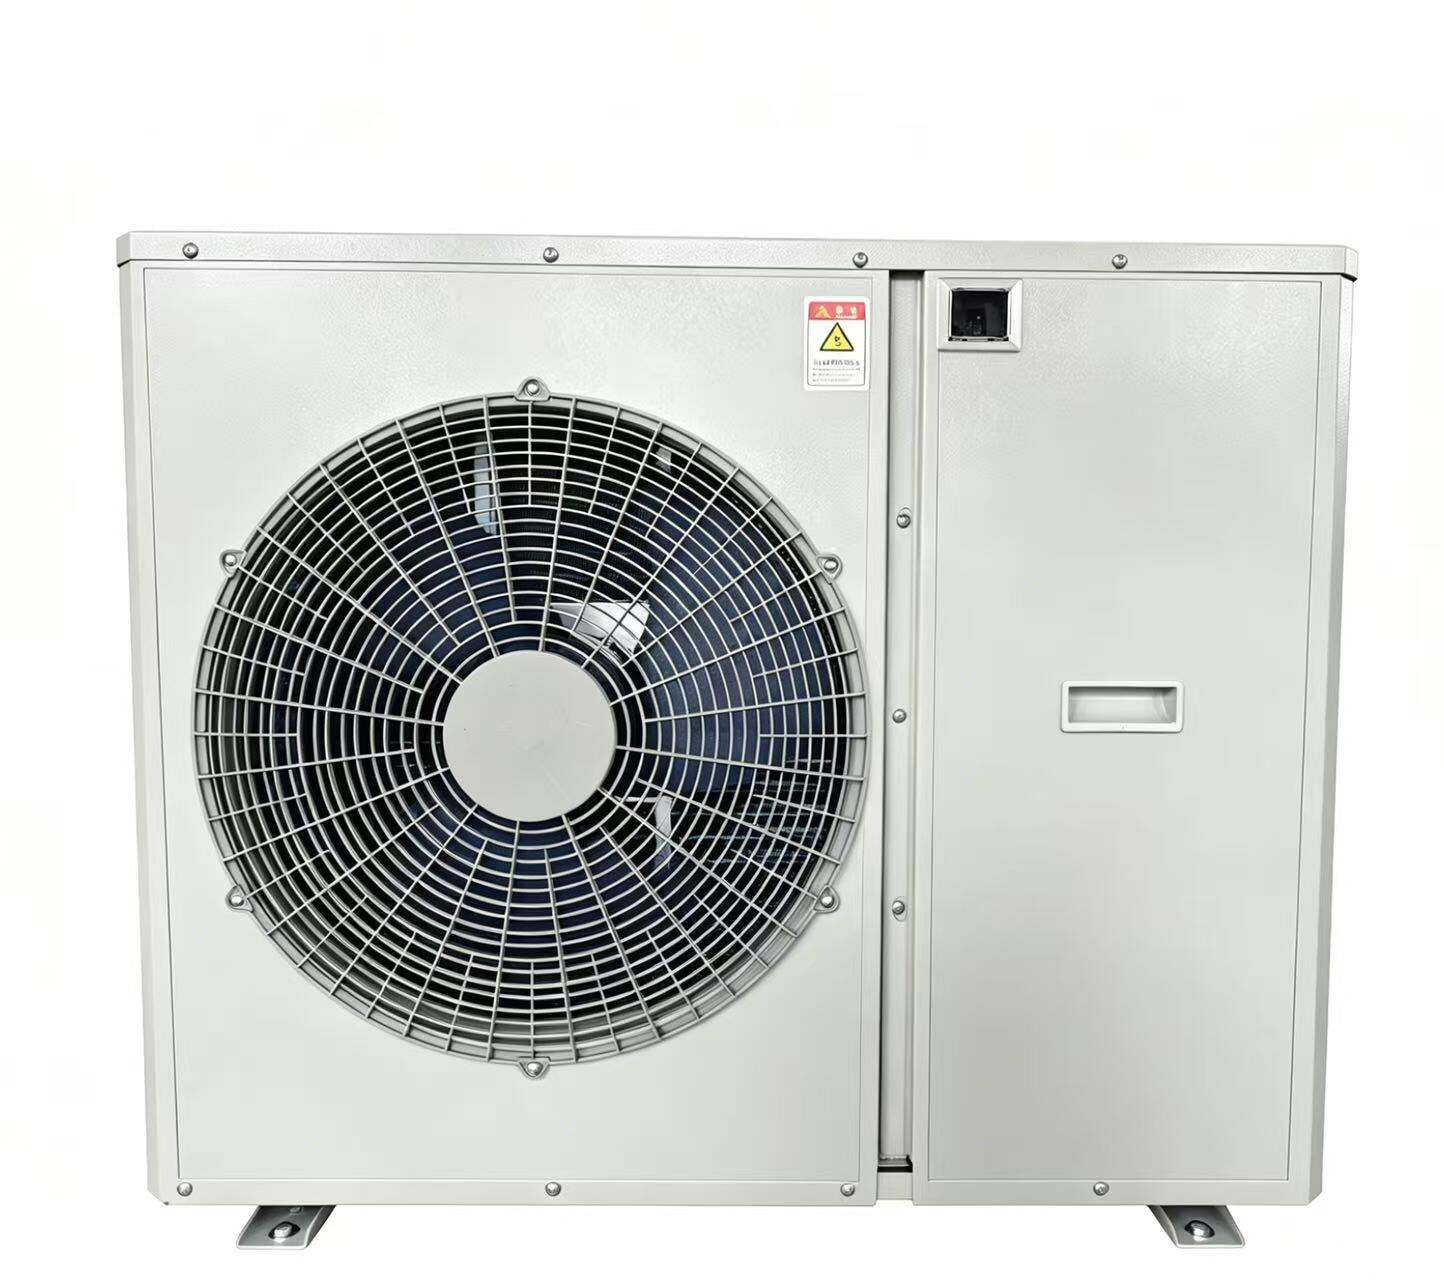
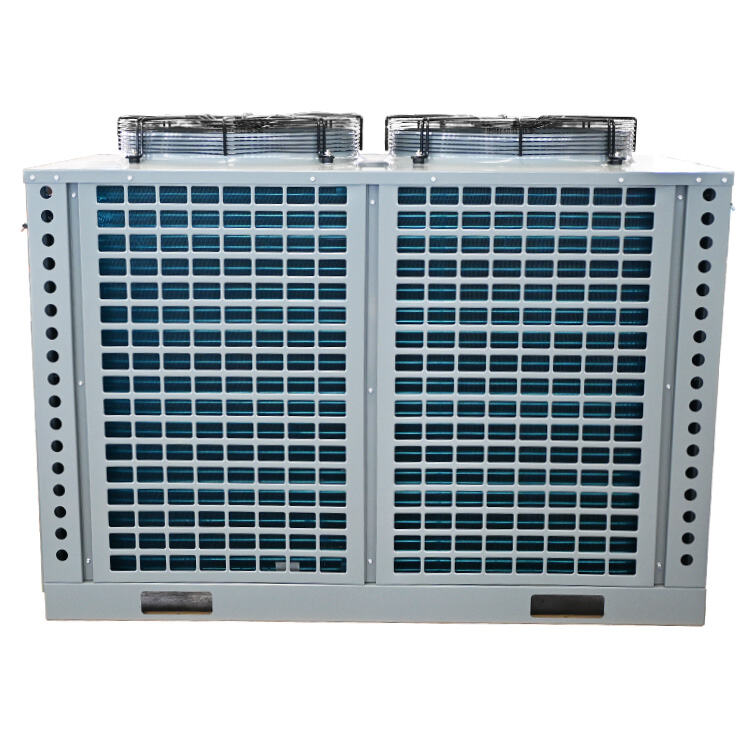
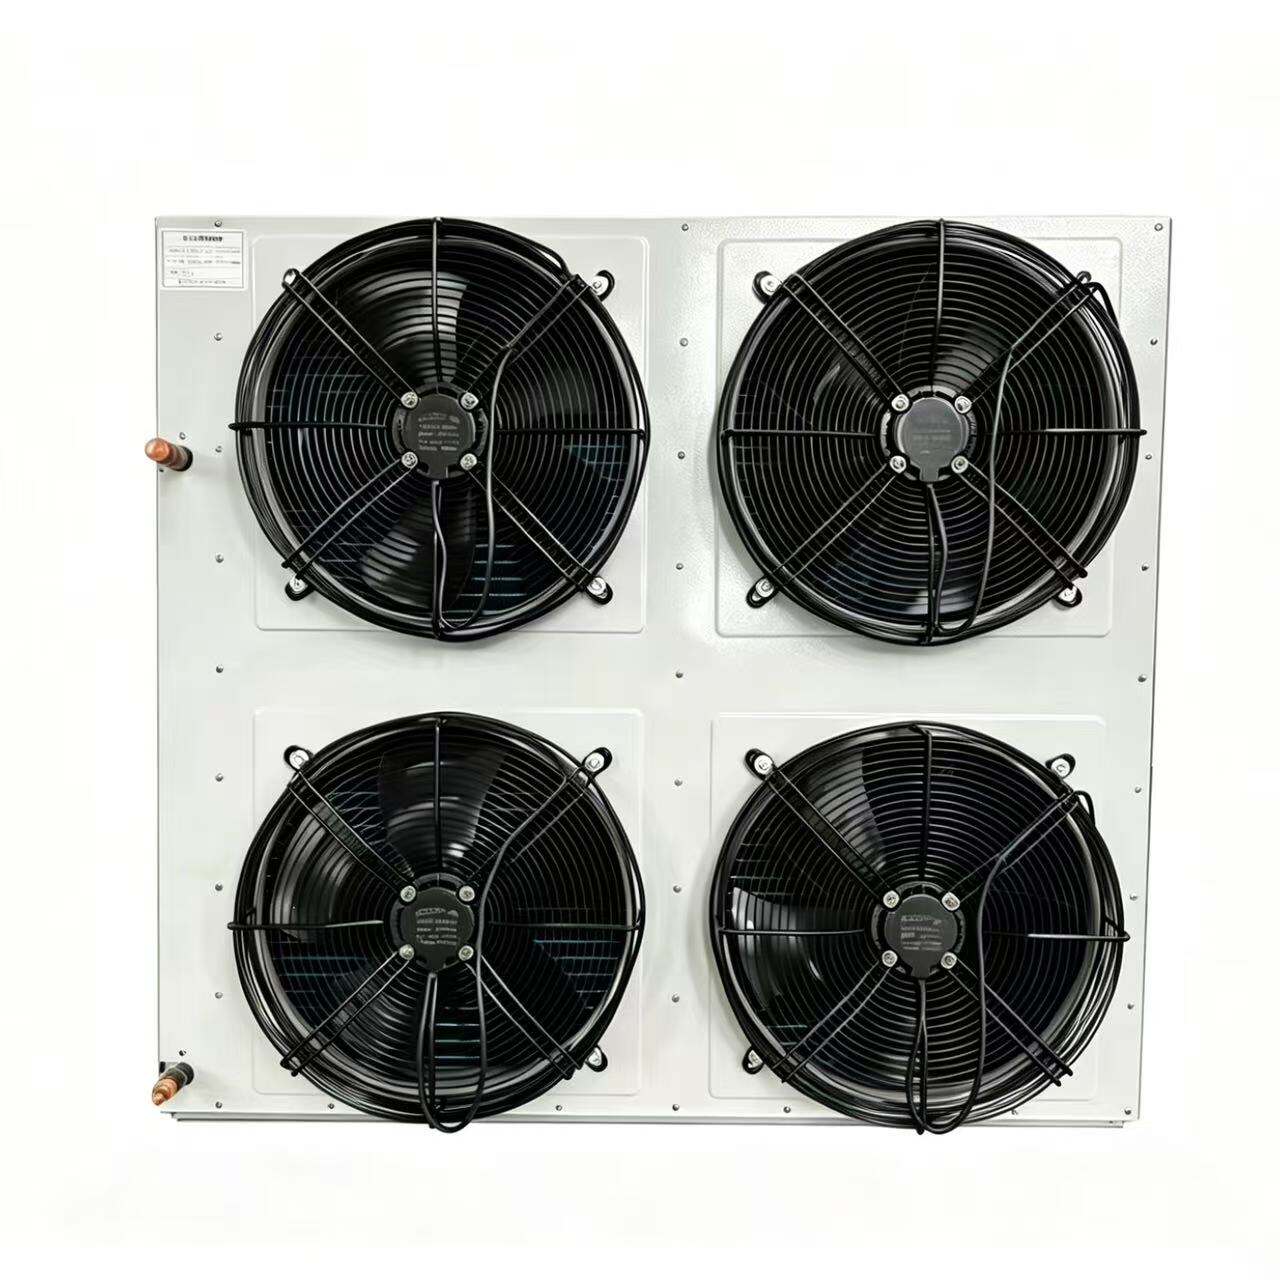
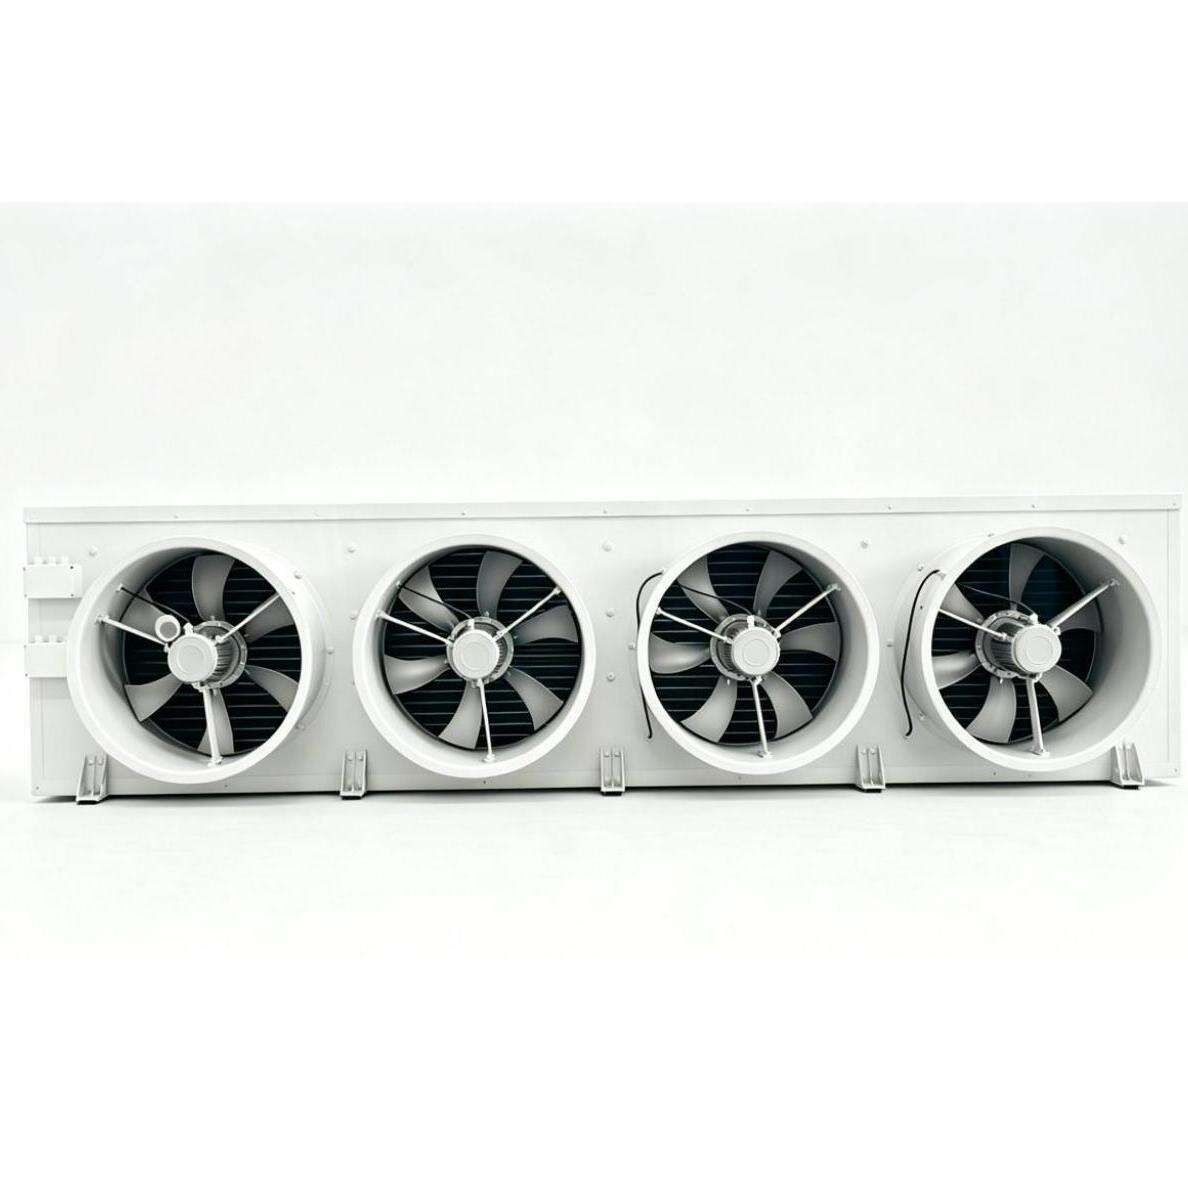
A hermetic condensing unit manufacturer specializes in producing fully sealed refrigeration systems that integrate compressors, condensers, and control components into compact, efficient packages. These manufacturers engineer units where the motor and compressor are enclosed in a welded steel shell, preventing refrigerant leakage and eliminating the need for external shaft seals. The hermetic condensing unit manufacturer focuses on delivering reliable cooling solutions for commercial refrigeration, air conditioning, and industrial process cooling applications. The main function of these units is to compress and condense refrigerant, releasing heat to the surrounding environment while maintaining precise temperature control. Advanced hermetic condensing unit manufacturer facilities employ cutting-edge technologies including variable speed compressors, intelligent control systems, and energy-efficient heat exchangers. These technological features enable superior performance across diverse operating conditions while minimizing power consumption and maintenance requirements. Applications span supermarket refrigeration, cold storage warehouses, food processing facilities, pharmaceutical manufacturing, and HVAC systems. The hermetic condensing unit manufacturer designs products to meet international standards for safety, efficiency, and environmental compliance. Manufacturing processes incorporate rigorous testing protocols to ensure each unit delivers consistent performance, quiet operation, and extended service life. By selecting a reputable hermetic condensing unit manufacturer, buyers gain access to customized solutions, technical support, and products engineered for specific capacity requirements and environmental conditions.
New Products

Partnering with an experienced hermetic condensing unit manufacturer provides numerous practical benefits that directly impact operational efficiency and cost savings. First, these manufacturers deliver products with exceptional reliability because the sealed compressor design eliminates refrigerant leaks and reduces exposure to contaminants, resulting in fewer breakdowns and lower repair costs. This sealed construction means businesses experience less downtime and maintain consistent temperature control, which is critical for preserving perishable goods and maintaining product quality. Second, energy efficiency stands as a major advantage, as a quality hermetic condensing unit manufacturer incorporates advanced compressor technologies and optimized heat exchange systems that reduce electricity consumption by up to thirty percent compared to older models. Lower energy bills translate to significant savings over the equipment lifespan, improving return on investment. Third, the compact design from a hermetic condensing unit manufacturer saves valuable floor space, allowing businesses to maximize facility layout efficiency. Installation becomes simpler and faster, reducing labor costs and minimizing business disruption. Fourth, reduced maintenance requirements mean lower ongoing expenses, as the hermetic design protects internal components from dust, moisture, and environmental factors. Fifth, a reputable hermetic condensing unit manufacturer offers extensive product ranges tailored to specific applications, ensuring buyers find solutions perfectly matched to their cooling capacity needs, ambient conditions, and space constraints. Comprehensive technical support, warranty coverage, and readily available spare parts further enhance buyer value. Finally, compliance with environmental regulations is assured, as leading manufacturers use eco-friendly refrigerants and design units that meet stringent efficiency standards, helping businesses fulfill sustainability commitments while avoiding regulatory penalties.

Tips And Tricks

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

28

Feb

Breakthroughs in Refrigeration Equipment Technology Driving the Future of Cold Chain Solutions

View More
Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

28

Feb

Industry Update Emerging Trends in Global Cold Chain Solutions and Lucky Star's Pivotal Role in Shaping the Future

View More
Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

28

Feb

Precision Cooling The Indispensable Role of Industrial Cooling Systems in the Pharmaceutical Cold Chain

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

hermetic condensing unit manufacturer

Advanced Hermetic Compressor Technology

Advanced Hermetic Compressor Technology

The cornerstone of any hermetic condensing unit manufacturer's product line is the advanced hermetic compressor technology that delivers unmatched reliability and performance. Unlike open compressors with external drive mechanisms, hermetic compressors feature motors and compression components sealed within a single welded housing, eliminating shaft seals that commonly fail and cause refrigerant loss. This sealed design protects internal components from moisture, dust, and contaminants that accelerate wear and reduce lifespan. Leading hermetic condensing unit manufacturer facilities integrate variable speed drive technology that adjusts compressor operation to match real-time cooling demands, significantly reducing energy waste during partial load conditions. The precision-engineered valve systems and balanced rotating assemblies minimize vibration and noise, creating quieter operation suitable for retail environments and temperature-sensitive facilities. Advanced lubrication systems ensure optimal oil distribution under all operating conditions, extending compressor life beyond fifteen years with proper maintenance. The hermetic condensing unit manufacturer employs rigorous testing protocols including endurance trials and extreme temperature cycling to validate performance before products reach customers, ensuring each unit meets exacting quality standards.
Customized Solutions for Diverse Applications

Customized Solutions for Diverse Applications

A professional hermetic condensing unit manufacturer understands that different industries and applications demand tailored cooling solutions rather than one-size-fits-all products. These manufacturers maintain extensive engineering teams dedicated to developing customized configurations that address specific operational requirements, ambient conditions, and space limitations. Whether clients need low-temperature units for frozen food storage operating at minus thirty degrees, medium-temperature systems for fresh produce displays, or specialized units for pharmaceutical cleanrooms, the hermetic condensing unit manufacturer provides precisely engineered solutions. Customization extends to refrigerant selection, with options including traditional and low-global-warming-potential alternatives that comply with evolving environmental regulations. Electrical configurations accommodate various voltage standards and phase requirements across international markets, while control system integration allows seamless connection with building management systems and remote monitoring platforms. The hermetic condensing unit manufacturer offers various condenser designs including air-cooled, water-cooled, and evaporative models suited to different climate zones and facility infrastructure. Mounting configurations range from floor-standing to wall-mounted and outdoor weatherproof enclosures, maximizing installation flexibility. This comprehensive customization capability ensures buyers receive optimized equipment that delivers maximum efficiency and reliability for their specific operational context.
Comprehensive Quality Assurance and Support

Comprehensive Quality Assurance and Support

Distinguished hermetic condensing unit manufacturer companies prioritize comprehensive quality assurance programs and customer support services that extend throughout the product lifecycle. Manufacturing facilities implement ISO-certified quality management systems with documented procedures governing every production stage from component sourcing through final testing and packaging. Each hermetic condensing unit undergoes multiple inspection points including pressure testing, electrical safety verification, refrigerant charge validation, and performance certification under simulated operating conditions. The hermetic condensing unit manufacturer maintains detailed traceability records enabling rapid identification and resolution of any quality concerns. Beyond manufacturing excellence, leading producers provide extensive technical support including application engineering assistance, installation guidance, and troubleshooting resources. Comprehensive documentation packages include detailed specifications, wiring diagrams, maintenance schedules, and parts lists that simplify service procedures. Training programs educate technicians and facility managers on proper installation techniques, operational best practices, and preventive maintenance protocols that maximize equipment lifespan. Warranty coverage typically extends multiple years, reflecting manufacturer confidence in product durability. Established distribution networks ensure replacement parts availability and minimize equipment downtime. This commitment to quality and support from a hermetic condensing unit manufacturer delivers peace of mind and protects customer investments.
Hermetic Condensing Unit Manufacturer Solutions

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000
Hermetic Condensing Unit Manufacturer Solutions

Copyright © 2026 Ningbo Lucky Star Import & Export Co., Ltd. All rights reserved.  -  Privacy policy